- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
BLOG LIST
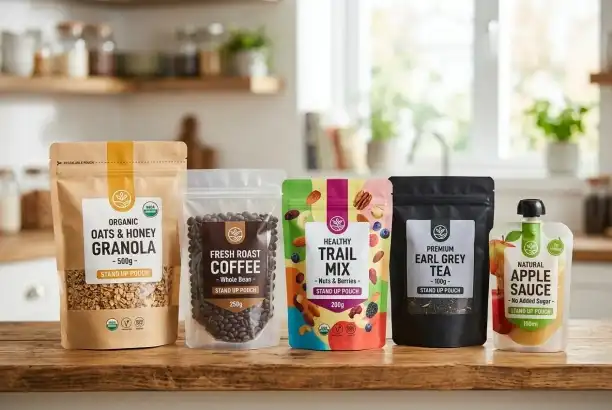
Stand up pouches have revolutionised packaging in many industries by combining functionality and aesthetics. These self-supporting flexible packages have a reinforced bottom gusset to stand upright on retail shelves, maximising visual impact and product freshness. Flexible pouch packaging is preferred by brands of snack foods, coffee, pet treats, and cosmetics for cost-effective, space-efficient product protection and convenience.
Understanding Stand Up Pouches and Their Key Benefits
Flexible pouch packaging has transformed product delivery. Multilayer barrier materials protect contents from moisture, oxygen, and light in these novel packages.
What Makes Stand Up Pouches Different


The structural design includes a bottom gusset for stability without external support. This self-standing feature improves retail display and reduces material use compared to boxes or jars. Multiple film layers—each providing a protective or functional purpose—are laminated into a durable, flexible structure during manufacturing.
Core Advantages for Procurement Teams
Procurement experts know these bundles provide supply chain value. Compact design saves storage and shipping costs and maximises shelf space. Advanced barriers reduce spoiling and refunds by extending product shelf life. Resealable zippers, tear notches, transparent windows, and high-definition printing help brands differentiate products while meeting functional needs. Our VMPET material architecture protects products from external influences that degrade quality, keeping them fresh from manufacturing to consumption.
Regulatory Compliance and Safety Standards
FDA- and BRC-certified food-grade materials assure direct food contact safety. SGS and other third-party testing verify barrier performance and material compliance. Working with qualified manufacturers that understand international standards and paperwork reduces supply chain compliance risk for brands entering regulated markets.
The Most Popular Uses of Stand Up Pouches Across Industries
Stand up pouches, a flexible pouch packaging, are popular across several industry categories owing to their performance and customer acceptability.
Food and Beverage Applications
The food business has used flexible packaging instead of jars, cans, and cartons. Oxygen barrier properties keep aromatics fresh and prevent staleness, which roasters like. Dried fruits and nuts stay crisp in moisture-resistant structures. Portion control and resealable closures help snack manufacturers. Spice manufacturers use transparent windows to display quality and exclude dampness. Light-blocking laminates preserve tea blends. These examples show how material selection affects product performance and customer satisfaction.
Pet Food and Treat Packaging
Pet brands have quickly adopted flexible pouches for dry food and treats. Pet owners may easily open and reseal the package, which protect product freshness. Barrier films prolong shelf life without preservatives by preventing fat oxidation and rancidity. High-impact graphics can convey quality and stand out in competitive retail environments. Shipping costs are lower with the lightweight construction, boosting distribution economics.
Health and Wellness Products
Supplement companies use stand up pouches for protein powders, vitamins, and superfood blends to protect them from moisture and oxygen. Resealable zippers prevent product deterioration and keep products fresh. From single-use packets to bulk containers, custom sizes are available. Modern, simple packaging for active lives matches wellness brand concept.
Non-Food Market Applications
Flexible pouches carry cosmetics, personal care, home cleansers, and industrial components. Cosmetic manufacturers provide samples and travel quantities in smaller pouches. Cleaning product makers value chemical resistance and longevity. Reclosable bags from hardware vendors protect tiny components from loss and contamination. Moisture barriers and UV protection help seeds and fertilisers. Material attributes and functional aspects must match product characteristics and user demands for each application.
How to Choose the Right Stand Up Pouch for Your Procurement Needs

Selecting effective packaging involves careful study of performance, cost, and market acceptability variables.
Material Property Assessment
Product sensitivity drastically affects barrier needs. Coffee needs strong oxygen barriers to stay fresh. Product moisture-sensitivity requires water vapour resistance. Light-sensitive contents need opaque or metallized films. Our high-performance VMPET structure provides multi-barrier protection for demanding applications. Procurement teams should set barrier performance objectives based on shelf life and storage circumstances, not general material descriptions.
Functional Features and Convenience Elements
Brand impression and repeat purchases depend on user experience. No scissors or equipment needed for easy-tear notches. Resealable zippers preserve freshness. Spouts provide regulated liquid and sauce pouring. Retail display versatility is enhanced with hanging holes. Degassing valves offgas coffee without damaging packages. Each feature increases functionality but also increases manufacturing complexity and cost, requiring brand positioning and target market expectations-based decisions.
Print Quality and Branding Capabilities
Packaging is a silent salesperson, so visual impact is crucial for purchases. Rotogravure printing maintains brand standards by reproducing colours consistently over huge manufacturing runs. Our 11-color printing allows sophisticated designs, gradients, and eye-catching photos. Spot UV coating gives a superior feel. Matte finishes look natural, while glossy surfaces look fresh and high-quality. Design elements should convey brand identity and regulatory and product information.
Supplier Evaluation Criteria
Quality control and filling line performance depend on manufacturing uniformity. Dimensional correctness guarantees automated equipment compatibility. Seal integrity avoids contamination and leaking. Colour constancy ensures brand standards throughout reorders. Lead time reliability aids inventory planning and market response. Our 25 years of manufacturing expertise and solid quality procedures ensure procurement teams' operational stability. Evaluation of suppliers based on certifications, manufacturing capacity, technical assistance, and long-term relationship potential decreases supply chain risk.
Sustainable and Eco-Friendly Stand Up Pouch Solutions

Environmental sustainability is a procurement issue as rules tighten and customers expect sustainable products.
Recyclable Material Options
Traditional multilayer constructions of stand-up pouches are complicated, making recycling difficult. Innovative mono-material developments employing polyethylene or polypropylene across all layers allow recycling using current streams. Our recyclable packaging supports circular economy concepts and barrier performance. Recycling icons and disposal instructions may show brands' environmental efforts.
Compostable and Biodegradable Alternatives
Renewable plant-based films provide end-of-life benefits for some applications. Dry items with shorter shelf lives benefit from these materials. Certified compostable packaging corresponds with environmental positioning for brands entering sustainability-focused markets, but performance restrictions demand careful application matching.
Environmental Manufacturing Practices
Production processes have a big environmental impact for stand up pouches. Our regenerative thermal oxidizer (RTO) reduces air pollution by capturing and neutralising volatile organic compounds during printing and laminating. Equipment that saves energy reduces the carbon footprint per unit. Waste reduction initiatives optimise production planning to reduce scrap. Procurement teams increasingly assess suppliers based on environmental management systems since manufacturing practices impact regulatory compliance and company sustainability.
Practical Tips for Using and Recycling Stand Up Pouches
From filling to disposal, packaging performance must be optimised.
Optimizing Filling Line Performance
Dimensional uniformity makes vertical form-fill-seal and pre-made pouch filling systems work well. Material thickness impacts machine compatibility and handling. Heat seal parameters must match film structure for dependable closures without barrier damage. Our technical team tests filling equipment compatibility and recommends parameters to avoid expensive production delays. Operators learn pouch handling, orientation verification, and quality inspection to guarantee output uniformity.
Maintaining Product Freshness and Quality
Good storage protects empty pouches and full items. Controlled temperature and humidity avoid material deterioration before use. Sealed storage prevents contamination and odour absorption. Inventory rotation keeps materials within specs. To prolong shelf life, store items according to manufacturer instructions after filling. Clear on-package instructions are essential for consumer satisfaction because resealable closures only work when opened.
Supporting Recycling Infrastructure
Labelling and consumer education can help brands dispose of waste while recycling capabilities develop. Consumers make better choices by knowing the main material composition. Working with store take-back programs helps gather goods not accepted curbside. Collaboration with recycling and material recovery organisations improves infrastructure. Brands are sustainability leaders when they buy recyclable structures to reduce waste before widespread recycling.
Conclusion
Flexible pouch packaging has been popular in the food, pet, health, and consumer goods sectors because of its protection, convenience, cost-efficiency, and sustainability. These flexible packages enhance brand visibility and consumer experience for coffee, snacks, supplements, and cosmetics. Reviewing barrier qualities, functional features, printing capabilities, and supplier dependability helps choose the correct solution to ensure package performance throughout manufacturing and market lifespan. As sustainability demands grow, recyclable and compostable alternatives help companies accomplish environmental goals without sacrificing product safety. The packaging landscape changes, yet flexible pouches' space efficiency, barrier performance, and design flexibility keep them relevant across market sectors, and stand up pouches remain a prominent example of how this format combines self-supporting structure with the same protective and aesthetic advantages demanded by modern brands.
FAQ
1. What products work best in stand up pouches?
These flexible packages excel for dry and semi-moist products including snacks, coffee, nuts, dried fruits, pet treats, protein powders, spices, and granular foods. Spouted versions accommodate liquids, sauces, and beverages. Products requiring oxygen and moisture protection particularly benefit from barrier film structures that extend shelf life compared to traditional packaging.
2. How do I determine the right pouch size for my product?
Calculate required volume based on product weight or volume plus appropriate headspace for sealing and gas release if applicable. Consider retail presentation and handling convenience—oversized pouches waste material while undersized versions appear insufficient. Our design team provides sizing recommendations based on your specific product characteristics and target market positioning.
3. Can stand up pouches run on automated filling equipment?
Yes, these packages work with both vertical form-fill-seal machines using rollstock film and pre-made pouch filling systems. Material specifications and dimensional tolerances must match equipment requirements. We provide technical support ensuring compatibility with your existing filling lines or assist with equipment selection for new operations.
Partner With a Trusted Stand Up Pouches Manufacturer

Guoshengli Packaging brings over 25 years of flexible packaging manufacturing expertise to brands seeking reliable, high-performance pouch solutions. Our comprehensive capabilities include advanced VMPET material construction with superior barrier protection, up to 11-color rotogravure printing with spot UV enhancement, and complete customization from material selection through final production. We maintain ISO 9001, BRC, and FDA certifications, ensuring consistent quality and regulatory compliance for international markets. Our production capacity—featuring 7 printing lines, 6 laminating machines, and 49 converting machines—supports both urgent orders with 7-10 day digital printing and standard production with 15-20 day lead times. Whether you need packaging for snacks, coffee, pet treats, supplements, or specialty products, our technical team provides comprehensive consultation on material properties, barrier optimization, and filling line compatibility. Contact our experts at sales@guoshengpacking.com to discuss your specific requirements and discover how our proven manufacturing systems deliver packaging that performs consistently, order after order. Experience the difference of working with a stand up pouches supplier committed to reducing your operational risk while supporting long-term growth.
References
1. Robertson, Gordon L. "Food Packaging: Principles and Practice, Third Edition." CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Volume 72, 2007.
3. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. "Plastics Packaging: Properties, Processing, Applications, and Regulations, Third Edition." Hanser Publications, 2015.
4. Yam, Kit L. "The Wiley Encyclopedia of Packaging Technology, Third Edition." Wiley, 2009.
5. Coles, Richard and Mark Kirwan. "Food and Beverage Packaging Technology, Second Edition." Wiley-Blackwell, 2011.
6. Brody, Aaron L. and Kenneth S. Marsh. "The Wiley Encyclopedia of Packaging Technology, Second Edition." John Wiley & Sons, 1997.
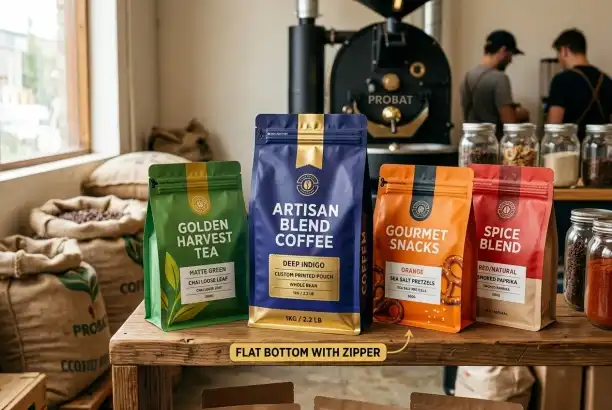
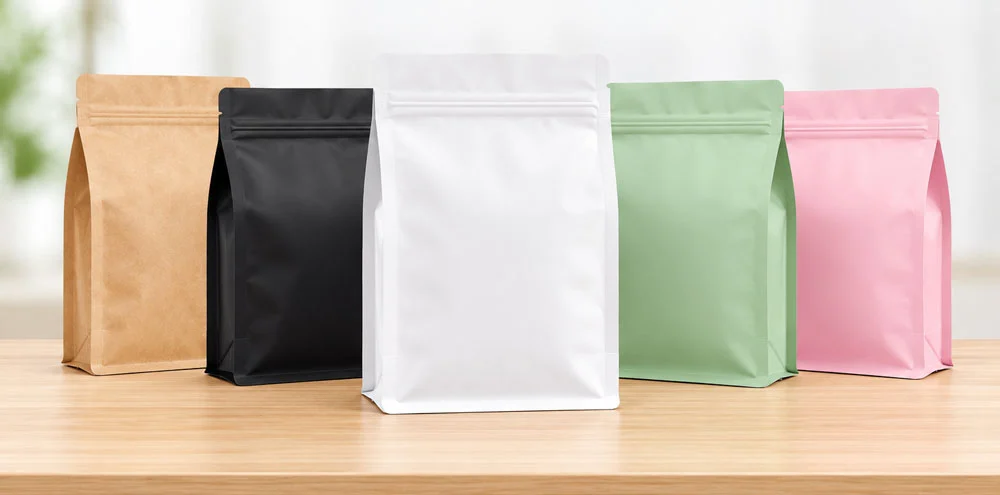
Custom flat bottom pouches with zippers are just what you need for today's competitive markets when you need packaging that will stay put on store shelves and keep contents fresh through multiple uses. Our 250g custom flat bottom pouch is stable like a box and easy to reseal, making it a smart way to protect products from the time they are made until they are eaten. Multiple layers of barriers protect these bags from wetness, air, and light. They are also easy to open and close with notches and zippers that stay closed, even after being opened many times.
Understanding 250g Custom Flat Bottom Pouches with Zipper
What Makes Flat Bottom Pouches Different
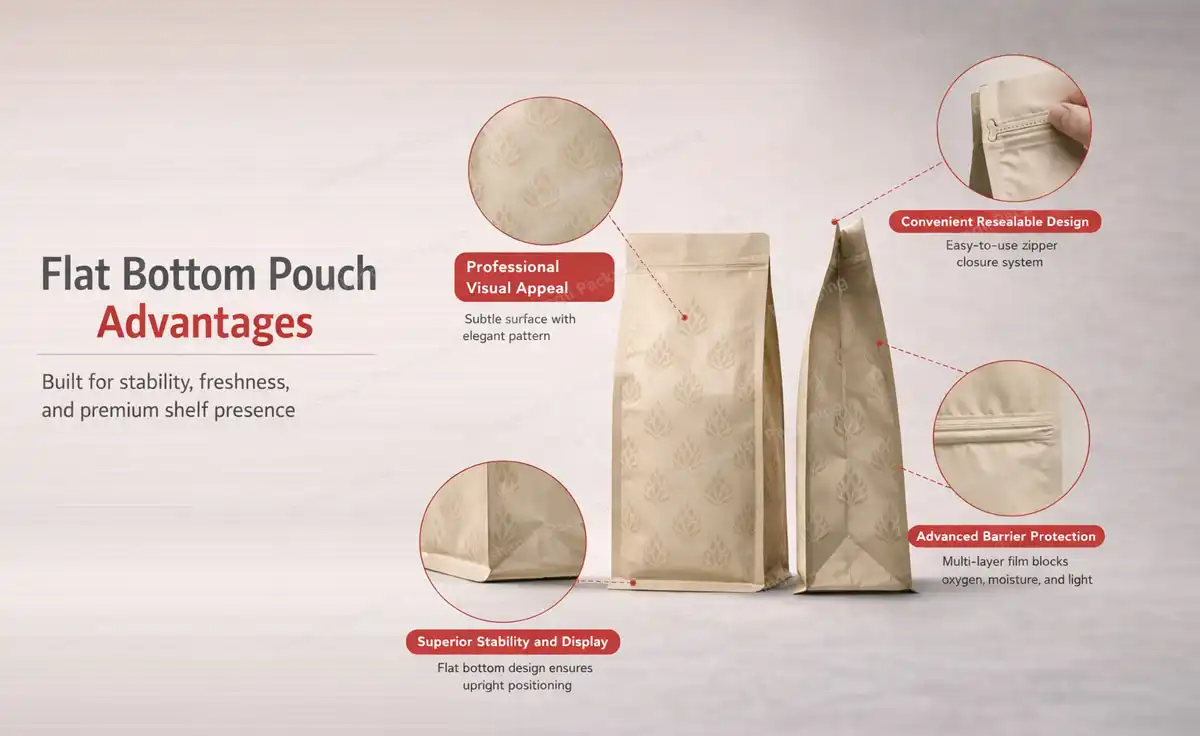
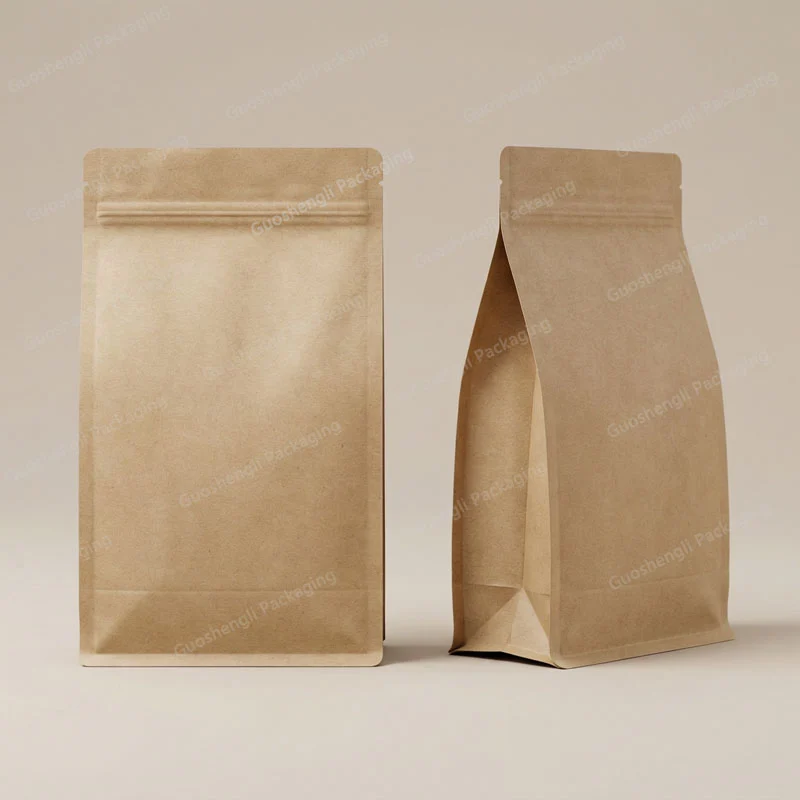
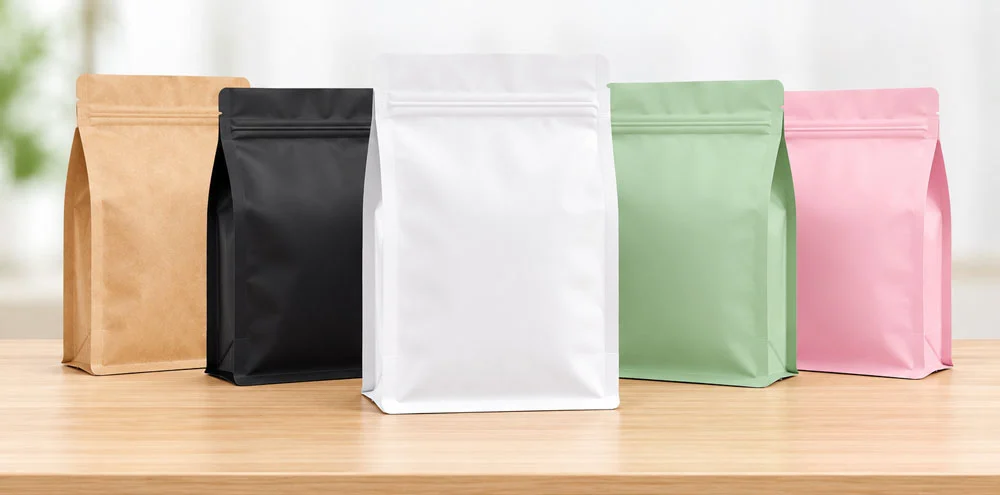
Box-style bags are a big step forward in the design of bendable packaging. Traditional stand-up pouches are stable because their gussets are folded, but flat bottom designs have five separate panels: the front, the back, two side gussets, and a fully flat base. This makes a structure that stands straight even before it is filled. This special design makes it stand out more on the shelf than regular pouches, which can lean or fall over when they're half full.
These bags' engineering strikes a mix between making good use of materials and keeping the structure strong. The flat base spreads the weight evenly across the bottom panel, and the side gussets expand to fit the size of the object. This design stops people from tipping and gives the store a professional look that makes customers feel more confident at the point of sale.
Material Composition and Barrier Technologies
Modern flat bottom pouches with zippers utilize sophisticated laminate structures tailored to specific product protection requirements. Common material combinations include:
- PET/PE Laminates provide excellent moisture resistance and puncture strength, making them suitable for dry snacks, coffee, and pet treats. The polyester outer layer accepts high-quality printing, while the polyethylene inner layer creates reliable heat seals.
- PET/Foil/PE Structures offer maximum barrier protection against oxygen, light, and moisture. This configuration extends shelf life significantly for sensitive products like ground coffee, protein powders, and specialty food ingredients that degrade when exposed to environmental factors.
- Kraft Paper Composites meet growing sustainability demands while maintaining functional performance. These structures typically combine kraft paper exterior layers with thin barrier films, creating packaging that feels natural yet protects contents effectively.
Our factory can make laminate structures that are unique to your product and meet the requirements for its shelf life using all of these combinations of materials. We improve the protective qualities without adding extra thickness to the material, which would raise costs and have a negative effect on the environment.
The Functional Advantage of Zipper Closures
With resealable zippers, single-use boxes can be turned into cases that can be used more than once and keep food fresh for weeks. It's especially important for products that are eaten slowly, like coffee, pet food, snacks, and supplements, to have reliable reclosure mechanisms.
Precise manufacturing control is needed for good zipper fitting in a 250g custom flat bottom pouch. The zip needs to be able to close all the way along its length while still being easy to open and close many times. Customers will complain about the product and the brand will be damaged if the zipper is placed wrong or the adhesive is not strong enough. As part of our production process, we check the quality of the zipper line, seal strength, and opening force to make sure that the product always works the same way.
Eco-Friendly Material Options
Sustainability affects purchase decisions in every market. Our environmentally friendly choices fulfil product safety standards:
- Normal recycling techniques may recycle mono-material assemblies with suitable polymer layers. Mixed-material laminates block more light than these designs, but they're appropriate for moderately protected objects.
- Addition of post-consumer recycling reduces new material use while meeting food contact safety standards.
- RTO exhaust gas treatment removes volatile organic compounds from printing and laminating in our factory. This makes production considerably greener than before.
How to Choose the Right 250g Flat Bottom Pouch with Zipper for Your Product
Evaluating Barrier Requirements
Safety relies on product sensitivity. Coffee requires oxygen barriers to preserve volatile taste compounds. Pet food must be moisture-resistant to maintain texture and prevent microbial growth. Protein powders should be kept away from air and water to maintain their nutritional value and prevent sticking.
Knowing your product's shortcomings helps us create laminate constructions. In our barrier tests, we measure oxygen, water vapour, and light passage using standard methods. These steps ensure that your packaging keeps your products safe for the expected storage term.
Accuracy in measurements matters too. For automated packaging equipment to operate, pouches must retain the same size to avoid becoming caught, misaligned, or not sealing. Our converting equipment ensures high-speed packaging lines work smoothly by keeping crucial dimensions.
Zippered Versus Non-Zippered: Cost-Benefit Analysis
When compared to standard heat-seal closures, adding zipper functionality raises the cost of packaging by about 15 to 25 percent per unit. This investment makes sense when resealability clearly adds value for end users—products that are used more than once benefit a lot from being able to reclose them.
Products that are offered in single-serving amounts or are eaten right away may not need the extra cost of a zip. We help procurement teams make this choice by looking at how the product is used, how it compares to other products on the market, and what the target customer wants.
For example, zippers work well on retail packaging for consumers, but easier closures work better on food service or institutional sizes where the contents are moved to other containers after being opened.
Customization Techniques That Enhance Brand Impact
How the surface is finished has a big impact on how appealing the shelf is and how people feel about the brand. Matte finishes give things a high-end, classy look that health and speciality food brands like. Gloss finishes are great for snack foods and pet products because they make colours stand out and shine brightly.
We can do both rotogravure printing and digital printing for a 250g custom flat bottom pouch. Rotogravure printing has wait times of about 15 to 20 days and always makes high-quality prints, even when doing a lot of them. Digital printing lets you print fewer products and get them to you faster (usually 7–10 days), which makes it perfect for testing the market, launching a new product, or making seasonal products.
Transparent windows let people see the products inside, which boosts their trust by letting them see the product before buying it. Placing windows correctly requires careful planning to keep the structure's strength and blocking qualities while also showing off the product's look well.
Applications and Use Cases of 250g Flat Bottom Pouches with Zipper
Coffee and Tea Packaging Solutions
When it comes to packing, speciality coffee roasters have their own problems. Freshly roasted beans keep giving off carbon dioxide for days after they've been roasted, so they need one-way degassing valves that let the gas leave but not the oxygen. Our flat-bottom coffee pouches have these valves built in without any problems, and the zippers still work for your convenience.
The stable base design makes coffee branding look great, and the four vertical panels give you plenty of room for information about the coffee's origin, grinding, and drinking suggestions. A lot of roasters have clear windows on the front that let customers see the quality of the beans and the level of roasting before they buy them.
Moisture barriers and reusable seals that keep delicate flavour profiles safe are also good for tea packing. Loose-leaf tea needs extra care because humidity can make it clump together and lose its flavour over time.
Snack Food and Dried Fruit Applications
Chips, nuts, dried fruits, and other similar foods need to be packaged in a certain way to keep their texture. The main quality issue for these groups is that they lose their brightness when moisture gets in. Our multi-layer laminates keep the right amount of moisture in them while they are being shipped and used by customers.
When compared to bag-style packaging, which needs to be hung or laid flat, the flat bottom pouch format makes for efficient shelf displays that make the most of facings per linear foot. Retailers like packaging that makes the best use of expensive store space and presents products in a way that looks good.
Portion control is becoming more important as people look for easy, pre-measured amounts. The 250g size is good for normal family use because it's big enough to provide value but small enough to keep fresh during normal use cycles.
Pet Food and Treat Storage
When pet owners buy treats and extra food for their animals, they look for things that are fresh and easy to use. Resealable pouches are a good solution for both problems because they keep the quality of the product and make it easier to store and use.
Keeping smells in check is another important thing to think about. Good barrier films stop smells from moving and affecting other kept foods or making your home smell bad. This also keeps the food's taste, since many pet foods and treats lose their appeal when volatile flavour compounds break down.
Our food-grade materials and production approvals make sure that products meant for animals are safe to use. We keep our BRC approval for packaging pet food, which means we meet the quality standards set by retailers and brands.
Health Supplements and Protein Powders
For powder to flow and not clump, the moisture level needs to be carefully managed. Hygroscopic ingredients are often found in protein powders, vitamin supplements, and other speciality nutrition products. These ingredients easily absorb water, which can make the texture of the product and the amount of water that it takes in inconsistent.
High-barrier pouches keep the low-moisture environment that powder needs to stay stable. When compared to non-resealable packaging that lets moisture in with each use, zip seals keep products from getting damaged when they are opened more than once.
On flat-bottom designs with clear labelling space, you can put full supplement facts panels, usage directions, and the regulatory statements that are needed for health goods. This information is presented in a clear and professional way by the organised style.
Practical Packaging Ideas for Brand Recognition
Visual distinction helps you stand out in crowded markets. We assist businesses in finding new packaging perspectives by:
- Custom colour matching ensures the brand appears the same across goods and packages. Our rotogravure printing makes accurate colour copies with 11 ink stations.
- Touchable textures make people want to connect with the product. Soft-touch coatings provide luxury, while etched components highlight brand names or characteristics.
- Different flat bottom shapes give brands personalities. Bags with die-cut hang holes, zipper pulls, or handles are more functional.
Procurement and Ordering Guide for 250g Custom Flat Bottom Pouches with Zipper
Step-by-Step Ordering Process
Creating clear specifications is the first step to a successful custom packing job. During the initial meetings, we help clients choose the right material, finalise the dimensions, and integrate features—whether for a 250g custom flat bottom pouch or other formats. This way of working together avoids misunderstandings and makes sure that the finished pouches meet the requirements for their purpose.
Sample production lets you test things physically before committing to large quantities of production. We offer pre-production samples that show the real materials, printing quality, and how well the structure works. This step looks for possible problems while fixes are still easy and cheap.
Production wait times change based on the type of printing the order is and how big it is. Digital printing jobs are usually done 7–10 days after the artwork is approved. For rotogravure printing, the barrel has to be made and set up, which adds 15 to 20 days to the process. We suggest that you plan your inventory needs ahead of time, especially for seasonal products or campaigns that use them.
Understanding Minimum Order Quantities and Pricing
MOQ requirements streamline manufacturing and give customers many options. Digital printing enables you to produce 5,000–10,000 pieces at once, which is useful for innovative goods or niche markets. Rotogravure printing requires 20,000 or more units to justify the cylinder investment, but it has lower ongoing production costs.
Bulk orders are quite cost-effective. Big savings can result from buying more materials, fewer setups, and better production schedule planning. Our pricing clearly demonstrates how prices vary by number. This helps buying managers decide when and how much to order.
Factors impact unit pricing beyond number. Material type greatly affects cost; high-barrier foil laminates cost more than plastic films. Adding buttons, vents, or windows gradually raises the price. The pricing depends on the quantity of colours, print area size, and special finishing.
Selecting Reputable Suppliers and Building Partnerships
Technical support and quality control are available directly from the factory, eliminating middlemen markups. Communicating with makers enables you to discuss modifications, plan production, and handle issues swiftly.
Supplier trust grows with quality assurance transparency. We list all materials, test results for barrier properties and seal strength, and inspection reports showing quality control checks during production. This documentation supports your quality plans and tracks products across supplier chains.
Long-term collaborations benefit both parties beyond transaction expenses. After building contacts, you may obtain assistance arranging your supply, create new goods, and book first during peak demand. It costs money to learn about our customers' operations, estimate what they'll require, and recommend improvements before they materialise.
Clear communication is crucial for international sourcing. Our team uses straightforward business language when discussing technical topics to avoid misconceptions that might lead to production errors or mismatched specs. For all orders, modifications, and agreements, we provide full written confirmation.
Innovations and Future Trends in Flat Bottom Pouch Packaging
Emerging Sustainable Material Solutions
Consumer preferences and regulatory pressures drive packaging sustainability innovation. Extended producer responsibility regulations in Europe and similar initiatives in North America require brands to plan packaging end-of-life.
Development of mono-material structures is promising. These designs, such as a 250g custom flat bottom pouch, allow recycling using existing infrastructure by employing suitable polymers in laminate layers. Performance gains continue to close the mono-material-multi-material barrier property gap.
Biodegradable and compostable films are another option; however, performance and infrastructural issues restrict commercial feasibility. Certain dry products benefit from PLA-based structures, but moisture-sensitive or oxygen-sensitive contents lose protection. Industrial composting capacity is limited in many regions, reducing environmental benefits.
We study and test new materials and introduce proven technology as they achieve performance and commercial viability standards. Our development strategy prioritises real-world solutions above ecologically good but unworkable ones.
Advanced Sealing and Closure Technologies
Tamper-evidence features address safety and quality assurance concerns across food, supplement, and pet food categories. Integrated tear bands provide visible evidence of package integrity, building consumer confidence while protecting brand reputation. These features add minimal cost while delivering substantial risk mitigation value.
Smart packaging technologies incorporating QR codes, NFC tags, or printed electronics enable consumer engagement and supply chain tracking. Brands use these features for authentication, usage instructions, recipe ideas, and loyalty program integration. Implementation costs continue declining, making smart packaging accessible for mid-volume production.
Improved zipper designs enhance usability and durability. Recent innovations include easy-glide profiles requiring less force to open and close, extended zipper life supporting hundreds of open-close cycles, and child-resistant options for products requiring access restrictions.
Enhanced Printing and Customization Capabilities
Digital printing technology advancement enables shorter runs and faster iterations compared to traditional rotogravure methods. This flexibility supports market testing, limited editions, and personalized packaging campaigns that strengthen consumer connections with brands.
High-definition printing delivers photographic image quality and intricate detail reproduction. Extended color gamut printing expands achievable color ranges beyond standard CMYK limitations, enabling more accurate brand color matching and vibrant shelf appeal.
Variable data printing allows individualized package content within production runs. Serialization for traceability, regional language variations, or personalized messaging all become feasible without inventory complications from maintaining multiple SKUs.
Evolving B2B Supply Chain Dynamics
Recent global disruptions elevated supply chain resilience. In procurement networks, brands prioritise supplier diversification, inventory buffer maintenance, and transparency. These changes impact supplier selection and relationship management.
Brands want distinction, raising customisation demands. Standard catalogue goods work effectively for limited applications; most successful packaging projects today customise specifications to product needs and brand positioning.
Leading time compression is difficult. Manufacturing realities clash with buyers' demands for extensive customisation and fast turnaround. Capacity investment, process optimisation, and clear communication about achievable timelines under different specification scenarios address this.
As companies increase manufacturing and distribution, repeat order quality matters more. Packaging that works effectively in first shipments but not in later orders disrupts operations and destroys customer relationships. Our production processes prioritise specification integrity and performance stability throughout the order lifecycle.
Conclusion
Custom flat bottom bags with zip closures fulfil market demands. The 250g custom flat bottom pouch works well for speciality coffee, premium snacks, pet treats, and health supplements. Material innovation, production accuracy, and customisation flexibility provide package solutions that safeguard product integrity, improve brand appearance, and maximise customer convenience. Understanding barrier requirements, weighing feature benefits against costs, and working with reliable suppliers are key to successful procurement. Long-term packaging success depends on choosing experienced manufacturing partners with technical depth and production capability as sustainability standards rise and customisation requests rise.
FAQ
1. What products work best in 250g flat bottom pouches?
Products consumed over multiple occasions benefit most from this format and capacity. Coffee, tea, snacks, dried fruits, pet treats, protein powders, and supplements all perform well. The size provides enough volume for household value while maintaining freshness through normal consumption patterns. The flat bottom design creates excellent shelf presence for retail environments where visual impact drives purchasing decisions.
2. How long does custom pouch production take?
Production timelines depend primarily on printing method selection. Digital printing projects complete within 7-10 days after artwork approval, making them suitable for quick launches or seasonal products. Rotogravure printing requires 15-20 days due to cylinder preparation and setup requirements but delivers superior quality for large production runs. We recommend planning inventory timing accordingly and ordering samples before committing to full production quantities.
3. Can flat bottom pouches with zippers run on automated filling equipment?
Properly manufactured pouches integrate smoothly with most vertical form-fill-seal and pre-made pouch filling systems. Dimensional consistency and material stiffness specifications must match equipment requirements to prevent jamming or misalignment. We provide technical specifications and can coordinate with equipment manufacturers to confirm compatibility before production. Our quality control processes maintain tight dimensional tolerances essential for automated handling reliability across production shifts.
Partner With Guoshengli Packaging for Your Custom Pouch Needs
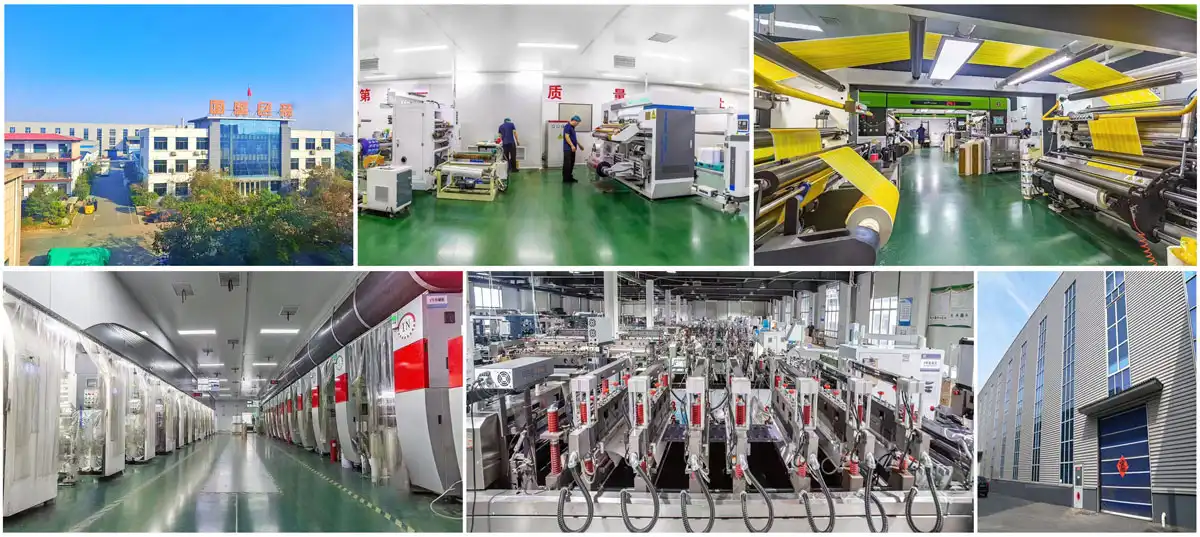
Quality packaging shouldn't create production headaches or compromise product protection. Guoshengli Packaging brings 25 years of flexible packaging manufacturing experience to every custom flat bottom pouch with zipper project we undertake. Our facility operates advanced rotogravure printing, precision laminating, and converting equipment that delivers consistent results across repeat orders—not just initial shipments. We maintain ISO 9001, BRC, FDA, and SGS certifications that meet international quality standards and support your compliance requirements. Whether you need 250g custom flat bottom pouch solutions for coffee, pet food, supplements, or specialty products, our engineering team designs packaging matched to your specific barrier requirements, filling equipment, and brand positioning. Contact our team at sales@guoshengpacking.com to discuss your project specifications with experienced flat bottom pouch manufacturers who understand B2B procurement priorities and deliver reliable packaging that performs consistently in real production environments.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice. 3rd ed. CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, vol. 72, no. 3, 2007, pp. 39-55.
3. Selke, Susan E.M., et al. Plastics Packaging: Properties, Processing, Applications, and Regulations. 3rd ed. Hanser Publications, 2015.
4. Coles, Richard and Derek McDowell, editors. Encyclopedia of Packaging Technology. 3rd ed. Wiley, 2011.
5. Yam, Kit L., editor. The Wiley Encyclopedia of Packaging Technology. 3rd ed. John Wiley & Sons, 2009.
6. Emblem, Anne and Henry Emblem. Packaging Technology: Fundamentals, Materials and Processes. Woodhead Publishing, 2012.
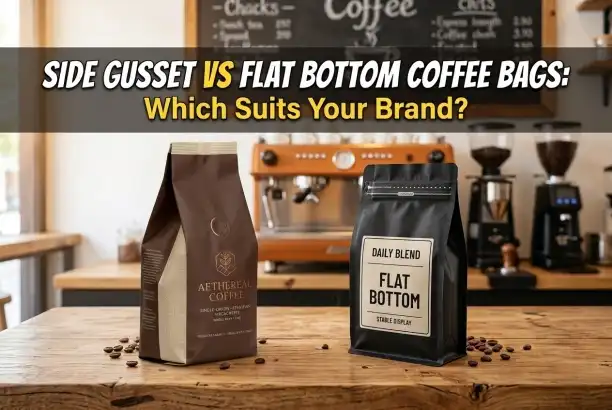
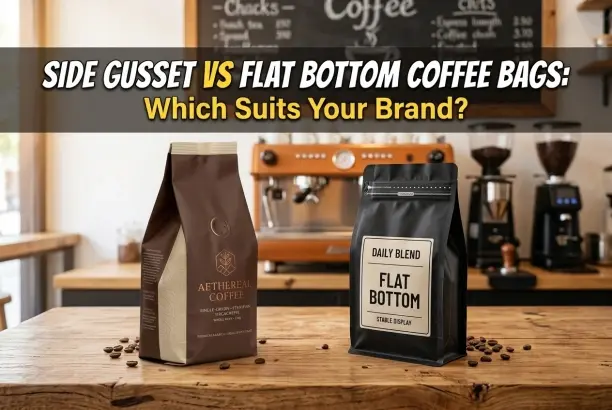
You can choose between a 1kilo side gusset pouch with valve and a flat-bottom coffee bag based on your brand's needs. If keeping the coffee fresh for longer and saving room are the most important things to you, side gusset pouches with degassing valves are the best option because they let CO2 out while blocking oxygen in. However, flat bottom bags stand out more on the shelf because they are shaped like boxes and have a larger surface area for marking. Both types of barriers are strong, but side gusset designs usually cost less to ship and work better with automatic filling lines. Your choice should be based on the features of the product, how it will be distributed, and whether your market positioning is based on freshness or visual impact.
Introduction
The way businesses buy and sell things has changed a lot when it comes to coffee packaging. Brands now want solutions that protect the purity of their products, make them look better on shelves, and make operations easier. Finding the right structure for one-kilogram coffee pouches means finding a balance between keeping the coffee fresh, making sure the bags work with other machines, and making the brand stand out. Side gusset pouches with valves and flat bottom coffee bags have become the most popular options. Each has its own technical and business benefits.
Side flap designs with built-in degassing holes solve the unique problem of freshly roasted beans giving off CO₂, which stops the pouch from expanding and going bad. Flat bottom structures, on the other hand, have a stable, rectangular footprint that makes them stand out visually. Procurement professionals can make smart choices that are in line with supply chain goals and market standards when they know how these forms differ in terms of barrier performance, filling efficiency, and branding potential.
This analysis makes things clear for packaging engineers, distributors, and brand managers who are investing in coffee packaging. To help you make your choice, we look at changes in structure, performance measures, buying factors, and actual usage issues.
Understanding Side Gusset Pouches with Valve and Flat Bottom Coffee Bags
Structural Design and Core Functionality
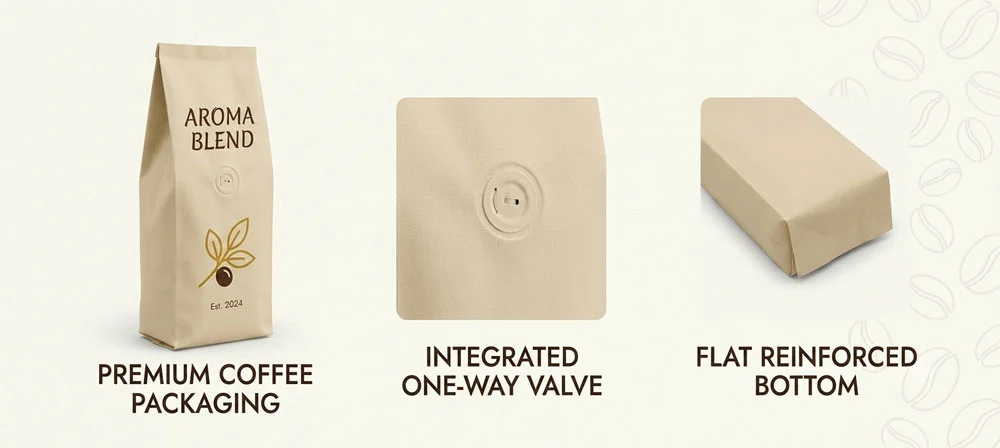
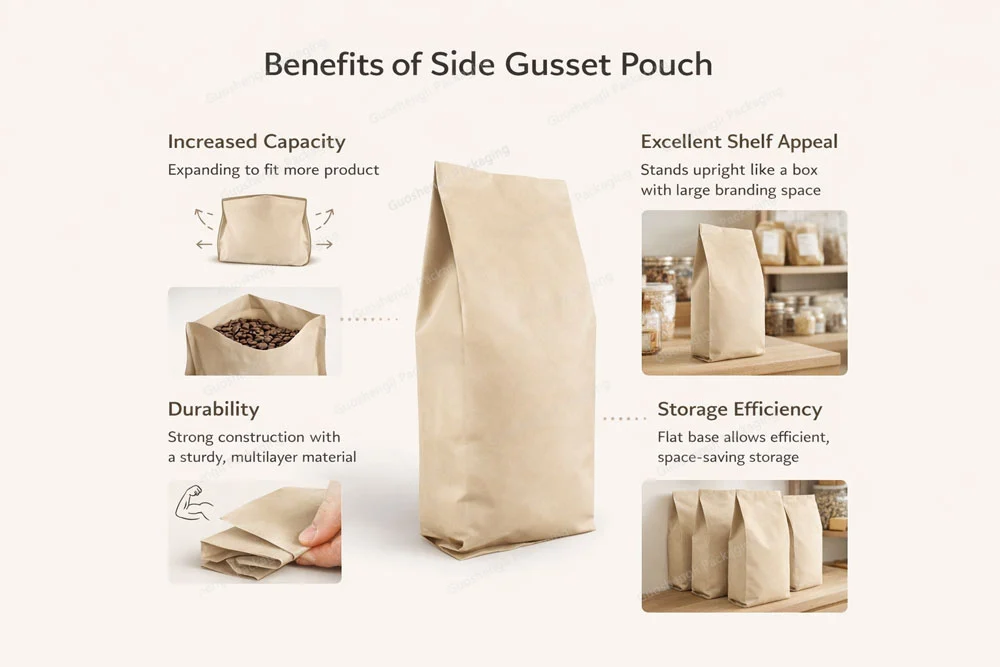
Side gusset pouches with valve have vertical expansion pleats on both sides, which lets the package hold more while still being small and saving space. The built-in one-way degassing valve is designed to let out the CO₂ that freshly roasted coffee beans give off while blocking oxygen from the outside.
Multi-layer laminate structures like PET/AL/PE or MOPP/VMPET/PE are often used in a 1 kg side gusset pouch with valve. These structures provide excellent protection against moisture, oxygen, and light. The thickness is between 120 and 160 microns so that it can hold a one-kilogram load without warping while it's being moved or stored. The side gussets spread the weight evenly across the base, which stops stress from building up that could damage the seal.
Flat bottom coffee bags, on the other hand, make the most of shelf space by having a strong rectangular base that lets the pouch stand up straight without any help. This design makes the front display area bigger, which is great for big branding and high visibility in stores. Flat bottom formats can also have valves, but their main benefit is the quality look and box-like stability that shoppers like when they're browsing store shelves, compared with a 1kilo side gusset pouch with valve.
Material Selection and Barrier Properties
High-barrier laminates can be used in both formats, but the choice of material is usually based on the needs of the application. Most side gusset bags with valves focus on keeping out as much air and wetness as possible to keep food fresh longer in storage and delivery settings. Some flat-bottom bags may have clear window films or special finishes added to them to make them look better, even if it means sacrificing some of their barrier performance.
The valve itself is an important point of quality control. Using vacuum methods to test the functionality of valves makes sure that air can only flow in one direction and not backwards. Tests that measure burst pressure show that side gusset seals can handle the stress of a full kilogram load. Oxygen Transmission Rate and Water Vapour Transmission Rate tests show that the barrier is strong enough to meet FDA and EU food contact compliance standards.
Performance and Functional Comparison
Freshness Preservation and Shelf Life Extension
Side gusset pouches with valves keep coffees that are sensitive to smells fresh longer. The degassing valve solves the biggest problem in the business, which is keeping the inside of the pouch oxygen-free while stopping the pouch from bloating. Over the next 7 to 14 days after being roasted, freshly roasted beans give off large amounts of CO2. Without a valve, internal pressure can build up and break the seal or make packaging take longer than planned. This problem is solved by the one-way valve, which lets you pack right away while keeping the best flavour and taste.
When used in side gusset designs, multi-layer barrier films offer strong protection against air, moisture, and light. This security can be seen through increased shelf life tests. When kept in controlled settings, properly made bags can keep coffee fresh for an extra 12 to 18 months. The small size cuts down on headspace, which lowers the amount of air left over that speeds up the staling process.
It is also possible to integrate valves into flat bottom bags, which can provide similar barrier performance. Their advantage comes from being able to handle bigger batches and making it easier to see the products inside through clear panels. Brands that want to be seen as high-end often choose flat bottom forms because they look more expensive, even if it means paying a little more for materials and needing more space to store them.
Space Efficiency and Logistics Optimization
A 1-kilogram side gusset bag with a zipper makes sending and storing things more efficient. When it's full, the side gusset design expands to its full size, but it stays narrower than flat-bottom versions of the same thing. This means fewer pallets, lower freight costs, and better use of warehouse space, all of which are important for B2B buyers who handle large orders.
Even though flat-bottom bags look nice, they take up more room per unit. Because their bases are rigid, they can't be nested or stacked as well as side gusset formats. Because of these logistical benefits, distribution centers that ship a lot of coffee often choose side gusset pouches with valves. This is especially true when shipping internationally.
Printing Capabilities and Brand Differentiation
Both types can handle high-quality rotogravure printing, which can produce images with up to 11 colours that catch people's eyes. Side gusset bags, including 1kilo side gusset pouch with valve, have four printable areas: the front, the back, and the two side panels. This gives you a lot of room to put your logo on them. The vertical layout works well with big graphics and a clear hierarchy of product information.
The stable, box-like shape of flat bottom bags makes them great for making a statement on the shelf. The front panel can be used as a natural sign, and the flat base can have more branding elements added to it. Premium coffee brands that want to sell in stores often choose this format to stand out from competitors who use standard pillow pouches.
Procurement Considerations for B2B Buyers
Cost Analysis and Pricing Structures
Because they use less material and are easier to make, side gusset sacks with valve usually cost 15 to 25 percent less per unit than similar flat bottom bags. For custom-printed rotogravure production, the minimum order quantity varies by supplier but is usually between 10,000 and 30,000 units. With digital printing, MOQs can be as low as 5,000 to 10,000 units, which makes them more suitable for smaller names or test market launches.
Lead times are different for each format and printing method. Rotogravure printing takes 15 to 20 days from the time the artwork is approved until the side gusset pouches with valve are delivered. For rush orders or seasonal products, digital printing cuts this time down to 7–10 days. Due to more complicated changes, flat bottom bags may add 2–5 days to wait times.
Due to their small size, side gusset designs are cheaper to ship. It usually takes four to five days to ship by air, and twenty to thirty-five days to ship by sea, depending on where it's going. When you add up all the costs, like packing, printing, and shipping, side gusset bags with valves are often the best deal for high-volume businesses.
Supplier Evaluation and Quality Assurance
Reliable makers show uniform quality across multiple orders, which is an important factor that is often missed when choosing the first provider. Baseline guarantee comes from ISO 9001 quality management approval, BRC food packing accreditation, and FDA compliance paperwork. Third-party testing results from SGS back up claims about the performance of barriers and the safety of the materials.
When processes are scaled up, production ability is important. Multiple rotogravure printing lines, advanced binding equipment, and precise pouch-making tools in a facility lower the risk of bottlenecks during times of high demand. Suppliers who offer in-house testing and inspection at every important stage reduce the number of defects that stop the filling line from working.
Professional packing partners are different from product providers because they can communicate clearly and offer expert help. You can expect thorough information about the materials, drawings of the sizes, and data on how well the valves work. Beyond just supplying products, manufacturers who offer design advice, artwork optimisation services, and filling trial help add a lot of value.
Sustainability and Eco-Friendly Options
Environmental duty is becoming more and more important when it comes to buying things, especially for brands that want to sell in Europe and North America. Using single-material PE or PP laminates in recyclable packaging supports the idea of a circular economy while still having good barrier properties for coffee uses. Compostable PLA/PBAT-based solutions are useful for people who care about the environment, but they need to be carefully tested for shelf life performance.
Concerns about sustainability come up with degassing valves themselves. Traditional valve materials have a lot of plastic parts that make recycling harder. New solutions for biodegradable valves are addressing this issue, but they are still not widely available in the market. When suppliers spend money on eco-friendly valve solutions, they show that they are ahead of regulation trends and buyer tastes.
The ways things are made are also important. RTO exhaust gas treatment systems keep printing and laminating operations as environmentally friendly as possible. Certifications that show sustainable practices improve the story of a brand and meet retailer needs in markets that care about the environment.
Matching Packaging Solutions to Your Brand Needs
Segment-Specific Recommendations
Side gusset pouches with valves are best for coffee roasters who want to keep their coffee fresh and save money. The improved degassing technology, better barrier protection, and better transportation optimisation work well with wholesale distribution models where keeping the integrity of the product during long storage periods is very important. This format is perfect for medium- to large-volume operations that handle 1-kilogram bulk packages because it keeps the smell and taste of the food fresh throughout the supply chain.
Speciality coffee brands that want to stand out on store shelves and be seen as high-end should think about using flat-bottom bags. The high-end design gets people's attention in busy stores, which makes up for the slightly higher packing costs by improving how people see the brand. This format is good for artisan roasters who want to sell to gourmet markets where visual differences are important for making decisions about what to buy.
Side gusset pouches with valves are also used by companies that make pet food and health supplements to package powdered products. The 1kilo side gusset pouch with valve shape is flexible enough to fit a wide range of dry goods that need to be kept dry and under controlled pressure while they are stored. The side panels that can be expanded make it easier to pour, which is good for customers in both store and food service settings.
Automated Packaging Line Compatibility
Compatibility with the filling line is an important but often overlooked factor in choosing packaging. Side gusset pouches with valves usually work well on vertical form-fill-seal machines and pre-made pouch fillers because they have consistent sizes and behave in predictable ways, which cuts down on downtime. Precision in valve placement affects the trustworthiness of the seal, which is why quality control standards set by the maker are so important.
To make the hard base that is typical of flat-bottom bags, you need special making tools. Not all filling lines can be used with this style without being changed. Checking for compatibility before placing big orders avoids the need for expensive updates or retrofitting. By asking for filling trials with sample bags, problems can be found before full production starts.
Practical Usage and Storage Tips for Side Gusset Pouches with Valve
Understanding Valve Mechanics
The one-way degassing valve works with a thin silicone membrane that opens when pressure inside the valve rises, letting CO2 escape while keeping air from the outside out. The best valve performance depends on how well it is calibrated to the coffee. For example, valves that need slightly lower opening limits are needed for darker roasts because they give off more gas. Valve placement is usually in the upper third of the back panel of the pouch to make it easier for gas to escape when the package is kept upright.
Filling and Sealing Best Practices
Using the right filling methods will increase the shelf life and lower the number of defects. To avoid problems with under- or over-filling, filling machines should always give accurate weights within ±2 grams. Keeping the right amount of headspace—usually between 15 and 20 mm—allows for changes in internal pressure without putting too much stress on seals. Temperatures between 160°C and 180°C, stay times between 1.5 and 2 seconds, and sealing pressures between 0.4 and 0.6 MPa are all important factors for heat sealing that need to be carefully calibrated.
The conditions of storage have a big effect on how well packing works. To keep things from breaking down because of moisture, warehouses should keep the temperature between 15°C and 25°C and the relative humidity below 60%. Palletised bags are better protected by wrapping that keeps them from getting damaged by light or handling. Following the first-in, first-out rule of regular rotation makes sure that customers get older stock within the best freshness windows.
Common Issues and Troubleshooting
Fine coffee droplets can sometimes block the membrane and cause the valve to get stuck. This risk is kept to a minimum by keeping production areas clean and adding inner screens to equipment used for filling. Limiting the height of the pallet and putting protective dividers between layers can stop the pouch from deforming under the weight of storage. Most seal failures are caused by incorrect heat-sealing settings or dirt along the seal areas. These problems can be fixed by properly teaching operators and maintaining equipment on a regular basis.
Conclusion
Which side gusset pouches with valve to use versus flat bottom coffee bags depends on how your brand wants to protect freshness, run its business efficiently, and place itself in the market. Side gusset forms are great for extending the shelf life of goods, cutting down on transportation costs, and working with automatic systems that handle large amounts of work. Flat-bottom bags stand out more on the shelf and are easier to see in stores. When designed correctly, both formats offer strong barrier properties, but the 1kilo side gusset pouch with valve consistently performs better for B2B buyers who value product integrity and cost-effectiveness across long supply chains.
FAQ
1. Can side gusset pouches with valves include resealable features?
Resealable zipper closures can be integrated into side gusset pouches with valves, combining degassing functionality with consumer convenience. This combination suits retail packaging where customers purchase one-kilogram quantities for home use. The zipper placement occurs below the valve, preserving freshness after initial opening. Manufacturing complexity increases slightly, affecting minimum order quantities and unit costs. Brands targeting premium retail segments find resealable formats enhance perceived value and repeat purchase rates.
2. What are typical minimum order quantities for custom-printed pouches?
Rotogravure printing requires 30,000-50,000 units to justify cylinder engraving costs, though some manufacturers accept 10,000-unit minimums with surcharges. Digital printing reduces MOQs to 5,000-10,000 units, ideal for new product launches or limited editions. Ordering larger quantities reduces per-unit costs through economies of scale. Balancing inventory investment against price optimization requires careful demand forecasting and supplier negotiation.
3. Are biodegradable valves commercially available?
Biodegradable valve technology has advanced significantly, with several manufacturers now offering compostable alternatives made from PLA and other plant-based materials. Performance validation remains critical, as valve reliability directly impacts product freshness. Not all biodegradable valves match conventional petroleum-based versions in pressure tolerance and longevity. Brands committed to sustainability should request testing data and conduct shelf life trials before full-scale adoption.
Partner with a Trusted 1Kilo Side Gusset Pouch with Valve Manufacturer
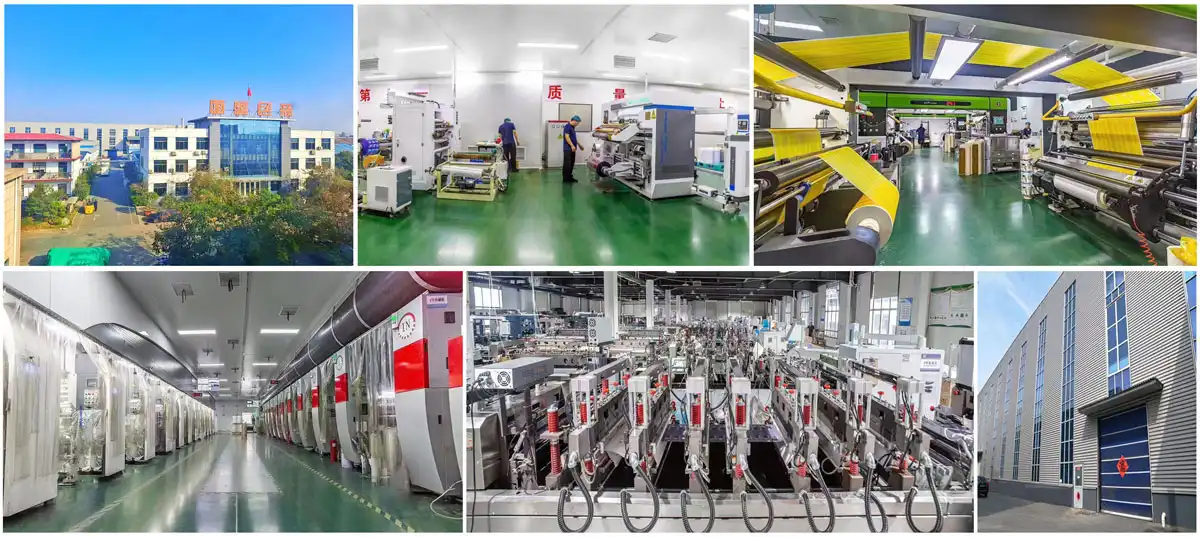
Guoshengli Packaging delivers reliable, export-ready packaging solutions engineered for consistent performance across repeat orders. Our 1kilo side gusset pouch with valve combines 25+ years of manufacturing expertise with advanced production capabilities, including 11-color rotogravure printing, ISO 9001 and BRC certifications, and 100% recyclable material options. We understand that packaging problems rarely appear in samples—they emerge during production scaling and market expansion. Our quality systems prevent costly failures through rigorous barrier testing, valve functionality validation, and dimensional consistency verification.
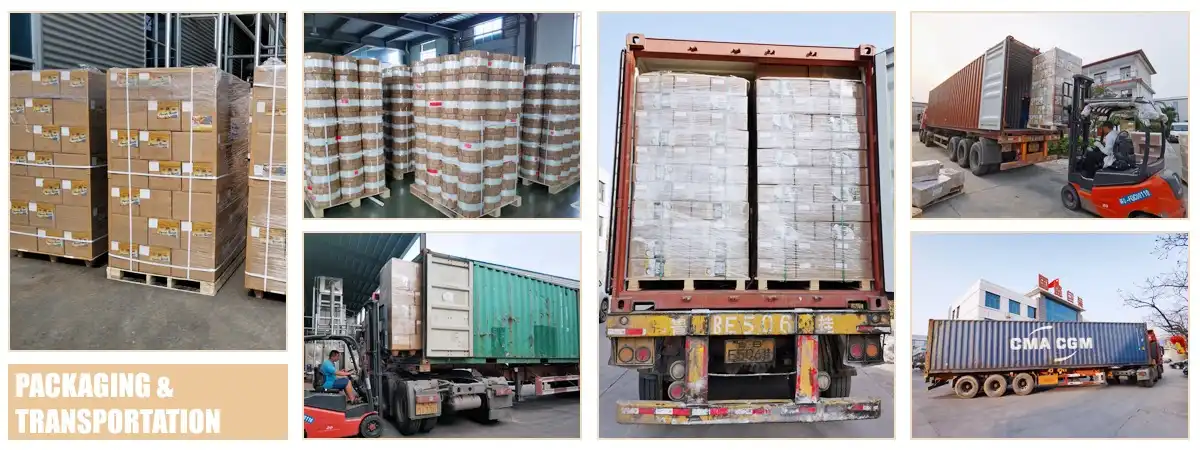
Whether you're a coffee roaster, pet food manufacturer, or health supplement brand, we provide customized solutions matching your filling equipment, regulatory requirements, and growth objectives. Contact our team at sales@guoshengpacking.com to request samples, discuss your specific needs, or receive detailed technical specifications. We offer flexible MOQs, rapid production timelines—7-10 days for digital printing—and fast global delivery. Connect with a 1kilo side gusset pouch with valve supplier committed to reducing your procurement uncertainty and supporting long-term success.
References
1. Smith, J. & Anderson, K. (2022). Flexible Packaging Engineering for Coffee Preservation: Barrier Properties and Valve Technology. Journal of Food Packaging Science, 15(3), 245-267.
2. Chen, L. (2021). Comparative Analysis of Coffee Packaging Formats in B2B Procurement. International Packaging Research Association, Technical Report Series No. 89.
3. Williams, R. (2023). Sustainability in Flexible Packaging: Materials, Manufacturing, and Market Trends. Packaging Technology Review, 28(1), 112-134.
4. Thompson, M. & Rodriguez, A. (2022). Optimizing VFFS Operations for Side Gusset Pouches with Degassing Valves. Automation in Packaging Conference Proceedings, pp. 567-582.
5. European Coffee Packaging Alliance (2023). Best Practices Guide for One-Kilogram Coffee Pouch Selection and Quality Control. Brussels: ECPA Publications.
6. National Coffee Association (2021). Packaging Impact on Coffee Freshness and Shelf Life Extension: A Technical White Paper. New York: NCA Research Division.
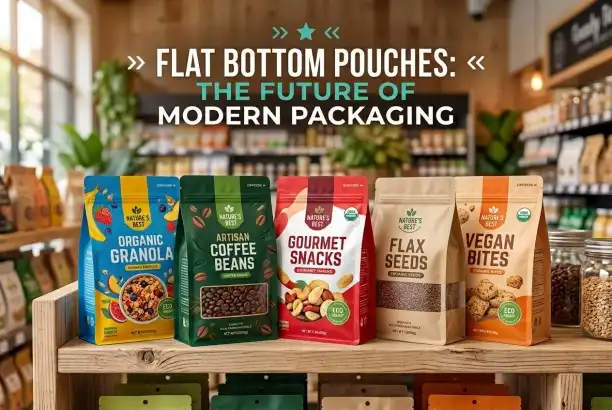
The packaging business is going through a big change, and flat bottom pouches are at the front of it. It's more than just a container—a 250g custom flat bottom pouch is a sophisticated way to package things that looks good, works well, and is structurally stable. The bags are made in a unique box shape, with five separate panels: a front, a back, two side gussets, and a flat bottom. This design makes it possible for goods to stand straight and be very balanced, giving them a strong appearance on the shelf that is hard for other types of packaging to match. Flat bottom bags have become the package of choice for forward-thinking companies in the food, pet care, and health industries. They protect goods and help them stand out in the market.
Understanding 250g Custom Flat Bottom Pouches
What Makes These Pouches Different
Flat bottom pouches, which are also sometimes called "box pouches," are very different from standard stand-up or three-side seal forms. The engineered flat base gives the unit a stable base that keeps it from tipping over, even if the products inside move around while being moved or handled. These packages stay upright before, during, and after filling, unlike traditional pouches that depend on the product inside to keep them stable.
The 250-gram volume is just the right size for many uses—it's big enough to give customers good value while still being easy to carry and store. This size works great for premium coffee blends, speciality pet treats, protein supplements and gourmet snacks that need to be portion controlled and kept fresh.
Material Construction and Barrier Performance
Flat-bottom packaging works best when it has structures made of multiple layers that are laminated together. Materials like polyethylene terephthalate (PET), aluminium foil, oriented polypropylene (OPP), and polyethylene (PE) are often used together in these structures to make better shields against air, light, and moisture.
The performance of the barrier has a direct effect on the shelf life. High-barrier designs are very helpful for products that are easily oxidised, like roasted coffee or omega-3 supplements. Our research team chooses material choices based on the product's moisture content, fat level, volatile flavour, and how long it needs to stay fresh.
More and more, brands want environmentally friendly options that don't hurt security. Companies that care about the environment can now choose from packaging structure made of recyclable materials and films that can be composted. Careful testing is needed to make sure that these options provide enough security throughout the supply chain.
Structural Features That Drive Performance
The flat bottom design has a number of technical benefits. Four straight panels make the most of the printable area, giving you lots of room for branding, legal information, and messages to customers. When compared to standard bag forms, this larger medium allows for more powerful graphic stories.
Side gussets grow to fit the size of the product while keeping the package small while it's being stored or shipped in a 250g custom flat bottom pouch. This saves space, which means less money spent on shipping and storage, two things that have a big effect on the total cost of ownership in large-scale operations.
Benefits and Applications of 250g Custom Flat Bottom Pouches
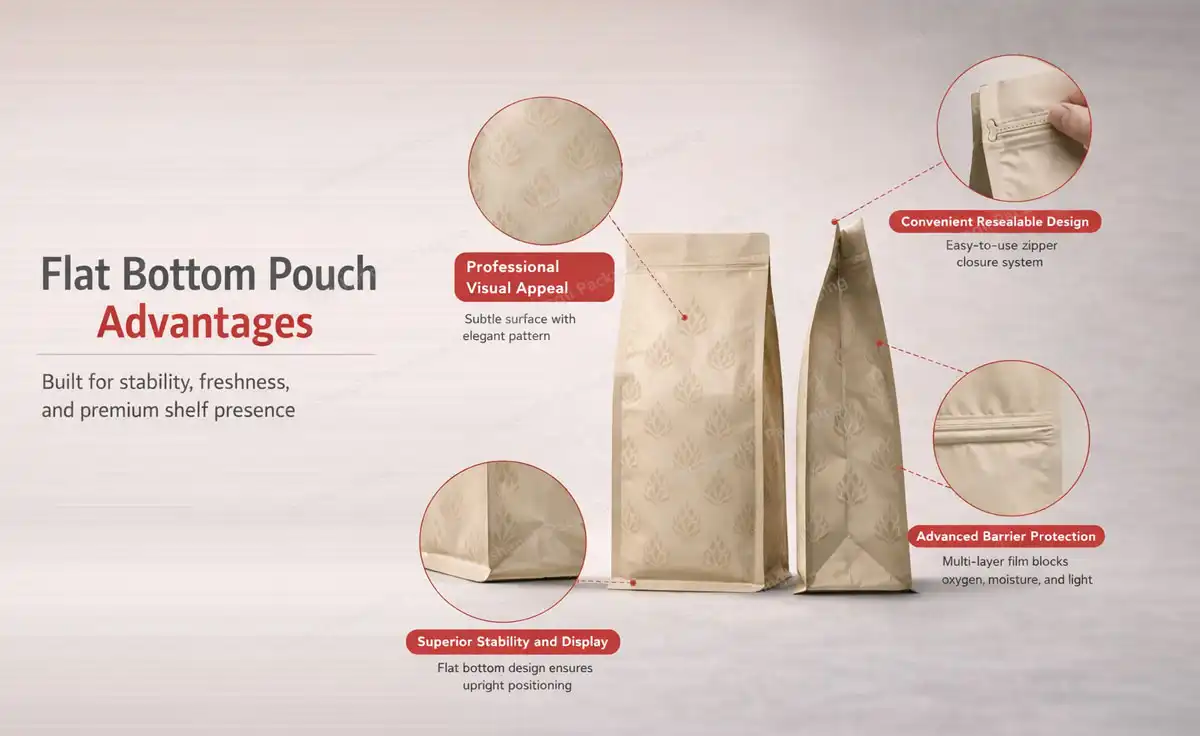
Superior Shelf Presence and Retail Performance
In retail settings, packaging needs to grab people's attention right away. The box-like shape of flat bottom pouches gives products a high-end look that makes them seem more valuable. This visual effect is especially important in crowded categories where buyers decide what to buy by how different the products are.
The stable base makes sure that products stay upright all the way from the factory to buyers' homes, from store displays to their homes. This reliability gets rid of the hassle of packages that lean or fall, which can hurt the brand's reputation and make it hard for stores to restock.
Functional Advantages for Product Protection
Barrier properties that are more advanced than those found in traditional packaging keep food fresh longer. We build multi-layer structures at our site that offer measured oxygen transmission rates (OTR) and water vapour transmission rates (WVTR) that are made to fit the needs of each product.
Resealable zipper seals keep food fresh even after being opened, so they can be used more often and less is wasted. This function is especially helpful for things like coffee, pet toys, dried veggies, and vitamin pills that are used more than once. The easy-tear notch makes it easy to get to things without using knives or other tools. This makes the user experience better and lowers complaints about packages.
Food-grade materials made to FDA, BRC, and ISO standards are used to make our 250g unique flat bottom bag choices. These approvals make sure that foreign rules are followed, which lowers the risk for brands that sell in more than one market.
Industry Applications and Use Cases
Coffee roasters like how flat-bottomed bags keep flavour compounds safe while also making the product look nice on the shelf, which shows that it is of high quality. The degassing valve choice lets carbon dioxide escape without letting oxygen in, which keeps speciality beans at their freshest.
Manufacturers of pet food like it when the structure stays strong so it doesn't tear when it's being handled. The strong design can handle stress from transportation while keeping the healthy content from breaking down. Premium positioning is easier when the quality of the packaging matches the quality of the product.
The professional look and protective barriers that stop moisture absorption and oxidative damage are good for health and wellness brands. If protein shakes, vitamin pills, and superfoods are packed in the right way, they stay effective for as long as they are stored.
Comparing 250g Custom Flat Bottom Pouches with Alternative Packaging
Flat Bottom vs. Stand-Up Pouches
Both types of pouches can stand up, but flat bottom pouches are more stable because they have an engineered base panel. Stand-up pouches have bottom gussets that fold inward, making the bag stand smaller. This difference stands out more on store shelves, where the way products are placed affects how well they can be seen.
When it comes to graphics and information, 250g custom flat bottom pouch designs with five panels have more space than three-panel stand-up formats. This extra room is helpful for brands that need to tell complicated stories or follow a lot of rules.
Material Efficiency and Sustainability Considerations
Instead of adding extra thickness, flat bottom pouches use structural engineering to get the most out of the material they have. This efficiency cuts down on the amount of raw materials needed while keeping the protective performance the same. The steady base evenly spreads the weight, which lets smaller gauge films be used in some situations.
Recyclability relies on the type of material used, not the shape of the bag. Structures made of a single material work just as well in flat bottom designs as they do in other styles. However, the high-end nature of flat-bottom packaging often makes it worth spending money on certified recyclable or compostable materials that support the environmental messaging of the brand.
Cost Analysis and Value Proposition
Because they are harder to make, flat-bottom bags usually have higher initial unit costs than basic three-side seal forms. But a total cost study shows that the investment is worth it because it improves brand placement, makes transportation more efficient, and lowers the number of damaged products.
Better shelf presence often leads to higher velocity at retail, which lowers the cost of keeping inventory and raises the return on shelf space. When it comes to high-end goods, the choice of style has a direct effect on how the product is positioned in the market and how much it costs.
How to Choose and Procure the Best 250g Custom Flat Bottom Pouch
Critical Selection Criteria
Packaging requirements are based on the features of the product. Goods that are sensitive to moisture need sheets with low WVTR, and goods that are sensitive to air need materials with low OTR. To keep the smell in, you need to use certain barrier ratios, which our technology team can suggest based on tests and experience.
Print quality changes how people think of a brand. Rotogravure printing is better than flexographic printing at reproducing colours and details, which is especially important for photos or colours that change slightly. Digital printing lets you do shorter runs or make changes to the design more often.
Features that are functional should match how they are used. Resealable closures are better for products that are used more than once, but the extra cost might not be worth it for single-use applications in a 250g custom flat bottom pouch. Windows let you see the goods, but they need extra material factors to keep the barrier intact.
Working with Manufacturing Partners
Minimum order quantities vary a lot from one manufacturer to the next, which can make it hard for new brands or test markets to get started. Our building can handle orders of different sizes because we plan our production well and set our minimum order quantities in a way that balances working efficiency with customer accessibility.
Lead times are based on the printing method and the schedule for production. Orders for digital printing are usually processed in 7–10 days, but orders for rotogravure printing take 15-20 days because the cylinders need to be prepared. Knowing these dates helps brands make good plans for managing their supplies and releasing new products.
Compliance risks can be avoided by verifying the certification. Manufacturers with a good reputation show proof that their products meet FDA food contact requirements, BRC packaging standards, and ISO quality management systems. These qualifications show that you know how to keep quality high and follow the rules that are needed for foreign shipping.
Quality Assurance and Testing Protocols
Reliable providers use inspection methods at all stages of production, including checking new materials, keeping an eye on work-in-progress, and testing finished products. Every time our facility makes something, the seal's strength is tested, the barrier's performance is confirmed, and the size is checked.
Quality records make things clear and easy to track. Detailed paperwork helps brands show stores and governmental officials that they have done their research and supports efforts to keep getting better. This information is very helpful when increasing production or figuring out problems in the field.
Maximizing the Performance and Efficiency of Flat Bottom Pouch Packaging
Design Optimization Strategies
The design of packaging should strike a balance between how it looks and what it needs to do. The four vertical panels of a 250g custom flat bottom pouch make it possible to tell stories in a logical order: the front panel shows the effect of the brand, the side panels show information about the product, and the back panel shows governmental information and company message.
Structures make things easier to use. Putting tear notches in places that are easy to reach, zip ends that line up with how products are dispensed, and clear views that show off the quality of the products all help to create good user experiences that keep people loyal to the brand.
The choice of material changes both ability and how something is seen. Matte finishes show that something is natural or high-end, while shiny finishes make colours stand out. In competitive categories, tactile features like soft-touch finishes or engraving make products stand out.
Advanced Printing Capabilities
Our building has seven printing machines that can do up to eleven-color rotogravure printing. This feature lets you add photographic reproduction, subtle gradients, and metallic effects that make the package look better than average. As production volumes rise, brand integrity is kept up by matching colours consistently across runs.
Versioned packaging, like regional variations, limited editions, or personalised designs, can benefit from digital printing. The technology gets rid of the need for cylinders and shortens the time it takes to set up. This makes shorter runs affordable for testing or niche markets.
Hot printing and other special finishes add high-end touches that make goods stand out on the shelf. When it comes to expensive products or gifts, where the wrapping adds a lot to the perceived worth, these methods work especially well.
Real-World Performance Benefits
When brands move to flat bottom bags, they often see real changes in how well they do in stores. The better visibility on the shelf gets people's attention in categories that are already full, and the more expensive look supports higher prices that make the margins better.
Damage rates go down, which makes distribution more efficient. Handling stress that damages regular flexible packaging doesn't affect this packaging's structural integrity, so fewer shipments are rejected, and customers are less unhappy. This dependability is becoming more important as more stress points are added to packages through e-commerce platforms.
Metrics for sustainability get better when optimised material structures lower the total weight of packaging without lowering its protection. Our engineering approach aims for the least amount of material use that still meets performance standards. This helps both environmental goals and cost management goals.
Conclusion
250g custom flat bottom pouches are a good example of how form and function can work together to solve modern packaging problems. The one-of-a-kind structure design gives it stability, shelf appeal, and protection that are hard to find in other formats. New materials keep making it possible to be more environmentally friendly without lowering the safety of the products, and better printing methods help businesses stand out in crowded markets. Flat bottom bags have benefits that have been shown to work across production runs, marketing routes, and customer uses. These benefits are backed by technical concepts and market proof. The format has gone from being a niche application to a common solution as makers, stores, and customers have come to understand the many benefits these packages offer.
FAQ
1. What products work best in 250g flat bottom pouches?
This capacity suits premium coffee beans, specialty pet treats, protein supplements, gourmet snacks, dried fruits, and wellness products. The format works particularly well for products consumed over multiple occasions where resealability maintains freshness. Material barriers can be customized for moisture-sensitive, oxygen-sensitive, or aroma-volatile products based on specific protection requirements.
2. How do flat bottom pouches improve sustainability?
Material efficiency comes from optimized structures that use thinner films while maintaining protection. Recyclable mono-material options eliminate multi-material separation challenges. The stable structure reduces damage during distribution, lowering waste from rejected shipments. Extended shelf life through superior barriers reduces product spoilage, addressing sustainability across the entire value chain beyond just packaging materials.
3. What minimum order quantities should I expect?
MOQs vary based on printing method and customization complexity. Digital printing typically allows smaller initial orders, while rotogravure printing achieves better economics at higher volumes. Established manufacturers like Guoshengli structure MOQs to balance production efficiency with customer accessibility, offering flexibility for brands at different growth stages while maintaining quality consistency.
Ready to Elevate Your Product Packaging?
Guoshengli Packaging brings 25 years of flexible packaging manufacturing expertise to your 250g custom flat bottom pouch projects. As an experienced supplier serving food, pet food, coffee, and wellness brands across North America, Europe, and Asia-Pacific, we understand the operational realities behind successful packaging programs. Our facility maintains ISO 9001, BRC, FDA, and SGS certifications, ensuring your packaging meets international standards from the first production run through long-term repeat orders. We offer flexible MOQs, fast turnaround times, and complete customization—from material selection through final printing. Contact our technical team at sales@guoshengpacking.com to discuss how properly engineered flat bottom pouches can solve your specific packaging challenges and support your market growth objectives.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice. Third Edition. CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Vol. 72, 2007.
3. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations. Third Edition. Hanser Publications, 2015.
4. Yam, Kit L. The Wiley Encyclopedia of Packaging Technology. Third Edition. Wiley-Blackwell, 2009.
5. Coles, Richard and Mark Kirwan. Food and Beverage Packaging Technology. Second Edition. Wiley-Blackwell, 2011.
6. Emblem, Anne and Henry Emblem. Packaging Technology: Fundamentals, Materials and Processes. Woodhead Publishing, 2012.
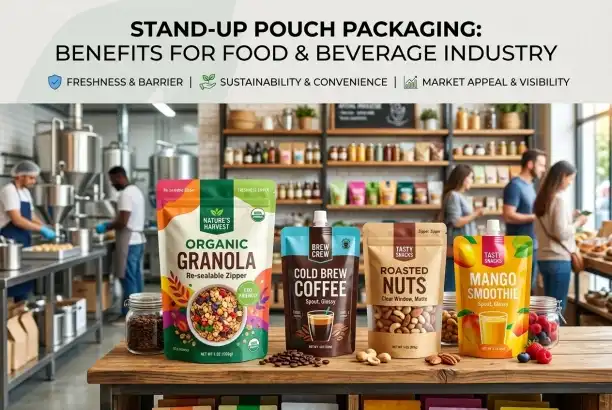
Stand up pouches have changed flexible packaging for food and drink businesses that want cheap, shelf-stable, and user-friendly options. These self-supporting packages are becoming more and more popular among procurement managers, product makers, and marketers because they offer both advanced barrier security and great branding options. In contrast to rigid containers, flexible pouches use less material while increasing product visibility and shelf impact. Their strengthened gusset base lets them stand upright on store shelves, which makes the name stand out right away. Knowing all the benefits of this type of packaging is important for brands that want to stay ahead in today's fast-paced market because consumers are increasingly looking for eco-friendly, resealable, and convenient options.
Understanding Stand Up Pouch Packaging
Stand-up bags are a big step forward in flexible packaging technology. They give food and drink companies a flexible option to regular containers. Because these packages are made with a bottom flap, they can stand up on their own on store shelves, making the product and company more visible. Multiple layers of materials are laminated together during the production process. These layers are usually polyethylene, polyethylene terephthalate, aluminium foil, or recyclable films. This creates protective qualities that are specific to the needs of the product.
Material Construction and Barrier Technologies
Modern pouches are made with complex mixtures of materials that keep the goods safe from outside influences. VMPET (Vacuum Metallised Polyester) technology protects very well against water getting in, oxygen getting in, and light breaking down. With this multilayer method, manufacturers can create precise barrier properties that match the sensitivity levels of their products. High-oxygen barriers help coffee brands keep their products from going bad, while snack makers focus on keeping their snacks crisp by protecting them from moisture. Using advanced glue, the lamination process joins these layers together to make a single structure that works well during storage and delivery.
Choosing the right material depends on more than just its barrier qualities. It also needs to be strong, resistant to heat, and able to keep the seal intact. When it comes to closing and fluidity, polyethylene is great, and PET adds structural stiffness and clarity. For goods that need to stay fresh for a longer time, aluminium foil layers work better as a barrier. When made right, biodegradable options made with PLA or PBAT materials address concerns about sustainability without lowering product safety.
Customization Capabilities and Features
There are many ways to customise flexible pouch formats to fit a wide range of product needs. Zipper closures make it easy to get to the product more than once while keeping it fresh, which is especially useful for packages that serve more than one person. Spout fittings make it easier to pour liquid or almost-liquid things like sauces, drinks, and seasonings in a controlled way. Tear notches make it easy to open, which is more convenient for customers. Window screens let customers see the product, which builds trust among customers by showing the product honestly.
Sizes range from single-serving amounts to large sizes that weigh more than five kilos, so they can be used for a wide range of purposes and by different types of customers. Shape variations include standard stand-up pouches, flat-bottom designs that offer box-like stability, side-gusset formats that maximise fill volume, and speciality contours that make the product stand out on the shelf. This design freedom lets brands make their goods stand out while also making them work better in certain situations.
Manufacturing Process and Quality Control
Production begins with rotogravure printing for stand up pouches. On film, cylindrical plates produce high-resolution pictures. Our facility features seven high-speed, eleven-color printing lines. This lets us vividly describe brand and product messages. Spot UV treatment adds visual and physical depth to trademarks and important statements, increasing their value.
Laminating machines adhere layers of material under pressure and temperature after printing. This ensures uniform layer adhesion and a sturdy barrier. Six specialist laminating lines can handle material combinations from two to five layers. Next, laminated rolls are precisely cut, folded, and sealed by pouch-making machinery. Our 49 converting tools provide exact measurements for automated finishing lines to function together.
Quality assurance techniques are employed throughout the manufacturing process, not simply at inspection sites. Raw material verification verifies the supplier respects FDA and BRC food handling requirements. In-process tracking monitors printing accuracy, laminate bond strength, and seal integrity. Final testing ensures the shield works, is sturdy, and retains the same size. This all-around approach reduces defects and ensures repeat product performance.
Key Benefits of Stand Up Pouch Packaging for the Food and Beverage Industry
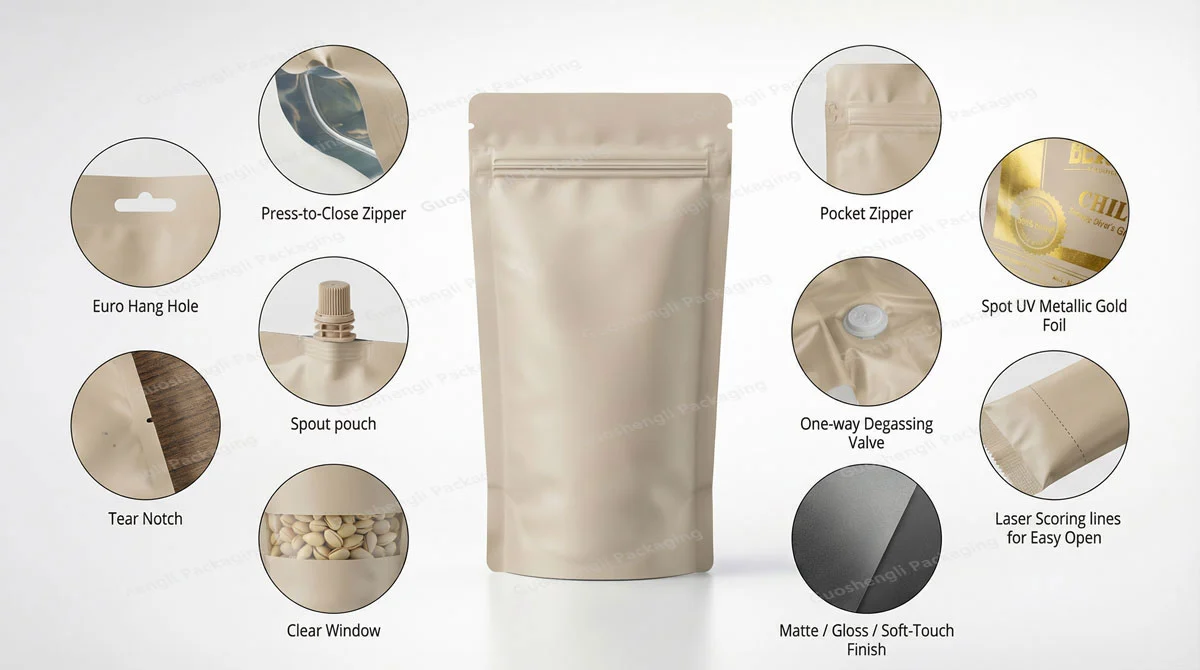
Flexible pouches outperform rigid packaging in multiple ways. Food and beverage firms are realising these advantages go beyond cost reductions to include supply chain efficiency, brand uniqueness, and environmental responsibility. Understanding these interrelated benefits helps procurement professionals make educated choices that meet operational and strategic goals.
Superior Product Protection and Shelf Life Extension
Advanced pouch structures' main benefit is barrier characteristics. Oxidation degrades flavours, nutrients, and colours, but multilayer construction blocks oxygen. Hydroscopic products like powders, dried fruits, and baked goods are protected from humidity-induced quality loss by moisture barriers. Light-blocking coatings protect photosensitive substances including vitamins and natural colourants.
Product categories and barrier specifications affect shelf life improvements. High-barrier pouches keep snacks crisp three to five times longer. More aromatic compounds are retained in metallized coffee than paper-based alternatives. Protection from oxygen and moisture reduces active ingredient degradation in nutritional supplements, sustaining label claims throughout product lifespan.
Resealable closures protect beyond opening, reducing waste and customer use. After each access, zipper mechanisms seal, maintaining barrier integrity for repeated product use. Family-sized packages and bulk formats benefit from this functionality because preservation between uses affects consumer satisfaction and repurchase behaviour.
Cost Efficiency and Supply Chain Optimization
Material efficiency boosts the economy. Flexible pouches save raw material by using less packaging material per volume. Transporting lighter packages reduces distribution network costs, fuel usage, and carbon emissions. Small pre-shipments optimise warehouse space and save storage expenses.
Production economics promote flexible forms for faster changeover and reduced equipment costs. Pouch lines increase production flexibility by supporting multiple product sizes and requirements with minimal downtime. Automated filling systems provide high-volume, precise manufacture.
Digital printing provides market testing and limited edition manufacture with customisable minimum order quantities. Digital printing allows small runs without rotogravure plate-making costs. This reduces inventory risk when launching new products or seasonal varieties and lets brands test market response before mass production.
Enhanced Brand Visibility and Consumer Appeal
Packaging is quiet salesmanship at the moment of purchase; thus, visual impact is crucial. Stand-up pouches maximise brand communication with large front, rear, and gusset printed areas. Rotogravure printing produces highly detailed images with rich colour saturation that attracts customers.
Structural design enhances shelf presence beyond graphics for stand up pouches. Horizontal formats are less prominent than vertical ones. Pouches with unique silhouettes break up shelf clutter. Products are seen via transparent windows, boosting customer trust.
Premium finishes increase value and tactile engagement. Matte surfaces reduce store lighting glare and express natural, handcrafted positioning. Glossy finishes convey modernity and product freshness. Soft-touch coatings distinguish luxury products with a pleasant touch. Spot UV highlights emphasise brand logos and key messaging.
Environmental Sustainability and Regulatory Compliance
Sustainability affects packaging as consumer awareness and legislation evolve. Due to their reduced capacity, flexible pouches produce less waste. Studies show flexible packaging creates 30% less landfill debris than rigid containers.
More infrastructure means more recycling options. Single polymer mono-material architectures allow end-of-life mechanical recycling. Recycling accepts polyethylene pouches. Clear recycling guidelines promote the circular economy.
Renewable compostable materials have other uses. Industrial composting breaks down PLA dry product mixtures. Product protection and fossil fuel reduction are achieved using these materials. Because plastics have different barrier and mechanical characteristics, performance validation is needed.
Market entry requires food contact standards. Global standards, FDA approval for US distribution, and EU regulations for European markets require rigorous material testing and documentation. The ISO 9001 quality management system and BRC food safety certification ensure materials and procedures meet regulations. SGS tests migration limits and material composition for client compliance.
How to Choose the Best Stand Up Pouch for Your Food or Beverage Product
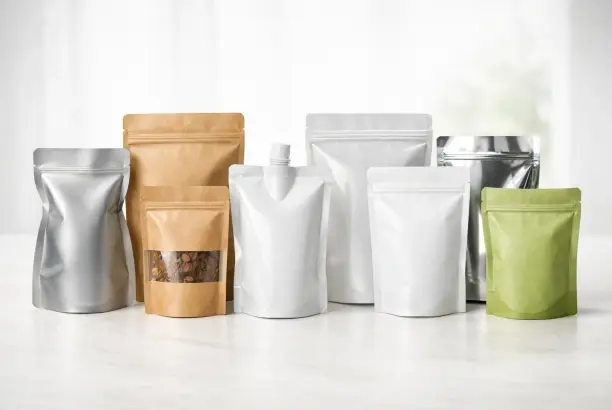
Product qualities, distribution circumstances, and brand positioning goals must be considered while choosing bag parameters. Procurement experts must balance technical performance, cost, and sustainability. Systematic evaluation frameworks assist in choosing packaging for particular applications despite many factors.
Assessing Product Compatibility and Barrier Requirements
Minimum barrier performance depends on product characteristics. Powders, dried fruits, and snacks need high moisture vapour transmission rate barriers like metallised films or aluminium foil. To prevent oxidation and rancidity, oxygen-sensitive products like coffee, nuts, and fats need low oxygen transmission rates. Coffee and tea aroma retention need structures that restrict volatile chemical escape.
Temperature during distribution and storage affects material choice. Flexible and sealable films are needed for refrigerated and frozen products. Product materials must tolerate high temperatures without deforming. Heat- and pressure-resistant constructions are needed for post-packaging sterilisation retorts.
Product-packaging chemical compatibility prevents unwanted interactions. Materials that resist degradation are needed for acidic products. Grease-resistant structures are needed for oils and fats. Spices and seasonings with volatile ingredients need strong flavor-blocking properties.
Evaluating Design Features and Functional Elements
Closure methods greatly affect product preservation and user experience. Products used several times stay fresh with resealable zippers. Press-to-close systems ensure closure with audible and tactile feedback. Consumers with limited dexterity may use slider systems easily. Controlled liquid and pourable product distribution is easier with spout fitments.
Opening characteristics balance accessibility and tampering. Intuitive tear notches make opening without tools easy. Laser scoring allows predetermined tearing. Top-seal designs provide full access to culinary products and snacks.
Transparent windows have uses beyond product visibility. They build consumer confidence by assessing quality before purchase. They decrease package waste by letting customers check condition and amount. Window location and size must be carefully considered for structural stability and visibility.
Comparing Supplier Capabilities and Certifications
Supplier selection strongly impacts supply chain reliability and product uniformity for stand up pouches. Production capacity affects volume and corporate growth. High-volume orders and specialist production are possible with our 7 printing lines, 6 laminating machines, and 49 converting machines.
Food safety and manufacturing regulations are verified by quality certifications. The ISO 9001 certification shows quality management. BRC certifies major retailers' food safety standards. Compliance papers from the FDA validate food-contact material compatibility. These certifications reduce customer compliance risk and open global markets.
Lead time manages urgent and regular production. Time-sensitive launches and promotions may be manufactured in 7-10 days using digital printing. Rotogravure printing creates high-quality graphics at an affordable cost for large quantities in 15-20 days. These timelines help procurement teams coordinate package availability with product launches and inventory management.
Technical assistance helps beyond product delivery. Barrier attributes and cost are optimised by material selection. Designers ensure pouch artwork prints effectively. Filling line compatibility testing avoids production start-up issues. Our team provides specification-phase solutions for unique application needs with 25 years of manufacturing experience.
Procurement and Ordering Guide for Stand Up Pouches
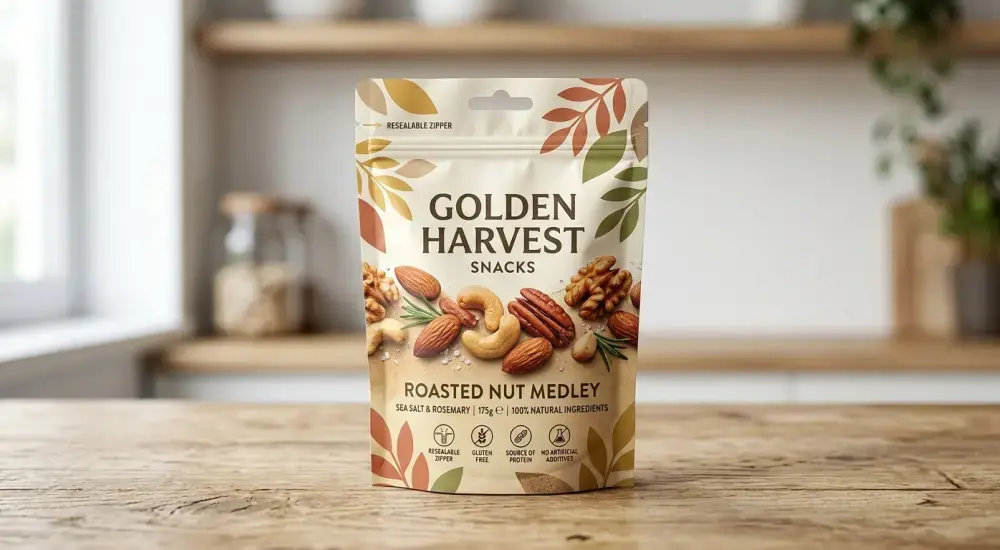
Streamlining procurement reduces costs, lead times, and manufacturing supplies. Supplier interaction, specification creation, and order management strategies provide value across the procurement lifecycle. Understanding industry norms and using manufacturer capabilities improves first orders and continuing connections.
Developing Clear Specifications and Requirements
Comprehensive specifications reduce confusion and assure product functionality. Technical parameters should specify material structure, layer composition, barrier performance targets, oxygen transmission rate and moisture vapour transmission rate thresholds, and width, length, and gusset depth with acceptable tolerances.
Graphic needs include artwork file formats, Pantone-based colour matching systems, and matte, gloss, or spot UV finishing. Zipper type, spout specifications, and window dimensions must be defined. Production volume, package configuration, and delivery timing complete the specification structure.
Sample testing verifies specifications before mass production. Physical samples provide accelerated shelf life testing, drop testing, seal strength measurement, and colour accuracy verification for barrier integrity, structural performance, and graphic replication. This validation process identifies adjustments before mass production.
Negotiating Pricing and Minimum Order Quantities
Material purchase, printing plate investment, and production setup pricing reflect economies of scale. Bulk material purchases and lengthier production cycles amortise setup expenses, giving volume commitments better pricing. Understanding these dynamics helps procurement teams arrange orders for cost effectiveness and inventory control.
Minimum order quantities vary per manufacturing technique. Due to printing plate investment and setup complexity, rotogravure printing has higher minimums but lower unit costs for huge quantities. For market testing and specialised applications, digital printing allows smaller quantities without plate costs. Total procurement cost is optimised by balancing these options against demand forecasts and cash flow.
Custom printing, premium materials, and special features increase cost. Embossing, spot UV coating, and metallic inks boost finishing expenses. Multi-layer barrier constructions using aluminium or speciality polymers cost more. Component prices include proprietary zippers and fitments. Clear communication regarding these aspects during the quote helps balance functionality and budget.
Managing Production Schedules and International Logistics
Production planning coordinates packaging availability with product manufacturing. Artwork approval, pre-production sample, manufacture, and shipping include lead time management. Delays in downstream activities are avoided via milestone communication.
International shipping involves customs, import charges, and transit time. Ocean freight is cost-effective for large volumes and takes 4-6 weeks from Asian manufacturing to North American ports. Air freight delivers in 4-5 days for urgent needs or inventory shortages. Understanding these tradeoffs helps choose a mode that balances cost and timing.
Product categorisation, country of origin paperwork, and commercial invoicing must be correct for customs. Duty rates are determined by Harmonised System codes. Trade agreements may provide favourable tariff treatment for certificates of origin. Experienced manufacturers help navigate these standards, decreasing clearance delays and compliance risk.
Building Strategic Supplier Relationships
Long-term relationships provide benefits beyond transactions. Manufacturers can research customer needs, anticipate needs, and prioritise service with established relationships. Volume commitments help optimise capacity allocation and material procurement by predicting production schedules.
Supplier dependability is measured by quality, on-time delivery, and response. Regular company reviews evaluate performance, identify improvements, and match strategic goals. Through waste reduction, process optimisation, and innovation, collaborative continuous improvement benefits everyone.
Communication protocols clarify technical concerns, order status, and problem resolution. Designated account reps maintain relationships. Application-specific questions and troubleshooting are handled by technical specialists. This organised method streamlines information flow and speeds up time-sensitive decisions.
Future Trends Shaping Stand Up Pouch Packaging in Food & Beverage
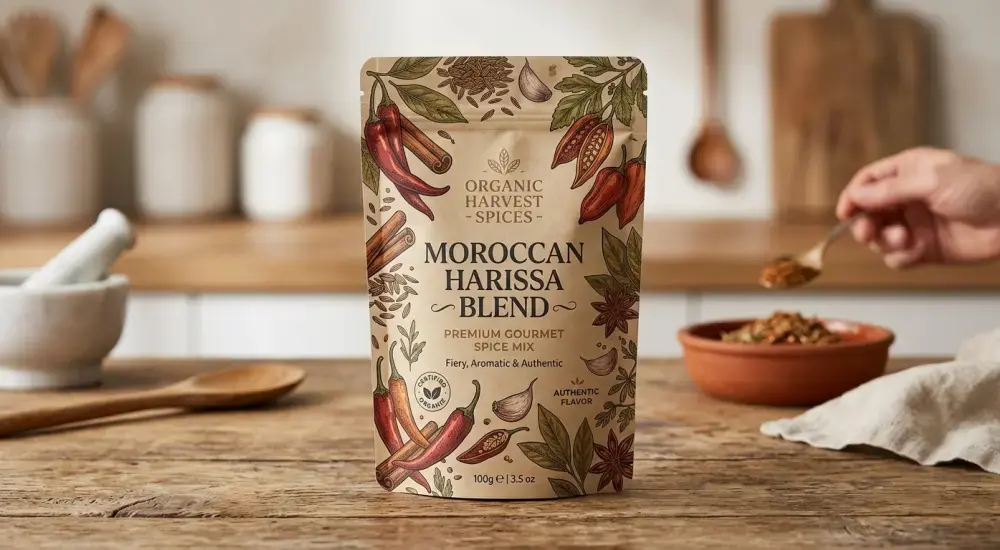
Technological advancements, regulatory changes, and customer preferences drive fast flexible packaging sector evolution. Understanding new trends helps procurement experts predict future demands and assess supplier capabilities. Packaging strategies increasingly consider long-term market trends and functional needs.
Sustainability Innovation and Circular Economy Integration
Environmental factors increasingly influence packaging material and design. Developers emphasise recyclable mono-material designs for end-of-life processing and product preservation. Polyethylene pouches solve recycling collecting system, and disposal difficulties.
Recycling reduces virgin material consumption and promotes circular economy. Food-contact-safe post-consumer recycled materials allow sustainable sourcing claims. This process involves careful supplier selection for recycled material quality and regulatory compliance.
Without recycling facilities, biodegradable and compostable materials operate. Renewable PLA and PBAT blends degrade under certain conditions. These materials vary from plastics in barrier, mechanical, and thermal endurance, requiring performance evaluation.
Lightweighting saves material by optimising structures and performance. Advances in material science offer thinner gauges with appropriate strength and barrier. Reducing resource use and transportation impacts helps the environment and saves money.
Smart Packaging and Digital Integration
Connected packaging improves supply chain visibility and customer interaction. Smartphones can read pouch QR codes for product information, preparation instructions, and brand storytelling. This digital link allows data collection for marketing and product development.
Visual indications from time-temperature exposure or packaging integrity indicate product freshness. These technologies objectively analyse product quality, boosting customer trust and reducing waste. Application is restricted by cost but grows as technological prices fall.
Blockchain-based food traceability solutions address safety and authenticity. Serialisation tracks shipments across supply chains, enabling quick quality and counterfeit reaction. As traceability needs grow, regulations may speed adoption.
Advanced Barrier Technologies and Material Science
Nanotechnology improves barrier characteristics via molecular-level material engineering. Nano-clay composites are transparent and increase oxygen and moisture barriers. These advances might decrease material thickness and improve protection, boosting sustainability and performance.
Renewable bio-based barrier coatings replace petroleum-based ones. These coatings improve paper and film barrier properties and assist sustainability. Application-specific validation guarantees product category performance.
Instead of passively blocking oxygen, oxygen scavenging systems remove oxygen from package headspace. This technology uses proactive atmosphere management to extend sensitive product shelf life. Sachets or integrated film additives are used, each with benefits for certain applications.
Conclusion
Food and beverage companies seeking efficient, sustainable, and consumer-friendly packaging will benefit from stand up pouches. Superior barrier protection prolongs shelf life and reduces loss. Economical production and distribution optimise supply chain economics. Marketing distinctiveness is improved by strong branding. Flexible pouch formats enable innovation as sustainability requirements rise and consumer preferences change. Choose manufacturing partners with established capabilities, extensive certifications, and application experience for dependable supply and performance. Strategic packaging selections that address these factors help businesses compete in global marketplaces.
FAQ
1. Are Stand Up Pouches Recyclable and Environmentally Friendly?
Recyclability depends on material structure and local infrastructure availability. Mono-material polyethylene pouches integrate into existing plastic recycling streams where collection programs operate. Multi-layer structures incorporating different polymer types present recycling challenges, though specialized facilities process certain combinations. Clearly labeled recycling instructions improve consumer participation. Compostable options provide alternative end-of-life pathways for specific applications, requiring industrial composting facilities for proper degradation.
2. How Much Does Custom Printing Affect Lead Time and Cost?
Digital printing enables production within 7-10 days without plate investment, supporting short runs and rapid turnaround at higher unit costs. Rotogravure printing requires 15-20 days including plate preparation but delivers superior graphics quality and cost efficiency for volumes exceeding 50,000 units. Spot UV coating and premium finishes add processing time and incremental cost. Balancing these factors against volume requirements and timeline constraints optimizes procurement decisions.
3. What Barrier Properties Should I Specify for Different Product Types?
Moisture-sensitive products require structures achieving moisture vapor transmission rates below 0.5 g/m²/24hr. Oxygen-sensitive products need oxygen transmission rates under 1 cc/m²/24hr for adequate protection. Coffee and products containing volatile aromatics benefit from metalized films providing superior barrier performance. Working with experienced manufacturers helps match barrier specifications to product characteristics and desired shelf life targets.
Partner with a Trusted Stand Up Pouches Manufacturer
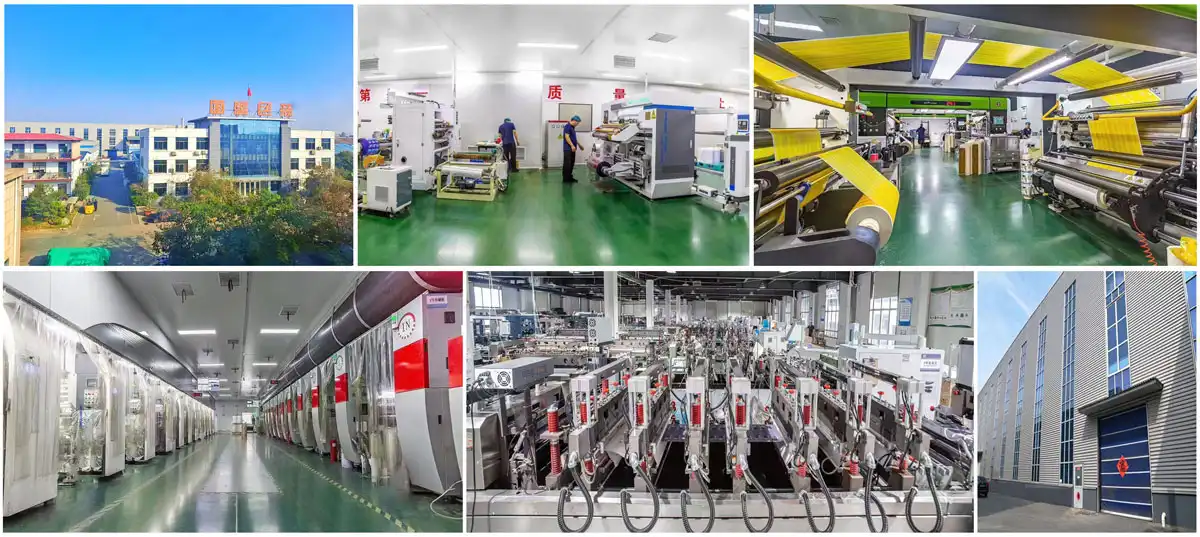
Guoshengli Packaging brings 25 years of flexible packaging manufacturing experience serving food, beverage, pet food, and supplement brands across North America, Europe, and Asia-Pacific markets. Our comprehensive capabilities include rotogravure printing up to 11 colors, advanced VMPET barrier structures, and rapid production timelines meeting urgent requirements. ISO 9001, BRC, and FDA certifications ensure consistent quality and regulatory compliance. Whether you need custom printed pouches for product launches or reliable supply for established production lines, our technical team provides expert consultation matching pouch specifications to your specific application requirements. Contact our stand-up pouches supplier team at sales@guoshengpacking.com to discuss your project requirements, request samples, and discover how our manufacturing capabilities can support your packaging objectives with reliable, cost-effective solutions.
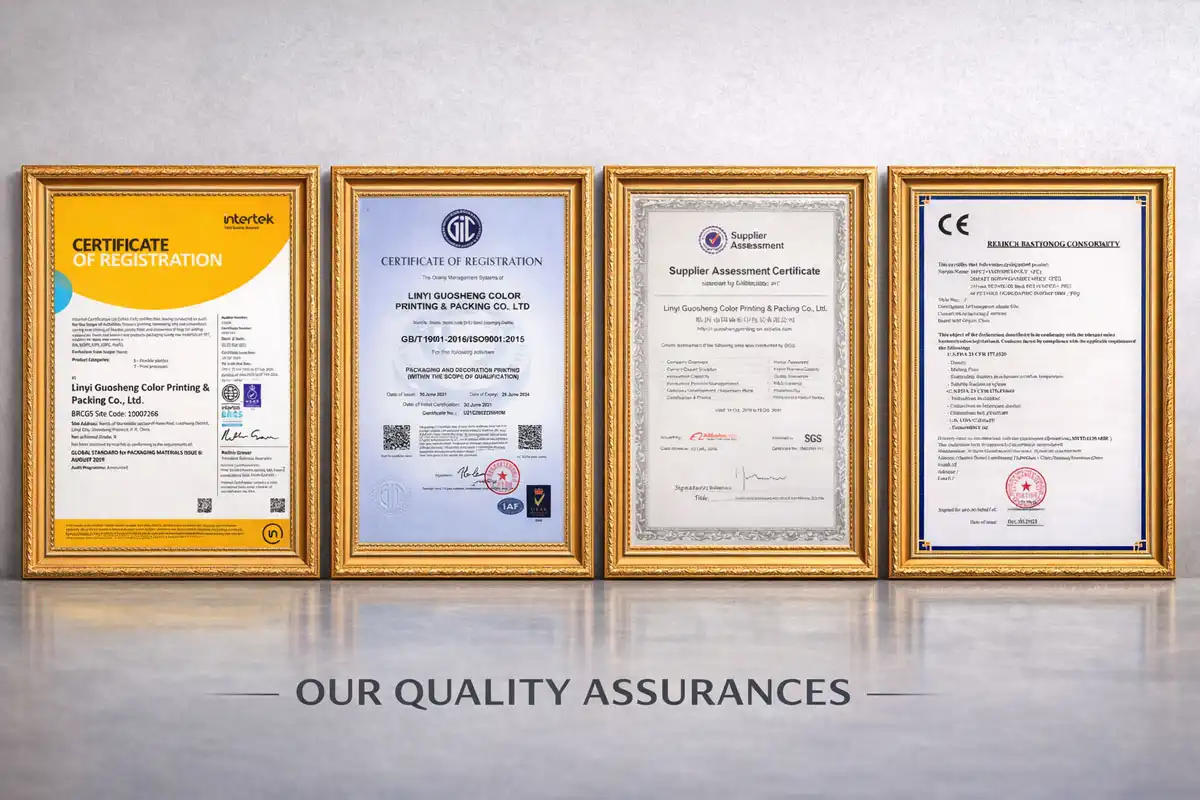
References
1. Robertson, Gordon L. "Food Packaging: Principles and Practice, Third Edition." CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Vol. 72, No. 3, 2007.
3. Yam, Kit L. "The Wiley Encyclopedia of Packaging Technology, Third Edition." John Wiley & Sons, 2009.
4. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. "Plastics Packaging: Properties, Processing, Applications, and Regulations, Third Edition." Hanser Publications, 2016.
5. Coles, Richard and Mark Kirwan. "Food and Beverage Packaging Technology, Second Edition." Wiley-Blackwell, 2011.
6. Brody, Aaron L. and Kenneth S. Marsh. "The Wiley Encyclopedia of Food Science and Technology: Flexible Packaging." John Wiley & Sons, 1999.
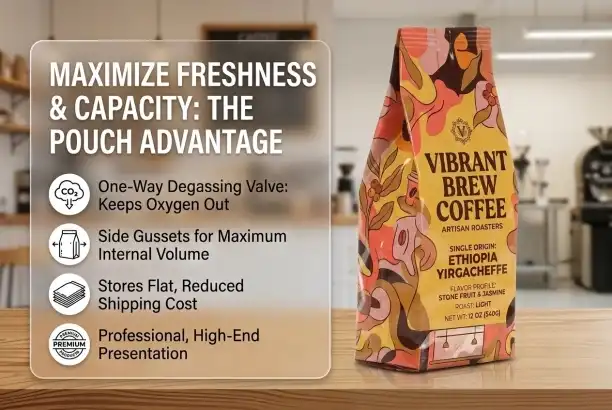
The main benefits of using a side gusset pouch with valve are that it keeps food fresh longer by degassing it automatically, it protects against air and moisture better than other packaging, it takes up less room, and it makes products last longer. The 1kilo side gusset pouch with valve is designed to hold things like freshly roasted coffee, which need to release CO2 quickly. This style of packing has expandable side panels and a one-way opening system that lets interior gases leave but keeps outside air from coming in. This keeps the product's taste, flavour, and integrity while it's being shipped and displayed in stores.
Understanding Side Gusset Pouches with Valve: Features and Benefits
What Makes Side Gusset Design Unique
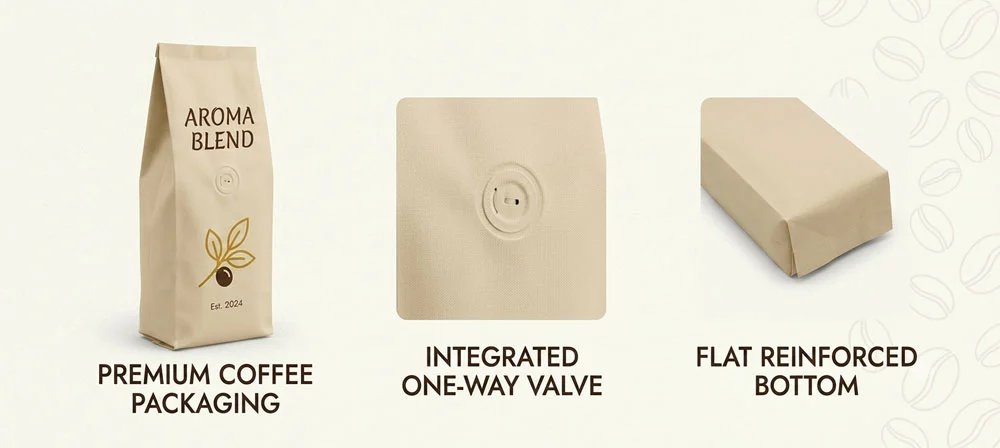
Side gusset bags have panels on both sides that can be expanded. These panels fold flat when not in use but open up when they are. This design makes a box-like, rectangular shape that stands straight up on shelves and takes up very little space in the warehouse before it is used. Because this structure is structurally efficient, it has big benefits for brands that need to manage a lot of goods. Side gusset designs spread weight evenly along vertical lines, making it easier to stack during travel and storage. This is different from stand-up bags, which need a bottom gusset to be stable. Coffee roasters like this shape for packing because it holds exactly one kilogram of beans without leaving too much empty space, which lowers the cost of shipping each unit.
How the Degassing Valve Functions
The built-in one-way valve is very important for coffee packaging and other related uses. For several days after being roasted, freshly roasted coffee beans give off large amounts of carbon dioxide. If there isn't a way for this gas to escape, it builds up inside the pouch and can cause it to expand or even burst. The one-way design of the valve lets CO₂ exit but keeps oxygen from getting in, which would speed up the staleness process. This feature greatly increases the shelf life compared to options that don't have valves. Protocols for testing show that valves that work properly keep the purity of the internal atmosphere for months, protecting the volatile chemical compounds that define the quality of speciality coffee products.
Barrier Protection Through Multi-Layer Construction
Modern 1kilo side gusset pouch with valve solutions use complex laminate structures, usually made of PET for strength, aluminium foil for blocking light and oxygen, and polyethylene for being able to seal with heat. This multi-layer structure stops moisture transmission rates below 0.5 g/m³/24 hours and oxygen transmission rates below 0.01 cc/m²/24 hours. These are the levels of performance that are needed to keep the quality of the product in tough transportation settings. The barrier properties keep out outside contaminants and keep freshness markers inside. Food companies that want to package moisture-sensitive powders, high-end pet treats, or health supplements can use these engineered barrier specifications to keep the products from breaking down over the course of months.
Material and Design Considerations for 1 Kilo Side Gusset Pouches with Valve
Selecting Appropriate Laminate Structures
The composition of the materials directly affects how well the packaging works and how much it costs. Standard food-grade laminates come in PET/AL/PE types that offer the best barrier protection and are good for products that need to stay fresh for a long time in climates that change often. Different types of structures, like PET/VMPET/PE, offer good barrier qualities at lower material costs, making them good for products that are moderately sensitive to air. New environmentally friendly choices have top layers made of bio-based plastic or paper that keep their usefulness while making them easier to recycle. When making a procurement decision, it's important to weigh barrier requirements against sustainability goals and the preferences of the target market. When brands come to Europe, they often choose reusable buildings made of a single material, even if they cost a little more. This is because consumers expect brands to follow circular economy rules, and regulations are also moving in the same direction for 1kilo side gusset pouch with valve.
Valve Placement and Customization Options
The best place to place the valve depends on the filling tools and the product itself. Standard placement is in the upper third of the front panel, which lets gas escape quickly after the pouch is closed and stood upright. Some automatic filling lines need valves to be placed in certain ways so that they don't get in the way of quality checking cameras or conveyor systems. Side gusset pouches with valves can be customised in many ways, such as by adding a zipper for resealing, tear notches for easy opening, clear windows to see the product inside, and a matte or glossy finish that changes how the pouch looks on the shelf. Custom printing options that include eleven-color rotogravure processes let brands use complex graphics that set their products apart in stores where competition is high.
Impact on Supply Chain Efficiency
Choices about materials and designs affect how well logistics work all along the supply chain. Because side gusset bags are small and empty, they take up less space when they are shipped, which saves money on freight costs. Their stable, rectangular-filled form makes palletisation more efficient because it lets more units fit on each pallet than options with more complicated shapes. The strong seal strength built into high-quality 1kilo side gusset bag with valve goods keeps them from breaking while being handled, which cuts down on product loss and customer complaints. Brands that want to expand their distribution networks need packaging that works well in all kinds of transportation situations, from temperature-controlled warehouses to last-mile deliveries in extreme temperatures.
Comparing Side Gusset Pouches with Other Packaging Solutions
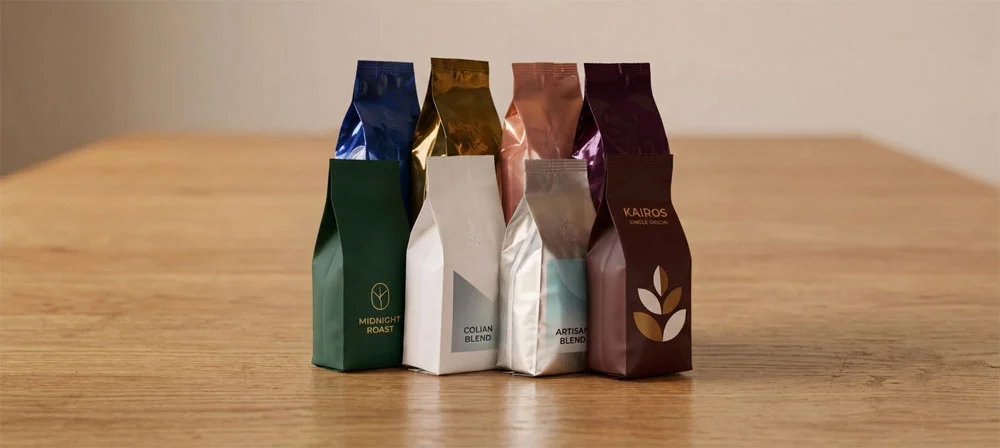
Side Gusset vs. Stand-Up Pouch Formats
While both formats provide vertical shelf presentation, they serve different operational priorities. Stand-up pouches utilize a bottom gusset that makes a wide base that is very stable on store shelves and gives you plenty of room for branding. But this design needs more space when it's not full, and it might not work as well for goods that don't need to sell themselves with the front panel being as visible as possible. Side gusset bags are great at saving room and are often used in trade or membership models where safety and shipping performance are more important than brand message. The 1 kg side gusset pouch with valve is perfect for bulk coffee distribution, where roasters care more about keeping the coffee fresh than how it looks on a store shelf.
Flat Bottom Pouches and Their Applications
Flat bottom pouches, which are also called box pouches, are more stable when standing because they have a square base. This format gives products a premium shelf presence that makes it perfect for high-end retail positioning. Because they are harder to make and use more materials, they usually cost more per unit than side gusset configurations. In competitive retail settings, brands that put an emphasis on luxury presentation may be able to charge more for this. Side gusset pouches with valve, such as a 1kilo side gusset pouch with valve, are more affordable and offer great functionality. This makes them useful for volume packaging tasks in coffee roasting, pet food production, and supplement production, where protection and efficiency are more important than premium looks.
Evaluating Total Cost of Ownership
When comparing packing options, you need to look at more than just the unit buy price. Side gusset bags are better for shipping weight, storage density, and handle efficiency, all of which lower the overall cost of the supply chain. As a result of being easier to make than flat bottom designs, they usually have faster lead times and more production options. Being able to order smaller production runs without having to pay too much extra gives brands strategic flexibility when they have to deal with seasonal changes in volume or test out new product variants. Quality manufacturers offer competitive minimums on side gusset pouches with valve while still letting you make the changes that are needed for your brand to stand out.
Procurement Insights: How to Select and Buy the Right Side Gusset Pouch with Valve
Verifying Supplier Certifications and Capabilities
As the first step in your due diligence research, you should make sure that any possible sellers have the right quality certifications for the places you want to reach. Getting ISO 9001 certification shows that you can manage quality in a structured way. The BRC Global Standards for Packaging approval is very detailed about meeting the quality and safety standards for packaging that are accepted in all foreign markets. Documentation from the FDA shows that the products meet US food contact rules. Third-party confirmation of barrier qualities and seal strength standards is given by SGS tests results. In addition to certificates, you should also look at the providers' production ability to make sure they can grow with your business. Companies that have more than one printing and turning line show that they have the means to handle both new orders and future volume growth without affecting delivery times.
Understanding Lead Times and Order Processes
Depending on the printing method and the size of the order, custom 1kilo side gusset pouch with valve orders usually take between three and six weeks to be made. Digital printing allows for shorter runs and faster response times, usually seven to ten days. This makes it perfect for testing the market or launching a new product. Rotogravure printing needs to have the cylinders prepared, but it produces more consistent colours and saves money on larger orders. Lead times are about fifteen to twenty days. When you plan your purchases well, you take these deadlines and the time it takes to ship into account. Air freight cuts the time it takes to send to four or five days, but it costs more to ship. Ocean freight is a cheap way to ship well-known goods that have predictable demand cycles. By building stock buffers, you can avoid running out of stock while manufacturers make more for later orders.
Evaluating Customization and Private Label Services
Since packaging is one of the first times people see a company, being able to customise it is an important factor to consider when buying something. Check to see if the providers offer design help to make sure that the artwork is optimised for printing processes so that the colours and graphics are clear. Make sure the file formats work together and ask the technical teams if they can suggest changes to the structure that will make it work better or cost less. Private labelling lets brands get tried-and-true package designs with little change, which speeds up time to market. Flexible minimum order quantities help businesses grow by letting them place smaller orders at first, which lowers the risk of running out of inventory and opens the door to volume discounts as sales rise. Building ties with providers who understand how these business factors work leads to long-term success that goes beyond routine buying.
Environmental Impact and Future Trends in Side Gusset Pouch Packaging
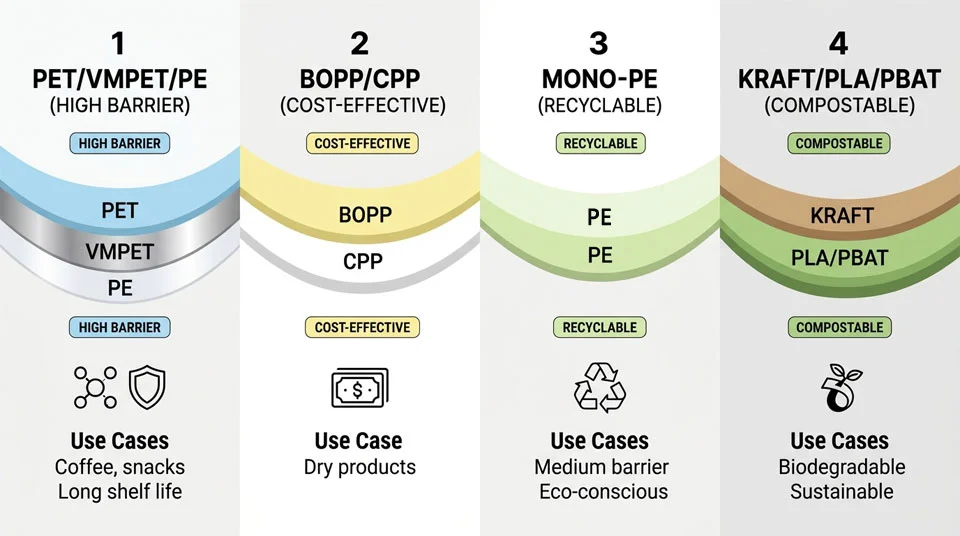
Sustainability Challenges and Innovations
Traditional multi-layer laminates protect products very well, but they are hard to recycle because the materials are so complicated. To separate the layers of aluminium, plastic, and adhesive, you need special equipment that most municipal recycling systems don't have. Because of this limitation, people have come up with better, more environmentally friendly solutions. Mono-material polyethylene buildings get rid of walls made of different materials, which lets recycling happen through current plastic garbage streams. Bio-based polyethylene made from green feedstocks cuts down on the need for dirty fuels while keeping the same level of functionality. Compostable films made of PLA and PBAT can be thrown away through industrial composting when they are no longer useful. However, brands need to make sure that the local composting infrastructure can handle these materials. The 1kilo side gusset bag with valve structure can be changed to fit these new materials. This lets brands match their goals for sustainability with their needs to protect their products.
Regulatory Landscape and Market Expectations
Both government action and market desire for long-term answers are driven by consumers' knowledge of packing trash. More and more, European Union rules require packaging materials to be able to be recovered and to contain recyclable materials. In the United States, consumers are becoming more and more interested in brands that are environmentally friendly through their package choices. When businesses buy things from each other, they often look at sustainability factors along with cost, quality, and delivery reliability. A brand that is looking to the future knows that investing in environmentally friendly packaging now will help them meet current customer needs and meet future regulatory requirements. Manufacturers who offer both conventional and environmentally friendly options give brands the freedom to move through this transition at a pace that works for their market positioning and cost structures.
Emerging Technologies in Valve and Printing Design
Side gusset pouches with valve are always getting better in terms of both how they look and how well they work. Modern valve designs use smaller shapes that save money on materials while still removing gases efficiently. Smart package technologies let QR codes and NFC tags be added, which connect customers to brand stories, authenticity checks, or brewing directions. New developments in digital printing make it possible to get quality close to rotogravure at shorter run lengths. This makes custom packaging more accessible for smaller brands. When applied to paper surfaces, improved barrier layers make long-lasting options that are similar to the performance of plastic film. By keeping up with these changes, procurement workers can use new ideas that give them a competitive edge in protecting products, setting brands apart, and taking care of the environment.
Conclusion
Finding the right packaging solution means balancing a lot of different things, such as protecting the product, saving money, showing off the brand, and being environmentally friendly. The 1kilo side gusset pouch with valve meets these needs with a well-thought-out design that keeps food fresh, makes logistics easier, and allows for customisation. Procurement professionals can make decisions that are in line with business goals if they understand the structural benefits, material choices, and seller evaluation factors that have been discussed in this analysis. Sustainability is becoming more important in packaging, but performance standards that are necessary for product quality must still be met. In order to be successful in the long run in competitive markets, you need to work with makers that have a lot of experience, scientific knowledge, quality standards, and a dedication to new ideas.
FAQ
1. Can side gusset pouches with valve be reused after opening?
These pouches are designed as single-use packaging optimized for maintaining unopened product freshness. Once opened, the barrier integrity and valve functionality are compromised. Products requiring extended use after opening benefit from resealable zipper integration, which many manufacturers can incorporate into the design. The zipper enables consumers to close the package between uses, though freshness preservation will gradually decline compared to the unopened state.
2. What are typical lead times when ordering a custom 1-kilo side gusset pouch with valve?
Production timelines typically range from three to six weeks depending on printing method and order specifications. Digital printing processes deliver finished pouches within seven to ten days, suitable for urgent needs or small production runs. Rotogravure printing, offering superior color consistency for larger volumes, requires approximately fifteen to twenty days. These timelines reflect manufacturing duration; shipping adds four to five days for air freight or several weeks for ocean transport.
3. How can buyers verify valve functionality before placing large orders?
Working with certified suppliers holding ISO, BRC, and FDA approvals provides assurance that manufacturing processes include valve functionality testing. Request pre-production samples to conduct internal testing simulating your specific product and storage conditions. Reputable manufacturers perform vacuum testing and pressure testing on valves during production runs, confirming one-way airflow performance. Establishing quality specifications in purchase agreements and requesting test reports with shipments creates accountability for consistent valve performance across repeat orders.
Partner with Guoshengli Packaging for Your Side Gusset Pouch with Valve Needs
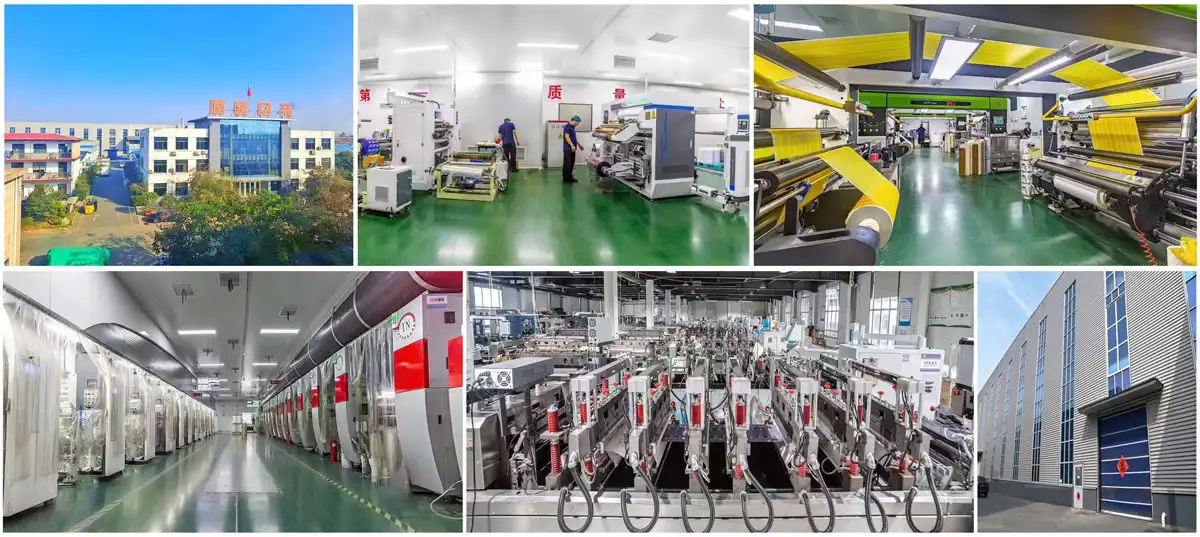
Guoshengli Packaging brings over 25 years of flexible packaging manufacturing expertise to help your brand achieve consistent product protection and professional market presentation. As a trusted 1kilo side gusset pouch with valve supplier, we deliver solutions engineered for real-world production environments, from material selection through final delivery. Our ISO 9001, BRC, and FDA certifications, combined with advanced rotogravure printing capabilities up to eleven colors, ensure your packaging meets both functional requirements and brand standards. We understand the complexities B2B buyers face in balancing quality, cost, and sustainability objectives. Our team provides technical guidance on material structures, valve placement optimization, and design customization that enhances shelf appeal while controlling total packaging costs. Contact our team at sales@guoshengpacking.com to discuss your specific requirements and request samples that demonstrate our commitment to manufacturing excellence and reliable supply.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice, 3rd Edition. CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Vol. 72, No. 3, 2007.
3. Coles, Richard, Derek McDowell, and Mark J. Kirwan. Food Packaging Technology. Blackwell Publishing, 2003.
4. Yam, Kit L. The Wiley Encyclopedia of Packaging Technology, 3rd Edition. John Wiley & Sons, 2009.
5. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations, 3rd Edition. Hanser Publications, 2016.
6. Brody, Aaron L. and Kenneth S. Marsh. The Wiley Encyclopedia of Food Science and Technology, 2nd Edition. John Wiley & Sons, 1999.
Stand up pouches are a revolutionary type of bendable packaging that protects products better while keeping the structure strong. These bags have a strengthened bottom flap that lets them stand up straight on store shelves. This makes your brand stand out and keeps the product fresh. Multi-layer laminated films are great at blocking moisture, air, and light, which is why stand up pouches are the package pick of choice for health supplement companies, pet food brands, and food makers who want reliable, low-cost packaging. Procurement professionals can make smart choices that extend the life of a product and make it more appealing to customers if they know about the materials, manufacturing processes, and customisation options.
Understanding Stand Up Pouches – Definition, Materials & Manufacturing
What Are Stand Up Pouches?
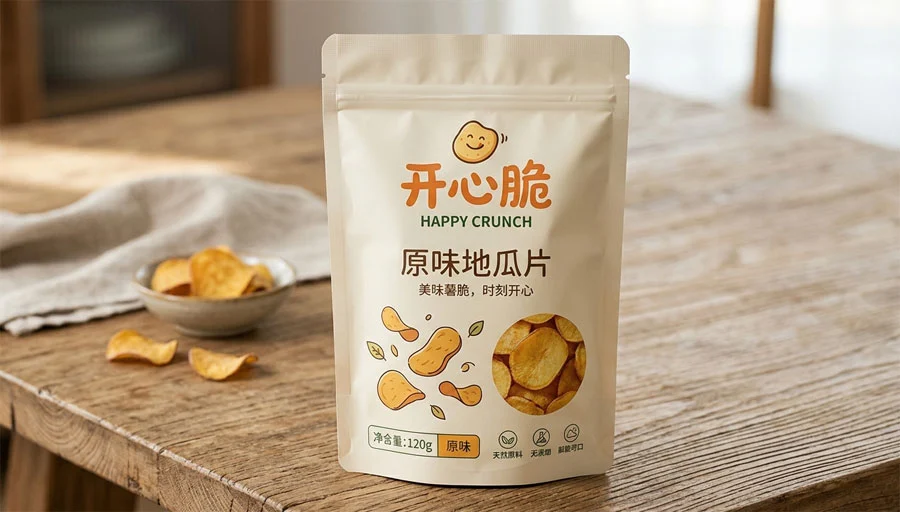
Stand up pouches are flexible packaging options made from multiple layers of laminated films that are meant to stand up on their own. The foundation of a structure is made up of a bottom gusset, which usually has a W-fold or K-seal shape and expands when filled with water to make a stable base. This design makes the best use of shelf space while giving brands and product information a lot of room to show off their work. These pouches are different from regular flat bags or hard cases because they can be filled with different amounts of product and in different ways. This means that they can be used for both automatic and human packing lines.
Material Construction and Barrier Performance
The material selection directly influences product protection and shelf life. Most pouches utilize multi-layer laminated structures combining different films to achieve specific performance characteristics:
- VMPET (Vacuum Metallized Polyester): This material provides exceptional barrier protection against moisture infiltration, oxygen exposure, and light degradation. The metallized layer reflects ultraviolet radiation while preventing gas transmission, making it ideal for products sensitive to oxidation such as coffee, nuts, and dried fruits.
- Aluminum Foil Laminates: For applications requiring maximum barrier performance, aluminum foil layers deliver near-absolute protection. These structures extend shelf life for products containing oils, fats, or volatile aromatic compounds that would otherwise permeate through standard plastic films.
- Recyclable Mono-Material Structures: Environmental considerations have driven innovation in single-polymer constructions that maintain barrier properties while enabling easier recycling. These solutions balance sustainability requirements with product protection needs, addressing regulatory pressures and consumer preferences.
Manufacturing Process Overview
The first step in production is film lamination, which attaches several layers together using glue or extruder covering to make the final barrier structure. Rotogravure printing uses brand images and product details to make accurate copies of up to eleven colours. After being printed, the laminate goes through transforming steps where bags are made, sealed, and given useful features.
Customisation options for stand up pouches include resealable zippers to keep the product fresh after opening, tear notches to make it easier for customers, hang holes for retail display, and clear windows to see the product inside. Spout fittings can hold liquid or almost liquid products, and degassing valves let carbon dioxide out of freshly roasted coffee without letting oxygen in.
Comparing Stand Up Pouches With Other Packaging Solutions
Advantages Over Rigid Containers
Because they are not as stiff as standard containers like cans, jars, and boxes, flexible bags are much easier to ship and cost less. The material efficiency is clear all along the supply chain: less weight means lower shipping costs and carbon emissions during travel; small storage before filling means less building room is needed; and so on. These things lead to real cost savings, since flexible packaging usually needs 70% less material than rigid formats of the same size.
Making things easier for customers also improves their experience. With resealable closures, you don't need to use extra storage containers because the product stays fresh between uses. Easy-tear openings get rid of the frustration that comes with rigid packages that are hard to open, and the lightweight design makes it easier for people of all ages to handle.
Laminated Versus Non-Laminated Pouches
Knowing the difference between laminated and non-laminated options makes it easier to match the needs of the product to the right packaging. Laminated bags have better protective qualities, tear protection, and structure stability because they have more than one film layer. This design is necessary for goods that need to last longer or be protected from the elements.
Single-layer bags that aren't sealed are used when high barrier performance isn't needed, like for goods with a short shelf life or things that need extra protection. These options are cheaper, but they don't last as long or as well as barriers. Because of this, they're best for promotional packaging or dry goods that don't need to be protected from oxygen or moisture.
Functional Features for Product Differentiation
Because bag designs are so flexible, they can be perfectly matched to the features of the object. Products that are eaten more than once should have resealable zip ends to keep them fresh and stop spills. Degassing valves are designed to meet the special needs of coffee packing. They let newly roasted beans release carbon dioxide while keeping air from breaking down flavour ingredients. Customers are more likely to buy something if they can see what it is before they buy it through clear windows or fully transparent constructions.
Coatings that are resistant to heat and oil solve problems with certain products. For high-temperature tasks like retort preparation for shelf-stable meals, you need special film structures that can handle being sterilised. Oil-resistant layers on the inside of goods that contain natural oils stop fat from moving around, which would otherwise damage the seal.
How to Choose the Right Stand Up Pouches for Your Business
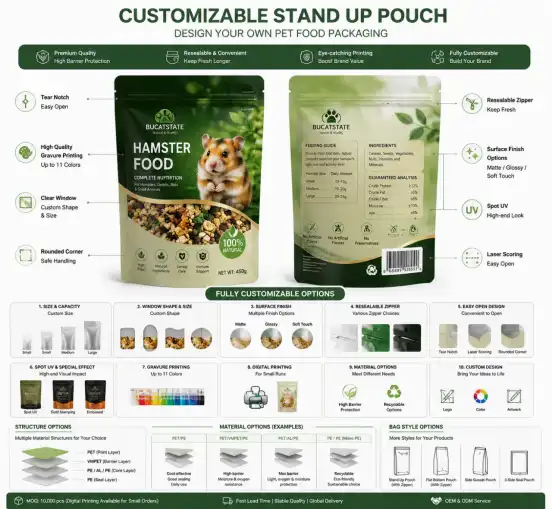
Defining Your Packaging Requirements
To choose the right package, you must first carefully look at the product's features and where it fits in the market. The type of product—dry, liquid, powder, or chunky—determines how the stand up pouches should be made and how they should be sealed. The expected shelf life affects the barrier requirements. Products that are sensitive to moisture need higher levels of protection than stable dry goods. The minimum order quantity that can be made depends on the size of the distribution network, and the budget limits determine which materials and features can be used.
It's just as important to understand your filling process. Automated vertical form-fill-seal machines need different film qualities and size limits than horizontal machines that fill pre-made bags. When you match the specifications of the package to the capabilities of the filling line, you avoid costly production delays and inconsistent quality.
Critical Selection Criteria
Material fit with your product keeps quality problems from happening and makes sure you follow the rules. Materials that come into contact with food must follow FDA or EU rules about chemical migration and keeping food safe from contamination. There are many printing choices, from simple one-color patterns to complicated images with spot UV finishing for extra shelf appeal. Environmental certifications show that a company cares about the environment and meets the needs of retailers in markets that value eco-friendly packaging.
Minimum order amounts are an important thing to think about for new brands and small businesses. Manufacturers usually need commitments on volume that match their production efficiency levels. However, digital printing technologies now allow for shorter runs for testing the market. To balance the initial investment with the costs of keeping inventory, you need to carefully plan your finances so that they are in line with your sales projections.
Industry-Specific Applications
Food and snack makers put a lot of emphasis on barrier properties that keep the texture, flavour, and nutritional value of the food. For coffee and tea, the packaging needs to be able to release gases and keep the aroma. Dried fruits and nuts, on the other hand, need moisture barriers to keep them from going bad. The needs for pet food are similar to those for human food, with extra thought given to bigger package sizes and resistance to punctures during handling.
Anti-static films keep powders from sticking to the inside of pouches, which is useful for supplement and nutritional powder packaging. Zipper seals make doses easier and keep the medicine's strength by keeping air out as much as possible. Customers are more likely to believe a product when it has clear windows or elements that let the whole thing through.
Procuring Stand Up Pouches: From Sample to Bulk Order
Sourcing and Supplier Evaluation
A thorough evaluation of the supplier is the first step in effective procurement. Your production skills must match your number needs and growth goals, and quality certifications prove that manufacturing standards are met and that regulations are followed. ISO 9001 certification shows that quality management is done in a planned way, and BRC and FDA approvals show that food safety measures meet foreign standards.
Communication skills have a big effect on the success of a project, especially when working with makers in other countries. When people talk about technical things like material specifications, barrier testing, and filling line compatibility, they need to use clear language and make sure everyone understands. Suppliers with experience in foreign markets usually have expert teams that speak English and provide a lot of information to help people make smart choices.
Understanding Pricing Elements
Custom printing adds a lot to the cost of stand up pouches, and the number of colours, complexity of the graphics, and printing method all play a role. Rotogravure printing gives better quality for large orders, but it needs cylinder engraving, which has a setup cost that is spread out over the number of orders. Because digital printing doesn't have setup costs, it's cheaper to do short runs, but the price per unit is higher.
Minimum order quantities show the levels of production efficiency at which setup costs are reasonable. Manufacturers try to find a balance between giving customers options and running their businesses efficiently. Depending on how complicated the customisation is, MOQs usually range from 10,000 to 50,000 units. Volume prices encourage people to make bigger promises, which lowers the cost per unit by making better use of materials and lowering the number of times they need to be set up.
Sample Evaluation Protocol
Asking for samples before placing a production order lowers the risk and confirms that the supplier can do what they say they can do. A full evaluation checks the integrity of the material by testing the seal's strength, checking the barrier's properties, and measuring the accuracy of its dimensions. Print fidelity assessment checks the colour reproduction against brand standards. Functional features are tested by real people, who fill out the product and handle it.
The situations used for tests should be similar to those your package will face in real life. Drop testing checks how well the package will hold up during shipping, and shelf ageing at a controlled temperature and humidity level shows if the seals might fail or the material is breaking down. This investment in validation keeps failures that cost a lot from happening after full production commitment.
Industry Trends and Sustainability in Stand Up Pouches
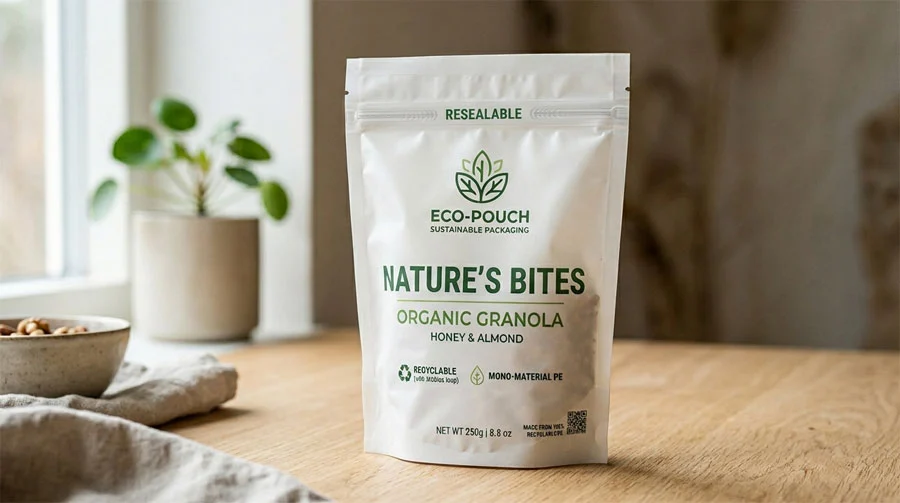
Environmental Innovation and Material Development
There is more and more pressure on the packaging business to protect products without hurting the earth. Biodegradable materials made from green resources could be used in composting, but their performance limits mean they can only be used for goods that need to last a shorter time. More business-friendly options include structures made of one recyclable material that make processing easier after use while keeping the barrier's effectiveness through advanced film technologies.
Lightweighting materials cuts down on the use of resources and pollution from transportation. Engineers are always trying to find the best film thickness and layer building by getting rid of material that isn't needed while keeping the structure strong and the shield working well. These changes help the environment in measured ways and lower the cost of packaging, which is good for both the environment and the economy.
Digital Printing and Design Technology
Digital printing makes high-quality images available to more people than they could have before, when they had to be made in big quantities to cover the costs of setup. Brands can now try multiple design variations without breaking the bank, make products more relevant to specific regions, or put out limited editions without having to pay for expensive printing methods. The adaptability speeds up response times to changes in the market and lets personalisation strategies that build stronger relationships with customers work.
Advanced design software lets you see things in three dimensions before they are made, which lets stakeholders check out how they will look on shelves and how customers will interact with them. This feature cuts down on revision cycles and boosts confidence in decisions, which shortens the time it takes to develop something and keeps the number of expensive fixes made after production commitment to a minimum.
Circular Economy Integration
Forward-thinking brands follow the principles of the circular economy by making packaging that can be used more than once and is easier to recycle. Multi-polymer laminates can be hard to separate, but mono-material designs don't have those problems. This means that more materials can be recycled and recovered. Taking part in extended producer responsibility programs shows care for the earth and gets people ready for rules that will apply all over the world.
Sustainable innovation happens faster when people in the supply chain work together. Suppliers of raw materials, converters, brands, and recyclers are working together more and more to make packaging systems that are better for both performance and processing at the end of their lives. This all-around approach knows that for something to really be sustainable, it needs system-level solutions instead of small improvements here and there.
Conclusion
When choosing the right flexible packaging, you have to think about how to protect the product, make it easy for customers, show off your brand, and be environmentally friendly. Stand up pouches are very flexible because the materials, functions, and designs can be changed to fit the needs of a wide range of industries. Knowing about the qualities of materials, how they can be made, and how they are bought lets you make smart choices that improve the success of your product while keeping costs low. As we move toward more eco-friendly materials and digital customisation, brands can find ways to stand out while still meeting customer needs. Working with experienced makers who offer full technical support, quality standards, and reliable production makes sure that packaging works the same way throughout the duration of a product and for repeat orders.
FAQ
1. What products are best suited for stand-up pouch packaging?
These flexible pouches excel with dry foods including snacks, coffee, nuts, and dried fruits, as well as powders like protein supplements and nutritional products. Pet treats and pet food represent growing applications, while non-food uses include cosmetics, household products, and industrial components. The key consideration involves matching barrier properties and functional features to specific product sensitivity regarding moisture, oxygen, and light exposure.
2. How do I determine the right material structure for my product?
Material selection depends on product characteristics and shelf-life requirements. Moisture-sensitive products require high barrier films like VMPET or foil laminates, while less sensitive products may utilize standard plastic laminates. Products containing oils benefit from specialized barrier constructions preventing fat migration. Consulting with packaging engineers who understand both material science and filling processes ensures optimal specification matching product needs with production capabilities.
3. What minimum order quantities should I expect?
MOQs typically range from 10,000 to 50,000 units for custom-printed pouches using rotogravure printing, reflecting setup costs and production efficiency thresholds. Digital printing enables smaller quantities starting around 1,000-5,000 units, though at higher per-unit pricing. Manufacturers balance customer flexibility against operational requirements, with volume commitments enabling more favorable pricing through improved material utilization and reduced setup frequency.
Partner with an Experienced Stand Up Pouch Manufacturer
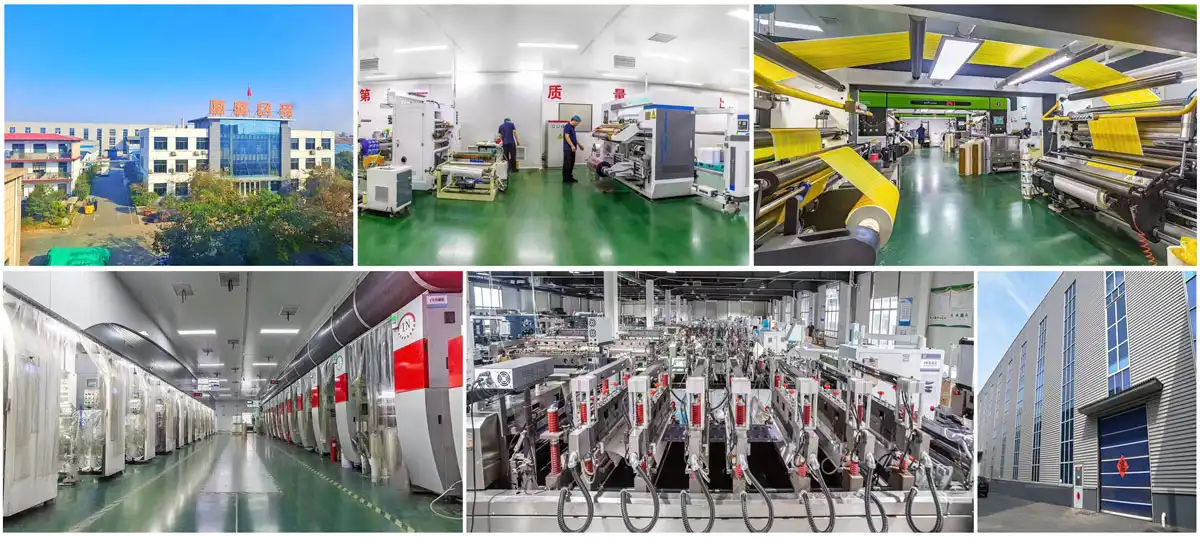
Guoshengli Packaging delivers reliable flexible packaging solutions backed by 25 years of manufacturing expertise serving food, pet food, and health supplement brands worldwide. Our production capabilities include 7 high-speed printing lines, 6 laminating machines, and 49 converting machines, ensuring consistent quality across repeat orders. We offer customizable stand up pouches with advanced VMPET construction providing superior barrier protection, premium spot UV printing for enhanced brand recognition, and fast delivery with lead times as quick as 7 days for urgent requirements. Certified under ISO 9001, BRC, and FDA standards, our food-grade packaging includes recyclable options supporting your sustainability commitments. Contact our technical team at sales@guoshengpacking.com to discuss material selection, design specifications, and production timelines tailored to your procurement requirements.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice (3rd Edition). CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Vol. 72, Issue 3, 2007.
3. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations (3rd Edition). Hanser Publications, 2016.
4. Yam, Kit L. The Wiley Encyclopedia of Packaging Technology (3rd Edition). Wiley-Interscience, 2009.
5. Coles, Richard and Mark Kirwan. Food and Beverage Packaging Technology (2nd Edition). Wiley-Blackwell, 2011.
6. Hotchkiss, Joseph H. "Food-Packaging Interactions Influencing Quality and Safety." Food Additives & Contaminants, Vol. 14, Issue 6-7, 1997.
Of course, Quad Seal Pouches & Bags are perfect for packing coffee. Their reinforced four-corner seal design provides great protection against moisture, oxygen, and light, which are three important things that lower the quality of coffee. The multi-layer laminate structure keeps smells and freshness for a much longer time than other types of packaging. Coffee roasters and wholesalers like the pouch's box-like sturdiness, which makes large goods from 250g to 1kg look better on shelves and increases the pouch's internal volume. With features that can be changed, like degassing valves and reusable zippers, these bags can meet the strict needs of speciality coffee brands and can be easily scaled up for high-volume production at a low cost.
Understanding Quad Seal Pouches and Their Design
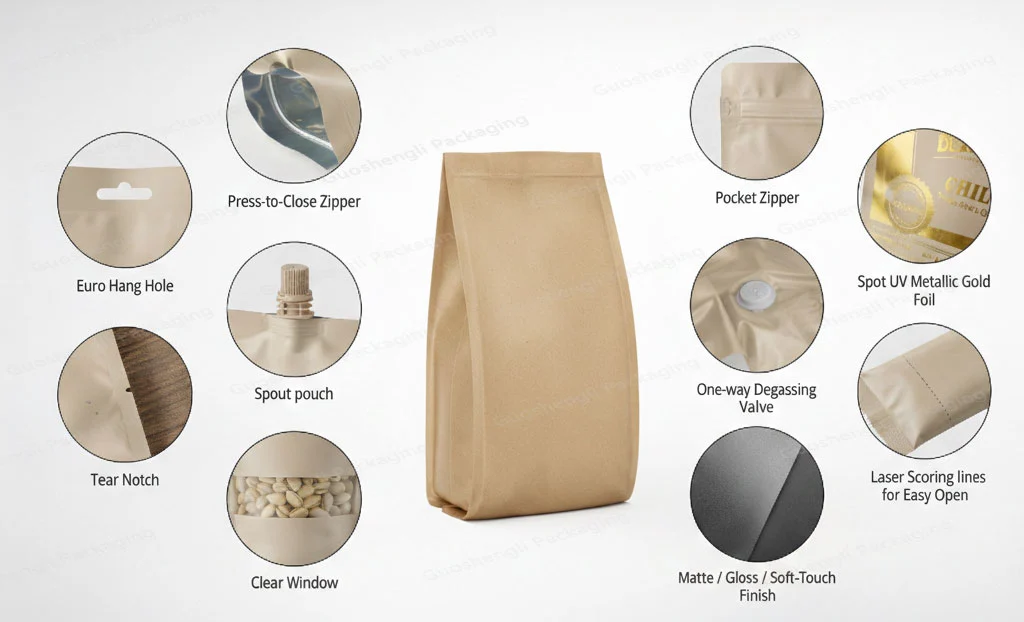
Quad seal bags are a big step forward in the making of bendable packaging. This style is different from regular three-side seal bags because it has four vertical seals at each corner. This makes a stronger rectangular structure that can stand on its own. This design gets rid of the center back seal, leaving five separate printable panels: the front, the back, two sides, and the bottom. This gives coffee companies that want a premium shelf presence the most branding opportunities.
Material Composition and Barrier Technology
Multi-layer laminates made of BOPP (biaxially orientated polypropylene), PET (polyethylene terephthalate), aluminium foil, and PE (polyethylene) are usually used to make Quad Seal Pouches and Bags. The oxygen transmission rate (OTR) and water vapour transmission rate (WVTR) goals are used to choose these materials. To keep volatile aromatic compounds from oxidising, coffee packaging needs OTR values that are very low, often below 1 cc/m²/day. In our manufacturing process, high-barrier metallised films and aluminium layers work together to meet these strict requirements. They also keep their flexibility and resistance to punctures throughout the supply chain.
The width of the laminate is usually between 120 and 180 microns, but this can change based on the fill weight and how it is handled. For heavier coffee goods, structures that are thicker are better because they have better burst power and keep the seal from breaking during shipping. Inner layers that are resistant to heat make sure that they can be used with hot-fill uses and keep the structure strong even when temperatures change, which is common in foreign shipping.
Size Variations and Structural Benefits
Coffee brands need packaging that can hold a range of product volumes while keeping quality high. There are a lot of different sizes and shapes of quad seal pouches, from small store packs of 250g to large wholesale forms of 1kg. Because the four-corner seal architecture is so stable vertically, filled pouches can keep their box-like shape even as the product settles during shipping. This "dead-fold" feature makes sure that the product looks the same on store shelves, which is important for differentiating brands in the coffee market.
When compared to flat-bottom or stand-up bags, the strengthened side seals can hold more weight. This structural benefit is especially useful when packing dense whole bean coffee or coarse ground coffee that puts a lot of pressure inside the package. Our engineering team figures out the best gap sizes to balance the internal volume efficiency with the external measurement. This helps coffee brands get the most out of their shipping containers while still making an appealing retail package.
Why Choose Quad Seal Pouches for Coffee Packaging?
Keeping three things in check in the environment is important for keeping coffee fresh: oxygen exposure, moisture infiltration, and light penetration. In all three areas, quad seal pouches do better than others thanks to their engineered barrier performance and structural design advantages that have a direct effect on how long a product lasts and how happy customers are with it.
Superior Barrier Protection
The many layers that make up Quad Seal Pouches & Bags make a winding path that makes gas and moisture barrier much slower. Metallised films offer great security at a lower cost, while aluminium foil layers make almost perfect shields. Because of this, coffee roasters can choose the right level of barriers based on the features of their products. For example, they can choose lower barriers for store settings with a lot of product movement and the highest levels of safety for foreign markets with long distribution cycles.
When coffee oils and aromatic compounds are exposed to oxygen, they oxidise. This makes the flavours go bad and the product less appealing to customers. Our high-barrier laminates keep the amount of air inside below critical levels for months, which protects the taste profile that makes expensive coffee brands stand out. Independent tests show that quad seal bags keep coffee 40–60% fresher longer than regular packing. This means that fewer products will be returned and the brand's image will improve.
Controlling moisture is just as important, especially for ground coffee that has a lot of surface area. Infiltration of humidity speeds up staling reactions and, in the worst cases, can help microbes grow. Because quad seal bags have a soldered seal and low WVTR laminate constructions, the humidity inside stays fixed no matter what the storage conditions are outside.
Enhanced Structural Integrity
Damage to transportation is a big cost factor in getting coffee to people. Quad seal pouches are very hard to cut, tear, or have their seal break while being handled. The placement of the corner seal spreads mechanical stress over four strengthened places instead of putting all of the force on one bottom seal. This engineering principle lowers the chance of package failures during automated filling and rough handling in distribution networks.
Coffee makers that ship abroad have to deal with a lot of problems, like having to load and unload their goods many times, dealing with changes in temperature, and having their goods squished together. In these situations, our bags keep their seals, which keeps product loss to a minimum and protects the brand's image across global supply lines. The strong construction also makes warehouse work easier because it doesn't need to be handled in the same way as more fragile packaging formats.
Comparison With Alternative Formats
While stand-up pouches and flat-bottom bags are useful for some things, quad seal pouches are the best way to package big coffee. Stand-up bags work best for smaller market sizes, but they might not be strong enough for heavy contents. Flat-bottom bags look great on shelves, but they usually cost more per unit because they are harder to make.
For coffee applications ranging from 500g to 2 kg, quad seal pouches are the best choice because they are both cost-effective and effective. The easier way of making them lowers the cost per unit while still giving them the same or better construction performance. Coffee distributors who are in charge of large production runs can really benefit from the reliable machinability of quad seal formats, which keep the same sizes that are important for the efficiency of automated filling lines.
Manufacturing and Customization Options for Coffee Businesses
Brands of coffee set themselves apart with packaging that talks about quality, location, and company values. Quad Seal Pouches and Bags allow for a lot of customisation while keeping production efficiency high, which is important for cost-effective scaling.
Production Process and Quality Control
Rotogravure printing with up to 11 colours is the first step in our manufacturing process. This lets us get images that look like photographs and match brand colours perfectly. The printing stage makes the visual base that tells people what the brand is on store shelves. High-resolution graphics stay clear across the large printed area of quad seal pouches. This lets coffee brands show images of the beans' location, boiling directions, and certification logos with great detail.
After printing, barrier layers are stuck together in a controlled temperature and pressure environment during the laminating process. This step decides how well the shield works and how strong it is. Our six laminating lines use solvent-less adhesive systems that get rid of any smells that might be left behind and are in line with FDA rules for food contact. Before the laminated film is turned into a pouch, it goes through quality checks that check for barrier properties, seal strength, and visual flaws.
Printed, laminated film is turned into finished bags in the conversion stage by cutting it precisely and closing it with heat. Our 49 changing machines can quickly switch between different pouch sizes, so they can handle both big production runs and smaller special orders. Each pouch is checked automatically to make sure the seal stays in place, the measurements are correct, and the valve is placed correctly when needed.
Custom Features for Coffee Applications
Standard pouches might not have all the functional features that coffee packaging needs. The most important part of newly roasted coffee is the degassing valve, which lets carbon dioxide leave but keeps oxygen from getting in. During pouch production, we put one-way valves in the right place so that they let out the most gas without weakening the structure. Choosing the right valve relies on the type of coffee being roasted and how long it will take to package. Dark roasts need more flow capacity because they release more strong gases than lighter roasts.
Resealable seals let you use the product for longer after opening it, which is a trait that people who buy bigger package sizes are increasingly asking for. Tin-tie closures are a cheap way to reseal traditional coffee bags, while press-to-close zipper systems are more convenient and reliable when opening and closing many times. To keep the barrier continuous across the closure mechanism, zip integration needs careful engineering. This is a skill we have honed over thousands of coffee packaging projects.
Handle features make it easier for customers to carry bigger packages. Adding die-cut handles or attached rope handles to bulk coffee pouches makes them easy to carry and works well for warehouse clubs and food service. These improvements need structural supports to keep them from tearing when they're loaded. We design these changes based on the expected fill weight and handling.
Lead Times and Minimum Order Quantities
When purchasing managers look at quad seal pouches, they need to know exactly when they can be made and how flexible the orders can be. Rotogravure printing production for standard bag shapes using current tools usually takes 15 to 20 days, which includes testing before production and quality approval stages. Lead times can be cut down to 7–10 days for rush orders that use digital printing technology. This helps with product launches and seasonal advertising needs.
Minimum order quantities depend on how complicated the customisation is and how the product is made. Rotogravure printing is most cost-effective when it's used in quantities greater than 50,000. This makes it perfect for well-known coffee brands whose demand is likely to stay steady. Digital printing makes short runs affordable starting at 5,000 units, so speciality roasters can try out new mixes or holiday products without having to keep a lot of stock on hand.
We keep our MOQ policies open because we know that new coffee brands need easy ways to get luxury packaging. Our team works closely with procurement managers to set up orders in a way that minimises costs and maximises cash flow. We often suggest phased production schedules that are in line with the growth paths of the market.
Procurement Considerations for Coffee Brands and Distributors
To find a trusted Quad Seal Pouches & Bags maker, you need to look at more than just price quotes. Coffee brands that want to stay in the market for a long time need package partners that can keep the quality of their work the same for return orders and help their businesses grow by being able to handle more orders and following all the rules.
Supplier Evaluation Criteria
Quality certificates give third-party proof of a company's ability to make things and its process control systems. Standardised quality management is shown by ISO 9001 certification, and major retailers require BRC (Brand Reputation through Compliance) certification to make sure that food safety rules are followed. FDA compliance makes sure that materials meet U.S. rules about food contact, and SGS testing results, which are based on independent lab analysis, back up promises about barrier performance.
We keep all of these certificates up to date because coffee makers can't afford packing problems that lower the quality of their products or cause problems with the law. Our testing methods check the strength of the seal, its ability to form a barrier, and the movement of materials at higher frequency than what is required by certification. This adds an extra safety cushion that safeguards the brand's image.
Production capacity affects how reliably deliveries happen and how much the business can grow. When coffee brands grow quickly, they need packaging suppliers that can handle more orders without affecting quality or lead times. Our building has 49 converting machines, 7 printing machines, and 6 laminating lines. This gives us a lot of capacity headroom to handle the changes in volume that happen in seasonal coffee markets.
Sustainable Sourcing Strategies
As coffee brands try to meet customer standards and keep their business sustainability promises, environmental duty plays a bigger role in their buying choices. Quad Seal Pouches and Bags can be made from structures made of a single reusable material or bio-based laminates that can be broken down and reused. However, choosing the right material means weighing the benefits and drawbacks of barrier performance and end-of-life choices.
Structures made of a single material, polyethylene, can be recycled in many places, so they are environmentally friendly without needing new collection systems. Compared to multi-material laminates, these structures don't provide as good of a barrier, but they are good for coffee products that need to be kept fresh for a shorter time or in controlled distribution environments.
Compostable laminates made of PLA (polylactic acid) and PBAT (polybutylene adipate terephthalate) offer different ways to get rid of waste, but they need industrial composting facilities that aren't always available. We give clear advice on these trade-offs, which helps coffee brands choose environmentally friendly packaging options that meet performance needs and work with the way the market is set up.
Our factory uses RTO (regenerative thermal oxidiser) exhaust treatment technology to get rid of volatile organic compounds from the production process. This shows that we care about the environment in more ways than just packaging materials. This all-around approach to sustainability works for coffee brands that want to work with suppliers who share their values and can back up their environmental claims to customers who are becoming more knowledgeable.
Building Long-Term Supplier Relationships
Suppliers that are reliable are different from those that aren't because they use the same packaging for all orders. As production goes on for months or years, colour matching, measurement accuracy, and the security of the seal must stay the same. Our process control systems keep a very close eye on all important parameters and keep samples that can be used as a guide to look at past changes when figuring out what might happen in the future.
Misunderstandings that slow down production and throw off shipping plans can be avoided by being clear when communicating. Our team has experience exporting, so they can handle technical talks, production reports, and transportation planning all in English. This gets rid of the language hurdles that often come up when buying from manufacturing areas. We understand that procurement managers need partners who can respond quickly, see problems coming, and talk to them before they get worse.
Before committing to large quantities of production, it is important to test samples. We don't give best-case scenarios that make people have high hopes. Instead, we give representative samples that show how well the process can work. Being honest builds trust and makes sure that production runs meet the agreed-upon requirements without any shocks.
Practical Use Cases and Industry Feedback
Quad Seal Pouches & Bags have been used by coffee brands in all market segments to solve specific packaging problems and take advantage of chances to differentiate their brands and improve operational efficiency.
Specialty Coffee Roasters
Small-batch speciality roasters need packaging that keeps the complex flavours and lets people know where they stand in the craft market. Quad seal pouches provide the necessary barrier protection and come in sizes that can be changed to fit both direct-to-consumer and café wholesale channels. The large printable area lets you tell in great detail about where the beans come from, how they are processed, and tasting notes that coffee lovers who know what they're doing will enjoy.
When a regional roaster switched from valve bags to quad seal pouches with built-in degassing valves, customers complained about bad coffee 35% less. The better barrier performance kept the food fresher for longer than the usual three weeks with their old packaging. This made it possible for them to sell more in stores that they couldn't reach before because of shelf-life restrictions.
Commercial Coffee Distributors
High-volume wholesalers that sell to restaurants and stores put stability, machine-ability, and low costs at the top of their list of priorities. These needs are met by quad seal pouches, which also have structural benefits that make them less likely to get damaged while being moved around in the building. The strengthened corner seals can handle the rough handling that happens a lot in distribution centers, so torn packages don't lose as much product.
When a national distributor that sells to institutions switched from flat-bottom bags to quad seal pouches, the efficiency of their packaging line went up by 18%. The uniform sizes and reliable seal area made automatic filling more accurate and cut down on downtime caused by misfeeds and jams that were a problem in their packing process before.
Private Label Coffee Brands
When stores start their own coffee programs, they need packaging that strikes a balance between keeping costs low and making the coffee look good. Quad seal bags look high-end and come at prices that support competitive pricing strategies for stores. Customisable printing lets brands stand out, and efficient production keeps unit costs in line with the economics of private label.
Limitations and Considerations
To be honest, you have to admit that quad seal pouches work better in some situations than others. When it comes to saving money, stand-up bags may be better for very small packages (less than 100g). Even though quad seal pouches offer similar barrier performance, the extra cost of rigid canisters or flat-bottom bags might be worth it for very high-end positioning.
For coffee makers that need packages in forms other than rectangles, there are other options available. Quad seal bags work best for structures that look like boxes; making methods for forms that aren't boxes need to be changed. During the initial consultations, we talk to coffee brands about these restrictions and make sure they choose packaging formats that meet both technical needs and market positioning strategies.
Conclusion
Quad Seal Pouches & Bags have many benefits for all types of coffee packagers, from small speciality roasters to large industrial sellers. The designed layer protection keeps the coffee fresh by being very resistant to air, moisture, and light. Structural stability stands up to handling during transport and gives the product a high-end look on the shelf that helps place the brand. Customisation needs can be met with manufacturing flexibility, which includes degassing valves and resealable closures, without slowing down production. Sustainable material choices take care of the earth while still meeting performance standards. When purchasing managers evaluate suppliers, they look at things like licenses, production ability, and making sure that quality is the same for each order. Because of these things, quad seal bags are a smart choice for coffee businesses that want to protect their product investments and support their market growth goals in global markets that are becoming more competitive.
FAQ
1. Can quad seal pouches integrate degassing valves for freshly roasted coffee?
Quad Seal Pouches & Bags accommodate one-way degassing valves positioned on the front or side panels. Valve integration occurs during pouch manufacturing, with placement optimized for gas release efficiency without compromising structural integrity. We recommend valve selection based on roast profile and expected outgassing rates—high-flow valves suit dark roasts producing aggressive carbon dioxide release, while standard valves serve light to medium roasts adequately.
2. What are typical production lead times for custom coffee pouches?
Rotogravure printing production requires 15-20 days, including proofing and quality approval stages. Digital printing alternatives reduce timelines to 7-10 days for urgent orders or smaller production runs. Lead times begin after artwork approval and deposit receipt, with shipping adding 4-5 days via air freight for international deliveries.
3. Are quad seal pouches recyclable or compostable?
Material selection determines end-of-life options. Mono-material polyethylene structures integrate with existing recycling infrastructure where available. Compostable bio-based laminates provide alternative disposal pathways requiring industrial composting facilities. Traditional multi-layer laminates with aluminum provide maximum barrier protection but currently lack widespread recycling options. We provide guidance matching packaging materials to sustainability objectives while maintaining required coffee protection.
Partner With a Trusted Quad Seal Pouches & Bags Manufacturer
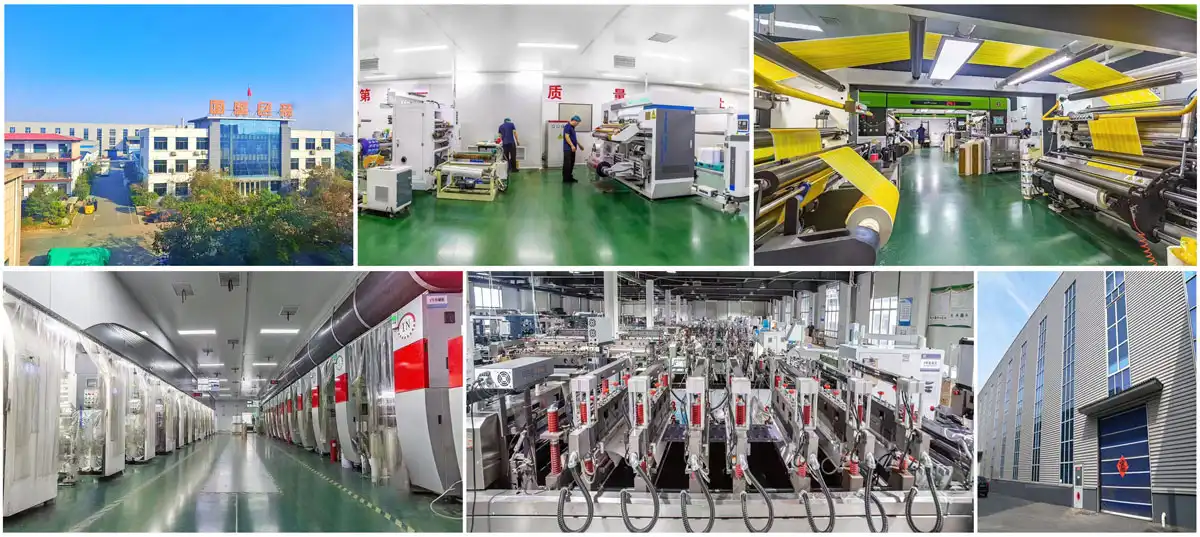
Guoshengli Packaging brings over 25 years of flexible packaging manufacturing expertise to coffee brands seeking reliable, high-performance packaging solutions. Our comprehensive capabilities span material engineering, rotogravure printing, lamination, and precision pouch converting—ensuring consistent quality across every production run. We maintain ISO 9001, BRC, FDA, and SGS certifications that validate our commitment to food-grade manufacturing standards your coffee brand depends on.
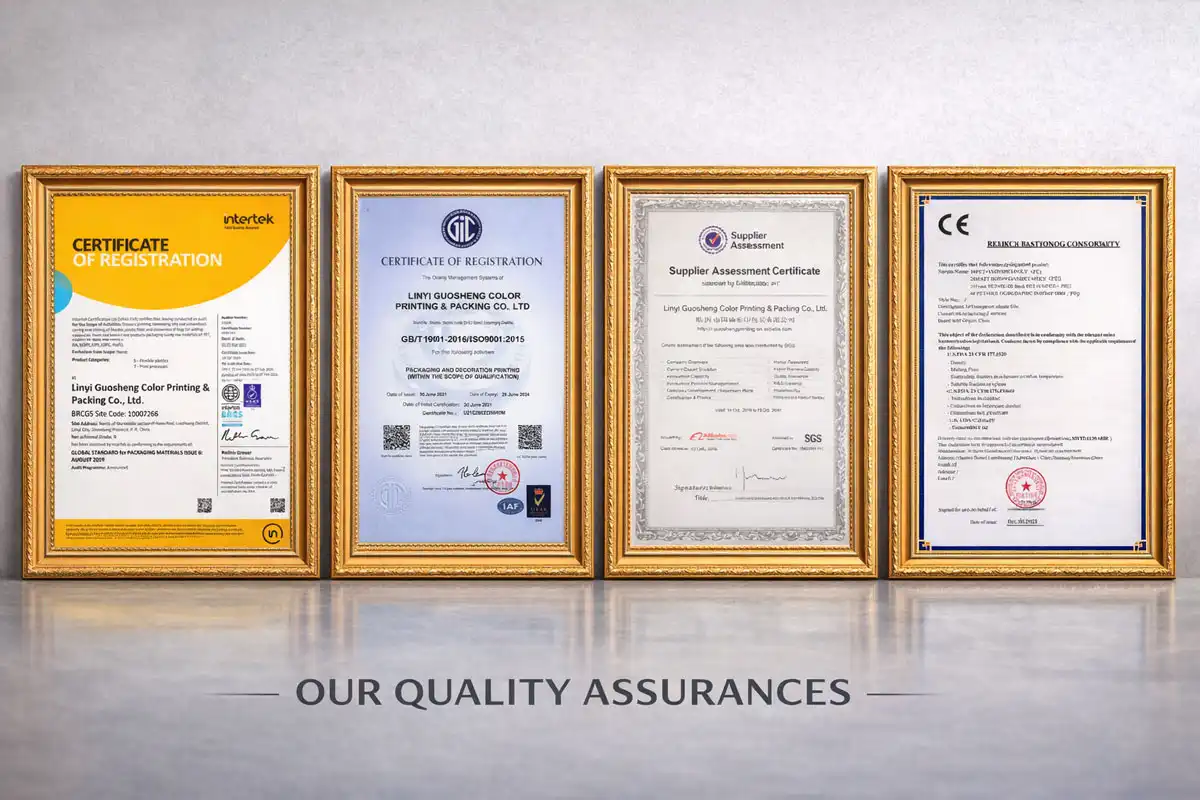
Coffee packaging represents more than product protection; it communicates your brand story and preserves the quality that defines your market position. We understand these dual requirements and deliver Quad Seal Pouches & Bags engineered specifically for coffee applications—from degassing valve integration to barrier optimization that extends shelf life. Our factory-direct supply model provides competitive pricing while maintaining the production flexibility that accommodates both established brands and emerging roasters.
Whether you are sourcing quad seal pouches as a supplier for an expanding product line or evaluating new packaging formats, our team provides expert guidance through material selection, structural engineering, and sustainable options aligned with your market objectives. Contact us at sales@guoshengpacking.com to request samples or discuss your specific coffee packaging requirements. We deliver packaging solutions you can depend on—order after order, shipment after shipment.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice, 3rd Edition. CRC Press, 2013.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science 72(3), 2007.
3. Santeramo, Fabio G. and Emilia Lamonaca. "Food Loss and Waste Policy: From Theory to Practice." Resources, Conservation and Recycling 182, 2022.
4. Yildirim, Selcuk et al. "Active Packaging Applications for Food." Comprehensive Reviews in Food Science and Food Safety 17(1), 2018.
5. Coles, Richard et al. Food and Beverage Packaging Technology, 2nd Edition. Wiley-Blackwell, 2011.
6. Ahvenainen, Raija. Novel Food Packaging Techniques. Woodhead Publishing, 2003.
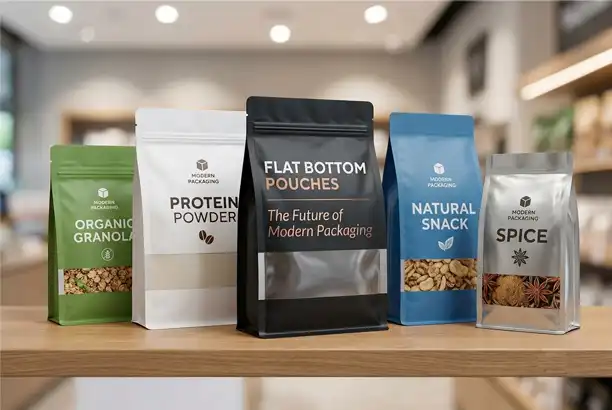
It shouldn't feel like a risk to find the right package partner. The 250g custom flat bottom pouch has become a popular choice for companies that want reliable packaging that looks good and works the same way every time. This detailed guide tells procurement managers, brand owners, and sellers everything they need to know to choose, customise, and get these useful pouches, from the types of materials and printing choices to how to evaluate suppliers and keep track of long-term costs. These basics will help you avoid making mistakes that cost a lot of money and create packing solutions that support long-term growth, whether you're packaging coffee, pet treats, or health products.
Understanding 250g Custom Flat Bottom Pouches
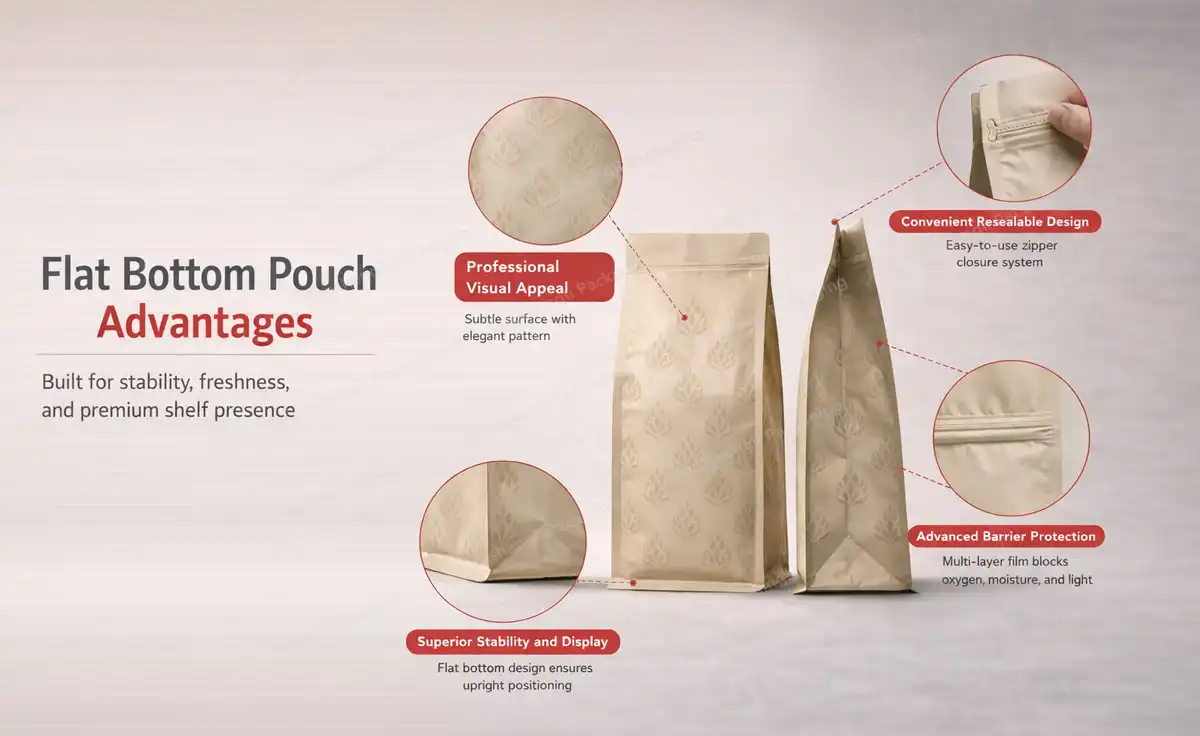
What Makes Flat Bottom Pouches Different
Because it is made of five panels, a flat bottom pouch is also called a box pouch. Traditional stand-up pouches only have side gussets, but flat bottom versions have a separate base piece that makes them very stable. Because of this difference in structure, your packaging can stand straight on shelves before it is even filled. The box-like shape makes the inside space as big as possible while keeping the overall size small. This makes the pouches perfect for stores where appearance is key to making a sale.
The physics behind this design includes gussets that are folded very exactly and a base that is completely flat and strong. The pouch stays in shape when it's full of 250 grams of something, like coffee beans, pet food, or protein powder. It doesn't lean or tip over. This security isn't just for looks; it comes from carefully choosing the materials and making sure the product is made correctly, which means that the filling line isn't interrupted as often and the product works the same way on different orders.
Material Compositions and Performance Characteristics
Material selection directly impacts shelf life, product security, and environmental effect. The multi-layer laminate structures used in most 250g custom flat bottom pouches are made of PET for strength, aluminium foil or metallized films for barrier protection, and PE for heat sealing. These mixtures give better protection against wetness, air, and light, which are important for keeping food fresh longer and stopping it from going bad.
Global procurement teams are giving more weight to sustainable options along with performance options. When designed correctly, structures made of a single material that can be recycled, films made of recyclable PLA, and high-barrier paper laminates are all good for the earth. But sustainability is only important if the shelf life needs are met. Working with experienced makers makes sure that the materials used are both environmentally friendly and protect the product in the real world, so that it doesn't break down too soon and cause loss and customer complaints.
Capacity and Dimensional Considerations
As a practical middle ground, the 250-gram capacity works well for many uses. It's big enough to give customers value while still being small enough to ship and store. Usually, they are between 140mm and 180mm tall and 100mm to 140mm wide, but special sizes can be made to fit the needs of certain brands and filling equipment.
Knowing the density of your product and the level of filling you want can help you figure out the best pouch dimensions. Overfilling makes it hard to finish and doesn't look good, while underfilling makes it look bad and loses material. Packaging partners with a lot of experience can give you advice on the right dimensions based on the features of your product. This makes sure that the pouches work well during automated filling processes and look good on store shelves.
Comparing 250g Flat Bottom Pouches with Other Packaging Types
Structural Advantages Over Stand-Up Pouches
Standard stand-up pouches are stable thanks to bottom gussets, but they often lean or need extra support when there isn't much room on the shelf. With its dedicated base panel, the flat bottom pouch gets rid of this problem, making a structure that looks like rigid boxes and can stand on its own. In busy stores, where every millimetre of shelf space counts, this difference becomes important.
The five-panel form also has more space for printing than the three-panel stand-up styles. There are branding possibilities on the front, back, two side panels, and bottom. These areas can hold a lot of information about the product and have images that catch people's eyes from different viewing points. This bigger space is worth the small extra cost over basic forms for high-end goods where the package communicates quality.
Side Gusset and Quad Seal Comparisons
Side gusset pouches are great for saving space but don't have the premium shelf presence of flat bottom designs. They work well for big pouches and uses that need to save money and don't need to be very stable. There are some structural similarities between quad seal pouches and flat bottom styles. However, quad seal pouches don't usually look like boxes and may not stand as strongly when they're only partly full.
Your priorities will help you decide which of these formats to use. Coffee brands often choose flat-bottom pouches because they look more expensive and keep smells out. Pet food companies might choose side flap designs because they can make more food at a lower cost. Knowing these trade-offs helps make sure that the product you choose fits with how you want to place your brand and your business's needs, instead of just following general suggestions.
Resealable and Valve Options
Structure is not the only thing that is functional. Zippers that can be resealed let people keep food fresh for more than one use, which is important for coffee, snacks, and pet treats. 250g custom flat bottom pouches can have different zipper styles, such as standard 'press-to-close' options or sliders that make the user experience better and support the premium positioning.
There are specific uses for degassing valves, like in coffee packaging where freshly roasted beans give off CO2. These one-way valves keep the package from expanding and keep oxygen from getting in from the outside, which keeps the smell inside and extends the shelf life. To choose the right functional features, you need to know about the problems your product solves and how customers usually use it, not just copy the packaging of your competitors.
Cost Dynamics and MOQ Considerations
Prices depend on the type of material, size, complexity of the print, and number of orders. Due to more steps and materials used in production, flat bottom pouches usually cost 15–30% more than basic stand-up versions. But this extra cost usually pays off in a measured way, like less wasted product, fewer stops in the filling line, and a better reputation for the brand, which supports the extra cost.
Another important thing to think about is the minimum order quantity. Digital printing can do runs as small as 5,000 to 10,000 pouches, and the lead time is only 7 to 10 days. This makes it a good way to test the market and launch new products. Rotogravure printing needs more pouches—usually at least 50,000—but it produces more consistent colours and costs less per unit for well-known pouches. Knowing how these things work helps you find the right balance between initial investment and long-term cost savings.
Key Benefits and Use Cases of 250g Custom Flat Bottom Pouches
Enhanced Branding and Shelf Impact
Packaging is like a quiet seller, and flat bottom pouches are great at getting people's attention in busy stores. The stable, straight position makes sure that your brand's message stays visible and doesn't get lost among rivals who are leaning or falling. There is plenty of room on the four vertical panels for interesting graphics, product stories, and regulatory information without making the page look crowded.
Working with companies that can do up to 11 colours of rotogravure printing lets you use complex designs that make your brand stand out. Matte and glossy finishes, soft-touch coatings, and metallic effects all make things feel good to the touch, which tells customers about the quality of the product before they even open the box. When your goods are up against well-known names with big marketing funds, these things matter.
Industry-Specific Applications and Performance
To keep the flavour and smell of coffee, the packing needs to be very good at blocking air and water. The multi-layer design of custom flat bottom pouches, along with degassing valves and reusable locks, meets these needs and gives the coffee a high-end look that supports its higher price. The 250-gram size is great for how people usually use a product at home.
Brands of pet food and treats benefit from the structural stability that keeps the package's integrity during shipping and stops spills. The easy-tear notch makes things easier for customers, and the resealable closures keep food fresh between feedings. Food-grade certification under FDA and BRC standards makes sure that pets are safe, which is one of the main reasons pet owners decide to buy something.
Protein powders, supplements, and superfood ingredients are all examples of health and wellness products that need to be able to reliably keep moisture out and keep contaminants out. Engineered flat bottom pouches have protective properties that make them last longer on the shelf. They also support clean-label branding through clear windows or simple patterns that show quality and purity.
Sustainability and Environmental Responsibility
Sustainability promises made by businesses are having a bigger impact on packaging choices. Many companies now make one-piece materials, such as 250g custom flat bottom pouch, that can be recycle-ready and keep their blocking properties thanks to new film technologies. These buildings support the ideas of a circular economy because they allow materials to be reused instead of going to landfills.
Environmental duty goes beyond the materials we choose and includes how they are made. The carbon footprint of your package supply chain is smaller when factories use Regenerative Thermal Oxidizer (RTO) technology to cut down on emissions during production. Asking for proof of environmental certifications and manufacturing practices shows that you are doing your research and helps your customers believe the sustainability messages you send them.
Operational Efficiency and Filling Line Compatibility
During production, problems with packaging that doesn't work consistently cost a lot of money. Accurate measurements make sure that custom flat bottom pouches go through automated filling equipment without getting stuck or out of place. When the seal is strong enough, it stops leaks during filling, sealing, and transport, but it's still easy for customers to open.
Working with manufacturers who have strong quality systems (backed by ISO 9001 certification and in-process inspection protocols) lowers the chance that packaging defects will stop production. Consistency from batch to batch is more important than having perfect samples, because inconsistent packaging causes ongoing operational problems that eat away at the cost savings that come from competitive pricing.
Custom Design and Printing Solutions for 250g Flat Bottom Pouches
Advanced Printing Technologies and Quality Standards
Digital printing lets you make small amounts of pouches quickly, which makes it perfect for limited editions, seasonal pouches, and testing the market. The process is flexible and produces good quality, but the colour may not be the same across large volumes. Lead times of 7 to 10 days allow for quick product launches and market plans that adapt to changing conditions.
Rotogravure printing is the best way to make sure that the colours of well-known products are exactly the same in every production run. The engraved cylinder process gives you a lot of detail and consistency. Some manufacturers even let you use up to 11 colours, which can handle complex gradients and photos. Even though there are higher setup costs and minimum order quantities, the cost savings per unit and consistent quality make the investment worth it for high-volume goods.
Design Principles for B2B Market Success
Good package design strikes a balance between how it looks and what it does. Colours are used in a smart way to draw attention to important brand messages and product benefits. Typography must be readable in a range of lighting conditions and viewing distances. This is to make sure that legal information is included while still keeping the purity of the design.
More and more, security measures are important to fight fraud and build user trust. QR codes make it possible to track goods through the supply chain and engage customers with digital content. Tamper-evident stickers and hologram elements stop people from copying them without permission. These features help protect the value of the brand and support premium placement, especially in health and fitness categories where fake goods are common.
Sealing Methods and Closure Technologies
For flat-bottom pouches, heat sealing is still the most common way. The PE layer in laminate designs is used to make effective airtight covers. Temperature, pressure, and dwell time must be optimised for your specific material structure and filling equipment in order to get the best sealing results. By offering technical support during line trials, manufacturers can avoid problems that could cost a lot of money later on in production.
Resealable zip locks make things more complicated, but they give customers a lot of value. Press-to-close zippers are simple and cheap, but slider zippers offer better functionality and should be more expensive because of it. The zipper needs to fit properly into the structure of the pouch so that the barrier properties and seal integrity stay the same after many opening and closing cycles.
How to Procure Your 250g Custom Flat Bottom Pouches Efficiently
Identifying Reliable Suppliers and Manufacturing Partners
One of the most important choices you can make about your packing plan is which supplier to use. Manufacturers who have been making flexible packaging for 25 years or more have seen material changes, regulatory changes, and technological advances. This institutional knowledge helps you spot problems early and solve them before they slow down production.
Certifications are an objective way to prove that quality systems and food safety practices work. ISO 9001 shows a mindset of process control and constant growth. BRC approval is all about making sure that food packaging is safe and that quality control is done right. FDA compliance makes sure that products meet US market rules for food interactions. Testing results from SGS are an independent way to check that barrier qualities and material safety claims are true.
Understanding MOQ and Lead Time Dynamics
Minimum order quantities have a direct effect on planning your inventory and your cash flow. Digital printing lets you print fewer pouches at a time, which is good for new products, seasonal changes, and niche markets, such as 250g custom flat bottom pouch. Rotogravure printing needs more materials, but it's more cost-effective for well-known goods that will always be in demand. For example, some manufacturers use a combination of rotogravure and digital printing to make bigger batches while still keeping smaller runs.
Lead times depend on the type of printing, the supply of materials, and the amount that can be made. Digital printing is usually done 7–10 days after the artwork is approved. Rotogravure takes 15 to 20 days because the barrel has to be prepared and set up. By planning procurement cycles around these dates, you can avoid rush orders that cost more and increase the chance of making mistakes.
Sample Approval Workflows and Quality Validation
Don't go ahead with full production runs before getting sample approval. Samples in the real world show how fabrics feel, how prints look in different lighting, and how well pouches work during filling tests. By using samples on your real filling equipment, you can find fit problems before they become production problems.
Along with samples, you should ask for material specifications and data on how well the barrier works. Tests done by a separate lab back up the claimed oxygen transmission rates, moisture vapour transmission rates, and seal strength values. This paperwork backs up shelf life studies and regulatory submissions and gives people a way to get their money back if production batches don't meet the agreed-upon standards.
Negotiating Pricing and Volume Discounts
Knowing how costs are structured helps you negotiate more effectively. Costs are mostly affected by the cost of materials, the difficulty of printing, and the number of orders. Asking for detailed quotes that break down the prices of materials, printing, and production can help you find ways to save money without lowering the quality.
When you make a volume promise, you can get deals that are worth it, but don't make too many commitments because you think sales will be good. Setting up framework agreements with graduated pricing tiers lets you plan your costs while still allowing for flexibility. Some manufacturers have inventory management tools that let you split up production into multiple packages. This lowers your need for working capital and helps you get better prices on larger orders.
Conclusion
When choosing the right 250g custom flat bottom pouches, you need to think about a lot of things, such as the structural performance, barrier qualities, branding possibilities, environmental goals, and the total cost of ownership. The 250-gram size is flexible and can be used for a wide range of things, including food, pet care, and health and fitness. It also has the right amount of space for customers and businesses to work efficiently. For your business to be successful, you need to work with experienced makers who know how to meet international quality standards, keep their production skills stable, and help your business through times of growth and changes in the market. This guide gives you the information you need to make smart choices that lower risk, keep costs down, and support the long-term success of your brand.
FAQ
1. What lead times should I expect for 250g custom flat bottom pouches?
Lead times vary by printing method and order volume. Digital printing typically requires 7-10 days after artwork approval, making it suitable for product launches and small batch needs. Rotogravure printing takes 15-20 days due to cylinder preparation but offers superior color consistency for established products. Factor in additional time for sample approval, material testing, and shipping when planning procurement cycles. Experienced manufacturers provide detailed production schedules that help coordinate packaging arrival with your filling operations.
2. Are biodegradable materials available for flat bottom pouches?
Yes, several sustainable options exist. Compostable structures utilizing PLA and PBAT films offer end-of-life benefits when properly disposed of through industrial composting facilities. Recyclable mono-material designs maintain functionality while supporting circular economy principles. Paper-based laminates with minimal plastic content appeal to brands prioritizing natural materials. However, sustainable materials must still meet shelf life requirements, so barrier testing and shelf life studies remain essential. Discuss your sustainability goals with manufacturers who can recommend validated solutions rather than unproven materials that risk product failures.
3. How do I choose between resealable and non-resealable options?
This decision depends on your product characteristics and consumer usage patterns. Resealable zippers benefit products consumed over multiple occasions—coffee, snacks, pet treats—by maintaining freshness and convenience. The feature justifies premium pricing for quality-focused consumers. Non-resealable designs reduce costs and complexity for single-use products or bulk pouches transferred to storage containers immediately after opening. Consider conducting consumer research to validate whether resealability influences purchase decisions in your category before adding the cost premium.
Partner with Guoshengli Packaging for Your Custom Flat Bottom Pouch Needs
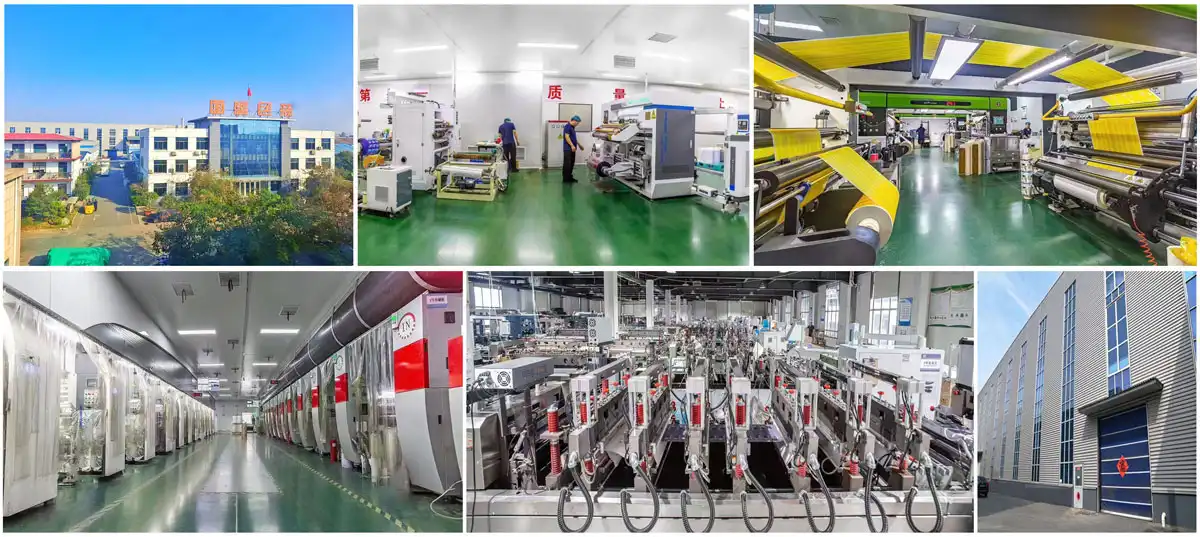
Guoshengli Packaging brings 25 years of flexible packaging expertise to your procurement strategy, specializing in 250g custom flat bottom pouch manufacturing for global markets. Our ISO 9001, BRC, and FDA-certified facility operates 7 printing machines, 6 laminating lines, and 49 converting machines, ensuring production capacity that meets demanding delivery schedules without compromising quality. We serve food brands, pet food manufacturers, health supplement companies, and beverage producers across North America, Europe, and Asia-Pacific with solutions engineered for automated filling lines and consistent repeat order performance. Choose from rotogravure printing up to 11 colors or digital printing for shorter runs, with lead times as fast as 7-10 days. Our technical team supports material selection, barrier optimization, and sustainable packaging development aligned with your corporate responsibility goals. Contact our specialists at sales@guoshengpacking.com to discuss your requirements, request samples, or receive detailed quotations. As an established 250g custom flat bottom pouch supplier, we reduce procurement risk through proven manufacturing capabilities and transparent communication that supports long-term partnerships.
References
1. Robertson, G.L. (2024). Food Packaging: Principles and Practice (5th ed.). CRC Press.
2. Marsh, K. & Bugusu, B. (2023). "Flexible Packaging Materials and Sustainability in Food Systems." Journal of Food Science and Technology, 60(4), 1245-1258.
3. Soroka, W. (2025). Fundamentals of Packaging Technology (7th ed.). Institute of Packaging Professionals.
4. Singh, P., Wani, A.A., & Langowski, H.C. (2024). "Barrier Properties and Material Selection in Flexible Packaging for Extended Shelf Life." Packaging Technology and Science, 37(2), 89-104.
5. Emblem, A. & Emblem, H. (2023). Packaging Technology: Fundamentals, Materials and Processes (3rd ed.). Woodhead Publishing.
6. Yam, K.L. (2024). The Wiley Encyclopedia of Packaging Technology (4th ed.). John Wiley & Sons.
For food packaging, the best high barrier film rollstock options include multi-layer structures with EVOH (Ethylene Vinyl Alcohol) coatings for better oxygen protection, metallised films for resistance to moisture and light, and PVDC (Polyvinylidene Chloride) coatings for balanced barrier performance. Newer choices have structures made of a single material that can be recycled and coated with aluminium oxide or silicon oxide. These offer good protection while also meeting the needs for sustainability. The choice is based on how sensitive the product is, how long it needs to last, how well it works with other machines, and the rules that must be followed.
Understanding High Barrier Film Rollstock for Food Packaging
In order to keep food safe while it is being stored and shipped, barrier films are necessary. These special packaging materials make a shield around the product that keeps outside elements from hurting its quality.
What Makes a Film "High Barrier"?
The ability of a film to stop the passage of oxygen, moisture, light, and smells is called its barrier qualities. Standard packaging films let a lot of air through, which can cause oxidation, moisture absorption, or flavour loss. High barrier films use modern polymer science and layered building to cut these transfer rates by a huge amount. These structures are made of EVOH layers that block oxygen, aluminium foil that completely blocks light and gas, and special coatings that make the structures safer without making them too thick.
Common Barrier Materials and Their Functions
For each application, a different barrier approach is needed. EVOH is very resistant to oxygen, which makes it perfect for things like coffee, nuts, and cured meats that tend to go bad quickly. Metallised films have a thin layer of aluminium placed on top of polymer bases. They are better at blocking light and moisture than foil laminates and are less expensive. PVDC coatings provide appropriate shields against air and moisture, but they are limited in some areas because of environmental issues. Modern inventions include vacuum-deposited aluminium oxide and silicon oxide coatings that make barriers that are see-through, perfect for products where visibility is important.
Knowing about these different types of materials helps procurement teams match the packaging's abilities with the needs of protecting the product. A snack brand that needs to keep out moisture needs different structures than a coffee maker that needs to keep air out.
Multilayer Construction: The Key to Performance
To make barrier films, most people use coextrusion or layering to put together several polymer layers. Each layer does a specific job: the outer layers make it possible to print and give the seal strength, the middle layers work as a barrier, and the inner layers make sure that food contact is safe and that the heat seal works with the material. By using this designed method, makers can improve performance while keeping costs low. A common construction might have polyester for strength, EVOH for an air shield, and polyethylene for sealing. Each layer works to make the film work better as a whole.
Comparing High Barrier Film Rollstock Options: Metrics Procurement Teams Must Know
To choose the right protection films, you need to know how to measure the performance of high barrier film rollstock. To make smart choices, you need to know about testing standards and what numbers for product shelf life really mean.
Oxygen Transmission Rate (OTR) and Its Impact
OTR finds out how much oxygen moves through a certain film area in 24 hours. This is usually shown as cc/m²/day. Products that are easily damaged by oxygen need OTR values that are very low, often less than 1.0 cc/m²/day. For example, coffee gives off carbon dioxide but is still very vulnerable to damage from oxygen. If the film doesn't keep oxygen out well enough, the flavours will go bad within weeks. ASTM D3985 standards are used for testing, so data from different suppliers is comparable. When looking over technical data sheets, make sure you check the test settings, such as the temperature and relative humidity, because these have a big impact on the results.
Moisture Vapor Transmission Rate (MVTR) Considerations
In certain situations, MVTR measures water vapour penetration in grams per square metre per day. Low MVTR is needed for powdered supplements, pet treats, and dried fruits to keep them from clumping, microbes from growing, and the texture from breaking down. MVTR levels for standard films can be between 5 and 10 g/m²/day, while levels for barrier structures are less than 1 g/m²/day. Because of the link between differences in temperature and transfer rates, packaging needs to take into account how it will be stored and shipped. Products that are going to wet places need better moisture shields than products that will stay in climate-controlled places.
Mechanical Properties That Affect Production Efficiency
How well a barrier works doesn't matter if films can't be counted on to run smoothly on packing lines. Tensile strength, extension, resistance to punctures, and the spread of tears all affect how well a production goes. Form-fill-seal machines need films with certain coefficients of friction. If the coefficient of friction is too high, the film won't run properly, and if it's too low, it will slip. Seal strength testing (ASTM F88) makes sure that seams can handle distribution stresses without breaking. We've seen cases where packaging failed not because the barrier wasn't strong enough, but because the seal wasn't strong enough or wasn't resistant to punctures during handling.
Metallized vs. Transparent Barrier Films
Metallised structures are great barriers that don't cost too much. The aluminium shell fully stops light, which keeps light-sensitive products from oxidising. However, traditional multi-material metallized laminates are difficult to recycle. Transparent barrier sheets with EVOH or oxide coats keep the product visible, help the brand stand out, and are becoming more and more recyclable. The choice will depend on whether blocking light and saving money are more important than being clear and protecting the environment. A lot of coffee brands like metal structures, while high-end snack lines choose clear films to show off the quality of their products.
Environmental and Cost Trade-offs
Traditional barrier films often use materials that don't work well together, which makes recycling harder. Structures that mix polyester, aluminium, and plastic are hard to separate when they need to be recycled. Newer methods that only use one material have frames made of plastic, which keeps them recyclable while adding protective coats. Most of the time, these solutions cost 15 to 25 percent more at first, but they build brand value through claims of sustainability and agreement with the ideals of the circular economy. Calculations of return on investment need to take into account more than just the costs of the goods themselves. They also need to take into account possible market access, changes in consumer tastes, and the direction of regulations.
How to Choose the Best High Barrier Film Rollstock for Your Food Packaging Needs
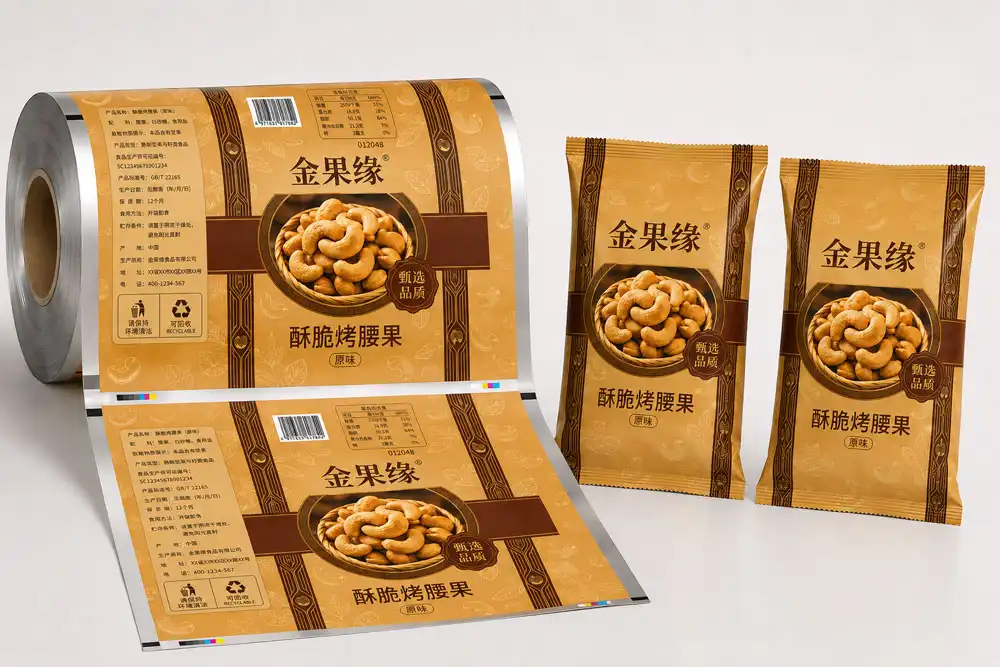
To make a choice, you have to match the properties of high barrier film rollstock to the needs of the application. A structured method keeps expensive mistakes from happening when the needs of the goods don't match the capabilities of the packaging.
Assessing Product Sensitivity and Shelf Life Targets
First, figure out what makes your offering worse. When foods are exposed to air, they quickly turn rancid. Powders that are hygroscopic soak up water and cake. Permeable packaging lets volatile compounds escape from aromatic goods. Testing shelf life under sped-up settings shows what causes quality to go down. If oxygen causes degradation, low OTR should be your top priority. If wetness is the main danger, pay attention to the MVTR specs. Products that are sensitive to more than one thing need complete barrier solutions that block all pathways at the same time.
Matching Films to Packaging Machinery
Packaging equipment compatibility is often forgotten until there are problems with production. Different types of machines—vertical form-fill-seal machines, horizontal flow wraps, and thermoforming lines—need different kinds of films. Film choice is affected by the speed of the machine, the temperature of the sealing jaw, the dwell time, and the tension control. We suggest giving possible providers full information about the tools you need, such as the brand, model, normal speeds, and any known quirks. Films that work great on one type of machine might not work at all on another because the seal mechanisms or handling characteristics are different.
Supplier Reliability and Technical Support
Long-term success in packaging depends on what the supplier can do beyond what is required by the product. Check to see if your sources can increase their production as your business grows. Use batch-to-batch performance data to check the uniformity of the quality. Check the documentation for food contact compliance and certifications like ISO 9001 and BRC. When dealing with production problems or making systems work better, technical help is very important. Suppliers should help with choosing materials, fixing problems, and making designs based on the problems that come up in a particular case. We value relationships where providers take the time to learn about how our customers run their businesses instead of just meeting orders.
Regulatory Compliance Across Markets
Food contact packaging has to follow strict rules that vary from place to place. In the US, FDA rules, EU Regulation 10/2011 in Europe, and extra rules in places like Australia and Japan all have specific requirements that must be met. Migration testing makes sure that no dangerous chemicals move from the packaging to the food. Compliance statements, migration test results, and material composition declarations should all be in the supplier documentation. To avoid having to pay more money to make new films, products that are going to be sold in more than one market need films that meet the strictest standards.
Volume Commitments and Lead Time Management
There are usually minimum order quantities for making barrier film that depend on the printing cylinders, lamination runs, and slitting configurations. Structures that are made to order may need pledges of several thousand kilograms. Lead times range from 7 to 10 days for digitally printed products to 15 to 20 days for larger quantities printed by rotogravure. Keeping a safety stock helps us deal with changes in the supply chain, especially when we buy from other countries. By building relationships that let you buy in a variety of ways, including both standard orders and special runs, you can keep your business running smoothly without having to pay too much for supplies.
Leading High Barrier Film Rollstock Products and Suppliers for Food Packaging
There are both large, well-known multinational companies and small, specialised manufacturers in the global packaging industry. Each has its own specialities. Knowing what the competitors are doing helps buying teams find good partners.
Global Industry Leaders and Their Offerings
International giants like Amcor, Berry Global, and Sealed Air keep huge inventories of high barrier film rollstock products that can be used in a wide range of situations. These companies have a lot of technical resources, make things all over the world, and spend a lot of money on research and development that leads to new materials. Because they are so big, they can keep up a steady supply even when the market is down. However, smaller names may not be able to meet the minimum order quantities, and standard production methods can make it hard to offer customisation choices.
Regional experts can often be more flexible and provide faster service. When manufacturers focus on certain market segments, they learn a lot about how to use their products. When we work with partners who know a lot about things like pet food safety, coffee packaging, and supplement protection, we can make better suggestions and avoid having to try things and see what works and what doesn't.
Material Innovations Advancing Performance
New developments in barrier technology have improved both performance and long-term viability. Mono-material polyethylene structures with oxide coatings can still be recycled and provide barrier properties that were previously only possible with mixed-material laminates. These films have OTR values below 5 cc/m³/day thanks to thin, clear layers that are put on using plasma-enhanced chemical vapour deposition. Even though they aren't as good as EVOH at extreme barriers, they work well enough for many uses and make end-of-life processing easier.
Compostable sheets made from PLA and PBAT plastics are appealing to brands that want to be seen as zero-waste. These materials break down in industrial composting facilities, but they aren't as good at blocking out light and heat as regular polymers. Careful application matching makes sure that recyclable films can be used on goods where simple barriers are enough and there is the right infrastructure for dumping. We advise against using recyclable packaging for goods that need to stay fresh for a long time or that are sold through outlets that don't allow composting.
Real-World Performance Validation
Case studies show how choosing the right barriers can help solve real-world problems. A company that makes pet treats noticed that their products were getting soft in the summer and switched from standard film to a structure that offered better MVTR protection. The shelf life was increased from 6 to 12 months, which cut down on waste and made distribution more flexible. A coffee roaster used metallised film with built-in degassing valve, which let the coffee be packaged right away after roasting while keeping air out. Customers were happier when they got fresher goods that still had their original smells.
These examples show that problems with packaging don't show up in samples, but when production goes up, changes with the seasons happen, and products are sent to more places. If you choose providers with a history of doing a good job, you're less likely to find problems after spending in packing equipment and supplies.
Environmental and Regulatory Considerations for High Barrier Film Rollstock
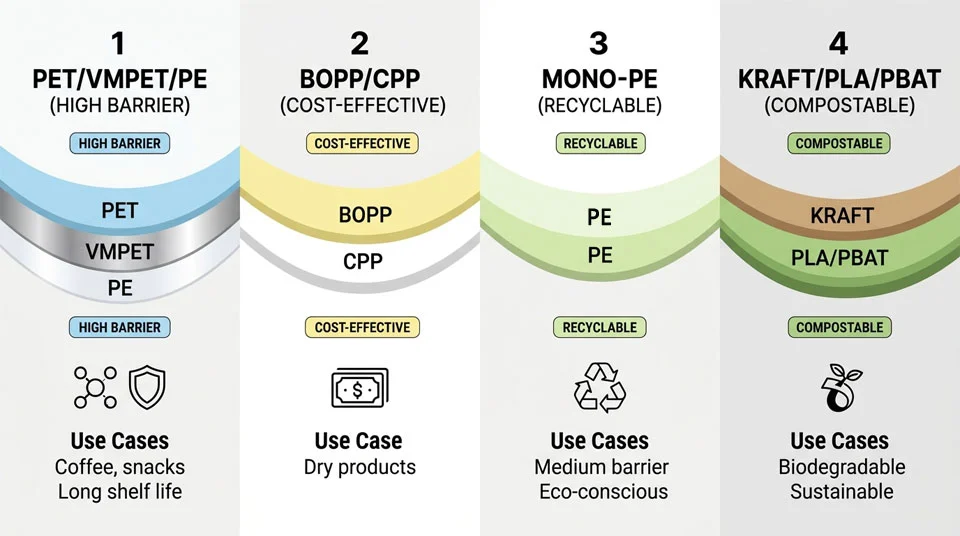
Today's packaging strategies are shaped by sustainability and compliance. When making procurement choices, people have to find a balance between performance standards, environmental duty, and legal duties.
Recycling Challenges and Emerging Solutions
Traditional barrier laminates made of plastics that don't mix well together don't allow recycling through mechanical means. Structures made of aluminium foil can block everything, but they can't be recycled with polyethylene or polyester. Most areas' waste management systems don't have the tools to separate complicated layered films, so they end up in landfills or are burnt.
As a response, the industry is coming up with recyclable alternatives that still meet the necessary safety standards. Structures made of polyethylene that are constructed entirely of polyethylene can be processed through established routes for reusing low-density polyethylene. When brands use these materials, they support the ideas behind the circular economy and meet customer expectations for caring for the environment. But making the switch means making sure that the new structures give the same shelf life in real-world distribution conditions. This takes a lot of testing and time.
Navigating FDA and EU Food Contact Regulations
Understanding the relevant frameworks is the first step to regulatory compliance. In the US, FDA rules focus on certain substances that are allowed to come into contact with food. Manufacturers must show that these substances are safe through migration testing and toxicological data. EU Regulation 10/2011 sets up lists of chemicals that are allowed to be used, along with specific limits on migration and makeup rules. Sometimes, extra partner state rules put even more limits on what can be done.
Suppliers should give a lot of paperwork, like declarations of compliance, migration test results done using standard methods, and lists of all the substances they offer. We suggest that you look over this paperwork during the seller approval process instead of thinking that it is correct. If there isn't enough governmental backing, there are risks of liability and possible barriers to market entry if officials question the safety of the material.
Balancing Performance and Sustainability Goals
There aren't any zero-compromise solutions yet because there are trade-offs between the best barrier performance and the best recycling ability. First, decision frameworks should put protecting the product first, and then they should try to make the environment as good as it can be while still meeting performance goals. If a nutrient powder needs to be protected from high wetness, it can't give up barrier integrity to make promises about being recyclable if the product breaks down. But a dry snack that can handle some hurdles can use recycled materials without losing any of its quality.
Being open and honest with customers about these trade-offs builds trust. Brands that say the choices they make about packaging put food safety first and reduce waste by making products last longer show that they are serious about sustainability and not just greenwashing. Life cycle studies, which measure the total environmental impact and include preventing food waste, often show that good packaging lowers the overall footprint, even when there are problems at the end of the product's life.
Conclusion
To choose the high barrier film rollstocks, you need to know about material science, performance measures, gear fit, and government rules. Depending on the needs of the application, multi-layer structures with EVOH, metallised coatings, or oxide barriers each have their own benefits. Suppliers must be judged on more than just their specs; they must also be reliable, offer good technical support, and be able to grow with the business. More and more, choices are based on environmental factors, and reusable single-material options are becoming more popular where performance allows. To be successful, you need to make sure that the film qualities fit the sensitivity of the product, the conditions of marketing, and the setting of the brand, all while keeping costs low. Working with experienced suppliers who can give you full technical support cuts down on trial and error and speeds up the time it takes to get products on the market with packaging solutions that keep them safe for as long as they last.
FAQ
1. How does humidity affect oxygen barriers in EVOH films?
EVOH exhibits moisture sensitivity, with barrier properties declining under high relative humidity conditions. Manufacturers address this by positioning EVOH layers between hydrophobic polymers like polyethylene or polypropylene, which protect the barrier layer from moisture exposure. Proper structure design ensures EVOH maintains effectiveness across varied storage environments.
2. Can barrier films support sustainability without compromising protection?
Recyclable mono-material structures using polyethylene with oxide coatings offer meaningful sustainability improvements while maintaining adequate barriers for many applications. These films achieve OTR values suitable for products with moderate oxygen sensitivity. Products requiring extreme barriers may still need traditional structures until technology advances further, though ongoing innovation continues improving recyclable options.
3. What distinguishes PVDC from EVOH barriers?
PVDC provides balanced oxygen and moisture resistance in thin coatings, making it efficient for applications requiring both barriers. EVOH delivers superior oxygen blocking but needs moisture protection. Regional environmental regulations increasingly restrict PVDC due to chlorine content, driving preference toward EVOH or oxide coating alternatives despite PVDC's performance advantages.
Partner with a Trusted Barrier Film Rollstock Manufacturer
Guoshengli Packaging brings over 25 years of flexible packaging manufacturing experience to help food brands, pet food companies, and health product manufacturers solve protection challenges with reliable barrier film solutions. Our multi-layer structures deliver OTR values below 1.0 cc/m²/day and MVTR under 1.0 g/m²/day, extending shelf life while maintaining compatibility with automated form-fill-seal equipment. We maintain ISO 9001, BRC, and SGS certifications alongside FDA and EU food contact compliance, ensuring your packaging meets international regulatory standards.
Our production capabilities include seven rotogravure printing lines, six lamination machines, and 49 converting units, enabling lead times of 15-20 days for custom-printed high barrier film rollstock structures. We offer recyclable options utilizing mono-material polyethylene constructions without sacrificing protection performance. Technical support throughout material selection, structure optimization, and production troubleshooting helps you avoid costly delays and quality issues.
Contact our team at sales@guoshengpacking.com to discuss your specific barrier requirements. We provide flexible minimum order quantities and expedited delivery options, making it practical to validate film performance before committing to large volumes. As an established barrier film rollstock supplier serving North American and European markets, we understand the operational demands of international food packaging and deliver consistency across repeat orders.
References
1. Robertson, Gordon L. (2016). Food Packaging: Principles and Practice, Third Edition. CRC Press, Taylor & Francis Group.
2. Marsh, Kenneth and Betty Bugusu (2007). "Food Packaging—Roles, Materials, and Environmental Issues," Journal of Food Science, Volume 72, Issue 3, pages R39-R55.
3. Coles, Richard, Derek McDowell, and Mark J. Kirwan (2003). Food Packaging Technology. Blackwell Publishing, CRC Press.
4. Siracusa, Valentina (2012). "Food Packaging Permeability Behaviour: A Report," International Journal of Polymer Science, Volume 2012, Article ID 302029.
5. Lange, Judith and Yasmine Wyser (2003). "Recent Innovations in Barrier Technologies for Plastic Packaging—A Review," Packaging Technology and Science, Volume 16, Issue 4, pages 149-158.
6. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez (2004). Plastics Packaging: Properties, Processing, Applications, and Regulations, Second Edition. Hanser Publications.
A side gusset bag with a valve is a special kind of flexible packaging that has side panels that can be expanded and a one-way degassing valve built right in. People who need reliable packaging for bulk goods, like coffee roasters, food manufacturers, and pet food manufacturers, love the 1kilo side gusset pouch with valve. When the pouch is full, this design lets it expand, making a box-like form that sits straight on shelves. The valve then lets out trapped gases, like CO2 from freshly roasted coffee beans, without letting air or moisture in. This one-of-a-kind mix keeps the product fresh, extends its shelf life, and keeps the aroma intact while it's being stored and shipped.
Understanding Side Gusset Bags with Valve
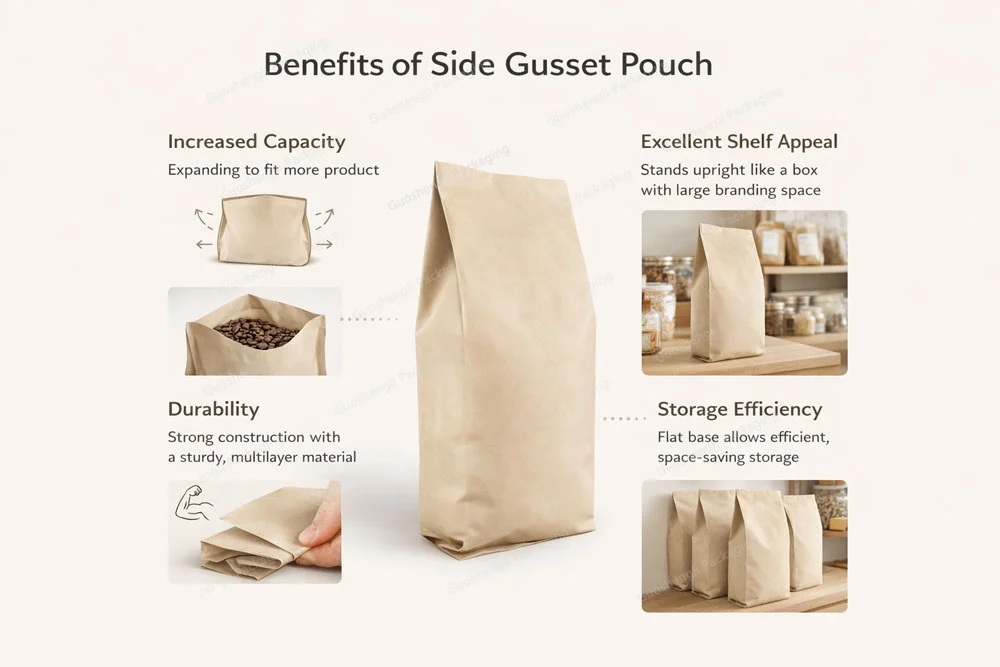
Side gusset packaging is very different from flat bottom bags or stand-up pouches. The folded pieces that run vertically along both sides of the pouch are what make it unique. When the inside is full of goods, these gussets expand outward, turning a flat package into a three-dimensional box with a rectangular base.
What Makes the Valve Essential
The built-in degassing valve is very important for products that give off gases after being packaged. In the days and weeks after they are made, coffee beans, roasted nuts, and some dried foods naturally give off carbon dioxide. Without a way to let go, these gases build up pressure inside sealed containers, which could cause bags to burst or seals to fail while they're being shipped.
There is an easy but effective way for the one-way valve to solve this problem. The pressure inside the valve from gases leaving briefly opens it, letting CO₂ escape. When pressure from the outside tries to push in, the valve shuts, keeping air and moisture from getting into the contents. During the product's shelf life, this constant freshness protection works on its own.
How Structure Supports Heavy Products
A 1-kilogram side gusset pouch with a valve needs to be able to hold a lot of weight without losing its seal. Usually, the multi-layer laminate structure is made up of PET (polyethylene terephthalate) for strength, aluminium foil or metallised film for barrier protection, and PE (polyethylene) for the ability to seal with heat. The thickness of this construction ranges from 120 to 160 microns, which is thick enough to handle one-kilogram packages.
The shape of the side gussets spreads the weight evenly across the bottom seal so that stress doesn't build up in one place. This engineering advantage makes it less likely that the bottom seal will break while the container is being moved, stacked, or shipped. Corner seals that are reinforced add extra security where stress tends to build up.
Key Benefits of Using 1 Kilo Side Gusset Pouches with Valve
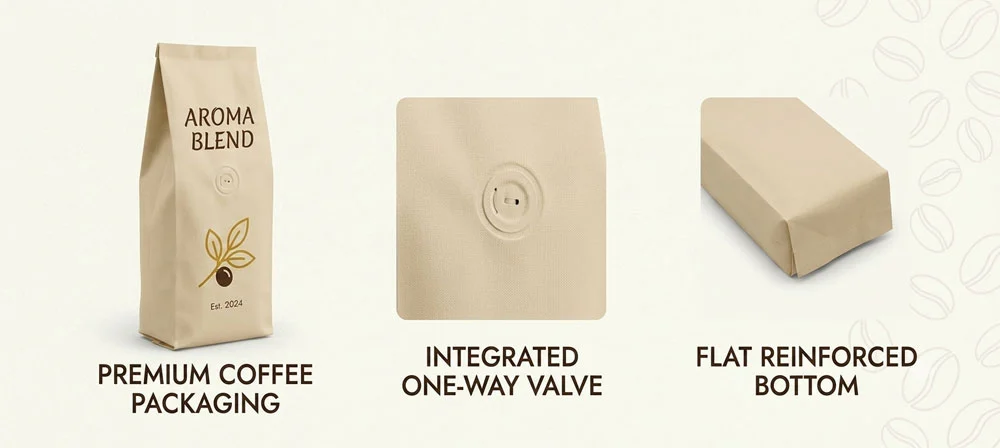
How a product is packaged has a direct effect on its quality, how people see the brand, and how efficiently the business runs. The side gusset structure with valves offers real benefits in a number of performance areas that are important to buying workers and production managers.
Superior Freshness Retention
Multi-layer barrier films make a wall that keeps oxygen, moisture, and light out, which are the three main things that keep food from staying fresh. Low oxygen transmission rate (OTR) and water vapor transmission rate (WVTR) structures help preserve product freshness. The degassing valve adds to this safety by letting gases inside the container leave while keeping outside contaminants out.
Coffee roasters say that switching from standard packaging to a 1kilo side gusset pouch with valve formats makes a big difference in how long the smell lasts. When barrier protection and gas control are used together, they keep the volatile flavour molecules that make premium coffee experiences unique. The same benefits apply to baked nuts, dried fruits, and other foods whose quality drops when exposed to oxygen.
Space Efficiency and Presentation
Side gusset bags have a small size that makes the best use of shelf space, even though they can hold one kilogram of goods. When full, the rectangular form lets store displays and storage racks fit together tightly. Because they are more efficient, they move less than hard crates and cost less to store.
The flat surfaces that widened gussets make are great for branding. The front and back panels are great places to put graphics, information about the product, and marketing messages. With high-resolution rotogravure printing, you can get up to 11 colours with great detail and colour accuracy. This turns useful packaging into strong brand assets.
Durability Under Real-World Conditions
Packaging is put through a lot of stress on production lines, transportation networks, and retail stores. Throughout the supply chain, the seal must be able to withstand punctures, tears, and other damage. A good 1-kilogram side gusset pouch with a valve is made with strong materials and careful craftsmanship to avoid problems.
Drop testing under application-specific conditions verifies package integrity during transportation, making sure that seals stay intact when packages are handled roughly. These quality control steps get rid of the expensive problems that come with packages that leak and goods that are tainted.
The above-mentioned real benefits directly lead to less trash, happier customers, and a better image for the brand. Production managers like how reliable it is and how it keeps the filling line from stopping. Marketing teams like how it looks and makes the products stand out on the shelf.
Common Uses & Industry Applications of Side Gusset Pouches with Valve
Valve-equipped side gusset packaging has been used successfully in many fields where keeping food fresh and looking professional are important for business goals. Real-life examples show that they are both flexible and useful.
Coffee Industry Leadership
The main people who use the 1kilo side gusset pouch with valve technology are coffee roasters. Premium whole bean coffee needs to be kept away from air, which breaks down flavour chemicals quickly. While letting CO2 out, the one-way valve stops air from getting in. This keeps the food fresh from cooking to eating.
These pouches help speciality roasters set their products apart in markets where there are a lot of other options. It looks professional, which sets high standards for quality, and it works well, keeping those promises. The benefits are the same for ground coffee, but it doesn't need to be degassed as much as whole beans do.
Food Manufacturing Applications
Side gusset valve pouches are the best way to protect dried fruits, certain freshly processed products, and granola. When these things are exposed to air, they often lose their freshness because they still have wetness or natural oils in them. The protective features stop the movement of moisture and oxidation that make food go bad.
This style of packing is also used for powdered foods like protein supplements, vitamin mixes, and speciality flours. The one-kilogram size is good for people who buy in bulk or who work in food service, and the reusable zipper makes it more useful after opening. The rectangular shape is good for manufacturers because it stacks well in warehouses.
Pet Food and Treat Packaging
More and more pet food companies are using 1 kg side flap pouches with valves for high-end treats and specialised nutrition products. The packaging conveys a sense of quality while also providing real freshness benefits. A lot of natural cat treats have oils and fats that break down quickly if they don't have the right layer protection.
When it comes to pet food, sturdiness is especially important because the package is handled roughly by customers and when it is being stocked in stores. Puncture-resistant construction stops the problems that happen when bags are torn, and products are scattered, which hurts how people see the brand.
Health and Wellness Segments
Valve pouches are used by supplement and health food brands for bulk powders, dried plants, and superfood ingredients. Based on claims of freshness and strength, these goods often have higher prices. Brand claims are stronger when the packaging clearly protects these traits.
Market research shows that people think of professional flexible packaging as a sign of high-quality health products. A well-designed 1kilo side gusset pouch with valve packaging looks good and supports a premium positioning. The higher price points are justified by the functional benefits, such as longer shelf life.
How to Choose the Right Side Gusset Bag with Valve for Your Procurement Needs
To choose the best packaging, you have to make sure that the technical details match the needs of the product, the production process, and what the market wants. Systematic review stops mistakes that cost a lot of money and cause problems with quality or inefficiency in operations.
Material Selection and Barrier Properties
Barrier requirements are set by the characteristics of the product. To keep from staling, coffee needs strong oxygen barriers, and powders that are sensitive to moisture need even stronger protection against water vapour. Barrier shapes that work best for different uses can be made into multi-layer laminates.
Aluminium foil layers in PET/AL/PE structures create full barriers against oxygen and moisture, giving them the best barrier performance. MOPP, VMPET, and PE options use metallised films that cover well, are more flexible, and might be able to be recycled. Choosing the right materials means finding a mix between performance needs, cost concerns, and environmental goals.
Valve Specifications and Compatibility
Where you put a valve affects both how it works and how it looks. Valve positions in the middle of the front panel give the best performance but take up valuable branding space. Side-mounted or back-positioned valves protect the images on the front panel while keeping the degassing working well. When describing the needs for a 1kilo side gusset bag with valve, the procurement specs should take both function and style into account.
Sizing and Dimensional Accuracy
The right sizes make sure that automated packaging lines can fill items quickly and correctly, and that products fit properly. One-kilogram pouches need to be about 200–240 mm wide and 300–350 mm tall when they are full, but the exact sizes depend on the density of the product and the look that is wanted.
The normal gusset width is between 80 and 120 mm, which allows the product to expand while still remaining stable when standing. For automated filling equipment to work reliably and avoid jams, the dimensions must always be within the acceptable range. Good makers stick to strict rules that help the production process go smoothly.
Comparing Alternative Packaging Formats
You can also get stand-up pouches with bottom gussets instead of side gusset designs. Bottom gusset designs are very stable and make the most of the space on the front panel for branding. Side pocket bags, on the other hand, are often cheaper for carrying one kilogram and give you the same utility.
For better display, rigid packages like jars are better, but they cost a lot more to make and ship. Flexible 1-kilo side gusset bag with valve packaging saves money on shipping costs by being lighter and taking up less room, but it still protects the product as well as hard options.
Knowing these trade-offs helps procurement professionals choose packaging that fits their budget, their business's needs, and their goals for placing in the market. Instead of maximising a single trait, the best choice strikes a mix between several factors.
Purchasing Guide and Supplier Selection for 1 Kilo Side Gusset Valve Pouches
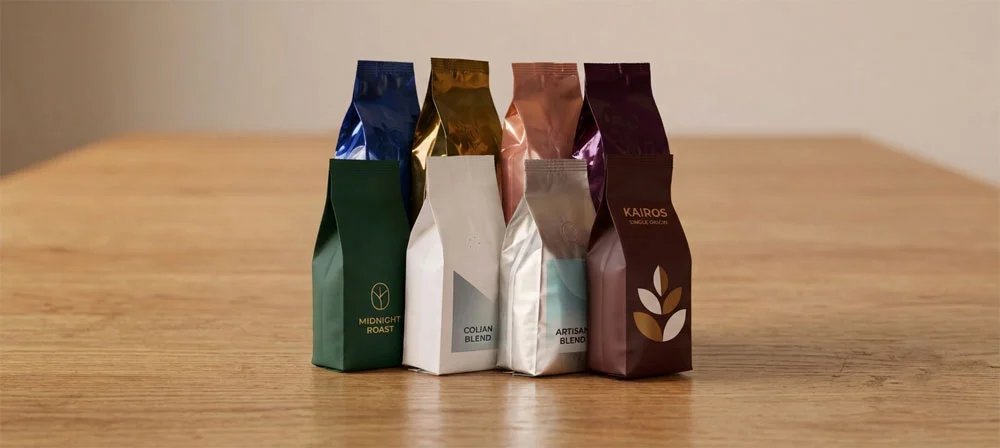
When making sourcing choices, it's not just about unit price; product stability, expert help, legal compliance, and long-term dependability are also important. Systematic review of suppliers lowers the risks of buying and helps businesses keep working together.
Certifications and Compliance Standards
Packaging that comes into contact with food must meet strict government standards. Following FDA rules in the US and EU rules in European markets sets the basic safety standards. Manufacturers with a good reputation show proof that their products and production methods meet these standards.
ISO 9001 certification shows that a quality management system is being used, and BRC (BRCGS Global Standard for Packaging Materials) certification talks about making sure that food packaging meets certain standards. These validations by a third party give buyers peace of mind that sellers keep quality controls uniform. The SGS testing reports give more proof of the barrier properties and material make-up.
Guoshengli Packaging has been serving foreign markets for 25 years and has all the major licenses needed to sell food packaging to other countries. This experience helps you understand how regulations differ in different markets and predict the compliance requirements that affect when a product will be approved for a 1kilo side gusset pouch with valve.
Minimum Order Quantities and Pricing Structure
When it comes to flexible package economics, setup costs for printing plates and production changes are common. For custom-printed bags, the minimum order quantity is usually between 10,000 and 20,000 units. However, digital printing technologies allow for smaller runs at higher costs per unit.
The way prices are set depends on the type of material, how complicated the printing is, and how many orders are placed. It is much cheaper to print simple two-color designs on standard materials than to print 11-color rotogravure designs on speciality laminates. Prices for a 1-kilo side gusset pouch with valve run from $0.1 to $0.45 per unit, based on these factors and the number of units ordered.
Different printing methods and current ability affect how long it takes to make something. Digital printing lets you turn around jobs in 7–10 days, which is good for test markets and small batches. Rotogravure printing takes 15 to 20 days, but the quality is better, and the cost per unit is lower for large orders. When you need service quickly, air shipping options can get your package to you in four to five days.
Customization Capabilities
To differentiate a brand, the packaging needs to stand out visually and clearly communicate the product's features. You can change more than just the pictures. You can also change the functionality of the product by adding tear notches, reusable zippers, hang holes, and clear windows.
Advanced suppliers offer design help that makes artwork work better with printing methods and suggests changes to the structure that make it work better. Technical advice helps buyers make decisions about which materials to use and which features to add that are in line with their needs and their budget.
A sample review is still necessary before agreeing to large sales. Good manufacturers give you samples before they start making the whole thing so you can check the colour, the way the material works, and the measurements. This confirmation step keeps production runs from having expensive shocks.
Assessing Supplier Reliability
For packing relationships to last, quality must be uniform, and service must be reliable. When evaluating a supplier, you should look at how much they can produce, how well they communicate, and how well they control quality. Site trips or video walks of factories can give you information about how they work and what they can make.
Customer references are a great way to find out how well a supplier is doing during a long-term relationship. Ask if the quality is the same for return orders, if they respond to problems, and if they can change their services to meet your needs.
We have long-term relationships with food brands, coffee roasters, and pet food makers in North America, Europe, and the Asia-Pacific region by being reliable and honest in our communication. Our experience of making products for 25 years shows that we are stable, which is something that procurement professionals look for when they are looking for sellers of important packaging parts.
Conclusion
1kilo side gusset pouch with valves have been shown to work well for coffee, food, pet goods, and health supplements that need to stay fresh. Barrier materials, structural design, and the way valves work together solve real problems in keeping products fresh and showing off brands. People who work in procurement should know how the quality of the materials, the valves, and the manufacturing process affect how well the packaging works. Systematic supplier selection based on certifications, production capabilities, and a history of dependability builds partnerships that help businesses reach their long-term goals. The 1kilo side gusset bag with valve is becoming more popular in fields where product quality and shelf life have a direct effect on customer happiness and company image.
FAQ
1. Can I customize side gusset valve pouches with my brand graphics?
Complete customization options exist for 1kilo side gusset pouch with valve designs. Rotogravure printing supports up to 11 colors with photographic quality reproduction, enabling complex graphics, gradients, and detailed imagery. Digital printing offers faster turnaround for shorter runs with somewhat more limited color matching. Both options accommodate logos, product information, nutritional panels, and marketing messages. Matte and glossy finish options affect visual presentation and tactile perception, with matte finishes often preferred for premium positioning.
2. What lead times should I expect for custom pouch orders?
Production timelines depend on printing method and current production schedules. Digital printing typically requires 7-10 days from artwork approval to finished goods, suitable for urgent launches or testing. Rotogravure printing extends to 15-20 days but delivers superior quality and cost efficiency for volume orders. Air shipping provides 4-5 day delivery, while ocean freight requires 3-4 weeks. Planning procurement cycles around these timelines prevents inventory gaps.
3. How do side gusset valve pouches impact environmental sustainability?
Modern laminate structures increasingly incorporate recyclable mono-material designs that simplify end-of-life processing. While traditional multi-layer laminates combining different polymers present recycling challenges, newer PE-based mono-structures enable recycling through existing infrastructure. Material efficiency compared to rigid packaging reduces overall resource consumption and transportation emissions. Manufacturers implementing RTO exhaust treatment systems minimize production environmental impact. Sustainability represents an evolving area where material science continues advancing packaging environmental profiles.
Partner with Guoshengli Packaging for Your Side Gusset Valve Pouch Needs
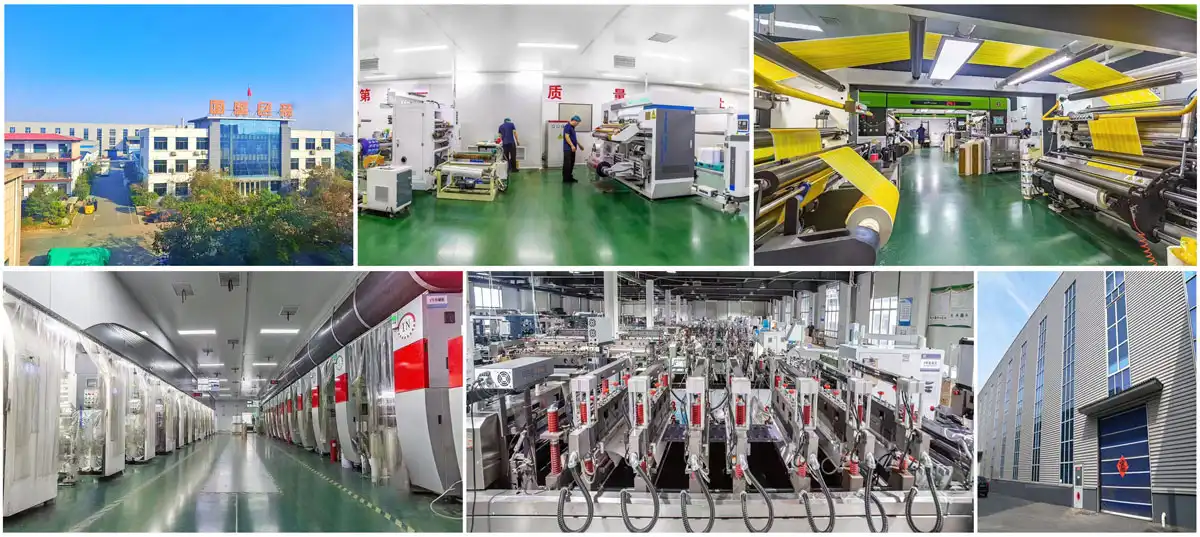
Choosing a 1kilo side gusset pouch with valve supplier impacts product quality, operational efficiency, and brand perception throughout your supply chain. Guoshengli Packaging brings 25 years of flexible packaging manufacturing expertise serving food, coffee, pet food, and supplement brands across international markets. Our ISO 9001, BRC, FDA, and SGS certifications demonstrate quality system maturity, while advanced production equipment ensures consistent output across repeat orders. We offer complete customization including up to 11-color rotogravure printing, flexible MOQ options, and rapid production timelines. Whether you need traditional multi-layer barriers or innovative recyclable structures, our technical team helps navigate material selections aligned with your product requirements and sustainability goals. Connect with our packaging specialists at sales@guoshengpacking.com to discuss your specific needs and request samples. As an established 1kilo side gusset pouch with valve manufacturer, we deliver the predictable performance that procurement professionals demand.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice, 3rd Edition. CRC Press, 2012.
2. Coles, Richard, and Derek McDowell. Packaging Technology: Fundamentals, Materials and Processes. Woodhead Publishing, 2003.
3. Marsh, Kenneth, and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Vol. 72, No. 3, 2007.
4. Yam, K.L. The Wiley Encyclopedia of Packaging Technology, 3rd Edition. John Wiley & Sons, 2009.
5. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations, 3rd Edition. Hanser Publications, 2016.
6. Brody, Aaron L., and Kenneth S. Marsh. Encyclopedia of Packaging Technology, 2nd Edition. John Wiley & Sons, 1997.
To find Quad Seal Pouches & Bags sellers you can trust, you need to know where to look and what to look for. Most of the time, companies that make goods do business at trade shows, direct plant routes, or business-to-business websites such as Alibaba and ThomasNet. The best sellers have proof that they work hard to make sure their goods are safe for food and are always made the same way, like having certificates from the FDA, BRC, and ISO 9001. Check to see how many of the four-seal pouches you want to buy, how they can be customised, how long the lead time is, and what kind of barrier protection technology they use. Most of the time, direct manufacturers have better prices, more flexible minimum order quantities, and the ability to make solutions that are unique to each customer. Businesses that want solid packaging for a long time should work with them because of this.
Understanding Quad Seal Pouches and Their Market Demand
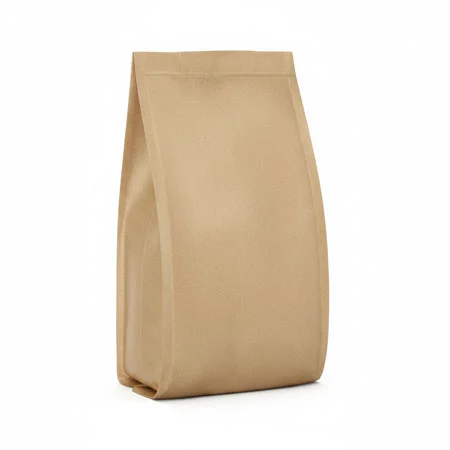
A new way to make flexible packaging is with quad seal pouches. They feature four vertical corner seals and side gussets, the base is formed when the pouch is filled, these pouches are more stable than regular three-side seal or stand-up pouches. These boxes can hold heavy things like flour, coffee, pet food, and grains without breaking because the stronger corner seals spread the weight out evenly.
These bags stand out because they are round and have flat sides. They stay straight on store shelves and give you more room to print your logo. It's easier to see the product and it looks more professional with this design. Both of these factors are very important in competitive markets where the way a store looks directly affects what people buy.
Materials and Customization Options
Multiple layers of materials, such as PET, PE, metal foil, and sometimes kraft paper, are used in quad seal packaging these days. The different layers allow certain amounts of air and water vapor to pass through, which keeps food fresh for as long as it's on the shelf. Oxygen, moisture, and light can't get through high-barrier films, so things last longer.
You can customise more than just the materials. Businesses can add many things, such as zippers that can be closed again, tear notches, one-way degassing valves for coffee use, and even ergonomic handles for bigger sizes. In terms of width, you can pick from 120 to 180 microns. Depending on how they are built, they can hold up to 20 kg of weight.
Why B2B Buyers Prefer Quad Seal Designs
The four-corner seal design gives these pouches great burst strength, which makes them perfect for automatic filling lines and rough handling in the supply chain. Their "dead-fold" design keeps the shape of the bag even as the products get smaller, so the shape is the same from the first use to the last. This dependability cuts down on stopping the filling line and rejects, which are common problems in high-volume production settings.
This style is being used more and more in the food packing, pet nutrition, health products, and beverage markets because it looks good and works well. The design works with strategies for buying in bulk and helps brands stand out by giving you flexible printing and finishing choices.
Key Criteria to Consider When Choosing Quad Seal Pouch Suppliers
Comparing unit prices isn't the only way to find the right supplier. Quality badges are basic signs of how well a product meets standards and follows the rules for Quad Seal Pouches & Bags.
Certifications and Compliance Standards
When materials get FDA approval, it means they meet the safety standards for food contact in the US market. BRC approval shows that a company follows world standards for food safety, which is especially important for companies that sell their products in Europe. ISO 9001 certification means that the company has strong quality management systems that make sure that the same high-quality products are made for all of its customers. SGS test results confirm the barrier performance, puncture strength, and material makeup by a third party.
With these certificates, brands don't have to worry about expensive product returns or fines from the government. Suppliers who don't have the right paperwork may offer lower prices at first, but they will end up causing big problems later on.
Customization Capabilities and Production Flexibility
A good provider should offer a range of printing methods, such as rotogravure printing for large quantities with up to 11-color reproduction and digital printing for smaller quantities or fast development. Finishes on the surface, like smooth, shiny, soft-touch, or metallic, affect both how something looks and how it feels to the touch.
Different providers have very different minimum order amounts. Some need at least 50,000 units, but manufacturers who are flexible can make smaller batches, which helps businesses test new products or keep an eye on their inventory. Rotogravure printing usually takes 15 to 20 days to make, while digital printing only takes 7 to 10 days, though faster services may be available.
Pricing Structures and Value Analysis
Price per unit goes down as volume goes up, but to figure out overall cost, you have to look at the quality of the materials, the accuracy of the manufacturing, and the number of defects. It's possible that cheaper choices use thinner films or worse ways to seal, which could cause the package to fail during shipping or filling. Problems like these have secret costs that show up in the form of lost products, angry customers, and damaged brands.
Direct factory price gets rid of markups for distributors, giving businesses that want to build long-term ties with suppliers a better deal. Clear pricing that breaks down the prices of materials, printing, and tools helps buyers make smart choices that fit their budgets and meet their quality standards.
Comparison of Top Quad Seal Pouch Supplier Types for B2B Purchasers
Businesses have different needs that are met by different types of suppliers. Being aware of these differences makes it easier to match buying tactics with the needs of operations.
Global Brands Versus Specialized Manufacturers
Global package companies that have been around for a long time offer stable quality and huge production capacities, which makes them a good choice for international businesses that need to follow the same rules in many areas. These sellers keep up large delivery networks and provide a wide range of expert help.
Specialised manufacturers focus on making new materials or products for specific uses. Most of the time, they offer more customisation options and faster reaction times for specific needs. They are willing to work with companies on custom formulations and structures, such as Quad Seal Pouches & Bags, which helps companies that are making high-end products or looking for more environmentally friendly ways to package them.
Geographic Sourcing Considerations
Suppliers in the US and Europe usually charge more, but they are closer, which has benefits like faster shipping times, easier communication across fewer time zones, and compliance with regional regulatory frameworks. When handling just-in-time stocking systems or needing to make quick changes to orders, these things matter.
Asian producers, especially those in China, can offer reasonable prices because their supply lines are more established and the cost of labour is lower. Quality varies a lot, so it's important to check with the supplier. Asian makers with a good reputation combine low prices with certifications that meet international standards. This makes them a great choice for businesses that want to save money without losing quality. Companies that have been making things for more than 25 years usually have a good track record in foreign markets.
Direct Manufacturers Versus Distributors
When you buy directly from manufacturers, you avoid the costs of going through middlemen and can work together more closely on specifications. When it comes to technology needs, quality problems, and customisation changes, direct ties make it easier to talk to each other. Manufacturers are also more open about how their products are made and where they get their materials.
Distributors make things easier by combining orders and letting you place smaller ones, but they charge markups that make the total cost more expensive. They work well for companies that need different types of packaging from different suppliers or don't have the means to manage ties with many factories.
Sustainable Packaging Trends
Environmental duty is becoming more and more important in purchasing decisions. When it comes to recycling, mono-material structures made of polyethylene make it easier than mixed-material laminates. Brands that care about the environment like compostable papers made from PLA or PBAT, but they may not have the same protection qualities as standard materials.
Suppliers who offer packages that can be recycled in their entirety or use foreign RTO exhaust gas cleaning technology show that they care about the environment. These features help companies reach their sustainability goals and meet customer demands for better options without lowering the safety of their products.
How to Find and Verify Reliable Quad Seal Pouch Suppliers
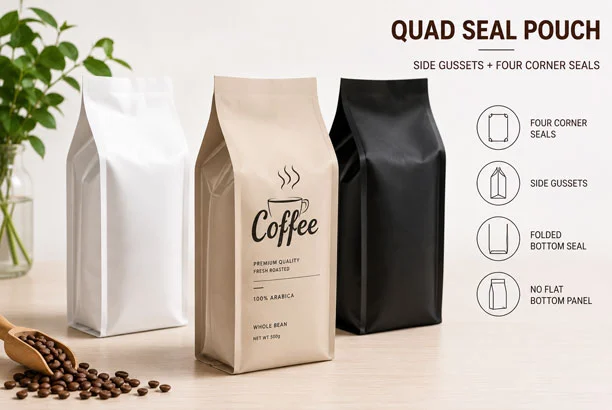
To find reliable partners, effective sourcing combines online research with strict verification steps.
Industry Platforms and Online Marketplaces
Alibaba is still the biggest business-to-business (B2B) site that connects buyers from around the world with Asian producers. Platform filters let you search by type of certification, minimum order quantity, and past transactions. Trade Assurance programs and stickers that say "Verified Supplier" add extra layers of security.
ThomasNet is an online directory that focuses on North American makers and wholesalers. It offers complete company descriptions, product catalogues, and direct contact information. Europages does the same things for European providers. These platforms make initial research easier by collecting information from suppliers and letting you compare them side-by-side.
Trade shows in the industry, such as Pack Expo, Anuga FoodTec, and PACK EXPO International, let you meet sellers in person, look at samples, and talk in depth about technical needs. Many long-lasting relationships start at these events where people meet.
Evaluating Supplier Credentials
In addition to certificates, you can figure out how much can be made by touring the building or looking at thorough photos. These days, modern buildings should have many printing machines, sealing lines, and converting machines. It's clear that a company with seven printing machines, six laminating units, and 49 converting machines can handle big orders and meet tight deadlines.
Sample evaluation is very important. Ask for samples that meet the requirements for your product, and then do fill tests, drop tests, and shelf-life simulations. Check the quality of the writing, the shape correctness, the strength of the seal, and the integrity of the barrier. Samples tell you more about how well a product can be made than any advertising material could.
Case studies and examples from clients can help you figure out how reliable a seller is. Talk to current customers to find out how often deliveries are made on time, how quickly they are responded to, how problems are solved, and how consistent the service is for repeat orders. Partnerships with names in Europe, the US, and Australia that can be proven show that the company has exported before.
Building Long-Term Supplier Relationships
When there are problems in the supply chain, transactional ways of buying things leave people open to harm. Stability is created by strategic relationships based on open communication and shared gain. Suppliers can better plan their capacity when they share production forecasts. Giving feedback on quality problems at the right time allows for ongoing growth. By negotiating outline deals, you can set stable prices and give production slots priority during busy times.
Reliable suppliers become like an extension of your operations team; they'll suggest ways to make things better, let you know when materials aren't available, and meet urgent requests when you need to be flexible. These relationships grow when both people are consistently involved, treat each other fairly, and understand that the success of the other person is good for both of them.
Practical Tips for Procuring Quad Seal Pouches for Your Business
To get the best deals on things, you need to make sure that the package requirements match the features of the product and the way things work with Quad Seal Pouches & Bags.
Matching Features to Product Requirements
One-way degassing valves must be used on coffee packaging to let carbon dioxide out while blocking oxygen from getting in. This keeps the volatile aromas that define quality. Light and water are also kept out by high-barrier aluminium layers. For 5–15 kg bags of pet food, the seals need to be stronger, and the film needs to be thicker so that it can handle rough handling during palletisation and shipping. Anti-static treatments and micro-perforations keep flour and powdered goods from puffing up while they're being shipped.
Knowing how sensitive your product is to external factors will help you choose the right materials. Goods that are sensitive to moisture need low rates of water vapour transfer. Products that are sensitive to oxygen need layers of aluminium foil or metallized films. Puncture-resistant materials are needed for products with sharp edges.
Cost-Efficiency Strategies in Bulk Purchasing
The best way to make money is to find the balance between minimum order quantities, inventory carrying costs, and turnover rates. Ordering more lowers the cost per unit, but it takes up more cash and stock room. The best order size can be found by accurately predicting demand based on past sales and growth projections.
Custom branding makes marketing more effective and may allow for higher prices that increase profits. With high-quality rotogravure printing, even on multiple runs, the colours will look the same, making the brand more recognisable and increasing its value.
Changing the terms of payment has an effect on managing cash flow. A lot of Asian makers will take lines of credit or organised payment plans that work with the way businesses run. This makes it easier on their finances when they are growing.
Supply Chain Management Best Practices
International shipping adds variables that suppliers can't control, like unpredictable changes in port congestion, customs delays, and carrier availability. Adding lead time buffers helps protect against problems. Ordering packing supplies 60 to 90 days ahead of time gives you time in case something goes wrong.
Concentration risk can be reduced by using a variety of suppliers in different areas. Having a primary supplier and a qualified backup option in mind at all times helps keep things running smoothly when problems do happen. This approach was very important during the recent changes in the world supply chain.
Misunderstandings can be avoided by writing down clear quality standards in buy deals. Include standards for acceptable sizes, seal strength, barrier properties, and how the product looks. Set up protocols for incoming inspections that check for compliance before production runs.
For pressing needs, rapid production and transport services can help. Some manufacturers offer air freight options that can deliver in 4 to 5 days, but they charge more. Digital printing lets you make smaller batches more quickly when you need to respond quickly to a market opportunity.
Conclusion
To find reliable Quad Seal Pouches & Bags providers, you need to carefully look at their certifications, production capabilities, and customisation options. Direct relationships with manufacturers that offer clear pricing, flexible minimum orders, and technical support are good for business-to-business buyers. Platforms like Alibaba and ThomasNet make it easier to find things to buy, and samples, references, and facility inspections are used to make sure they are reliable. When making choices about geographic sources, cost benefits are weighed against wait times and regulatory consistency. As brands become more environmentally conscious, sustainable packaging choices have a bigger impact on what they buy. Matching the barrier qualities, valve integration, and structure specs of the bag to the needs of the product ensures that the package works reliably during production and distribution. Long-term partnerships based on open communication and mutual benefit create a stable supply chain that helps businesses grow and keep quality high in tough markets.
FAQ
1. What distinguishes quad seal pouches from flat bottom pouches?
Quad seal bags utilize product weight to form the base, creating a traditional side-gusset appearance with enhanced stability. Flat bottom pouches feature a discrete gusseted base engineered into the structure. Quad seal designs often prove more cost-effective for large-volume fills exceeding several kilograms.
2. Can quad seal pouches accommodate sustainable materials?
Yes, manufacturers can produce them using mono-material recyclable polyethylene or compostable laminates, though barrier properties may vary compared to traditional multi-layer constructions. Discussing specific shelf-life requirements with suppliers ensures sustainable materials meet product protection needs.
3. What reclosable options work with this format?
Integrated press-to-close zippers are commonly applied to the front panel, enabling repeated opening and closing. Some applications use tin-tie closures, particularly for products like coffee where maintaining freshness after opening matters significantly.
Partner With a Trusted Quad Seal Pouch Manufacturer
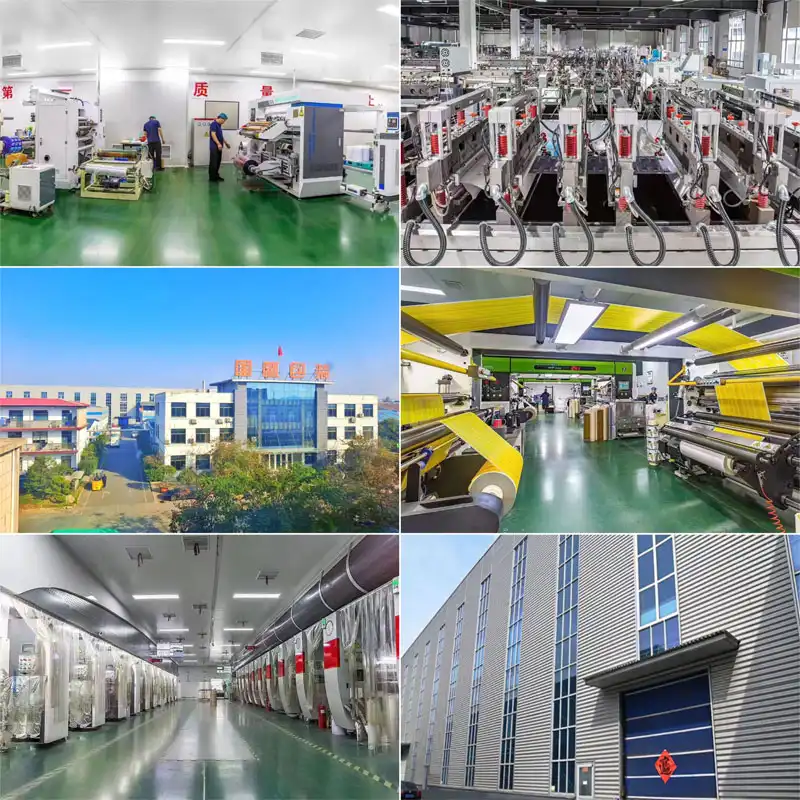
Guoshengli Packaging brings over 25 years of flexible packaging manufacturing expertise to businesses seeking reliable Quad Seal Pouches & Bags solutions. Our factory-direct supply model combines competitive pricing with flexible minimum order quantities, accommodating both emerging brands and established enterprises. We operate 7 printing machines, 6 laminating units, and 49 converting machines, ensuring production capacity meets your timeline requirements reliably. Our ISO 9001, BRC, FDA, and SGS certifications demonstrate commitment to quality standards that protect your brand reputation. Whether you need high-barrier films for extended shelf life, sustainable packaging development, or rapid production services with 7-10 day digital printing lead times, our team provides expert material selection guidance tailored to your specific applications. Contact our team at sales@guoshengpacking.com to discuss your packaging requirements. We offer sample evaluations, customized solutions, and transparent communication that simplifies international procurement.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice, 3rd Edition. CRC Press, 2013.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Volume 72, Issue 3, 2007.
3. Soroka, Walter. Fundamentals of Packaging Technology, 5th Edition. Institute of Packaging Professionals, 2014.
4. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations, 3rd Edition. Hanser Publications, 2016.
5. Yam, Kit L. The Wiley Encyclopedia of Packaging Technology, 3rd Edition. John Wiley & Sons, 2009.
6. Coles, Richard and Derek McDowell. Encyclopedia of Food Sciences and Nutrition: Packaging of Foods, 2nd Edition. Academic Press, 2003.