- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Greek
- German
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
BLOG LIST
Small businesses face a unique challenge when selecting packaging: how do you balance cost, quality, product protection, and environmental goals while creating a strong first impression? Brown kraft paper pouches offer a flexible solution that can address many of these priorities when the complete structure is properly specified. These natural-looking packages combine rustic authenticity with modern barrier technology, helping protect products while giving brands a distinctive paper-based appearance. At Guoshengli Packaging, we've seen many small businesses use kraft paper packaging to strengthen shelf presentation while tailoring the barrier, printing, and functional features to their actual product requirements.
Understanding Brown Kraft Paper Pouches: Materials, Types, and Benefits
What Makes Kraft Paper Packaging Different?
Brown kraft paper pouches are a flexible packaging format that combines kraft paper with one or more functional layers. Each layer can be selected to provide a different role within the package. The outer layer of brown kraft paper pouches, which is usually between 40 and 80 GSM (grams per square meter), can provide a natural appearance, surface strength, and a printable area for branding.
The multi-layer lamination system on these pouches is what allows the structure to deliver different levels of product protection. Materials such as metallized PET, aluminum foil, EVOH, nylon, PE, or CPP may be combined with the natural paper exterior depending on the product requirements. These layers can help control oxygen, moisture, aroma, grease, and light exposure. With the correct structure and sealing system, brown kraft paper pouches can support the target shelf life of products such as beef jerky, organic coffee, handmade snacks, and other dry or semi-dry foods.
Available Pouch Styles for Different Business Needs
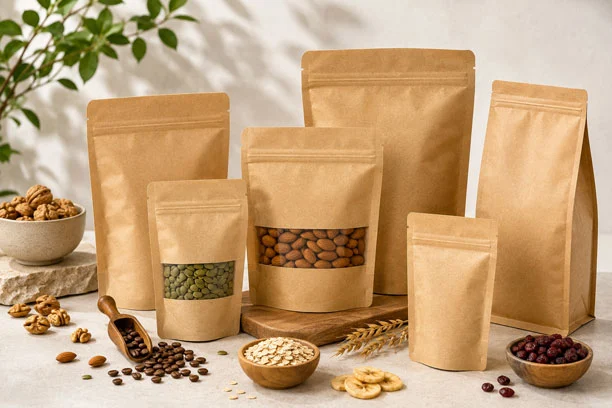
Picking the right bag type has a direct effect on both how well it works and how it looks on store shelves. Three-side seal bags can work well for dried meats, jerky, and sample products because they provide a flat, compact format with relatively simple construction. Their straightforward design can help control converting costs while still allowing the barrier structure to be tailored to the product.
Stand-up bags have bottom gussets that allow the package to stand upright on retail shelves. Coffee roasters and food brands often choose this format because it offers strong front-panel visibility and can incorporate features such as resealable zippers and degassing valves where appropriate.
Flat-bottom pouches offer a more structured presentation and multiple printable panels. This format can suit premium-positioned products and larger fill weights when pouch dimensions and material strength are correctly specified. Side gusset pouches provide additional internal volume and can work well for bulk powders, teas, coffee, and other products that require efficient use of pack space.
Core Benefits That Drive Business Results
Natural kraft can help a brand stand out immediately. Glossy plastic packaging can create a very different visual impression, while matte kraft can communicate a natural, artisanal, or premium identity. Brown kraft paper pouches therefore give small businesses a way to create a distinctive shelf appearance before the customer reads the label.
Barrier performance is another important advantage when the pouch is properly engineered. Multi-layer structures can help control oxygen and moisture exposure that may reduce product quality over time. Effective barrier protection can help reduce product deterioration and quality-related complaints when the packaging is matched to the actual food, shelf-life target, and storage route. For coffee, barrier performance can also help limit exposure to oxygen, moisture, and aroma loss.
Easy-to-use features can improve consumer convenience. Tear notches reduce the need for scissors when the pouch design supports easy opening. Hang holes allow selected pouch styles to work with hook-based retail displays. Resealable closures can help consumers close the package between uses, although they do not replace the primary factory heat seal.
Comparing Brown Kraft Paper Pouches with Other Packaging Options
Environmental Impact Assessment
Traditional plastic packaging remains widely used because it can provide strong product protection with relatively low material weight. At the same time, brands and regulators are placing greater attention on packaging reduction, recyclability, recycled content, responsible sourcing, and end-of-life management.
Brown kraft paper pouches can support different environmental strategies depending on their complete construction. Kraft paper itself is fibre-based, but conventional paper-plastic laminates should not automatically be described as biodegradable or recyclable. Some paper-plastic structures may require specialized recycling routes, while selected recyclable or compostable constructions should be evaluated separately according to the complete material structure and target-market infrastructure.
Brands that support circular-economy goals may also evaluate selected PLA- or PBAT-based structures where the complete package meets relevant compostability requirements and a suitable industrial-composting route exists. These materials should not be treated as automatically better for the environment simply because they are described as bio-based, biodegradable, or compostable. Their environmental performance depends on the complete packaging system, manufacturing process, product protection, and intended end-of-life route.
Durability and Performance Comparison
Buying professionals sometimes worry that brown kraft paper bags may not provide the same level of protection as other flexible packaging formats. In practice, performance depends primarily on the complete laminate rather than the kraft layer alone. Properly designed kraft-laminate pouches can achieve strong barrier and mechanical performance when the paper, polymer, and barrier layers are matched to the application.
Grease resistance is particularly important for products such as roasted nuts, nut butters, jerky, and other oily foods. For these applications, the complete pouch structure should be evaluated for grease resistance and resistance to oil migration or staining. Where grease-resistant paper treatments are used, applicable food-contact and chemical-compliance requirements should also be verified.
Puncture and tear performance also depend on the complete laminate. Paper strength, polymer layers, total thickness, seal design, and product geometry all influence how the pouch behaves during filling, transportation, and retail handling. Structures containing materials such as PA or suitable PE grades may be selected where additional toughness or puncture resistance is required.
Cost-Effectiveness Analysis
Brown kraft paper pouches may carry a higher material and converting cost than some all-plastic structures, depending on the kraft grade, barrier laminate, printing method, order size, pouch type, and added features. For small businesses, the relevant question is therefore not whether kraft packaging always costs more, but whether the total packaging value supports the product and brand strategy.
Effective product protection can help reduce quality losses, returns, and avoidable waste when the pouch structure is correctly matched to the product. The commercial value of that protection depends on the product category, shelf-life target, and distribution route rather than on the kraft paper layer alone.
The distinctive paper appearance may also support shelf differentiation and brand positioning. For small businesses competing with larger brands, this visual identity can be useful when it is consistent with the product, pricing, and target consumer. Packaging should therefore be evaluated as part of the overall product proposition rather than only as a per-unit material cost.
How Small Businesses Can Effectively Use Brown Kraft Paper Pouches
Optimizing Product Freshness and Shelf Life
Your product's shelf life depends on selecting barrier performance that matches its actual sensitivity. For oxygen-sensitive products such as coffee, nuts, and dried fruits, aluminium foil, metallized PET, EVOH, or other barrier technologies may be considered. OTR targets should be defined under specified test conditions and matched to the product, filling process, target shelf life, and distribution route rather than using one universal value.
Moisture-sensitive protein powders, supplement mixes, and dehydrated ingredients require structures with appropriate low-WVTR performance. EVOH may also be incorporated where additional oxygen barrier is required, but moisture protection should be evaluated through the complete laminate rather than attributed to EVOH alone.
Simpler kraft/PE or paper-laminate structures may suit selected dry products with modest barrier requirements and relatively stable storage conditions. We help clients compare barrier requirements with product needs so they can avoid both under-specifying a pouch and over-engineering a structure that adds unnecessary cost.
Enhancing Brand Perception Through Design
Custom printing turns brown kraft paper bags into strong brand surfaces. Rotogravure printing can reproduce up to 11 colours on suitable production runs and can support consistent colour reproduction when artwork, cylinders, inks, and process controls are properly managed.
Transparent windows can help consumers see the product, which can support confidence in categories where appearance matters. However, the window material and area should be evaluated because adding a clear section may change the overall oxygen, moisture, or light barrier compared with an opaque metallized or foil laminate.
High-end brands may use matte surfaces because they complement the natural texture of kraft paper. Spot UV, glossy details, embossing, or other specialty effects can also be considered where they are compatible with the material and converting process. These finishing techniques should be selected according to the actual pouch structure rather than treated as universal options.
Real-World Success Applications
Specialty coffee roasters often choose brown Kraft pouches because the natural paper appearance can support an artisanal or premium brand position. Where required, built-in degassing valves can allow carbon dioxide to escape from freshly roasted beans while helping limit outside air ingress. Final freshness still depends on the coffee, roast-to-pack timing, barrier structure, seal integrity, and storage conditions.
Pet treat manufacturers may also choose brown kraft paper pouches when a natural appearance fits the product positioning. For these applications, puncture resistance, grease resistance, seal performance, and barrier requirements should be evaluated using the actual treat rather than assuming that the kraft format alone provides the required protection.
Healthy snack companies can use brown kraft paper pouches to create a simple, natural, or premium shelf presentation. The packaging can support brand differentiation, but claims about consumer preference, price premiums, or sales increases should be based on actual market research or brand-specific evidence rather than assumed from the pouch material itself.
Buying Guide: How to Procure Brown Kraft Paper Pouches for Your Business
Selecting Qualified Suppliers
Supplier selection is an important procurement decision for long-term performance. Quality differences between samples and full production can create filling-line issues, returns, and delays for small businesses. Buyers should therefore evaluate suppliers using several core criteria before committing to repeat production.
Manufacturing certifications and compliance documentation can provide useful evidence of quality-system capability. ISO 9001 supports quality management, while BRCGS Packaging Materials certification applies specifically to packaging-material manufacturing sites. For products sold in the United States, food-contact materials should comply with applicable FDA requirements for their intended use rather than being described simply as "FDA-certified."
Production capacity affects whether a supplier can grow alongside the business. Guoshengli Packaging has annual flexible-packaging production capacity of approximately 20,000 tonnes and can support both smaller commercial programmes and high-volume repeat production, subject to the requirements of each project.
Technical knowledge distinguishes strategic partners from simple product suppliers. Instead of relying only on standard stock structures, our team reviews product sensitivity to moisture, oxygen, grease, aroma, and storage conditions to recommend barrier specifications that balance protection, manufacturability, and cost.
Understanding Minimum Orders and Pricing Structures
Minimum order quantities (MOQs) affect small businesses' cash flow and inventory planning. Rotogravure printing generally requires higher MOQs because of cylinder preparation and setup costs, although actual minimums depend on pouch size, material structure, number of designs, and production requirements.
Digital printing can help startups develop new products and serve smaller or more specialised markets. It can support lower MOQs for selected projects because conventional printing cylinders are not required. Digital printing may have a higher unit cost at larger volumes, while reducing tooling cost and inventory exposure for market testing or multi-SKU launches.
Larger commitments may reduce unit costs through more efficient production and material use. Businesses should compare annual consumption, number of designs, storage capacity, cash flow, and repeat-order needs before deciding whether one larger order or several smaller runs is commercially better.
Navigating the Customization Process
Product requirements and brand goals should guide customization. We recommend materials and structures according to product-protection needs without adding unnecessary complexity. Factors such as moisture sensitivity, fat content, filling method, target shelf life, and storage conditions can all influence the final recommendation.
Artwork preparation affects production speed and print quality. Vector artwork is generally preferred for logos and line graphics because it scales cleanly, although the final artwork format should follow the printer's technical requirements. Digital mock-ups can help visualize how artwork will sit on a three-dimensional pouch before production.
Sample production is an important part of testing before mass production. Depending on the project stage, suppliers may provide stock samples, material samples, printed mock-ups, or production samples. Customers can use these for filling, fit, handling, and preliminary storage evaluation, while final barrier and shelf-life performance should be validated under defined conditions using the actual product.
Printing technology and order complexity influence manufacturing lead times. Digital printing can support relatively fast short-run development for selected projects, while rotogravure orders require cylinder preparation and additional production steps. Actual lead time depends on artwork approval, material availability, pouch construction, curing requirements, production scheduling, and order complexity.
Why Brown Kraft Paper Pouches Are a Smart Choice for Sustainable Small Businesses
Supporting Circular Economy Principles
The circular economy focuses on reducing waste and keeping materials in use through reuse, recycling, and other appropriate recovery routes. Brown kraft paper pouches can support these objectives in selected applications, but their recyclability depends on the complete package rather than the kraft paper exterior alone.
Although paper recycling infrastructure is widely available in many regions, laminated kraft pouches should not automatically be placed in standard mixed-paper streams. Paper-plastic laminates may behave differently during pulping and sorting depending on fibre yield, polymer content, adhesives, coatings, windows, closures, and local recycling-system requirements.
Recyclable PE technologies can support circularity when the complete pouch is designed as a suitable mono-PE structure. However, simply adding a PE inner layer to a kraft-paper laminate does not make the entire package mono-material or fully recyclable. Brands interested in recyclable flexible packaging should evaluate the full construction against the relevant recycling guidelines and target-market collection system.
Meeting Regulatory Requirements and Consumer Expectations
Extended producer responsibility (EPR), packaging-reduction requirements, recycled-content rules, and recyclability requirements are evolving across Europe and parts of North America. These obligations vary by jurisdiction and should be reviewed according to the specific target market rather than assuming that one regional trend will automatically become a nationwide requirement elsewhere.
Businesses may use brown kraft paper pouches as part of a broader packaging strategy when the format, material construction, and environmental claims align with the applicable market. Early technical planning can also help brands avoid redesigning packaging later when regulations or retailer requirements change.
Some consumer segments show strong interest in sustainability-related packaging attributes, but purchase behaviour varies by market, product category, price sensitivity, and the credibility of the environmental claim. Brown kraft paper pouches can communicate a natural visual identity, but the environmental performance of the finished package should be supported by the actual structure and end-of-life route.
Innovations Enhancing Functionality
Modern barrier technology continues to improve the range of structures available for brown kraft paper pouches. Metallized films can provide strong barrier performance with a thin deposited metal layer, while aluminium foil can provide stronger opaque light and gas barrier for more demanding applications. Material selection should be based on the required protection rather than assuming that one barrier technology always matches another.
Selected mono-material barrier technologies are also being developed to improve recyclability compatibility while retaining required product protection. Their actual performance depends on barrier layers, coatings, adhesives, sealants, processing conditions, and the target shelf-life requirement, so product-specific testing remains important.
PLA, PBAT, and other compostable packaging materials may be tested and certified against standards such as EN 13432 or ASTM D6400 where applicable. Degradation conditions and time depend on the certified system and industrial composting environment. These materials should not be described as automatically recyclable or universally biodegradable simply because they contain compostable polymers.
Smart packaging can also add functionality to modern products. QR codes printed on kraft surfaces can link consumers to product information, sustainability documentation, traceability data, or loyalty programmes. Some brands may also evaluate NFC or other digital technologies for premium products or supply-chain applications where the added cost and functionality are justified.
Conclusion
Brown kraft paper pouches can help small businesses address several packaging priorities at once, including product protection, brand differentiation, flexible customization, and selected sustainability objectives. Their natural appearance can support artisanal, premium, or sustainability-oriented brand positioning, while functional barrier layers can be selected independently according to the product's oxygen, moisture, grease, light, and shelf-life requirements. Choosing the right pouch style, barrier specification, and customization options can turn packaging into an important part of the product experience rather than treating it only as a cost of doing business. Guoshengli Packaging has more than 25 years of flexible-packaging manufacturing experience and works with small businesses by providing technical recommendations, quality-management support, and scalable production options.
FAQ
1. Can brown kraft paper pouches be recycled properly?
It depends on the complete structure. Standard brown kraft paper pouches laminated with PE, PET, metallized film, foil, adhesives, windows, or zippers should not be assumed to be recyclable through ordinary paper streams simply because the outer layer is kraft paper. Fibre recovery, polymer content, adhesive systems, coatings, accessories, and local collection and recycling infrastructure all influence recyclability. Certified compostable structures are a separate end-of-life route and should not be described as recyclable unless they are also accepted in an appropriate recycling system.
2. How do these pouches handle grease-heavy products?
Brown kraft paper pouches for oily products can be designed with inner laminate structures that help resist oil migration and staining of the outer paper surface. The actual performance depends on the complete laminate rather than the kraft layer alone. For roasted nuts, nut butters, jerky, and other fatty foods, the structure should be evaluated for grease resistance, seal performance, and compatibility with the actual product over the intended storage period. Where grease-resistant paper treatments are used, applicable food-contact and chemical-compliance requirements should also be confirmed.
3. What shelf-life extension can I expect compared to basic plastic bags?
Shelf-life improvement cannot be predicted from pouch type alone. It depends on the product's sensitivity to oxygen, moisture, light, aroma loss, fat oxidation, initial product quality, filling conditions, seal integrity, storage temperature, and distribution route. A high-barrier kraft laminate may support a longer shelf-life target than a low-barrier structure, but actual shelf life should be validated using the specific product and defined storage conditions rather than estimated from the material name alone.
Get Started with Guoshengli Packaging—Your Trusted Brown Kraft Paper Pouches Manufacturer
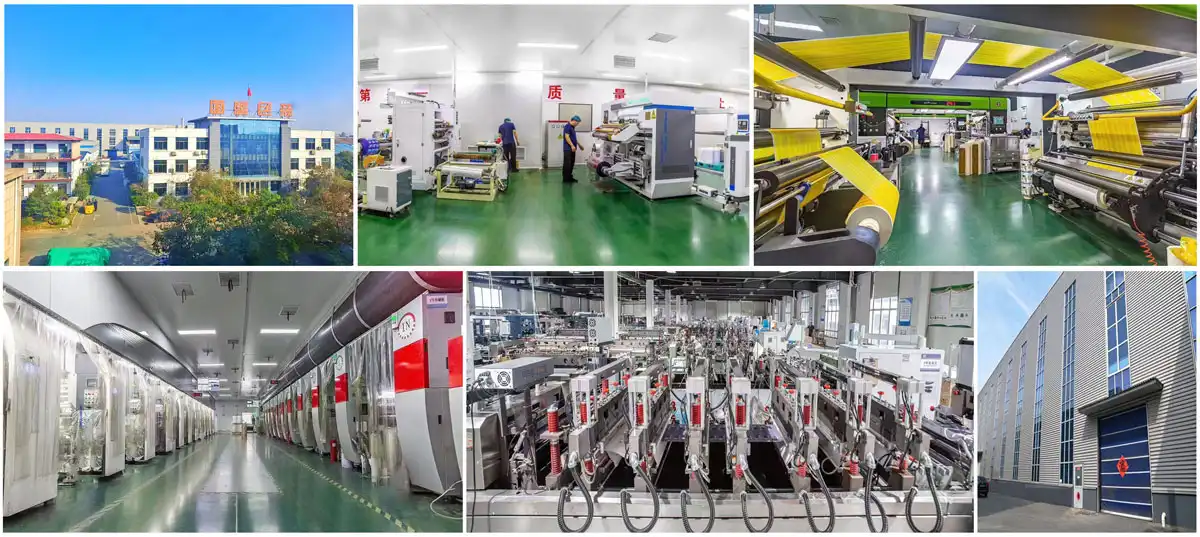
Small businesses need packaging partners who understand the challenges of cash flow, inventory control, product protection, and the need to stand out in competitive markets. With brown kraft paper pouches designed around product requirements and shelf presentation, Guoshengli Packaging supports brands at different stages of growth. Our quality systems include ISO 9001 and BRCGS Packaging Materials certification, together with food-contact compliance documentation for applicable target markets.
We support both digital and rotogravure printing so customers can test markets with lower-volume projects and move into larger repeat production as demand grows. MOQ, material structure, printing method, lead time, and customization options depend on the specific project rather than one fixed specification.
Email our team at sales@guoshengpacking.com to discuss your product, target market, pouch style, material requirements, and branding goals. We can recommend suitable brown kraft paper pouches, barrier structures, printing options, and functional features based on the actual product and commercial requirements.
References
-
Robertson, Gordon L. Food Packaging: Principles and Practice. 3rd ed. CRC Press, 2012.
-
Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, vol. 72, no. 3, 2007, pp. R39–R55.
-
Yam, Kit L. The Wiley Encyclopedia of Packaging Technology. 3rd ed. John Wiley & Sons, 2009.
-
Kirwan, Mark J. Paper and Paperboard Packaging Technology. Blackwell Publishing, 2005.
-
Selke, Susan E.M., John D. Cutler, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations. 3rd ed. Hanser Publications, 2016.
-
Coles, Richard and Derek McDowell. Food Packaging Technology. Blackwell Publishing, 2003.
Brown kraft paper pouches have emerged as a leading packaging solution for brands seeking to combine a natural paper appearance with practical product protection. These pouches can pair kraft paper aesthetics with functional barrier layers, offering a flexible alternative to conventional all-plastic packaging for selected applications. Their strength, versatility, and authentic appearance resonate with sustainability-conscious consumers while still allowing brands to meet food safety, barrier, and performance requirements.
Understanding Brown Kraft Paper Pouches: Features and Benefits
What Makes Brown Kraft Paper Pouches Unique
Brown kraft paper pouches are a hybrid type of packaging made with natural kraft paper and, in many applications, one or more laminated barrier layers. At Guoshengli Packaging, we make these pouches with kraft paper that is typically between 40 and 80 GSM together with functional layers such as PE, VMPET, or aluminum foil depending on product requirements. This construction helps solve an important packaging challenge: brands may want a natural, paper-based appearance while still needing adequate barrier, sealing, and mechanical performance. The kraft exterior provides a distinctive surface for branding while maintaining the rustic visual identity associated with natural paper packaging.
Core Structural Features
There are several pouch configurations available for brown kraft paper pouches, including three-side seal, stand-up, flat-bottom, and side-gusset formats. Depending on the application, material thickness may fall within a range such as 120 to 160 microns, although final thickness should be selected according to product weight, barrier requirements, puncture risk, and handling conditions. Tear notches can make the pouch easier to open without scissors, while optional hang holes can support retail display on hooks or racks. Because of these qualities, brown kraft paper pouches can work well for packaging beef jerky, coffee, pet treats, powdered supplements, and other dry or semi-dry products when the complete structure is properly specified.
Environmental and Brand Benefits
Brown kraft paper pouches can support selected sustainability strategies, but the environmental performance of the finished pouch depends on the complete material structure rather than the kraft layer alone. Kraft paper itself is fibre-based, but laminated plastic, metallized, foil, adhesive, coating, zipper, and window components all influence recyclability or compostability. Selected PLA- or PBAT-based structures may be considered where an appropriate industrial-composting route and relevant certification are available, while paper-plastic laminates may require specialised collection and recycling processes. The natural kraft look can still provide strong brand value by communicating a simple, premium, or artisanal visual identity and helping products stand out on crowded retail shelves.
How Brown Kraft Paper Pouches Outperform Traditional Packaging Solutions
Environmental Advantages Over Conventional Options
Brown kraft paper pouches can support brands that want to increase the use of fibre-based materials or create a more natural packaging appearance. Kraft paper is produced from wood fibre, which is a renewable feedstock, although the overall environmental footprint of the finished pouch depends on material weight, laminate construction, manufacturing, transport, and end-of-life route. Where certified fibre sourcing is important, buyers can request relevant FSC, PEFC, or supplier chain-of-custody documentation. Brands should therefore evaluate the complete packaging structure rather than assuming that all brown kraft paper pouches automatically have a lower carbon footprint than conventional plastic or foil packaging.
Functional Performance Characteristics
Our brown kraft paper pouches can use multiple layers that work together to provide moisture, oxygen, aroma, grease, or light protection according to the product requirement. Actual shelf life depends on the barrier structure, product sensitivity, filling process, residual oxygen, storage temperature, and distribution conditions. Aluminum foil barriers can provide strong oxygen, moisture, and light protection for demanding applications such as specialty coffee or roasted nuts, while metallized films can provide useful barrier performance with a thin deposited metal layer. For oily products, the complete laminate should also be evaluated for grease resistance and resistance to oil migration or staining. Where grease-resistant paper treatments are used, the relevant food-contact and chemical-compliance requirements should be verified.
Design Flexibility and Market Positioning
Brown kraft paper pouches can be sealed and converted in a number of different ways depending on the product and the filling equipment. Resealable zipper closures can improve convenience after first opening, making them suitable for coffee, snacks, and other multi-use products. Degassing valves can allow carbon dioxide to escape from freshly roasted coffee while helping limit outside air ingress when properly selected and installed. Clear windows can also be incorporated using suitable transparent films, although the window area may reduce light or gas barrier compared with an opaque metallized or foil structure. These customization choices allow brands to differentiate their products while maintaining the natural appearance that makes kraft paper packaging appealing.
Structural Configurations for Different Applications
Stand-up pouches with gusseted bottoms can stand upright on retail shelves, improving presentation and accessibility. Flat-bottom pouches provide a more structured shape and multiple printable panels, making them suitable for premium products and larger fill weights when properly sized. Side gusset pouches provide additional internal volume and are commonly considered for coffee, tea, powders, and other products where efficient use of pack volume matters. Three-side seal pouches provide a flat, compact format and can be suitable for beef jerky, dried meat, samples, and other products where a simple pouch structure is appropriate. Each configuration meets different operational and presentation needs while allowing brands to maintain a consistent brown kraft paper look.
Procurement Insights: How to Source the Best Brown Kraft Paper Pouches for Your Brand

Critical Supplier Evaluation Criteria
To find trustworthy suppliers of brown kraft paper pouches, buyers should review food-contact documentation, quality management systems, packaging certifications, production capabilities, and technical support. At Guoshengli Packaging, we maintain ISO 9001 and BRCGS Packaging Materials certification together with food-contact compliance documentation for applicable target markets. With more than 25 years of experience in flexible packaging manufacturing, we support stable production processes intended to reduce common procurement risks such as inconsistent quality across repeat orders, production delays, and communication gaps. When adding new products or entering new markets, procurement teams should also confirm that suppliers can scale production while maintaining agreed specifications.
Price Benchmarking and MOQ Considerations
Brown kraft paper pouches may have minimum order quantities in the range of 20,000 to 50,000 pieces for some rotogravure projects, but the actual MOQ depends on pouch size, material structure, number of designs, printing method, and customization requirements. Digital printing can support lower quantities for selected short runs, test markets, or seasonal products, with lead times depending on artwork, material availability, and production schedule. Rotogravure printing can reproduce up to 11 colours and is generally more suitable for larger-volume production, with typical lead times determined by cylinder preparation, material structure, and factory scheduling. Different material structures also carry different cost profiles. Procurement teams should therefore evaluate total packaging value, including material performance, waste, production efficiency, and product protection, rather than comparing unit price alone.
Customization as Competitive Advantage
Customizing packaging can strongly influence shelf appearance and consumer perception. Our rotogravure printing can support consistent colour reproduction across suitable repeat runs when artwork, cylinders, inks, and process controls are properly managed. Matte kraft finishes can preserve a natural paper texture, while selected coatings or finishes can create different visual effects. Window arrangements can help show the product, although they should be evaluated against the required barrier performance. Private-label programmes can also help wholesalers and manufacturers serve different customer groups efficiently. To get the most value from the packaging investment, customization should match brand positioning, target-market expectations, filling requirements, and product-protection needs.
Regional Manufacturing Considerations
Buying from established Chinese manufacturers such as Guoshengli Packaging can provide access to integrated printing, laminating, slitting, and pouch-making capabilities. Our production base includes seven rotogravure printing machines, six laminating machines, six slitting machines, and 49 pouch-making machines, with annual production capacity of approximately 20,000 tons. This scale supports growing brands that require stable production planning and repeat supply. We maintain technical communication with customers in North America, Europe, and other export markets, and our long experience in international packaging projects helps us understand documentation, quality, and buyer expectations. When choosing a regional supplier, buyers should balance cost, quality consistency, lead time, communication, technical capability, and supply-chain reliability.
Implementing Brown Kraft Paper Pouches Effectively in Your Packaging Strategy
Storage and Handling Best Practices
Brown kraft paper pouches maintain their performance more reliably when stored correctly before filling. Pouches should be kept in a clean, dry environment away from direct sunlight, excessive heat, and high humidity, following the supplier's recommended storage conditions. Before shipment, pouches can be checked for seal quality, print accuracy, dimensions, and relevant material-performance requirements according to the agreed specification. Filling-line teams should also confirm that pouch dimensions, opening characteristics, seal areas, and material behaviour are compatible with the intended manual or automatic filling equipment to reduce production interruptions.
Addressing Moisture Resistance Concerns
Although kraft paper itself is more moisture-sensitive than many plastic films, multi-layer lamination systems can provide the required moisture and oxygen protection for suitable products. PE and CPP inner layers can provide food-contact heat-seal surfaces and moisture protection, while EVOH can provide high oxygen barrier in appropriately designed structures. Metallized PET can contribute oxygen, moisture, aroma, and light barrier depending on the laminate design. Brands packaging hygroscopic powders such as matcha, protein isolates, or supplement mixes can use high-barrier structures where necessary to help reduce moisture uptake, caking, and quality changes. Final performance should be validated against the actual product, target shelf life, storage conditions, and distribution route.
Real-World Performance Examples
Coffee roasters often choose brown kraft paper pouches to combine a natural visual identity with high-barrier laminates, resealable zippers, and optional degassing valves. Pet treat manufacturers may use the format where the natural appearance supports product positioning, provided puncture resistance, grease resistance, and barrier performance are matched to the actual product. Snack brands can also use brown kraft paper pouches to create a simple, premium, or artisanal shelf presentation while selecting the barrier structure independently according to product needs. These application examples show how the visual benefits of kraft paper can be combined with functional packaging design rather than relying on appearance alone.
Anticipating Future Packaging Trends
Interest in sustainable packaging continues to increase as brands, retailers, and regulators place greater emphasis on packaging minimisation, recyclability, recycled content, responsible sourcing, and end-of-life management. New barrier coatings, mono-material structures, fibre-based designs, and selected compostable materials are expanding the range of available packaging options, although their actual performance and disposal routes still require application-specific validation. Brands that use brown kraft paper pouches can position themselves for changing market expectations when the complete structure is selected responsibly and environmental claims are supported by appropriate evidence. Procurement professionals who follow these trends can make packaging decisions that balance brand value, performance, compliance, and long-term sustainability objectives.
Conclusion
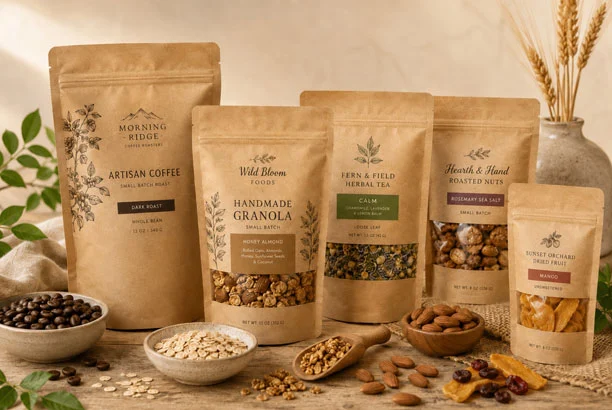
Brown kraft paper pouches offer brands a distinctive combination of natural appearance, flexible construction, and customizable product protection. Their kraft exterior can support premium, artisanal, or sustainability-oriented brand positioning, while functional laminate layers can be selected according to barrier, sealing, mechanical, and filling requirements. However, recyclability, compostability, shelf life, and environmental impact should be assessed from the complete finished structure rather than assumed from the presence of kraft paper alone. Successful implementation depends on selecting the right supplier, defining the appropriate barrier structure, validating filling compatibility, and making accurate environmental claims. At Guoshengli Packaging, our more than 25 years of flexible-packaging manufacturing experience helps procurement teams evaluate these choices for repeat production and changing market needs.
FAQ
1. Can Brown Kraft Paper Pouches Be Recycled?
It depends on the complete pouch structure. A brown kraft paper pouch laminated with PE, PET, metallized film, foil, adhesives, coatings, windows, or closures should not be assumed to be recyclable simply because the outer layer is paper. Fibre recovery, plastic content, adhesive system, pouch accessories, and local collection and recycling infrastructure all affect actual recyclability. Compostable structures are a separate category and should only carry compostability claims when the complete finished pouch meets the relevant certification and disposal requirements.
2. How Do These Pouches Handle Grease-Heavy Products?
Brown kraft paper pouches for grease-heavy products can be designed with inner laminate structures that help resist oil migration and staining of the outer paper layer. Performance depends on the complete material construction rather than the kraft paper alone. For products such as roasted nuts, beef jerky, and pet treats, the pouch should be evaluated for grease resistance, seal performance, and long-term compatibility with the actual product. Where grease-resistant paper treatments are used, the relevant food-contact and chemical-compliance requirements should also be confirmed.
3. What Shelf-Life Extension Can Be Expected?
The achievable shelf life depends on the product's sensitivity to oxygen, moisture, light, aroma loss, and grease, as well as the filling process, residual oxygen, storage conditions, and distribution route. Aluminum foil, metallized films, EVOH-containing structures, and standard PE-based laminates provide different levels of protection. The correct barrier should therefore be selected against the product's target shelf life, and the final shelf life should be validated with the actual product rather than estimated from the pouch material alone.
Partner with a Trusted Brown Kraft Paper Pouches Manufacturer
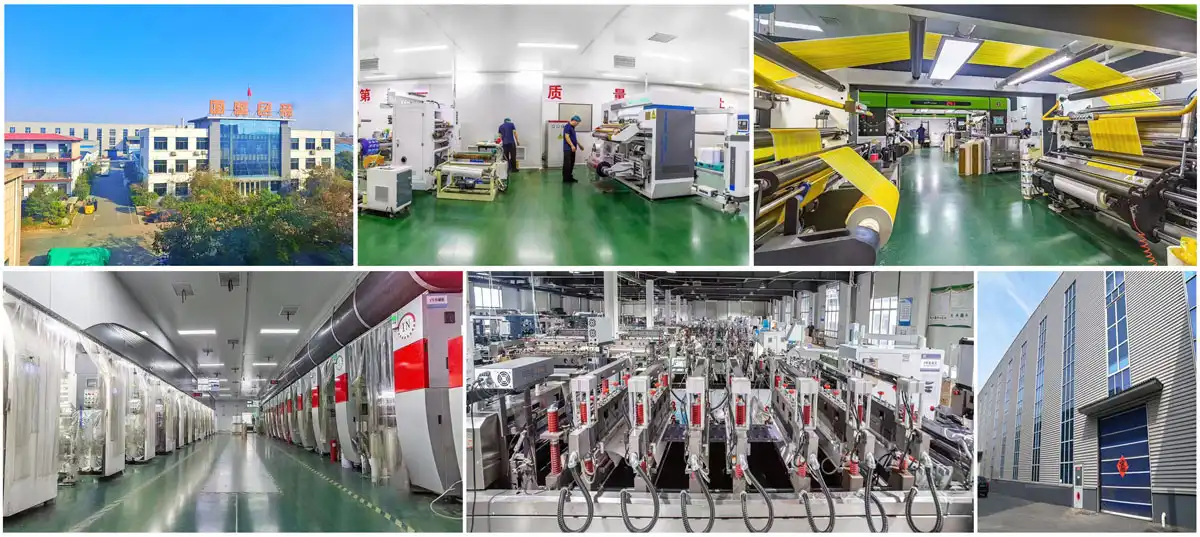
Guoshengli Packaging specializes in making custom brown kraft paper pouches for brands that need consistent quality, reliable delivery, and appropriate compliance support. Rotogravure printing in up to 11 colours, flexible barrier configurations, multiple pouch formats, and production capacity suitable for both one-time projects and long-term programmes are among the capabilities we provide. We work with brands in North America, Europe, Asia-Pacific, and other markets across food, pet care, coffee, and wellness categories. Our solutions are designed around repeatable production performance, product requirements, and target-market needs.
Email our technical team at sales@guoshengpacking.com to discuss your packaging requirements, request material recommendations, or ask for samples. Our integrated service includes pouch-format review, material selection, printing, laminating, and pouch making, helping simplify the procurement process and improve consistency from sampling through production.
References
-
Robertson, G. L. (2016). Food Packaging: Principles and Practice (3rd ed.). CRC Press.
-
Marsh, K., & Bugusu, B. (2007). Food Packaging—Roles, Materials, and Environmental Issues. Journal of Food Science, 72(3), R39–R55.
-
Yam, K. L. (2009). The Wiley Encyclopedia of Packaging Technology (3rd ed.). John Wiley & Sons.
-
Kirwan, M. J., & Strawbridge, J. W. (2003). Plastics in Food Packaging. In Food Packaging Technology (pp. 174–240). Blackwell Publishing.
-
Selke, S. E., Cutler, J. D., & Hernandez, R. J. (2004). Plastics Packaging: Properties, Processing, Applications, and Regulations (2nd ed.). Hanser Publishers.
-
Emblem, A., & Emblem, H. (2012). Packaging Technology: Fundamentals, Materials and Processes. Woodhead Publishing.
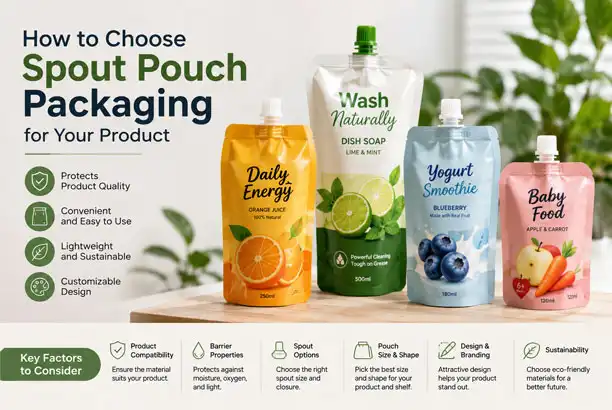
Choosing the right spout pouch packaging starts with understanding your product's specific requirements and matching them to the technical capabilities of the packaging solution. Spout pouch packaging combines a high-barrier laminated pouch with an integrated thermoplastic spout, offering controlled dispensing, excellent product protection, and logistical efficiency. This packaging format addresses critical B2B concerns including cost reduction, shelf-life extension, and brand differentiation across food, beverage, personal care, and industrial applications. Selecting the optimal solution requires evaluating material structures, barrier properties, spout specifications, supplier certifications, and compatibility with your existing filling equipment to ensure consistent performance throughout your supply chain.
Understanding Spout Pouch Packaging and Its Benefits
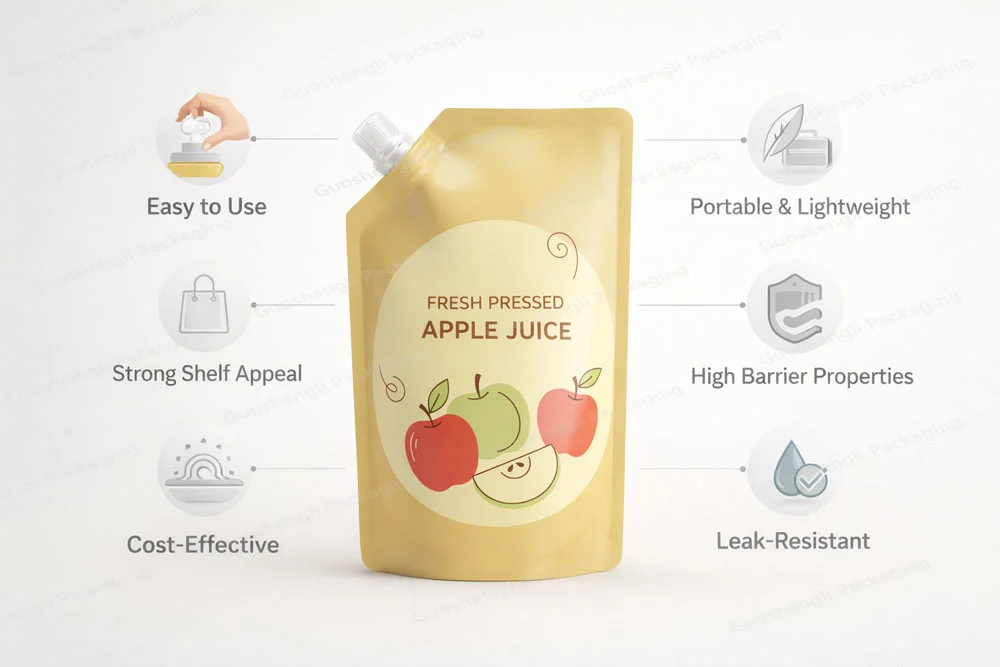
Spout pouch packaging is a complex type of flexible packaging that combines a multi-layer laminated bag with a stiff thermoplastic fitting. This mix makes a lightweight alternative to rigid containers that still protects products better and makes things easier for customers.
Definition and Core Functionality
The boxes are made of high-barrier films that are usually made up of PET, PA (Nylon), AL (Aluminum foil), and PE (Polyethylene) that are bonded together to meet certain barrier needs. The built-in spout, which comes in sizes from 8.5 mm to 33 mm, lets you control the pouring, and the structure itself keeps it in place on the shelf. With this design, customers can empty up to 99% of the goods, which means that almost no product waste happens.
Key Advantages for B2B Procurement
When purchasing managers look at flexible packaging with spouts, they see a number of strong advantages. Because empty pouches take up 90% less warehouse space than rigid containers, shipping costs go down by a lot. This improved storage efficiency directly leads to lower costs for keeping inventory and more efficient logistics operations.
High-barrier materials with very low Oxygen Transmission Rates (OTR) and Water Vapor Transmission Rates (WVTR) make products last longer. These technical requirements keep the integrity of the product by stopping moisture, oxidation, and contamination during distribution cycles. The reusable spout design keeps the food fresh even after it's been opened, which cuts down on customer complaints and returns.
Material Options and Sustainability Considerations
Standard multi-layer structures work really well as barriers, and new All-PE mono-material choices can really be recycled through city recycling systems. These structures can be recycled and keep their barrier properties with EVOH. This meets the needs of growing environmental regulations without lowering product safety.
RCPP (Retort Cast Polypropylene) inner layers allow hot-filling at temperatures between 85°C and 95°C and even retort sterilization at 121°C, which increases the number of ways that shelf-stable products can be used. The materials you choose have a direct effect on your sustainability story and how well you meet your corporate responsibility goals. This is a very important choice for putting yourself in the market in the long run.
Customization Capabilities for Brand Differentiation
The package style can handle rotogravure printing in up to 11 colors, which lets brands stand out on store shelves. Full-surface graphics and clear window screens make the packaging look good and let customers see how good the product is. This ability to customize helps brands stand out in markets with a lot of competition, where packaging is the main factor that makes people buy something at the point of sale.
Critical Criteria for Selecting Spout Pouch Packaging
To choose the right packaging, you need to carefully look at the product's features, the rules that apply, and the limitations of your business. To find solutions that work the same way every time, procurement teams have to weigh a lot of technical and business factors.
Product-Specific Requirements Assessment
The basic needs for packaging depend on its physical state. Liquid goods need protection that doesn't leak and spout sizes that match the thickness. For smooth pouring, thick soups need bigger holes (25–33 mm), while drinks work best with narrow holes (8.5–12 mm). Granular foods like salt and spices need materials that don't absorb water so they don't stick together while being stored or transported.
The volume needs affect the size of the pouch and how well it works with the filling line. Standard sizes range from 100ml to 5 liters, but custom sizes can be made for specific uses. Specifying the right number makes sure that the right amount of material is used and that production waste is kept to a minimum.
Barrier Properties and Sealing Reliability
Technical details are very important for keeping a product fresh. To make sure the barrier works, buyers should ask for written OTR and WVTR test results. Vacuum leak testing and burst pressure testing are objective ways to check the integrity of the seal and the strength of the structure under palletization loads.
The point where the spout meets the film is a key failure point. Ultrasonic welding or precise heat-sealing with special "W"-shaped sealing bars makes sure that the base of the spout melts evenly, which stops leaks during handling. Good providers test child-resistant caps for spout pressure to make sure they meet safety standards and can be used by the right people.
Regulatory Compliance and Certification Requirements
Materials that come into contact with food in spout pouch packaging must follow FDA and EU rules, which make sure that the chemicals are harmless and that harmful migrants are not present. Materials that don't contain BPA and liquid residue analysis (using Gas Chromatography) show that printing ink components can't get into goods. Certifications from ISO 9001, BRCGS, and SGS show that quality management and food safety rules are followed in a planned way.**
When a product is sold internationally, regulatory paperwork is very important. Full tracking from raw materials to produced goods helps purchasing teams meet audit standards and lowers the risk of not following the rules in many markets.
Cost Analysis and ROI Evaluation
Prices are different depending on the number of products ordered, the specifics of the materials, and how complicated the customization is. Flexible minimum order amounts let you test the market without having to commit to too much inventory. Instead of just looking at the unit price, people who work in procurement should look at the total cost of ownership, which includes things like savings on storage space, less money spent on freight, and fewer problems during transit.
Small price differences are less important than suppliers who are consistent over multiple orders. Poor quality causes filling lines to stop, shipments to be refused, and expensive production delays that quickly outweigh any initial savings from cheaper options.
Comparing Spout Pouch Packaging with Other Packaging Types
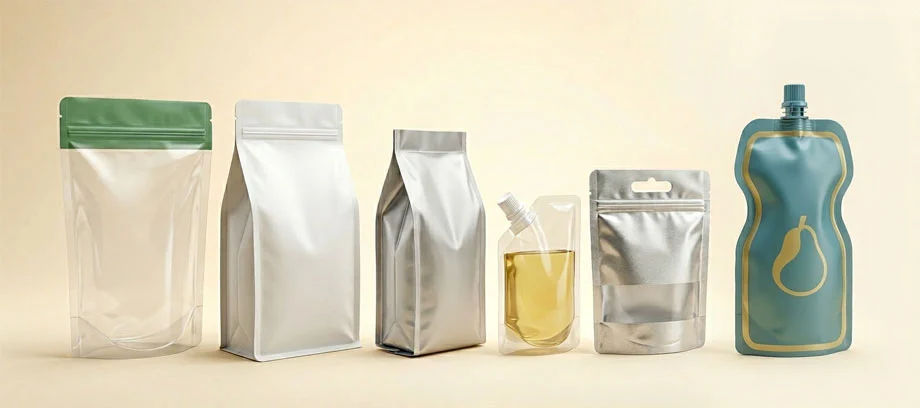
Procurement teams can make the best packaging choices for different uses and market conditions when they know when flexible pouches with spouts work better than other formats.
Spout Pouches Versus Stand-Up Pouches
Standard stand-up pouches without spouts are good for dry goods and one-time uses. Adding an opening makes the container more useful for liquids and semi-liquids and lets you close it again. The combined fitment increases unit costs by 15–25% but gives customers a much better experience with goods that need to be used for more than one thing. Controlled serving makes a big difference for drinks, sauces, and personal care products, so the extra money spent is well worth it.
Comparison with Rigid Bottles and Containers
Traditional plastic bottles and glass containers are easy for customers to use, but they are very hard to transport. When empty, rigid packaging weighs a lot more, which raises the cost of shipping each unit. The bigger volumetric footprint makes it more expensive to store and less efficient to ship.
Because of environmental concerns, open options are becoming more and more popular. Pouches use fewer raw materials to make the same amount of stuff, and they release less carbon dioxide over their whole life. The weight loss leads to real improvements in sustainability that support businesses' environmental goals and customers' preferences for brands that care about the environment.
Advantages Over Bag-in-Box Systems
Bag-in-box formats work well for large amounts of things like wine and industrial liquids, but they don't look good on store shelves. Pouches with spouts protect your goods like bag-in-box systems do, but they're also easy for customers to open and work well for smaller quantities. Because of this, spouted flexible packaging can be used in both store and food service without having to change its shape.
Transportation and Storage Efficiency Metrics
Quantitative comparisons show that there are big practical benefits. Empty bags can be stacked flat to make the best use of containers during incoming transport. Filled pouches fit better into shipping cartons than rigid bottles, so less void filling is needed and the pallet is more stable. Drop tests from normal heights (1.2m to 1.5m) show that the product is more resistant to impact, and spout-to-film welds that are properly sealed will stay intact during real-life handling accidents.
Selecting the Right Supplier and Ordering Guide
Long-term success in packaging depends more on the quality of the partnership than on the price at the start. By choosing makers with proven technical skills and quick customer service systems, you can keep quality problems and operating disruptions to a minimum.
Supplier Evaluation Criteria
Manufacturers with a good reputation show what they can do by having clear quality processes and written certifications for spout pouch packaging. ISO 9001 certification shows that the process is being controlled in a planned way, and BRC and FDA compliance show that the company knows how to keep food safe. Ask for facility audit records and customer examples to make sure that output stays the same for all orders.
Technical support is what sets capable suppliers apart from those who just take orders. Manufacturers should suggest materials based on the features of the product, a study of the filling process, and tests to see if they work with the tools you already have. Having access to applications engineering experts helps fix problems before they affect production.
Customization and Specification Process
Costly mistakes can be avoided by developing detailed specifications. Tell them about the product's pH levels, stickiness, temperature during filling, and how long it needs to be kept. Instead of using subjective language to describe size requirements, spout diameter preferences, barrier targets, and printing expectations, use measurable parameters instead.
For confirmation, pre-production sampling is still necessary. Fill testing can be done on real equipment with physical samples, which can show any interface problems before full production runs are committed to. During the sample process, you should check the color matching, print quality, and sealing performance.
Minimum Order Quantities and Lead Times
MOQs vary by pouch size, spout type, printing process and material structure. Digital printing may support smaller trial quantities, while gravure-printed orders commonly require higher volumes.. For testing the market, digital printing allows for faster runs (7–10 day lead times), while rotogravure printing provides better color stability for large-scale production (15–20 day lead times). Knowing these factors helps procurement teams balance the risk of having too much inventory with the efficiency of production.
Filling Equipment Compatibility
To make implementation work, the company that makes the packaging and the company that makes the filling equipment need to work together. Vertical form-fill-seal (VFFS) machines, pre-made pouch filling systems, and manual filling stations can all be used with spout pouch packaging, depending on the amount of work that needs to be done. To make sure that their products fit well with current lines, suppliers should include technical details like pouch tolerances, fitting measurements, and sealing parameters.
Best Practices for Handling and Maintaining Spout Pouch Packaging
When you store, handle, and check the quality of your packaging the right way, it works better and causes fewer problems in the production chain.
Storage Conditions and Shelf Life
When not in use, bags should be kept in climate-controlled areas where the temperature is between 15°C and 25°C and the relative humidity is less than 60%. Too much heat can weaken glue ties in laminated structures, and too much humidity can make seals less reliable. Pouches should stay in their original boxes until they are ready to be used. This will keep them safe from dust, light, and damage caused by handling.
Inventory rotation using first-in, first-out (FIFO) makes sure that bags are used within the time frames that are suggested. When stored properly, most flexible packaging keeps working at its best for 12 to 18 months, though specific instructions depend on the material structure.
Sealing Techniques and Quality Verification
The safety and shelf life of a product are directly affected by the right sealing parameters. Temperatures, dwell times, and pressure settings for heat seals must be set according to the material specs given by the package maker. Regular quality checks of the seals, which include measuring the peel strength and looking at them visually, find problems before they affect a lot of seals.
Operators should check full bags to make sure the spout is lined up correctly, the seal is complete, and there are no wrinkles or other problems in the seal areas. Using statistical process control and keeping track of how often inspections are done makes sure that quality standards are the same between shifts.
Common Defects and Troubleshooting
Leakage at the points where the spouts meet usually means that the welding pressure is too low or the temperature settings are wrong. Weak seals may result from contamination, incorrect sealing parameters, material variation, misalignment or worn sealing components. Most of the time, sharp edges on filling tools or bad "head-to-tail" packing arrangements in shipping boxes cause holes to form during handling.
To solve these problems, we need to do a systematic root cause analysis instead of making changes on the fly. Keeping detailed records of output makes it possible to find patterns and take preventative and corrective actions that make tools work better overall.
Contamination Prevention Protocols
Keeping things clean during the filling process is important for making sure the products are safe. Cross-contamination is avoided by cleaning the filling tools, conveyor systems, and equipment used to handle pouches on a regular basis. When operators are trained in the right way to handle materials, foreign materials are introduced less during changeovers and normal production.
Conclusion
When choosing the right spout pouch packaging, you need to find a balance between technical performance, cost-effectiveness, and source dependability. The style has many great benefits, such as lower transportation costs, longer shelf life thanks to high-barrier materials, and easier access for customers. To make implementation work, you need to carefully look at what the product needs to do, make sure that the materials are right for the job, and work with manufacturers who provide consistent quality and quick technical support. Professionals in purchasing who carefully consider suppliers based on their certifications, output skills, and prospects for long-term teamwork give their companies a long-term edge in markets that are becoming more competitive.
FAQ
1. What advantages do spout pouches offer compared to rigid bottles?
Because they are lighter and take up less room, flexible pouches with built-in spouts cut shipping costs by 40 to 60 percent. They let people get rid of 99% of the contents, compared to 85-70% with bottles, which cuts down on waste. The format supports efforts to be more environmentally friendly by using buildings made of a single material that can be recycled. It also has great barrier qualities.
2. Can customization accommodate specific branding requirements?
Advanced rotogravure printing can make pictures in up to 11 colors, and the colors stay the same across production runs. Positioning clear window panels in a certain way can show off the quality of a product. Differentiation options like matte or glossy finishes, specialty coatings, and custom shapes make it easier for people to recognize your brand at retail.
3. How does packaging comply with food safety standards?
Reputable manufacturers offer materials that meet FDA and EU rules for food contact and come with full documentation of their chemical inertness. A study of the solvent residue shows that printer paints don't pose any migration risks. ISO 9001 and BRC certifications show that quality control is carried out in a planned way throughout production.
Partner with Guoshengli Packaging for Reliable Spout Pouch Solutions
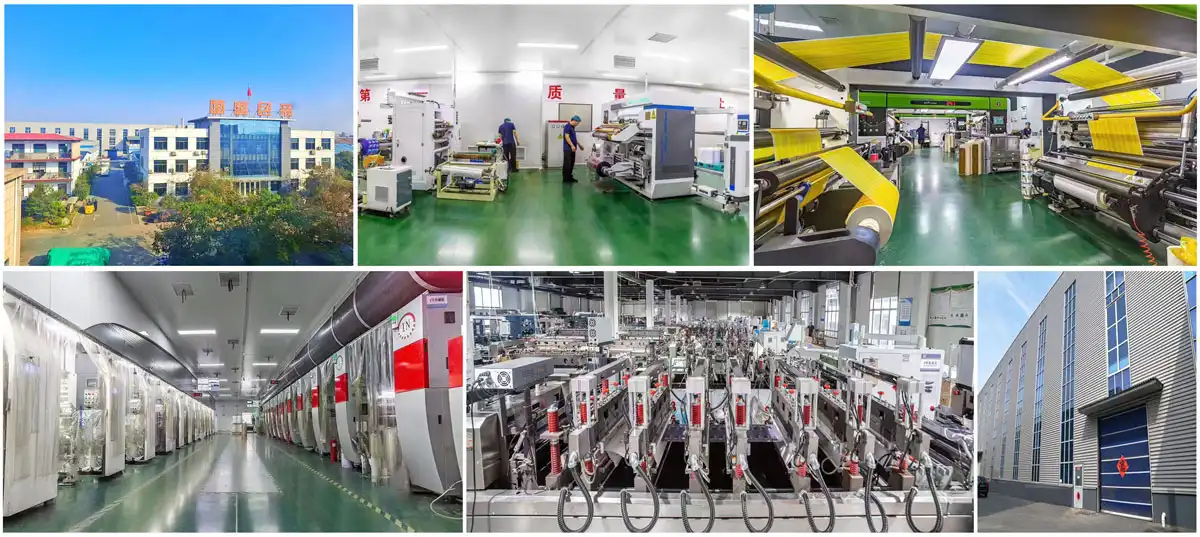
Guoshengli Packaging has been making flexible packaging for 25 years and can help brands avoid expensive production problems and inconsistent quality. As a reliable spout pouch packaging supplier, we offer factory-direct solutions with 7 specialized printing lines, 6 laminating machines, and 49 converting machines. This way, we can guarantee the same high quality for all repeat orders. Our ISO 9001, BRC, FDA, and SGS certifications show that we follow the rules for selling in foreign markets. Whether you need buildings made of a single material that can be recycled, RCPP options that can be hot-filled, or fast digital printing in 7–10 days, our expert team can help you with everything, from choosing the material to integrating it into production. Email our application engineers at sales@guoshengpacking.com to talk about your unique needs and get full technical specifications that are made to fit your product and filling equipment.
References
1. Robertson, G.L. (2016). Food Packaging: Principles and Practice (3rd Edition). CRC Press, Boca Raton, Florida.
2. Marsh, K. & Bugusu, B. (2007). Food Packaging—Roles, Materials, and Environmental Issues. Journal of Food Science, Vol. 72, Issue 3, pp. R39-R55.
3. Yam, K.L. (2009). The Wiley Encyclopedia of Packaging Technology (3rd Edition). John Wiley & Sons, Hoboken, New Jersey.
4. Coles, R., McDowell, D. & Kirwan, M.J. (2003). Food Packaging Technology. Blackwell Publishing, Oxford, United Kingdom.
5. Soroka, W. (2009). Fundamentals of Packaging Technology (4th Edition). Institute of Packaging Professionals, Naperville, Illinois.
6. Selke, S.E.M., Culter, J.D. & Hernandez, R.J. (2004). Plastics Packaging: Properties, Processing, Applications, and Regulations (2nd Edition). Hanser Publications, Munich, Germany.
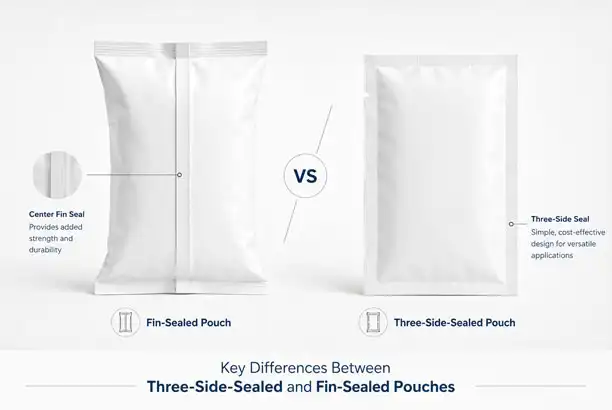
Choosing between Three Side Sealed and fin-sealed pouches can significantly impact your product presentation, filling efficiency, material use, and overall packaging costs. A fin seal pouch uses a longitudinal back seal where the inner sealant surfaces bond together, typically forming a raised "fin" on the back of a pillow-style pack. Three Side Sealed pouches, by contrast, are flat pouches with three sides sealed during converting and one side left open for filling before the final seal is made. Both formats serve important roles in B2B packaging, yet understanding their core differences helps procurement managers select the option that best aligns with product requirements, filling line compatibility, and market expectations.
Introduction
Flexible packaging impacts shelf life, production speed, shipping costs, and brand impression in today's competitive B2B market. Procurement managers, OEMs, and packaging buyers are working to protect products, control costs, meet regulatory requirements, and respond to sustainability expectations. Two common packaging formats are Three Side Sealed and fin-seal pouches. Each has advantages depending on the product, filling equipment, material structure, and market.
Buying teams can compare pouch construction, function, and pricing using this guidance. We examine seal placement, barrier requirements, customisation options, and total cost of ownership. Understanding these factors can help buyers reduce supply chain risks, improve product presentation, and make more informed decisions. This comparison will help you evaluate suitable packaging for snacks, pet treats, vitamins, household products, and other applications based on actual product and production requirements.
Understanding Three Side Sealed and Fin-Sealed Pouches
What Is a Three Side Sealed Pouch?
A Three Side Sealed pouch is a flat pouch with three sides sealed during pouch converting and one side left open for filling. After the product is filled, the remaining opening is heat sealed. Depending on the manufacturing method, the pouch may be produced from a folded film web or from separate film webs. This arrangement creates a flat, clean profile that works well for products requiring a uniform presentation and clearly defined front and back artwork areas. Three Side Sealed bags are often used in cosmetics, pharmaceuticals, food products, and other applications where compact packaging and shelf presentation are important. The structure also makes it possible to add features such as tear notches, euro holes, and selected resealable closures.
To achieve the required barrier performance, the pouch may use multilayer structures containing materials such as PET, metallised film, aluminium foil, PA, EVOH, PE, or CPP depending on the application. Three Side Sealed pouches can be produced in a wide range of sizes and material structures. They may be supplied as pre-made pouches or produced in suitable form-fill-seal configurations, depending on the equipment and package design. Because of this flexibility, they are widely used by brands that need consistent pouch appearance across different product formats and production volumes.
What Is a Fin Seal Pouch?
Fin seal bags are commonly produced from a continuous film web that is wrapped or folded around the product-forming area and sealed longitudinally at the back. The inner sealant surfaces are bonded together to create the raised "fin" associated with many pillow-style or back-seal packs. This seal configuration is widely used on vertical and horizontal form-fill-seal lines because it allows efficient continuous package formation.
Guoshengli Packaging provides multi-layer laminated fin seal pouches designed around the required barrier, mechanical, printing, and sealing performance. PET, matte PET, or BOPP may be used as outer layers for printability and surface performance. Depending on the product requirements, intermediate layers may include PA for toughness and puncture resistance, metallised PET or aluminium foil for additional barrier and light protection, or EVOH for enhanced oxygen barrier. PE, CPP, or suitable recyclable PE-based sealant layers may be used to provide heat-sealing performance for food packaging. Full-colour rotogravure printing with up to 11 colours is available for selected projects.
Fin seal formats are widely used for coffee, snacks, candies, frozen goods, pet treats, powders, and other products. Their continuous-web construction can support efficient material handling and high-speed production on compatible filling lines. Depending on the package design and equipment, features such as clear windows, euro holes, easy-tear notches, and selected resealable systems may also be incorporated.
Core Differences Between Three Side Sealed and Fin-Sealed Pouches
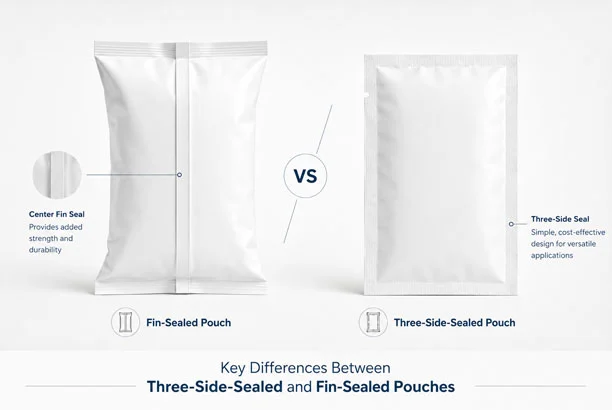
Structural Design and Seal Placement
These pouches differ mainly in seal location and package construction. Three Side Sealed pouches have three edges sealed during pouch converting, leaving one side open for filling before the final heat seal. Their flat construction provides clearly defined front and back panels and can support compact stacking, display, and storage. The absence of a longitudinal back fin also gives designers a clean rear panel for branding, product information, or regulatory copy.
Fin seal pouches use a longitudinal back seal formed by joining the inner sealant surfaces of the film. This seal runs along the rear of the pack and is combined with transverse seals to create a pillow-style package. The sealant-to-sealant configuration is practical for many form-fill-seal applications and can provide reliable sealing when the material structure, seal geometry, temperature, pressure, dwell time, and contamination control are correctly matched to the product and machine.
Material Compatibility and Manufacturing Methods
Three Side Sealed pouches can be produced from folded film or multiple webs depending on the converting process. This gives manufacturers flexibility in selecting laminated structures for the required barrier, mechanical, print, and sealing performance. Three Side Sealed formats can be made using foil, metallised laminates, paper-containing structures, high-barrier films, and suitable mono-material structures when validated for the application.
Fin seal pouches are commonly produced from a continuous film web, which can simplify web handling and package formation on compatible form-fill-seal equipment. Material selection still depends on the product and process rather than the seal format alone. PA may be used where additional toughness or puncture resistance is required, while EVOH, metallised layers, aluminium foil, or other barrier technologies may be selected where additional oxygen, moisture, aroma, or light protection is needed. Mono-PE or mono-PP structures may also be considered where recyclability objectives and machine requirements justify their use.
Multi-layer laminates are available from Guoshengli Packaging for both pouch formats. Material selection can be based on factors such as tensile and puncture performance, seal compatibility, oxygen transmission rate, water vapour transmission rate, light protection, filling conditions, and intended shelf life.
Printing Techniques and Branding Opportunities
Both pouches can support high-quality rotogravure and digital printing, although seal placement affects artwork layout and usable panel areas. Three Side Sealed pouches provide flat front and back panels that can accommodate branding, product photography, nutrition information, ingredients, and regulatory copy. Their flat construction makes artwork planning straightforward, particularly when a clean front-and-back presentation is required.
Fin seal pouches also support full-colour printing across the available web area, with the rear fin and seal zones considered during artwork development. Brands can use the remaining front, back, and side areas for graphics, product information, and selected transparent windows. Glossy, matte, metallic, and soft-touch finishes may be used where compatible with the chosen structure and process.
Rotogravure printing can reproduce up to 11 colours on suitable production runs, while digital printing can support shorter runs, prototypes, multiple designs, and market tests without conventional printing cylinders. The appropriate printing method depends on quantity, artwork complexity, number of SKUs, cost target, and production schedule.
Barrier Protection and Resealability
Barrier performance influences shelf life, product quality, and customer satisfaction, but it is determined primarily by the material structure, package integrity, seal quality, and product requirements rather than by pouch style alone. Three Side Sealed bags can achieve high oxygen, moisture, aroma, or light barrier performance when produced with an appropriate laminate and properly sealed. Seal integrity should be validated using the intended product, filling conditions, and heat-sealing parameters.
Fin seal pouches can also provide high barrier performance when the correct laminate and sealing system are used. The sealant-to-sealant longitudinal fin seal is widely used in form-fill-seal packaging because it provides a practical and repeatable sealing interface. Applications such as coffee, nuts, dried fruits, and powdered products may also use nitrogen flushing or modified-atmosphere packaging when appropriate, but the final package performance depends on the complete material, sealing, filling, and gas-management system.
Both pouch formats may incorporate selected resealable features such as press-to-close zippers or other closure systems, depending on the package design and filling equipment. Resealable features can improve convenience for snacks, pet food, supplements, and other multi-use products. Compatibility should be confirmed during pouch and line trials so that the closure does not interfere with forming, filling, sealing, or final pack integrity.
Comparison of Three Side Sealed and Fin-Sealed Pouches for Procurement Decisions
Performance Under Logistics and Storage Conditions
Procurement teams need to consider packaging durability during transportation and storage. The flat profile of Three Side Sealed bags can support compact storage and efficient carton packing in many applications. Their suitability for handling depends on the pouch dimensions, material structure, fill volume, product geometry, and seal design rather than symmetry alone.
Fin seal pouches are typically pillow-shaped and may use carton space differently depending on product volume and pack geometry. Their continuous-web construction can be advantageous on compatible automated lines. For products with sharp, rigid, or irregular edges, puncture resistance should be engineered through the material structure and validated using the actual filled product rather than assumed from the pouch format.
Both technologies can perform effectively under normal logistics conditions when the material structure, seal design, and package dimensions are properly specified. Temperature, humidity, product movement, drop impact, and mechanical stress should be considered during package validation. Guoshengli Packaging can test seal, tensile, barrier, and other relevant performance characteristics according to the agreed specification.
Cost Comparisons and Customization Options
In B2B packaging, setup, tooling, printing, material use, order quantity, converting speed, filling-line efficiency, and waste all contribute to total packaging cost. Neither Three Side Sealed nor fin seal pouches are automatically cheaper in every application. Pre-made Three Side Sealed pouches can be economical for many flat-pack applications, while fin seal formats can offer efficient film use and high productivity on suitable form-fill-seal equipment.
Fin seal pouches can be cost-effective on high-volume lines because they are commonly formed from a continuous web and integrated directly into the filling process. However, actual cost depends on pouch dimensions, material structure, printing method, production volume, features, machine speed, and waste rate. Minimum order quantities also vary by specification. Rotogravure is generally more suitable for larger runs, while digital printing may support lower quantities for selected projects.
Euro holes, tear notches, selected zipper systems, and clear windows may be added to both pouch formats depending on the structure and equipment. Both can also vary in size, barrier construction, printing process, surface treatment, and other functional features. Our team can work with clients from material selection and artwork review through sampling and production to balance performance, branding, cost, and manufacturing requirements.
Eco-Friendly Materials and Recycling Considerations
Sustainability is becoming increasingly important in B2B procurement due to legislation, customer expectations, and corporate environmental goals. Recyclable, compostable, recycled-content, and bio-based packaging represent different environmental strategies and should not be treated as interchangeable claims. The end-of-life performance of a Three Side Sealed or fin-seal pouch depends on its complete material construction and the relevant collection, sorting, recycling, or composting system.
Both pouch formats may use mono-PE or mono-PP structures where these materials can meet the required product-protection and filling-line performance. Mono-material design can improve compatibility with suitable polyolefin recycling processes, but it does not automatically guarantee recyclability in every market. Barrier layers, coatings, inks, adhesives, closures, labels, and other components should be considered when evaluating the complete finished package.
Guoshengli Packaging can also evaluate selected PLA/PBAT-based compostable structures and recyclable mono-PE solutions where the product, target market, certification requirements, and end-of-life route justify their use. Compostable materials should be selected only where an appropriate composting pathway and claim basis exist. Our RTO exhaust-gas treatment system supports lower-emission production operations, while material recommendations focus on balancing environmental objectives with packaging performance.
Choosing the Right Pouch: Practical Guidelines for B2B Buyers
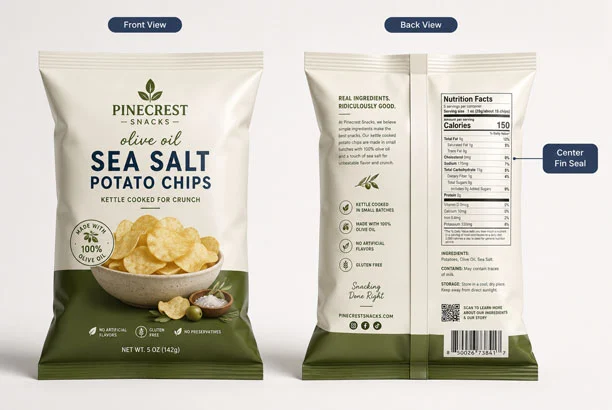
Matching Pouch Type to Product Requirements
First, understand the product characteristics and packaging requirements before selecting a pouch style. Fin seal pouches can be an efficient option for products packed on compatible form-fill-seal equipment, including coffee, powdered products, snacks, and pet treats. Product protection should still be determined by the laminate structure, seal quality, filling method, and required shelf life rather than by the back-seal format itself.
Cosmetics, single-serve snacks, pharmaceutical products, and other flat-pack applications may benefit from Three Side Sealed bags because of their clean front and back panels, compact shape, and flexible presentation options. The flat format can make it easier to organise branding, product photography, ingredients, instructions, and regulatory information.
Filling-line compatibility is another crucial factor. Fin seal pouches are widely used on VFFS and HFFS systems where continuous package formation and production speed are important. Three Side Sealed pouches may be used as pre-made pouches or in suitable form-fill-seal configurations depending on the equipment. To reduce integration problems, buyers should evaluate pouch style together with machine type, filling method, seal geometry, production speed, and expected volume.
Vetting Suppliers Based on Certifications and OEM Capabilities
Choosing the right supplier is important for reducing supply chain risk and maintaining consistent packaging performance. Procurement teams should consider manufacturers with appropriate quality and packaging-management certifications, such as ISO 9001 and BRCGS Packaging Materials, together with food-contact compliance documentation suitable for the intended market. For products sold in the United States, food-contact materials should comply with applicable FDA regulatory requirements rather than being described simply as "FDA-certified."
OEM capabilities such as in-house design support, material engineering, printing, laminating, slitting, and pouch-making can help suppliers provide more integrated solutions and respond efficiently to changing requirements. Guoshengli Packaging has more than 25 years of flexible-packaging manufacturing experience and annual production capacity of approximately 20,000 tons. We support customers ranging from emerging brands to larger international programmes. Our quality-management and packaging certifications support consistent production and documentation for international customers.
Good communication and technical capability are equally important. Suppliers should be able to provide material specifications, relevant barrier data, production tolerances, lead times, and transparent cost information. Sampling, testing, and responsive production support can help buyers avoid specification errors and reduce delays during product launches.
Tips on Customization for Brand Differentiation
Customisation can improve brand recognition while adapting the pouch to the product, filling process, and retail presentation. Buyers can modify pouch dimensions, shape, artwork, and functional features according to fill weight, product volume, machine requirements, and display needs. High-resolution rotogravure printing with up to 11 colours can reproduce detailed graphics and product information for suitable production runs.
Clear windows, euro holes, tear notches, and selected resealable closures can improve functionality and presentation. Clear windows may help customers view products such as snacks, confectionery, or pet treats. Euro holes support hanging display, while tear notches and resealable features may improve opening and repeated use where appropriate.
Metallic, glossy, matte, and soft-touch finishes can create different shelf effects, provided they are compatible with the selected material and printing process. Guoshengli Packaging works with customers to develop solutions that balance cost, functionality, manufacturability, and visual impact so that the finished package performs consistently under real production and distribution conditions.
Future Trends and Innovations in Pouch Packaging
Emerging Materials and Advanced Barrier Technologies
Sustainability and changing market requirements continue to drive development in flexible-packaging materials and barrier technologies. Recyclable mono-material laminates are receiving greater attention, but their suitability still depends on whether they can meet the required barrier, sealing, mechanical, and machine-performance specifications. Transparent barrier technologies such as aluminium oxide (AlOx) and silicon oxide (SiOx) coatings can improve oxygen or moisture protection in selected film structures, although actual performance depends on the substrate, coating system, converting process, flex resistance, and intended application.
PLA, PBAT, and other bio-based or compostable materials are also being evaluated in selected applications. These materials should not be assumed to provide the same end-of-life route or performance as recyclable polyolefin packaging. Buyers need to review certification requirements, composting infrastructure, mechanical properties, barrier performance, and filling-equipment compatibility before selecting them.
Guoshengli Packaging continues to evaluate new materials and packaging technologies that may support both functional and environmental objectives. Recyclable mono-PE structures, selected compostable solutions, and other new material developments are assessed against product protection, filling-line compatibility, manufacturing requirements, and the intended target market.
Digital Printing Technologies for Cost-Effective Customization
Flexible packaging can now be produced in shorter quantities and with greater artwork flexibility through digital printing. Unlike rotogravure, digital printing does not require conventional printing cylinders, which can reduce setup requirements for selected short-run projects. This makes it useful for market tests, seasonal products, multiple SKUs, prototypes, and emerging brands.
Digital printing can also support variable data and artwork changes across selected projects, making it useful for personalised packaging, regional versions, and short-run design variation. Improvements in digital print quality and productivity continue to expand the range of applications where it can be commercially practical, although rotogravure remains highly suitable for many larger-volume jobs.
We provide both rotogravure and digital printing so customers can select the appropriate process according to production volume, artwork requirements, cost, and time to market. Digital printing can support flexible short-run development, while rotogravure can provide efficient repeat production and high colour consistency at larger volumes.
Shifting Market Demands and Supplier Adaptation
The global B2B packaging market is moving toward greater sustainability, traceability, supply-chain resilience, and technical transparency. Buyers increasingly expect suppliers to provide clear material information, relevant compliance documentation, consistent quality, and realistic sustainability guidance. In response, manufacturers are investing in recyclable structures, production efficiency, waste reduction, and improved quality-management systems.
Flexible-packaging production is also benefiting from increasing automation and data-based manufacturing control. Online inspection, process monitoring, maintenance systems, and digital production records can improve consistency and help identify waste or quality problems earlier. The actual level of automation varies by factory and production process, but these technologies can support more stable manufacturing and faster quality response.
Guoshengli Packaging continues to improve manufacturing systems, production responsibility, and long-term customer support. Brands looking for reliable fin seal pouch solutions can work with us to evaluate packaging according to product requirements, material performance, production volume, and filling-line conditions rather than relying on one pouch format as a universal solution.
Conclusion
Choosing between Three Side Sealed and fin seal pouches requires consideration of product characteristics, filling-line compatibility, branding objectives, material requirements, and total packaging cost. Three Side Sealed pouches provide a flat format with clean front and back panels and can suit products that benefit from compact presentation and defined artwork areas. Fin seal pouches are widely used on high-speed form-fill-seal lines and can provide efficient continuous package formation when matched to the correct material and equipment.
Neither format automatically provides superior barrier protection, seal strength, puncture resistance, recyclability, or lower cost in every application. These performance characteristics depend on the laminate structure, sealant system, dimensions, converting process, filling conditions, and distribution requirements. Understanding the structural and production differences between the two formats helps procurement managers reduce supply-chain risks, improve product presentation, and select a specification that works reliably in production. Partnering with an experienced packaging manufacturer can also help buyers validate material, filling, printing, and compliance requirements before full-scale production.
FAQ
1. Can Fin Seal Pouches Be Made Resealable?
Yes, selected fin seal formats can incorporate press-to-close zippers or other resealable systems. However, compatibility depends on the pouch design, zipper construction, material structure, and filling equipment. Adding a resealable feature can affect converting complexity, sealing conditions, machine setup, and production speed, so it should be validated before full production. At Guoshengli Packaging, we can evaluate resealable options for snack, pet food, supplement, and other applications based on the intended filling process and pack design.
2. What Are the Minimum Order Quantities for Custom Fin Seal Pouches?
The minimum order quantity depends on the printing method, material structure, pouch dimensions, number of designs, and level of customization. Rotogravure printing is generally more suitable for larger production runs because cylinder setup costs are distributed across the order volume. Digital printing can support lower quantities for selected projects, making it useful for market testing, new brands, seasonal products, or multiple SKUs. Guoshengli Packaging can help buyers compare printing and production routes according to order volume, lead-time requirements, and customization needs.
3. How Do Fin Seal Pouches Compare to Stand-Up Pouches in Durability?
When correctly designed, both formats can provide strong mechanical and seal performance, but neither is automatically more durable. Stand-up pouches use a bottom gusset to create a self-standing format for retail presentation, while fin seal pouches are commonly used in pillow-style packaging on high-speed form-fill-seal lines. Durability depends on material structure, thickness, seal design, product geometry, filling conditions, and distribution stress. The final choice should therefore be based on the product, display requirement, packaging equipment, and validated package performance.
Partner with Guoshengli Packaging for Your Custom Fin Seal Pouch Solutions
Ready to optimise your packaging performance and reduce supply-chain risk? Guoshengli Packaging has more than 25 years of flexible-packaging manufacturing experience and produces custom fin seal pouches for food, snacks, pet treats, supplements, and other applications. Our manufacturing and quality systems include ISO 9001 and BRCGS Packaging Materials certification, together with food-contact compliance support for applicable target markets. Material structures, printing methods, barrier requirements, and functional features can be customised according to the product and filling process.
We also support rotogravure and digital printing, recyclable material development, sampling, and production trials. MOQ and lead time depend on pouch size, material structure, printing method, number of designs, and required features, so our team can recommend a suitable production route for both new launches and repeat programmes.
You can email our team at sales@guoshengpacking.com to request samples, discuss your project requirements, or review our flexible-packaging options. We support both ongoing production programmes and new product launches with material recommendations, artwork review, sampling, and production planning.
References
Robertson, G. L. (2016). Food Packaging: Principles and Practice (3rd ed.). CRC Press.
Marsh, K., & Bugusu, B. (2007). Food Packaging—Roles, Materials, and Environmental Issues. Journal of Food Science, 72(3), R39–R55.
Selke, S. E., Cutler, J. D., & Hernandez, R. J. (2004). Plastics Packaging: Properties, Processing, Applications, and Regulations (2nd ed.). Hanser Publications.
Yam, K. L. (2009). The Wiley Encyclopedia of Packaging Technology (3rd ed.). Wiley-Interscience.
Kirwan, M. J., & Strawbridge, J. W. (2003). Plastics in Food Packaging. In Food Packaging Technology (pp. 174–240). Blackwell Publishing.
Coles, R., McDowell, D., & Kirwan, M. J. (2003). Food Packaging Technology. Blackwell Publishing.
CEFLEX. Designing for a Circular Economy: Design Choices and Design Principles for Flexible Packaging. Current guidance for recyclable flexible-packaging structures.
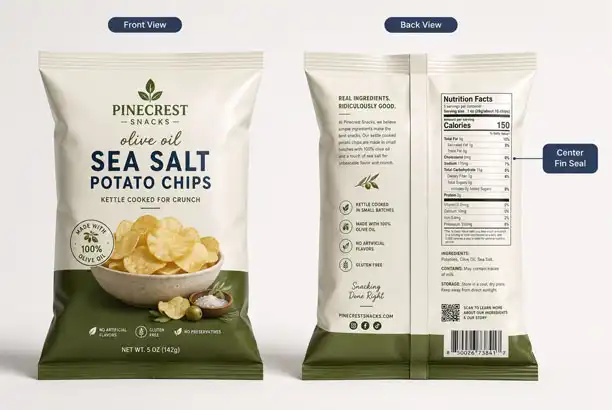
Choosing the right packaging format can determine whether your product succeeds or struggles on retail shelves. A fin seal pouch offers a combination of robust protection, operational efficiency, and brand-building potential that makes it a go-to solution across food, pet care, supplement, and beverage industries. This versatile pillow-style package features a distinctive back seal resembling a fin, delivering hermetic protection against moisture, oxygen, and contaminants. Whether you're launching a new snack line, scaling pet treat production, or optimizing filling operations, understanding how this packaging format works will help you make informed procurement decisions that protect product quality and reduce costs.
What Is a Fin Seal Pouch and How Does It Work?
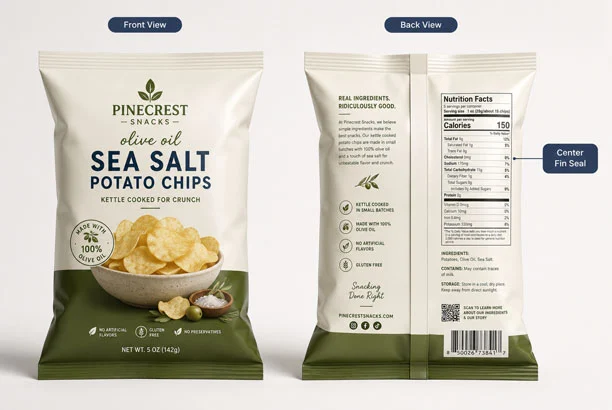
Understanding the Fin Seal Structure
You can make a fin seal pouch, which is also known as a pillow pouch or T-seal pouch, by folding a flexible film lengthwise and closing the backs of the inside sides together. This process makes a "fin" that sticks out from the back wall. When the top and bottom are heated together, they form a seal that keeps the package inside. When you use a lap seal, the outer and inner layers have to stick together. But with the fin seal method, the interior areas are all the same, so the barrier is stronger and it works with high-barrier materials.
Manufacturing Process and Technology
Rotogravure or digital printing on layered laminate films is the first step in the production process. The material is cured to make the sticky ties stronger after it has been printed and laminated. The film is then cut to the right width and put into tools that do vertical form-fill-seal (VFFS) or horizontal form-fill-seal (HFFS). At very high speeds, these machines fold the film, make the fin seal along the back, put the product inside the pouch, and seal the top and bottom. The advanced sealing jaws control the dwell time and pressure to keep the seal strength constant, even at the thicker T-junctions where three layers meet.
Types of Fin Seal Configurations
Fin seal pouches can be put together in different ways to meet different needs. Seals with a flat fin work well for dry goods like snacks and candy. Angled fin seals make the product more stable and look better on the shelf. Some designs have gussets to add extra volume or euro holes for hanging displays in stores. Customers can see right away if a product is still fresh with transparent window choices. This is especially useful in markets for sweets and unique foods.
Why Structural Design Matters for Procurement
Knowing about these structural aspects helps buying teams decide if a fin seal pouch meets certain business needs. The risk of delamination is lower with the interior-to-interior seal method than with other forms. When something works with automatic filling lines, it means that it can be used more quickly and with less labor. Machine changes and downtime are kept to a minimum when pouch measurements stay the same. For buyers handling just-in-time inventory systems, this means stable production plans and expected wait times.
Key Benefits and Uses of Fin Seal Pouches in Packaging
Selecting packaging involves balancing product protection, operational efficiency, and cost control. Fin seal pouches deliver measurable advantages across all three areas, making them a practical choice for diverse industries.
Superior Seal Integrity and Product Protection
High-barrier multilayer laminates stop light, air, and wetness from getting through, which are the three main things that hurt the quality of a product. You can change the oxygen transmission rates (OTR) and water vapor transmission rates (WVTR) by choosing the right material. This lets sensitive products like roasted coffee, protein powders, and pet treats last longer on the shelf. The airtight seal keeps food from getting contaminated while it's being shipped or stored. This cuts down on spoilage-related returns and protects the brand's image.
Operational Efficiency and Cost Savings
The cost of packing each unit goes down when it works with high-speed VFFS and HFFS tools. Waste is cut down by making good use of materials, and lead times are shortened by streamlining production processes. Lead times for some custom orders at Guoshengli Packaging can be as short as seven days. This helps brands that need to get their products on the market quickly or during busy times of the year. This format is good for new brands that want to try out new SKUs without having to keep too much inventory on hand because the minimum order quantities (MOQs) are lower.
Packaging Flexibility Across Industries
Fin seal pouches can be used for many things. They are used to store food like popcorn, chips, nuts, candy, and cold foods. Pet food makers use them to make treats and feed because they don't absorb smells and can't be punctured. Protein powders, vitamins, and superfoods from health and wellness brands are packed in ways that keep their potency. They are used by beverage makers to make powdered concentrates and quick drink mixes. Chemical-resistant inner layers help companies that make household goods handle things like soaps and personal care products.
Material Choices and Sustainability Options
Most multilayer structures are made up of PET or BOPP for strength and printability, nylon or metalized PET for barrier properties, and polyethylene for heat sealing. To meet the growing demand for sustainability, mono-PE structures that can be recycled and PLA/PBAT films that can be broken down naturally are being used. These environmentally friendly choices are in line with corporate social responsibility goals and meet consumer demand for packaging that is good for the environment.
Comparing Fin Seal Pouches with Other Pouch Types
Procurement teams benefit from understanding how different pouch formats compare in terms of functionality, cost, and application suitability.
Fin Seal vs. Side Seal Pouches
Side-seal pouches are formed with seals along the two side edges, with one end generally left open for filling. They have a flatter shape that makes them good for putting on shelves, but they usually need more material than fin seal pouches. The fin seal pouch only has one back seal, which saves money on materials and makes production easier. For automated lines that work at high speeds, the fin seal style gives more uniform sizes, which means that machines don't have to be adjusted as often and there is less downtime.
Fin Seal vs. Stand-Up Pouches
Stand-up pouches have a gusset at the bottom that lets them sit straight up on shelves. This makes the product more visible in stores, but it also uses more materials and makes it more complicated. Fin seal pouches can't stand on their own, but they make up for it by being cheaper and easier to make. Brands that want to make a big effect on the shelf may choose stand-up forms, while brands that want to save money and work with automation systems often choose fin seal designs.
Fin Seal vs. Zipper and Resealable Pouches
People who use the same product more than once will find resealable forms more convenient because they have zip locks or press-to-close features. Adding these traits raises the cost of materials and production. Fin seal pouches can have tear holes to make them easier to open, but they usually can't be closed again. Single-serve or quick-consumption products like candy, snack-sized portions, and sample sachets work great in them.
How to Choose and Procure Fin Seal Pouches for Your Business
Selecting the right packaging partner requires careful evaluation of materials, customization capabilities, supplier reliability, and regulatory compliance.
Evaluating Material Composition and Barrier Properties
Use the right material frameworks for the right goods. High oxygen barriers are needed for coffee and snacks, resistance to wetness is needed for frozen foods, and odor control is helpful for pet treats. Talk to your providers about OTR and WVTR goals to make sure that recipes meet your shelf-life goals. Materials that can be recycled or composted should be tested by a third party to make sure that performance claims are in line with sustainability goals.
Customization Options for Brand Differentiation
Full-surface printing lets brands share stories about their products, nutritional information, and how to use them. Rotogravure printing can use up to 11 colors, so the prints will be bright and consistent even over long runs. Digital printing is good for short runs because it can be done faster and costs less to set up. Finishes like shiny, matt, or glossy make things look better. Functional add-ons like euro holes, tear cuts, and clear windows make shopping easier and look better in stores.
Navigating Supplier Landscape and Compliance
Cost structures, wait times, and legal knowledge of suppliers in China, the US, and other places are different. Chinese producers often have low prices and a lot of products to make. To make sure that quality systems meet international standards, check for certifications such as ISO 9001, BRC, and FDA compliance. Before placing a large order, ask for samples and test the strength of the seal. Check how responsive they are to communication and how well they can help with technical issues. These are things that affect the long-term success of a partnership.
Understanding MOQs, Lead Times, and Pricing Models
Minimum order amounts depend on the source and how complicated the customization is. Because digital printing lowers MOQs, it can be used for limited editions or test launches. Rotogravure printing has higher MOQs, but for big quantities, the cost per unit is lower. Lead times depend on the details of the order. Standard forms ship faster than fully customized designs. To lock in prices and make sure you have enough supplies during busy times, talk about big deals and make framework agreements.
Industry Insights – Top Brands, Trends, and Future Prospects
Staying informed about market developments helps procurement professionals anticipate changes and align sourcing strategies with emerging opportunities.
Leading Manufacturers and Innovation Leaders
Global sellers keep putting money into high-tech laminating tools, solvent-free glues, and accurate conversion machines. Manufacturers with decades of experience, like Guoshengli Packaging, which has been making flexible packaging for over 25 years and can make 20,000 tons of it every year, offer steadiness and technical know-how that younger companies may not have. Suppliers that have been around for a while have a history of handling repeat orders, keeping colors consistent, and helping with legal compliance across foreign markets.
Emerging Trends in Material Science
Transporting films that are light saves money and the environment without losing security. Bio-based polymers made from natural materials meet the requirements for sustainability. Advanced barrier coatings make thinner gauges work better, which means less material is needed. Volatile organic compound (VOC) emissions can be cut down with water-based inks and solvent-free lamination. This helps make manufacturing processes cleaner and meets stricter environmental rules in North America and Europe.
Innovations in Production and Customization
Digital printing technology lets you make smaller runs, make changes more quickly, and customize products on demand. Smart package features like QR codes and virtual reality make it easier for customers to interact with the product. Vision inspection-based automated quality control systems find flaws in real time, cutting down on waste and making sure that output is always the same. These new ideas make it easier for smaller brands to get started and help with flexible product development processes.
Future Outlook and Regulatory Influences
New rules on plastic trash, recycling requirements, and extended producer responsibility (EPR) programs will make more people want products that can be recycled or composted. Brands that choose to use eco-friendly products and clear supply lines will have an edge over their competitors. If e-commerce keeps growing, more people will need packaging that can handle the stresses of shipping. Buying groups should give more weight to companies that can do research and development and have plans for sustainability that are in line with long-term market trends.
Conclusion
Fin seal pouches are good for food, pet care, vitamin, and drink brands because they protect products well, make operations more efficient, and keep costs low. Because they can be used with high-speed automated lines, have barrier properties that can be changed, and have options for sustainability, they are a good choice for many situations. Procurement pros can make choices that protect product quality, help brands stand out, and align with long-term business goals when they understand structural differences, material options, and suppliers' abilities. As market trends move toward sustainability and e-commerce growth, working with experienced makers is the best way to make sure you have a steady supply of products and that they work well on all of your orders.
FAQ
1. What materials are commonly used for these pouches?
Most designs have a top layer made of PET or BOPP, a barrier layer made of nylon or metalized PET, and a sealant layer made of polyethylene. Foil laminates keep out as much light and oxygen as possible from sensitive products. As more brands care about the environment without sacrificing shelf life, recyclable mono-PE designs are becoming more popular.
2. How do pillow pouches compare in cost to other formats?
Fin seal pouches usually cost less than stand-up or spouted pouches because they are easier to make and use materials more efficiently. High-speed production cuts costs even more per unit. Buyers can save even more by buying in bulk and getting material specifications that are better suited to their needs instead of solutions that are over-engineered.
3. Can I customize size, barrier properties, and branding?
Of course. The size, construction, and effectiveness of the barrier can be changed to fit the needs of the product. You can print anything from simple one-color designs to complex graphics with custom finishes that use many colors. Features that are useful, like euro holes, tear cuts, and clear windows, make things easier to use and make them look better in stores. During the design phase, work closely with your suppliers to make sure that the packaging fits in with your brand's look and feel and with how your business runs.
Partner with a Trusted Fin Seal Pouch Manufacturer
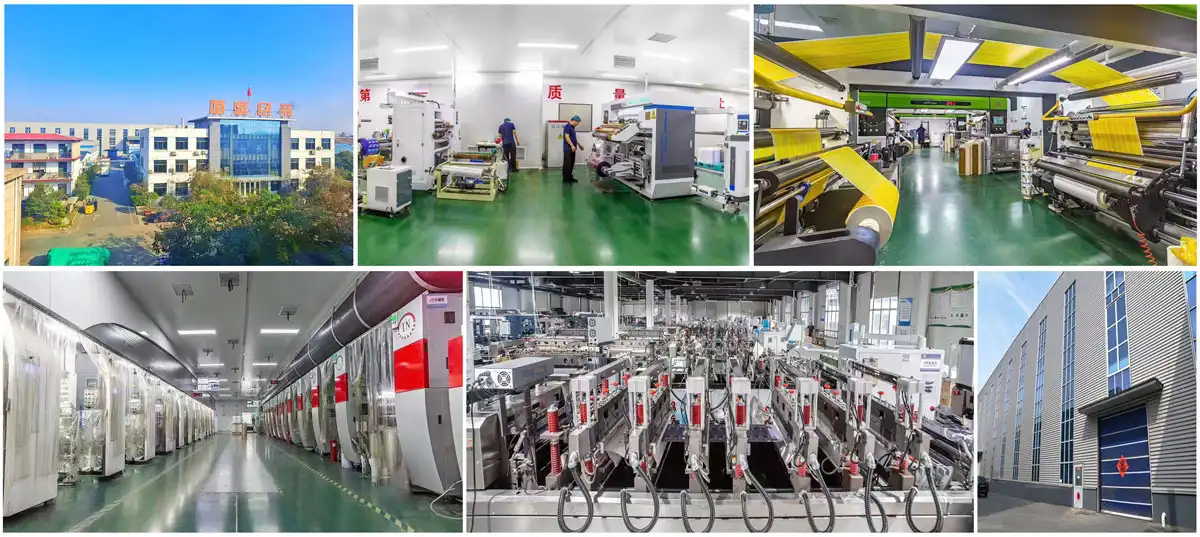
Guoshengli Packaging specializes in making personalized fin seal pouches that work in real-world production settings. We've been making things for 25 years, can make 20,000 tons of stuff a year, and are certified by ISO 9001, BRC, and FDA. We work with names in North America, Europe, and the Asia-Pacific region. Rotogravure printing in up to 11 colors, multilayer lamination, and precise converting equipment are some of the things we can do. We have flexible MOQs, wait times of as little as seven days for some orders, and choices for materials that can be recycled. Email our sales team at sales@guoshengpacking.com to get samples, talk about customization, or look into how much our next packaging project will cost.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice. 3rd ed. CRC Press, 2012.
2. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. Plastics Packaging: Properties, Processing, Applications, and Regulations. 3rd ed. Hanser Publications, 2016.
3. Marsh, Kenneth, and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science 72, no. 3 (2007): R39-R55.
4. Yam, Kit L., ed. The Wiley Encyclopedia of Packaging Technology. 3rd ed. Wiley, 2009.
5. Brody, Aaron L., and Kenneth S. Marsh, eds. The Wiley Encyclopedia of Food Science and Technology. 2nd ed. Wiley, 1999.
6. Coles, Richard, Derek McDowell, and Mark J. Kirwan, eds. Food Packaging Technology. Blackwell Publishing, 2003.
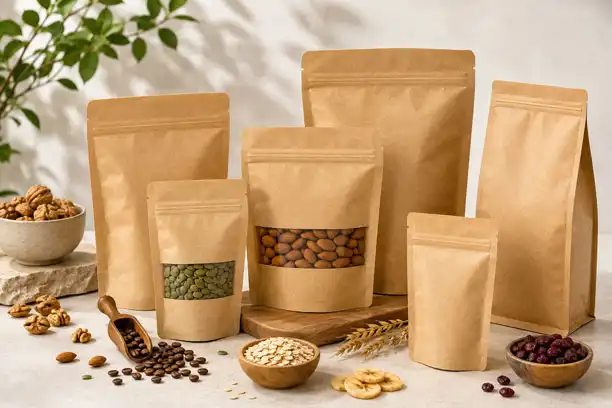
Brown kraft paper pouches represent a smart packaging solution combining sustainability with functionality. These natural-looking packages serve businesses seeking eco-friendly alternatives without sacrificing product protection. Manufactured from renewable kraft paper fibers and engineered with multi-layer barrier technologies, these pouches address growing consumer demand for environmentally responsible packaging while maintaining the strength and freshness protection required for diverse products. Their versatility spans food, pet treats, health supplements, and specialty goods, making them an increasingly popular choice among procurement professionals worldwide.
What Are Brown Kraft Paper Pouches Made Of and Why It Matters
Businesses can make better choices about where to get brown kraft paper pouches when they know what's in it. Product shelf life, brand image, and environmental effect are all directly affected by the structure of the material.
Natural Kraft Paper Foundation
It is made of raw kraft paper that is usually between 40 and 80 GSM (grams per square meter). This natural paper is made from sulfate wood pulp using a chemical process that keeps the long wood fibers. This makes the paper very strong and resistant to tears. Because it hasn't been washed, it has that unique brown color that people associate with organic and environmentally friendly brands.
Multi-Layer Barrier Engineering
Brown kraft paper pouches have high-tech lamination systems that keep the goods safe from outside influences. Depending on the needs of the product, Guoshengli Packaging designs pouches with carefully chosen barrier layers such as aluminum foil (AL), metallized polyester (MET-PET), nylon (NY), or EVOH. These layers in the middle keep out oxygen, water, and UV light, all of which are important for determining how long dried foods, coffee, snacks, and vitamins will last.
Food-Safe Inner Sealing Layers
The interior layer can be sealed with heat and is safe for direct food contact. Polyethylene (PE), cast polypropylene (CPP), or reusable PE formulas are all choices. During production, this layer makes sure that the seal is airtight, and it also keeps the product's structure while it's being shipped. Total thickness is usually between 120 and 160 microns, which is a good balance between protection and material efficiency.
Why Material Selection Impacts Your Business
The right makeup of materials affects three important business outcomes: the longevity of the product, compliance with regulations, and the image of the brand. Oxygen-sensitive products, like roasted coffee, need walls made of aluminum foil. Moisture-resistant metallized films are better for packing dried fruits. Knowing these differences can help you avoid expensive product failures and customer complaints, and it can also help you make environmental messages that appeal to current consumers.
Benefits and Practical Uses of Brown Kraft Paper Pouches in Packaging
Beyond being good for the earth, brown kraft paper pouch packaging has many useful benefits. These pouches solve real practical problems and improve your brand's image at the same time.
Superior Product Protection
Brown kraft paper pouches have strong barriers against moisture, oxygen, and light because they are made of multiple layers. This protection makes the shelf life a lot longer. The three-side seal structure that is often used to package jerky makes edges that are strong enough to handle being handled while shipping and while being displayed in stores.
Enhanced Brand Authenticity
The look of natural kraft expresses sincerity and quality without the need for extra marketing messages. Brands that promote organic ingredients, artisanal production, or caring for the environment can benefit from the instant visual link that kraft paper makes. The matte finish allows for high-quality printing—our rotogravure process gives you up to 11 colors with clear details—so brands can mix natural looks with high-tech graphics.
Functional Design Features
These days, brown kraft paper pouches have features that make them easier for people to use. Easy-tear notches get rid of the need for scissors, making opening easier without affecting the seal's strength. With the addition of hang holes, boxes can be turned into ready-to-sell displays that can be set up on shelves or pegs. products that are used more than once can be kept longer with resealable zippers, and clear windows let you see what's inside without taking away from the kraft look.
Versatile Application Across Industries
We make brown kraft paper pouches for a wide range of markets at Guoshengli Packaging. Coffee roasters like how degassing valves let CO2 out while keeping oxygen out. Brands of pet treats like the grease-resistant inner layers that keep oil from moving around. Supplement companies benefit from moisture barriers because they keep hygroscopic powders from sticking together. Snack food makers use the structure's resistance to punctures for things like pretzels and granola clusters that have sharp edges.
Sustainable End-of-Life Management
Using responsible ways to get rid of trash is an important part of the circular economy. Fully compostable models with PLA (polylactic acid) bio-based liners completely break down in industrial composting areas, meeting the tightest sustainability standards for brands that want to reduce trash to zero.
Comparing Brown Kraft Paper Pouches to Other Packaging Options
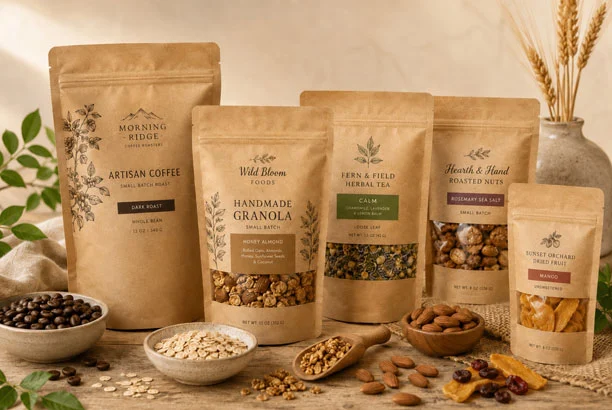
When looking at different types of packaging, you need to know both how well they work and how much they will cost throughout the whole supply chain.
Cost Considerations and Value Proposition
Most of the time, the cost of materials for brown kraft paper pouches is 15 to 25 percent higher than for similar plastic packaging. When you look at the total costs over the whole lifecycle, though, this price difference gets smaller. Brands often get higher prices by talking about sustainability, which helps them cover the costs of materials by making more money. Also, brown kraft paper pouches are cheaper for consumers and stores to throw away trash than hard plastic cases or multi-material packages that can't be recycled.
Resealable Features and Convenience
These days, brown kraft paper pouches are just as convenient as plastic packing. For zipper ends, PE or recyclable materials are heat-welded to the kraft structure to keep air out even when there are multiple holes. Degassing valves, which are important for coffee packing, work the same whether they are attached to paper or plastic. These feature additions make sure that kraft pouches can compete on functionality while still being good for the environment.
Brown Versus White Kraft Paper Selection
Compared to bleached white kraft paper, unbleached brown kraft paper is cheaper and better for the environment. The brown type doesn't need to be bleached with chemicals, so less water and chemicals are used in production. When you look at it, brown kraft gives off an air of rustic realism, while white kraft gives off an air of cleanliness and sophistication. The best choice depends on how the brand is positioned. For example, organic food brands tend to choose brown, while drug and vitamin companies tend to choose white for professional reasons.
How to Buy Brown Kraft Paper Pouches Wholesale: A B2B Procurement Guide
To buy brown kraft paper pouches effectively, you need to know what the suppliers can do, how to check the quality, and how to handle shipping.
Supplier Qualification Criteria
Reliable manufacturing partners show that they can do more than just make things. For entry to the US market, look for suppliers that have widely known certifications such as ISO 9001 for quality control systems, BRC for food packaging, and FDA compliance. These licenses show that quality control procedures have been put in place for a long time. This lowers the chance of batch differences or contamination problems that lead to expensive product returns.
Manufacturing Capacity and Scalability
How reliable the supply chain is is directly affected by how much can be produced. Our 20,000-ton annual capacity at Guoshengli Packaging makes sure that names that are growing quickly always have what they need. Check to see if potential suppliers use up-to-date tools. For example, rotogravure printing produces more consistent colors than flexographic options, and automated machinery for making brown kraft paper pouches ensures the accuracy of sizes that are necessary for automated filling lines to work.
Minimum Order Quantities and Lead Times
MOQ requirements are very different between suppliers. Digital printing lets you make smaller batches, starting at about 2,000 to 10,000 pouches. These can be used to test products or make limited editions. Rotogravure printing usually needs more than 20,000 bags to cover the costs of preparing the cylinder, but it has lower costs per unit for ongoing production. Standard wait times for rotogravure printing are 15 to 20 days, and for digital printing they are 7 to 10 days. Shipping from Asian makers takes an extra 4 to 5 days by air freight or 25 to 35 days by ocean freight.
Custom Printing and Branding Specifications
Production delays and quality problems can be avoided by giving clear instructions for the artwork. Give the right color values for the vector-format files—CMYK for digital printing or Pantone specs for rotogravure. During the initial discussions, make sure to include functional requirements such as where to put the tear notch, zipper, and hang hole. Before approving the production, ask for digital mockups to make sure you're happy with how it looks and where the features are placed.
Quality Verification Processes
Suppliers with a good reputation follow checking methods at several stages of production. Barrier film properties and paper specifications are checked when new raw materials come in. In-process tracking checks the correctness of the dimensions, print registration, and seal strength. Final inspection checks finished brown kraft paper pouches for flaws before they are packed. When you package food, get reports from a third party that test the barrier performance, seal integrity, and migration.
Global Shipping and Logistics Optimization
The cost of shipping has a big effect on the total cost of landing. Even though it costs more, air freight is best for pressing orders or small test amounts. For container-load volumes, ocean freight becomes cost-effective, but because of the longer transit times, accurate demand forecasting is needed. To make customs clearance and final delivery easier, work with companies that offer freight forwarding services or who already have relationships with foreign logistics providers.
Building Long-Term Supplier Relationships
Packaging accuracy between reorders depends on how stable the seller is and how well they can communicate. Set clear technical requirements that are written down in buy deals. Set up regular visits to the production facility or audits by a third party to make sure that quality standards are still being met. Keep lines of communication open so that problems can be fixed quickly. Suppliers who are responsive take quality concerns seriously and take clear corrective actions.
Why Choose Brown Kraft Paper Pouches: A Rational Decision Framework
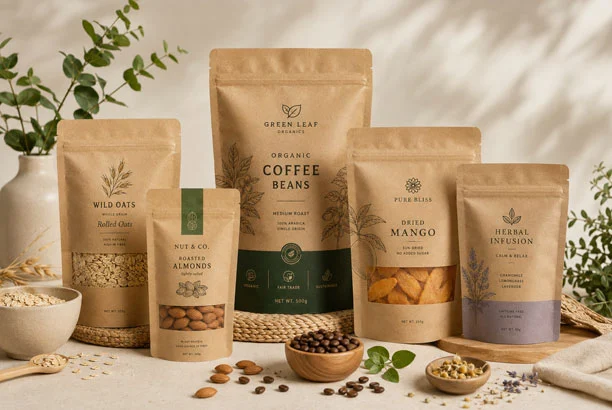
When making strategic decisions about packaging, you need to look at more than just the immediate cost of materials. Brown kraft paper pouches address a number of market forces that are coming together to affect business-to-business purchases.
Regulatory Environment and Trends in Compliance
More and more, government rules limit single-use plastics and require producers to take on more responsibility. SB 54 in California says that plastic packaging trash must be cut by 25% by 2032. The Single-Use Plastics Directive of the European Union bans some plastic products and sets standards for recycled material. Brown kraft paper pouches proactively meet these requirements, lowering the risks of not meeting regulations and the possible costs of making changes as rules get stricter.
Consumer Preference Shifts
More and more customers are willing to pay more for packaging that is better for the environment. Millennials and Generation Z users care a lot about being environmentally friendly, which affects their choices in food, pet care, and personal health. Brown kraft paper pouches stand out right away on store shelves and send a message that the brand's values are in line with what customers care about.
Brand Image and Where It Stands in the Market
Packaging acts as silent salespeople who talk about a brand's identity. Because brown kraft paper pouches look natural, they are good for premium, artisanal, or health-conscious markets. When compared to common goods in regular plastic packaging, this placement allows for higher prices. When brands switch to brown kraft paper pouches, they often use the change to show their commitment to sustainability in marketing efforts. This gets the attention of the media and makes customers happy.
How to Cut Costs in the Supply Chain
Even though the cost of materials is a little higher, brown kraft paper pouches save money in other ways. Because they are lighter than rigid crates, they cost less to ship, which is especially important for foreign shipping. When compared to bulky hard packing, the flexible shape makes the best use of warehouse room. Effective barrier protection keeps goods from going bad, which cuts down on waste all along the supply chain. These things help make total cost of ownership estimates more accurate.
Barrier Performance and Product Protection
Choosing the right brown kraft paper pouch structures is important for protecting the food's shelf life. Dried fruits, nuts, coffee, and other foods that go bad when exposed to air need aluminum foil or high-barrier metallized film layers. products that don't like being wet, like protein powders, do better in bags with EVOH or nylon buffer layers. By matching the barrier qualities to the needs of the product, you can avoid under-protection that leads to early spoilage or over-engineering that raises costs for no reason.
Partnership with Trusted Manufacturers
Long-term performance of packaging depends on how knowledgeable and reliable the supplier is. With 25 years of experience in flexible packaging, Guoshengli Packaging helps clients choose the right materials, plan their structures, and make the best use of barriers. During production, we use strict quality control methods to make sure that brown kraft paper pouches always work the same way, even when they are ordered again. Our factory makes things for names in North America, Europe, and the Asia-Pacific region. It has the global reach and technical communication tools needed for global supply lines.
Conclusion
Brown kraft paper pouches are a great way to protect products, show off your brand, and be good to the environment at the same time. Their natural kraft look appeals to eco-friendly shoppers, and multi-layer barrier technologies make sure that a wide range of products can stay fresh for a long time. Businesses can use brown kraft paper pouch solutions that help them meet both their operational goals and their sustainability pledges by learning about the materials used, reviewing their options, and working with qualified makers. Brown kraft paper pouches put brands in a good situation for long-term market success as rules get stricter and buyer tastes change.
FAQ
1. Are brown kraft paper pouches suitable for direct food contact?
FDA and EU food contact rules are met by brown kraft paper pouches made with food-grade inner layers. Instead of coming into direct contact with food, the brown kraft paper pouches have an inner layer of PE or CPP that keeps food safe. Manufacturers with a good reputation provide migration testing reports and compliance documentation that prove the material is safe for use in food applications.
2. Can I customize kraft pouches with my company logo and branding?
One of the best things about current brown kraft paper pouches is that they can be customized. Rotogravure printing can make images with up to 11 colors and great detail. The colors stay the same over long production runs. Digital printing is best for small runs because it can print in full color and gets the job done faster. Both ways keep the natural kraft look while accepting complicated artwork like logos, product photos, nutritional panels, and legal text.
3. How should businesses handle recycling and disposal of these pouches?
How to get rid of things depends on how they are constructed. To recycle brown kraft paper pouches with regular PE liners, you need special recycling centers that can separate the paper and plastic parts. These centers aren't available everywhere, but they are growing. Commercial composting centers that meet ASTM D6400 or EN 13432 standards can totally break down brown kraft paper pouches with compostable PLA liners. Brands should clearly sign packages with the right way to throw them away, based on the local trash management system, to help with the right end-of-life treatment.
Partner with Guoshengli Packaging for Your Kraft Pouch Needs
Businesses that need a reliable supplier of brown kraft paper pouches can benefit from Guoshengli Packaging's wide range of manufacturing skills and technical know-how. We've been making bendable packaging for more than 25 years and work with food brands, pet product companies, health supplement companies, and specialty goods companies all over the world. We keep our ISO 9001, BRC, and FDA certifications up to date and use modern rotogravure printing equipment that can produce 11-color images consistently of high quality across multiple orders. Email our team at sales@guoshengpacking.com to talk about your specific packaging needs, ask for samples, and get detailed quotes. We help you with everything, from choosing the right materials and designing the structure to printing, production, and safe foreign shipping. This way, we can make sure that your packaging always works well and supports your brand's goals.
References
1. Robertson, G.L. (2021). Sustainable Food Packaging: Principles and Practice. Academic Press.
2. Marsh, K. & Bugusu, B. (2019). "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, 72(3), R39-R55.
3. Yam, K.L. (2020). The Wiley Encyclopedia of Packaging Technology. John Wiley & Sons.
4. Kirwan, M.J. & Strawbridge, J.W. (2018). Plastics in Food Packaging: Properties, Design, and Environmental Impact. Smithers Pira Technology.
5. Siracusa, V. & Blanco, I. (2020). "Bio-based Polymers: Recent Developments in Sustainable Food Packaging Applications." Polymers, 12(8), 1635.
6. European Bioplastics Association. (2022). Bioplastics Market Data and Industry Standards. Berlin: EUBP Publications.
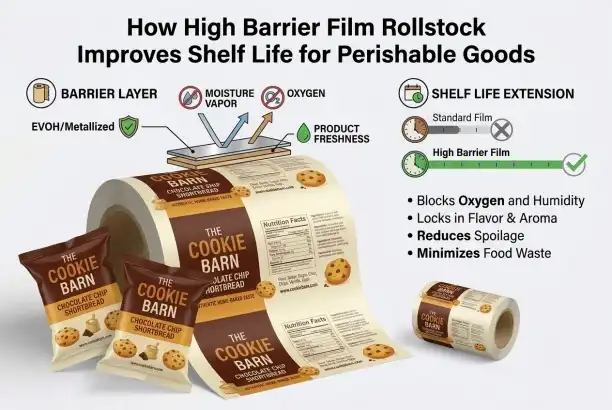
High barrier film rollstock extends the shelf life of fragile products by forming a barrier around them that keeps air, moisture, light, and outside contaminants out. This multi-layer packaging material has special polymer structures, which often include EVOH or metallized layers, that make it much harder for gases and vapours to pass through.
Understanding High Barrier Film Rollstock and Its Role in Shelf Life Extension
Failures in the packaging rarely show up during the first sample review. They show up weeks later, like when your production line stops in the middle of a run, when a lot of customers complain, or when your perishable goods go bad before they should. We at Guoshengli Packaging have seen these situations happen over the 25 years we've been making flexible packaging, and we've built our solutions to stop them.
What Makes High Barrier Films Different from Standard Packaging
Traditional packaging films offer some basic protection, but they aren't good enough to stop the four main threats to fresh goods: air getting in, moisture getting through, light exposure, and flavour loss. These weaknesses can be fixed with high barrier film rollstock that is made of designed multi-layer structures that use specific polymer combos. Each layer protects something different while still allowing automatic packing tools to move freely.
The structure usually has an oxygen shield layer (EVOH or PVDC), outer layers that don't absorb water (PE or PP), and structural stability layers that keep the structure from getting punctured while it's being handled. This careful layering makes transmission rates as low as 1 cc/m²/24h for oxygen and 1 g/m²/24h for water vapour, which are levels of performance that regular films can't even come close to.
Core Material Technologies Behind Barrier Performance
EVOH (ethylene vinyl alcohol) is very good at blocking oxygen, but it needs to be kept away from moisture because it weakens its barrier properties. We put EVOH between layers of slippery plastic to keep the performance stable even when the storage conditions change. The PVDC (polyvinylidene chloride) material protects well against both oxygen and water, but regulatory issues in some markets have made people prefer other structures.
Metallised films have layers of aluminium oxide or silicon oxide that work well as shields while still being flexible. New developments in single-material PE structures with AlOx or SiOx layers make them recyclable without lowering their security. This meets both performance needs and environmental standards.
The Science Behind Shelf Life Improvement for Perishable Goods
Understanding how barriers break down helps procurement teams choose the right specifications. Goods that go bad quickly go bad in expected ways that are sped up by certain natural factors.
How Oxygen Accelerates Product Degradation
Basically, oxidation is what breaks down lipid-containing foods the most. When oxygen molecules get into packaging, they start chemical processes that change the taste, colour, and nutrients of the food. Coffee gets old-smelling, nuts go bad, and dried fruits lose their bright colour. These processes are stopped by high barrier film rollstock with oxygen transfer rates below 1.0 cc/m²/24h. This makes the shelf life longer, from weeks to months.
When it comes to fresh meat, there are extra problems. Oxygen exposure helps aerobic bacteria grow and changes the colour of myoglobin from red to brown, which is not very appealing. Using high barrier films in modified atmosphere packing keeps certain gas mixtures (usually 80% O2 and 20% CO2 for red meat) that keep the colour and stop microbes from growing.
Moisture Control and Its Impact on Product Stability
Products are affected in both directions by moisture transmission. Products that are hygroscopic, like instant coffee, powdered vitamins, and dried pet treats, take in water from the air and cause them to clump, cake, and grow microbes. On the other hand, porous packaging lets goods that naturally contain water escape, like semi-moist pet food. This changes their feel and causes them to lose weight.
Our multi-layer barrier designs keep the transfer of water vapour below 1.0 g/m²/24h, which keeps the atmosphere fixed even when the humidity outside changes. This level of accuracy is especially useful for goods that are being shipped around the world and going through different climate zones.
Light Protection and Volatile Retention
Photochemical processes that break down vitamins, dyes, and flavour chemicals are sped up by ultraviolet and visible light. Products with light-sensitive ingredients, like some supplements, herbs, and speciality foods, need opaque or metallized barrier films that stop all light from passing through.
Keeping the smell is just as important. Volatile organic compounds can't get out of the packaging because of high barrier film rollstock. This keeps the sensory qualities that define product quality. This is shown by coffee packaging: if there isn't enough barrier protection, scent chemicals break down within days, leaving behind a flat, uninteresting product.
Comparing High Barrier Film Rollstock to Other Packaging Solutions
When making decisions about what to buy, it's important to compare the performance of different technologies in a fair way. Each type of packaging has its own pros and cons that affect total cost, working effectiveness, and product safety.
High Barrier Rollstock versus Metallized Films
Through vacuum-deposited aluminium layers, metallized films have great barrier properties. But these structures usually can't be recovered through regular plastic lines. This makes them hard to get rid of in markets with strict rules about extended producer responsibility. High barrier film rollstock provides the same level of protection as reusable mono-material choices, meeting both performance and environmental concerns at the same time.
There are also operational issues to think about. High-speed form-fill-seal machines can get static electricity from metallized films, which can cause registration issues and slow down production. Our high barrier films have anti-static chemicals and optimised surface processes that keep the coefficient of friction values fixed, even when production speeds reach more than 100 packages per minute.
Aluminum Foil Structures versus Polymer Barrier Films
Zero air, zero moisture, and zero light can pass through aluminium foil, making it a total barrier. There are some bad things about this performance. Foil shapes aren't flexible, so they can't be used for shaped or stand-up pouches. Also, getting rid of them is hard because foil-laminated buildings can't be recycled and need special trash handling.
A useful middle ground is high barrier film rollstock. Even though the transfer rates are a little higher than with foil, they are still low enough to keep most fragile things safe for as long as they are supposed to. The films are flexible, so they can be used in a variety of package formats. New structures made of only one material also help with circular economy efforts without sacrificing protection.
Vacuum Packaging and Gas Flushing Applications
Vacuum packing takes oxygen from the air by mechanical removal, and the film's protective qualities stop oxygen from entering again. Gas flushing, also known as "modified atmosphere packaging," replaces the air in the package with a mixture of gases that are best for the product. To keep protected atmospheres, both methods rely on packing materials that let very little air through.
The most important part of these technologies is the high barrier film rollstock. Without good barrier performance, vacuum packages slowly lose their tight seal as oxygen leaks in. At the same time, modified atmospheres change their make-up as gases move through permeable films. Our films keep OTR specs below 1.0 cc/m²/24h, which means that the vacuum and MAP effects last for months even during long distribution cycles.
Procurement Insights: Selecting and Buying High Barrier Film Rollstock
Successful procurement extends beyond comparing price quotes. The most cost-effective packaging solution balances initial material cost against total system performance, including production efficiency, product protection, and supply chain reliability.
Critical Specification Parameters
Oxygen transmission rate and water vapor transmission rate form the foundation of barrier evaluation, but complete specifications must address additional parameters. Seal strength determines whether packages maintain integrity through distribution handling. Puncture resistance indicates resilience against mechanical stress during transit. Heat seal initiation temperature defines the processing window for automated equipment.
We recommend requesting complete technical data sheets that document ASTM test results for all critical properties. Many packaging problems trace back to missing specifications that suppliers assumed were unimportant. Transparency at the specification stage prevents costly surprises during production scale-up.
Certification and Compliance Considerations
Food contact packaging must comply with FDA regulations in the United States and EU 10/2011 in European markets. These frameworks specify permissible materials, migration limits for monomers and additives, and testing protocols to verify compliance. Our high barrier film rollstock carries FDA and EU food-contact certifications verified through independent laboratory testing.
Beyond regulatory minimums, many customers require additional certifications. BRC (Brand Reputation Compliance) certification demonstrates systematic quality management throughout manufacturing operations. ISO 9001 certification provides framework assurance for process consistency. These credentials reduce procurement risk by confirming that suppliers maintain documented quality systems subject to regular third-party audits.
Evaluating Supplier Capabilities
Production capacity directly affects delivery reliability. At Guoshengli Packaging, our facility includes 7 rotogravure printing lines capable of 11-color reproduction, 6 laminating machines for barrier structure construction, and 49 converting units for rollstock finishing. This infrastructure enables us to handle both large-volume continuous orders and urgent short-run requirements without capacity conflicts that delay deliveries.
Lead times vary by printing technology and order volume. Digital printing enables prototype development and small-batch production with 7-10 day turnaround, ideal for market testing and new product launches. Rotogravure printing suits higher volumes with 15-20 day production cycles, delivering superior print consistency and lower per-unit costs for established products.
Sustainability and Total Cost Considerations
Recyclable packaging options increasingly influence purchasing decisions as brands respond to consumer preferences and regulatory mandates. Mono-material high barrier PE structures maintain recyclability while delivering OTR performance previously requiring multi-material laminates. These films support circular economy goals without compromising product protection—a combination that traditional barrier structures could not achieve.
Total cost analysis must extend beyond material price per kilogram. Thinner high-performance films reduce material usage and shipping weight while maintaining protection levels. Optimized barrier properties may eliminate preservative requirements, simplifying ingredient labels. Consistent quality reduces filling line stoppages and rework expenses. When evaluated comprehensively, premium barrier films often deliver lower total system costs than cheaper alternatives.
Best Practices and Future Trends in Using High Barrier Film Rollstock
The success of packaging rests on both the quality of the materials used and how they are used. When handled wrong or used with equipment that doesn't work with them, even the most advanced films don't work as well as they should.
Proper Storage and Handling Protocols
When kept properly (below 25°C and 60% relative humidity), high barrier film rollstock keeps its technical qualities for 12 months. If the storage conditions are not within these ranges, the barrier may not work as well before the material even gets to the production equipment. For the best material performance, we suggest climate-controlled storage and first-in, first-out product turnover.
The way things are handled affects how efficiently they work. Before it is used, rollstock should be brought up to the temperature of the working area. This keeps mist from forming, which can make heat sealing less effective. Corona treatment levels drop over time, so materials should be printed and coated within the time frames that are suggested. These details may not seem important, but they affect how well packing works across different production runs.
Heat Sealing Optimization
The integrity of the seal depends on exact temperature, dwell time, and pressure settings that are set to work with certain film structures. If you don't seal well enough, oxygen and moisture can get in, which defeats the purpose of the barrier. Too much heat breaks down polymers, which makes seals less strong and opens the door to contamination problems. We give detailed sealing setting suggestions for each film structure based on tests done on commercial form-fill-seal machinery.
These days, automatic seal checking systems check each and every package on modern packing lines. These technologies find tiny problems with the seals on goods before they leave the factory. This stops failures in the field that hurt the brand's image and lead to expensive refunds.
Emerging Innovations in Barrier Technology
New discoveries in material science keep changing what barrier packaging can do. Nano-clay additives improve barrier properties while lowering film thickness. This saves material without lowering protection. Bio-based barrier polymers made from renewable feedstocks meet sustainability goals while keeping up the performance standards set by materials made from petroleum.
Compared to traditional rotogravure printing, digital printing lets you make smaller runs and make design changes more quickly. Variable data printing helps with serialisation and anti-counterfeiting tasks that are becoming more important in controlled markets. These features make packaging useful for more than just protecting products.
The integration of smart packaging is a new frontier. With QR codes and NFC tags, you can interact with customers and keep track of your supply chain. Time-temperature indicators show that the cold chain is working properly. Oxygen indicators let you know when a barrier fails before the quality of the product goes down. Even though these technologies are still only used in a few situations, they show how packaging has changed from an inactive device to an active information platform.
Conclusion
By protecting against oxygen, moisture, light, and contamination, high barrier film rollstock makes it possible for perishable goods to last longer on the shelf. Multi-layer polymer structures with EVOH, metallised coats, or advanced mono-material shapes make transmission barriers that slow down the breakdown process. This keeps the quality of the product high for longer periods of time during distribution. Compared to other types of packaging, these films offer the best balance of protection, operational efficiency, cost-effectiveness, and new requirements for sustainability. To make a good purchase, you need to look at all the technical specs, make sure they follow the rules, and choose sources who have a history of making things and clear quality systems.
FAQ
1. What barrier performance should I specify for my product?
Required barrier levels depend on product sensitivity, desired shelf life, and storage conditions. Products high in fats or oils typically require oxygen transmission rates below 1.0 cc/m²/24h to prevent rancidity. Hygroscopic powders need water vapor transmission rates under 1.0 g/m²/24h to avoid caking. Our technical team conducts product-specific assessments to recommend optimal specifications based on your protection requirements and target shelf life.
2. Can high barrier films be made sustainable and recyclable?
Recent material innovations enable recyclable barrier films that maintain performance standards previously requiring multi-material structures. Mono-material PE films with AlOx or SiOx coatings deliver excellent oxygen barriers while remaining compatible with standard recycling streams. We also offer compostable PLA/PBAT-based solutions for applications where end-of-life disposal takes priority, though these materials require validation to ensure adequate shelf life protection for specific product types.
3. How do I verify that rollstock will work on my equipment?
Compatibility testing prevents costly production disruptions. We recommend requesting sample rolls for trials on your actual form-fill-seal machinery, evaluating runnability, seal quality, and package integrity under normal operating speeds. Critical parameters include coefficient of friction for web transport, heat seal initiation temperature for your sealing jaws, and dimensional stability under tension. Our team provides technical support throughout trial processes to optimize equipment settings for our film structures.
Partner With Guoshengli Packaging for Reliable Barrier Film Solutions
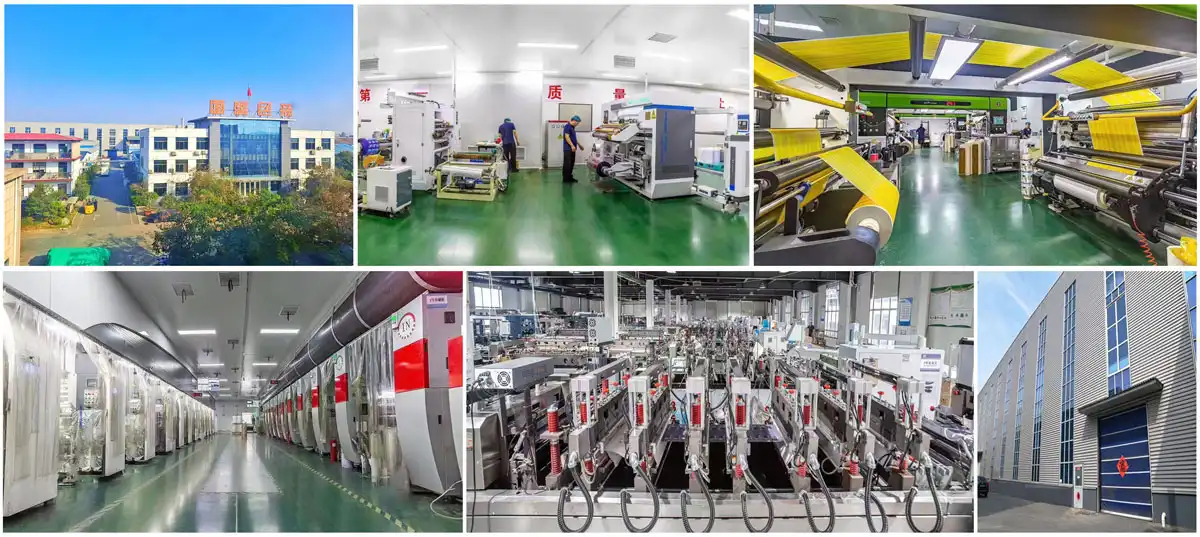
Packaging problems reveal themselves during production scale-up and repeat orders—not in initial samples. At Guoshengli Packaging, we eliminate these uncertainties through 25 years of manufacturing experience serving food, pet food, coffee, and health brands across North America, Europe, and Asia-Pacific markets. Our high barrier film rollstock delivers consistent oxygen and moisture protection engineered for automated filling lines, helping you avoid filling interruptions, product spoilage, and quality complaints.
We manufacture complete barrier packaging solutions—from custom rollstock films to finished pouches—using 7 rotogravure printing lines, 6 laminating machines, and 49 converting units. Whether you need recyclable mono-material structures, FDA-compliant food-contact films, or rapid digital printing for market testing, our team provides technical guidance from material selection through production optimization. Contact us today at sales@guoshengpacking.com to discuss your protection requirements with an experienced high barrier film rollstock supplier ready to support your long-term growth.
References
1. Robertson, Gordon L. "Food Packaging: Principles and Practice, Third Edition." CRC Press, 2012.
2. Coles, Richard, and Mark Kirwan. "Food and Beverage Packaging Technology, Second Edition." Wiley-Blackwell, 2011.
3. Marsh, Kenneth, and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Vol. 72, No. 3, 2007.
4. Yam, Kit L. "The Wiley Encyclopedia of Packaging Technology, Third Edition." John Wiley & Sons, 2009.
5. Hernandez, Ricardo J., et al. "Packaging and Food Quality." Modern Developments in Food Analysis, Volume 2, International Academic Publishers, 2015.
6. Singh, S. Paul, and Aaron L. Brody. "Packaging Technology: Fundamentals, Materials and Processes." Smithers Pira Technology, 2018.
When thousands of units need to be protected reliably and perform consistently every day, high barrier film rollstock is the packaging solution that was made for scale. This special multi-layer material protects against wetness and air very well while still working with automatic form-fill-seal machines. Over the past 25 years, Guoshengli Packaging has improved the way barrier film is made. We help food manufacturers, pet food brands, and health supplement companies keep the integrity of their products from production to retail shelf life.
Understanding High Barrier Film Rollstock: What It Is and Why It Matters
Composition and Structure
The use of high barrier film rollstock is an advanced technical method for protecting flexible packages. Unlike regular films with only one layer, these materials have several polymer layers that work together to protect the environment. The normal structure is made up of ethylene vinyl alcohol (EVOH) to fight oxygen, polyethylene or polypropylene to keep the structure strong, and special coats that protect against wetness better. Depending on the protection needs, metallised layers or PVDC (polyvinylidene chloride) can be useful in some situations.
Each layer does a different job of protecting. The outer layers make the material strong and easy to print, and the inner layers stop gases from moving through. This design makes it possible for oxygen to pass through at rates below 1 cc/m³/24h and water vapour to pass through at rates below 1 g/m²/24h. These are performance levels that greatly increase shelf life compared to regular packing materials.
Why Barrier Performance Matters
When air, wetness, or light touch sensitive chemicals, the product starts to break down. When they are exposed to moisture, coffee beans lose their aromatic compounds, dried snacks go bad, pet treats go bad, and supplement powders clump together. These problems with quality lead straight to customer complaints, store returns, and damage to the brand's image.
We make protective films that are designed to stop these problems. Our multi-layer structures keep their protective integrity even when they are moved around, the temperature changes, and they are handled with a lot of force. This dependability is especially helpful in delicate situations like nitrogen-flushed coffee packages, protein powders that are sensitive to wetness, and dried foods that are sensitive to air, where keeping the product fresh has a direct effect on how well the business does.
Critical Performance Indicators
Several technical factors, in addition to basic protection grades, decide how well packing works in the real world. Puncture strength, which is tested using ASTM F1306, makes sure that films can be handled without losing their protective properties. Seal strength (ASTM F88) keeps packages from breaking while they're being shipped. How easily rollstock goes through high-speed packing machinery is affected by the coefficient of friction. This may seem like a small thing, but it has a big effect on how efficiently production is done.
Each batch of our quality control process checks these parameters. We use MOCON sensors to test for leakage, interlayer bond strength analysis to keep layers from delaminating, and gas chromatography for solvent residue testing to make sure that no smells get into the packaged goods. This strict evaluation method gives procurement managers the stability they need when trying to place big orders.
Comparing High Barrier Rollstock Options: Making the Right Choice for Your Business
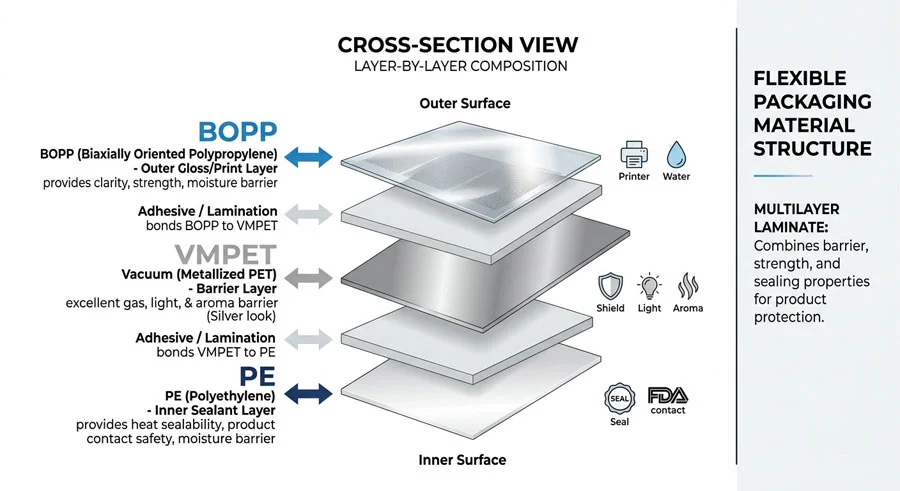
High Barrier vs. Standard Films
The difference between barrier classes affects both the amount of safety and the way costs are structured. Standard films usually let 10 to 100 cc/m² of oxygen through per 24 hours, which is fine for products that don't need to last long or aren't sensitive to oxygen. High barrier film rollstock works at transfer rates below 1.0 cc/m²/24h, which can protect products for weeks to months, based on their properties.
When you look at this difference in performance across different production volumes, it becomes economically important. A coffee maker that packages 10,000 units a month can save a lot of money by keeping the coffee fresh for longer, which cuts down on waste and helps the product reach more people. When you compare better product performance and lower loss rates, the extra cost of the materials is justifiable.
Material Selection Considerations
There are clear benefits to each type of barrier layer technology. EVOH is better at stopping oxygen, but it needs to be kept away from water because water weakens its protective qualities. To fix this, we put EVOH between layers of hydrophobic polyethylene or polypropylene. This makes a "sandwich" structure that keeps working well in a range of environmental conditions.
PVDC protects against both oxygen and moisture in a balanced way, and it works reliably in damp places. However, some markets don't allow PVDC because it contains chlorine, so EVOH shapes are better for exports to Europe and North America. Metallised films are a good barrier and don't cost too much, but they aren't clear, which is something to think about when product sight affects buying choices.
Evaluating Supplier Capabilities
When choosing a packaging partner, you have to look at more than just the material specifications. If your fifth production run works the same as your first, that's because of manufacturing stability. Controlled lamination processes, balanced ply tension during conversion, and systematic quality checks at multiple production stages help us keep this level of consistency.
Our certifications are proof that our products meet quality standards. ISO 9001 shows that quality management is done in a planned way, BRC certification proves that food safety rules are followed, and FDA/EU compliance paperwork makes sure that regulations are followed in key export markets. These certificates lower the risk of buying and make it easier for your quality assurance teams to check for compliance.
Fast and Cost-Effective Procurement Strategies for High-Volume Orders
Pricing Models and Volume Economics
When you buy a lot of something, the cost per bit goes down a lot because of economies of scale. This is reflected in our pricing, where cost-per-kilogram rates go down as order volumes go up. A trial order of 500 kilograms sets the standard price, while commitments of more than 2,000 kilograms unlock preferential rates that make the project's economics much better.
We make our prices clear by splitting the costs of materials from the costs of customisations like printing, special finishes, or specific size requirements. This makes it possible to accurately model costs when looking at different packaging options. Buying in bulk also keeps prices stable across multiple orders, which protects against changes in material costs that can make budget planning harder.
Customization Without Complexity
Each product has its own specific packing needs. Degassing valves are needed for coffee, anti-static qualities are needed for protein powders, and reusable caps are good for pet treats. Our method of customisation works with these requirements and doesn't make wait times too long.
For rotogravure printing projects, standard configurations ship within 15 to 20 days. For shorter runs or urgent needs, digital printing cuts the time to ship to 7 to 10 days. We have different widths, thicknesses, and finishes, and we can match the material specs exactly to your filling equipment and the way your product works. This freedom gets rid of the trade-offs that come up when goods are forced into standard packing options.
Lead Time Management
Scheduling production has a big effect on operations planning. To keep lead times low, we have a lot of manufacturing capacity. Our 7 printing lines, 6 laminating machines, and 49 converting units allow us to handle large orders without any production problems. This infrastructure supports both planned production runs and urgent orders that need to be filled quickly in response to market opportunities.
Coordinating logistics is the last part of the delivery equation. When production needs to be restocked quickly, we set up fast air freight that delivers the materials in 4 to 5 days. Standard ocean freight makes it cheap to ship planned orders. Our logistics team makes tracking clear and communicates ahead of time, which lowers uncertainty along the supply chain.
Quality Validation and Sampling
As part of responsible procurement, materials must be checked before production volumes are agreed upon. We give you samples that are true to the production materials, so you can test how well they work with your filling tools and product formulas. This step of confirmation finds possible changes that need to be made before going into full production. This keeps expensive changes from having to be made after production starts.
When you test a sample, you should make sure that it works as a barrier, that the seal is intact under the heat-sealing conditions you use, and that it is compatible with the chemical properties of your product. We help with this process by giving expert advice, explaining test results, and suggesting changes when they are needed.
Why Partner with Industry Leaders for High Barrier Rollstock Supply
Manufacturing Excellence and Experience
Twenty-five years of experience in manufacturing gives you ideas that younger businesses just can't copy. We have dealt with almost every packaging problem that comes up with a wide range of products. For example, we know how different formulations react with barrier materials, which film structures work reliably on different types of filling equipment, and how storage and shipping conditions affect the performance of packaging.
The information that has been gathered has real-world benefits. When you tell us about your product's features and how it needs to be packaged, we use a lot of past experience to come up with the best solutions instead of just giving you generic instructions. This consultation method cuts down on trial-and-error and speeds up your time to market.
Sustainable Manufacturing Practices
Regulatory standards and business sustainability pledges are making environmental duty more and more important in purchasing choices for high barrier film rollstock. There are several things we're doing to address these issues. Our factory uses imported RTO (Regenerative Thermal Oxidiser) exhaust treatment technology, which cuts down on manufacturing emissions by a large amount compared to traditional methods.
Material innovation is mainly about making structures that can be recycled and still work as barriers. We have created structures out of a single material polyethylene, that have aluminium oxide or silicon oxide coatings that give them high barrier properties while still being able to be recycled through normal waste streams. These solutions allow progress in sustainability without lowering the level of product security your customers expect.
Distribution Network and Logistics Support
For global processes to work, there needs to be effective foreign transportation. We serve customers in North America, Europe, and the Asia-Pacific region through established shipping relationships and knowledge of how to fill out customs forms. With this knowledge, you can easily meet regulatory requirements, which cuts down on clearance delays that make it hard to plan production.
Our approach to distribution strikes a balance between low costs and reliable delivery. When production is planned, container-load shipments are the most cost-effective way to send goods, while expedited air freight is best for urgent needs or market tests that need materials delivered quickly. This gives you the freedom to adapt to changing operational needs as your business grows.
Customer Success Evidence
We have long-term relationships with some of the biggest buyers of packaging in the US, Australia, and Europe, which shows that we can regularly meet high-quality standards. These relationships last for years and include many reorders, which is the real test of how reliable a manufacturer is. It's not noticeable to operations when packing works properly batch after batch. When it breaks, production stops, and costs go up very quickly. Our past performance points to the first possibility.
Maximizing Value from High Barrier Rollstock: Best Practices and Optimization Tips
Storage and Handling Protocols
Barrier film performance begins before materials reach your packaging line. Proper storage maintains technical properties throughout the material's usable life. We recommend climate-controlled warehousing below 25°C and 60% relative humidity. These conditions preserve barrier layer integrity and prevent film curl that can disrupt feeding on automated equipment.
Material rotation following first-in-first-out inventory principles ensures older stock moves to production before newer deliveries. While properly stored high barrier film rollstock maintains specifications for 12 months, systematic rotation prevents extended storage that might affect performance. Protecting materials from direct sunlight and contaminants further preserves quality through the supply chain.
Integration with Packaging Equipment
Successful rollstock performance depends on compatibility with your specific filling machinery. Film tension settings, unwind characteristics, and heat seal parameters require optimization for each material structure. We provide technical specifications that guide these adjustments, reducing setup time and minimizing waste during changeovers.
The coefficient of friction influences how smoothly material feeds through packaging equipment. We engineer surface properties to prevent slippage or excessive drag during high-speed operation. This attention to seemingly minor details translates into fewer production interruptions and higher overall equipment effectiveness.
Sustainability Implementation
Transitioning toward recyclable packaging structures requires balancing environmental objectives with product protection requirements. We approach this through systematic testing that validates barrier performance in recyclable constructions before recommending transitions away from conventional structures. This evidence-based methodology prevents sustainability initiatives from inadvertently compromising product quality.
Recycling infrastructure varies significantly across markets. Material selection should account for collection systems available in your target regions. Mono-material polyethylene structures align well with established recycling streams in North America and Europe, while other constructions may require specialized disposal processes. We provide guidance matching material recommendations to regional recycling capabilities.
Innovation Roadmap
Packaging technology continues advancing through new barrier layer chemistries, bio-based polymers, and enhanced multilayer structures. We monitor these developments, evaluating which innovations deliver practical benefits versus those requiring further maturation. Our research priorities focus on solutions that enhance product protection, improve sustainability profiles, or reduce total packaging costs without introducing operational complexity or unproven performance.
Recent developments in machine direction oriented polyethylene (MDO-PE) demonstrate the potential for recyclable films achieving barrier properties previously requiring mixed-material structures. As these technologies prove themselves through commercial-scale validation, we integrate them into our standard offerings, providing customers access to advancing capabilities without requiring them to navigate experimental materials.
Conclusion
High barrier film rollstock delivers the protection, performance, and efficiency that large-scale production demands. Through engineered multi-layer structures, rigorous quality control, and manufacturing capacity scaled for volume orders, this packaging solution addresses the core requirements of food manufacturers, pet food producers, supplement brands, and specialty product companies operating in competitive global markets. Successful procurement balances barrier performance with cost efficiency, lead time management, and supplier reliability—factors we have optimized throughout 25 years serving international customers. As sustainability requirements evolve and production volumes scale, partnering with experienced manufacturers ensures packaging continues performing reliably while adapting to changing market demands.
FAQ
1. What factors influence barrier performance in multi-layer films?
Barrier effectiveness depends on layer composition, thickness, and manufacturing quality. EVOH layers provide exceptional oxygen blocking but require moisture protection from surrounding polyethylene or polypropylene layers. Humidity affects EVOH performance, which is why we engineer sandwich structures that maintain barrier properties across varying environmental conditions. Material selection should match your specific product sensitivity and distribution environment.
2. How do I choose between high barrier rollstock and vacuum packaging?
This decision depends on product characteristics, production volume, and shelf life requirements. High barrier rollstock excels for products requiring modified atmosphere packaging or nitrogen flushing, particularly in high-speed automated lines. Vacuum packaging suits applications where removing air extends shelf life without requiring specialized barrier properties. We recommend evaluating both options based on your specific product chemistry and production capabilities.
3. What are typical lead times for bulk orders?
Standard rotogravure printing projects complete within 15-20 days, while digital printing reduces turnaround to 7-10 days for shorter runs. Lead times vary based on customization complexity, order volume, and current production scheduling. We provide accurate timelines during quotation, enabling reliable production planning. Expedited processing accommodates urgent requirements when needed.
Partner with Guoshengli Packaging for Your High Barrier Film Rollstock Needs
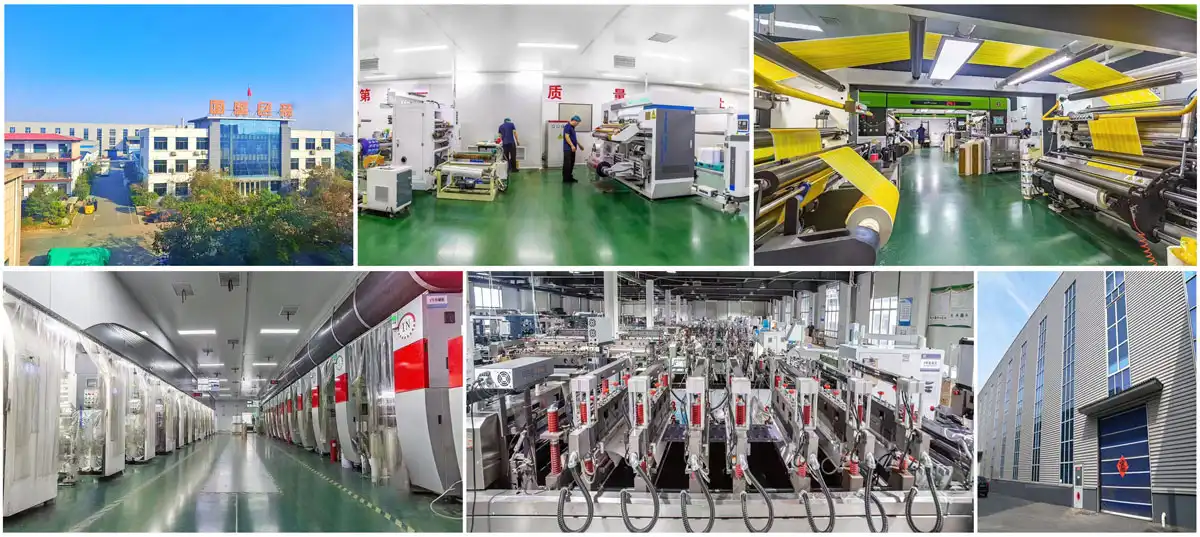
Reliable packaging should support your growth, not create operational uncertainty. As an established high barrier film rollstock supplier with over 25 years of manufacturing experience, Guoshengli Packaging delivers the consistency, quality, and technical support that large-volume production demands. Our ISO 9001, BRC, FDA, and EU certifications provide the compliance foundation international markets require, while our 7 printing lines, 6 laminating machines, and 49 converting units ensure capacity that scales with your requirements. Contact our team at sales@guoshengpacking.com to discuss your specific application, request samples for validation testing, and explore how our multi-layer barrier films can enhance product protection while optimizing your packaging costs.
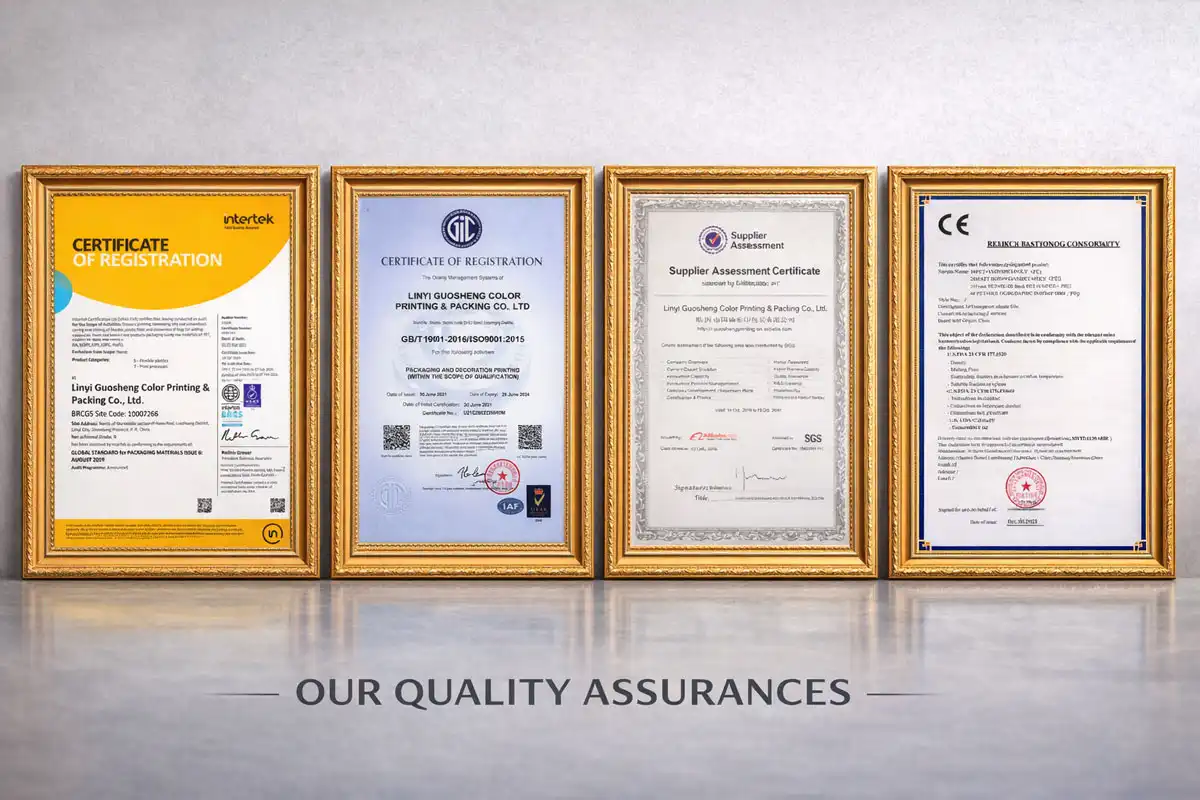
References
1. Robertson, Gordon L. (2016). Food Packaging: Principles and Practice, Third Edition. CRC Press, Boca Raton.
2. Marsh, Kenneth and Betty Bugusu (2007). "Food Packaging—Roles, Materials, and Environmental Issues," Journal of Food Science, Vol. 72, Issue 3, pp. R39-R55.
3. Siracusa, Valentina et al. (2008). "Biodegradable polymers for food packaging: a review," Trends in Food Science & Technology, Vol. 19, Issue 12, pp. 634-643.
4. Coles, Richard, Derek McDowell, and Mark J. Kirwan (2003). Food Packaging Technology. Blackwell Publishing, Oxford.
5. Hernandez, R.J. and J.R. Giacin (1998). "Factors Affecting Permeation, Sorption, and Migration Processes in Package-Product Systems," in Food Storage Stability, CRC Press.
6. Lange, J. and Y. Wyser (2003). "Recent innovations in barrier technologies for plastic packaging—a review," Packaging Technology and Science, Vol. 16, Issue 4, pp. 149-158.
It can be hard to find the right package partner for your product, especially if you need something unique, like handmade flat bottom bags that can hold 250 grams. There is a simple answer: you can buy a high-quality 250g custom flat bottom pouch from reputable B2B platforms, experienced makers like Guoshengli Packaging in China, or packaging dealers that serve North America and Europe. The important thing is to pick suppliers that have a history of reliable delivery, quality standards, and proven production capabilities. These are the things that set reliable makers apart from unreliable sellers in today's global supply chain.
Understanding 250g Custom Flat Bottom Pouches
What Makes Flat Bottom Pouches Different?
Flat bottom pouches, which are also sometimes called "box pouches," are a big step forward in the design of flexible packaging. Traditional stand-up pouches are only stable because of their gussets. These pouches, on the other hand, have a completely flat base panel and four vertical sides. This box-like structure lets the package stand straight up even before it's filled, giving it a great look on the shelf that grabs people's attention right away.
Five different pieces work together to make this design work: the front, the back, two side gussets, and the important flat bottom. This design makes the most of the space inside while keeping the overall size small. This makes moving and storing incredibly efficient. When the pouch is full of coffee beans, pet treats, or protein powder, it stays in its shape and doesn't lean or tip over. This is a huge plus in stores where look is important for making sales.
Common Applications Across Industries
Box bags in the 250-gram size work well for a wide range of products. Coffee roasters like how the stable base shows off the best beans and the multi-layer barrier keeps the flavourful oils from going bad. Pet food companies use these bags to keep treats and vitamins fresh because they know that the reusable zipper makes the product last longer after it has been opened. These pouches are used by health and wellness brands to package protein powders, superfood blends, and nutritional supplements because the structure shows quality and the large printable surface shows a lot of information about the product.
Manufacturers of snacks use flat bottom designs for nuts, dried fruits, and other unique products that look better when they are displayed upright. The 250-gram capacity is just the right size—big enough for a meaningful amount of product, but small enough for people who want easy-to-handle portions. Because it can be used in so many ways, this is why procurement teams in the food, pet care, beverage, and wellness industries are asking for flat bottom formats more and more.
Material Options and Barrier Properties
Modern pouches with flat bottoms are made with complex, multi-layer laminated structures that are designed to meet specific protection needs. Common designs include PET/AL/PE structures that offer the best protection against wetness, oxygen, and light. This makes them perfect for goods that are sensitive to oxygen, like coffee or fatty snacks that go bad quickly. PET/VMPET/PE laminates offer great performance at a lower cost for products that need moderate protection. The metallised layers keep the laminates' good looks.
Brands that care about the environment can now get structures made of a single material that are intended to be recycled for 250g custom flat bottom pouch. These structures are usually PE-based and keep their barrier qualities while making end-of-life processing easier. Some companies make recyclable choices with PLA or PBAT films, but these need to be carefully matched to the features of the product and the expected shelf life. To choose the right materials, you need to know how sensitive your product is to environmental factors, how long it's supposed to last, and what your target market wants in terms of sustainability. These are all things that you should talk about with experienced packaging engineers instead of looking at generic online catalogues.
Comparing 250g Flat Bottom Pouch Options to Make the Right Choice
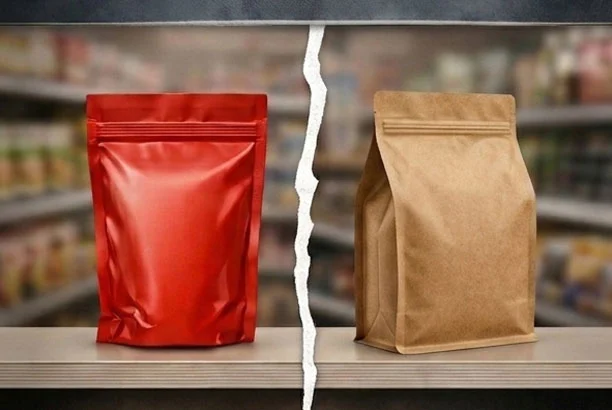
Flat Bottom vs. Stand-Up Pouches
Knowing the differences in structure helps procurement teams choose the right format. Traditional stand-up pouches have gussets on the sides or bottom that expand when the pouch is full. The weight of the product and the tension in the gussets keep the pouch stable. These are useful in many situations and usually cost a little less than flat bottom types. But they don't have the rigid, box-like look that flat bottom pouches do.
Flat bottom designs are more stable on shelves, even when they're only partly full. This is a big plus for goods that are sold by weight or that are eaten slowly. The four vertical panels, which are set up to look like hard box packing, give you more space to print and make it easier to tell your brand's story. Different filling lines work in different ways. For example, flat-bottom bags stay in the same place during automatic filling, which cuts down on jams and boosts output on high-speed lines. The choice depends on what's most important to you. If maximum shelf impact and premium positioning are the most important things to you, flat bottom construction is clearly the best option, even though it costs a little more.
Material Selection: Balancing Performance and Sustainability
More and more, decisions about what to buy have to balance functional needs with environmental concerns. Traditional aluminium foil laminates are the best at keeping out moisture and air, which greatly extends the shelf life of goods that are sensitive to these things. These structures work great for coffee, some snacks, and goods that need to be shipped or stored in difficult conditions for long periods of time.
When made with recycling in mind, plastic-based laminates that don't use foil can be good barriers at a lower cost and with less of an effect on the environment. New developments in high-barrier layers have made it possible for plastic structures to work almost as well as foil in many situations. Instead of depending on general material descriptions, procurement teams should ask for barrier property data, especially the rate of oxygen transmission and the rate of moisture vapour transmission. Failures after the product has been released to the market can be avoided by testing it in real storage conditions before committing to large production runs.
Valve vs. Non-Valve Configurations
One-way degassing valves are often used in coffee packaging. These valves let CO2 from freshly roasted beans leave while blocking air from entering. This feature keeps the package from growing and extends the shelf life, which is why roasters pay more for it. Products that don't make petrol usually skip valves, which saves money and gets rid of a possible failure point.
Zipper closures make it easier to use products more than once, which improves the user experience and justifies higher prices. Notches that are easy to tear make things easier to get to without using scissors or other tools. Each useful element increases the cost and difficulty of the product, so the design should be based on what the real product needs are and what the customers want, not just copying the package of competitors feature for feature.
How to Choose Reliable 250g Custom Flat Bottom Pouch Suppliers
Essential Quality Certifications and Standards
Packaging companies that want to sell their goods in controlled markets must show that they follow the rules by getting recognised licenses. For food-contact products sold in the US, FDA compliance is a must. This means that the materials used and the way they are made must meet food safety guidelines. Brand Reputation Compliance (BRC) certification shows that the manufacturer keeps quality controls and traceability in a systematic way. This is very important for brands that care about the integrity of their supply chains.
Getting ISO 9001 certification shows that you care about quality management systems, but it doesn't say anything about food safety for a 250g custom flat bottom pouch. Instead of depending on a single certification, look for sellers who have a number of useful certificates. Ask for copies of certificates and, if possible, check their validity with the organisations that issued them. In addition to certifications, you should also ask about the testing methods used. Reliable manufacturers test for migration, analyse seal strength, and check barrier properties during production runs, not just during the initial development phase.
Evaluating Production Capacity and Lead Times
Knowing how much a provider can make will help your business avoid problems as it grows. Ask clear questions: How many printing machines work every day? How many pouches can be made each month based on your specifications? For digital printing and rotogravure printing, how are the lead times different? Larger manufacturers with a lot of equipment, like those with multiple printing machines, sealing lines, and converting machines, can handle changes in volume and rush orders more effectively than smaller companies that are already at full capacity.
Your planning period should match the lead time you expect. Digital printing can finish bags in 7–10 days, but each unit may cost more, and the colours may not be as accurate for brand-critical uses. Rotogravure printing takes 15 to 20 days, which includes preparing the cylinder, but the colours are more consistent, and the unit costs are lower when you print in bulk. Setting reasonable due dates keeps people from making hasty choices that hurt quality or require expensive air freight to meet launch dates.
The Importance of Sample Evaluation
Don't commit to production quantities until you've looked at a sample carefully. Ask for samples that were made on real production equipment instead of trials that were made on research lines. Put test samples of your real product in real storage conditions for a few weeks to see how the seals work, how well the barriers work, and how the product and packing materials react to each other.
Carefully check the print quality by comparing the colours to brand standards, making sure the printing is straight across all panels, and using tape tests to see how well the print sticks. Functional parts should be tested. For example, do zippers open and close easily after being used several times? Do the valves work right and not leak? When it's full, does the pouch stand straight up? If you can, fill samples on your production equipment to find out if there are any fit issues before you buy the whole cylinder. This level of care finds problems early, before you have to ship thousands of broken units, when they are still easy to fix.
Where and How to Buy 250g Custom Flat Bottom Pouches Online
Understanding Purchasing Pathways
Buying custom packaging as a business takes a different road than buying it as a customer. You can work directly with manufacturers, use a business-to-business (B2B) platform to find suppliers, or join a distributor network. Having direct ties with makers like Guoshengli Packaging gives you the best prices and most customisation options, but you have to handle foreign shipping and talk to people in different time zones.
B2B platforms help businesses find suppliers and make transactions easier, but the quality of the sellers mentioned on these platforms varies a lot. Distributors and exporters offer local merchandise and easy buying, but they usually only offer ready-made stock products instead of fully customised solutions. Direct maker ties offer the best long-term value for branded packaging that needs specific sizes, custom printing, and regular repeat orders, even though they take more work to set up at first.
Step-by-Step Procurement Process
A structured approach is needed for sourcing to work well. Start by writing down everything you need: exact sizes, material requirements, barrier needs, functional features, print information (including artwork files and colour standards), and the number of products you want to order. Send this full list of requirements to potential suppliers and ask for formal quotes that include prices, lead times, minimum order quantities, and payment terms.
Carefully look over the quotes and don't just look at the unit price. Also, make sure you know the total landing cost, which includes shipping, taxes, and any tooling charges for printing cylinders. As we already talked about, ask for and assess samples. Once you're happy with the samples and the terms of the deal, place a trial order that's not too big and not too small so that you can see how well the seller does and still avoid too much risk if problems arise.
Keep a close eye on production and ask for reports on work and samples before shipping if you are making a lot of things. Set up an inspection before shipping if the value of the order justifies the cost. As soon as you get the package, carefully check it over and write down any problems right away. This methodical approach lowers risk and sets the stage for long-term supply relationships that get better as both parties learn more about each other's needs and skills.
Pricing Structures and Hidden Costs
To figure out how much packing costs, you need to look beyond the unit prices that are given. One-time cylinder etching prices for custom printing can be anywhere from a few hundred to over a thousand dollars, based on how complicated the design is and how many colours are used. These costs are spread out over many prints, which makes orders that are bigger cheaper overall.
Minimum order numbers are based on the economics of production. Because makers are more efficient when they work in large quantities, small orders cost more per unit. Shipping is very expensive. Sea freight takes 4 to 6 weeks but costs a lot less per unit than air freight, which gets the goods to their destination faster but increases the cost of logistics. Import duties can add 5–10% to the landed cost, depending on the country of destination and the type of material.
Payment terms affect cash flow. Some suppliers want to be paid in full up front, while others offer net terms after the relationship is established. Changes in the value of currencies add risk to international orders of 250g custom flat bottom pouch. To compare providers, you should find the total final cost per unit that takes all of these things into account, not just the FOB price that was given at the start.
Eco-Friendly and Sustainable 250g Flat Bottom Pouch Solutions
Why Sustainable Packaging Matters Now
More and more, regulations and consumer tastes are pushing for sustainable packaging. Recyclability goals are required by European Union guidelines, which push brands toward frameworks made of a single material and away from complex laminates. Extended producer responsibility programs in California and other U.S. states charge fees for packaging that is hard to discard. Consumer research consistently shows that environmental claims affect people's decisions to buy, especially when it comes to high-end products where the cost of packaging is already higher.
Sustainable packaging has real business benefits, such as a better brand image, easier compliance with regulations, the chance to charge more, and lower long-term risk as regulations get stricter. As supply lines change, early adopters gain a competitive edge, and laggards face more pressure and fewer choices. The question no longer is "should" we use sustainable packaging, but "which solutions balance performance, cost, and real environmental benefit?"
Material Innovations in Eco-Friendly Pouches
There are different material methods that deal with sustainability issues, each with their own pros and cons. Mono-material polyethylene structures make it possible to recycle by getting rid of layers of mixed materials that make sorting systems confused. However, for highly sensitive products, the barrier performance may not be as good as with traditional laminates. Paper-based laminates with thin PE layers have recyclable material and better waste potential. They are good for dry products that can handle modest barrier qualities.
Certified compostable films made from PLA, PBAT, or other bio-polymers break down in industrial composting facilities, which is a good way to get rid of waste where such facilities are available. Due to lower performance and higher costs, these can only be used in certain situations right now and can't be used in place of all conventional materials. The loop is closed by post-consumer recycled content in bag structures, but recycled content in direct food-contact layers is limited by rules about food safety.
To choose the right sustainable materials, you need to be honest about how to protect your product, the infrastructure that your target market has for collection and processing, and your willingness to spend money on validation testing. Instead of making vague marketing claims about how good something is for the environment, back up your claims with lifetime assessments and recognised badges.
Verifying Sustainability Claims
As more and more claims are made about recyclable packaging, it becomes important to check them. Instead of self-declared environmental qualities, look for approvals from a third party that you can trust. Labels with certifications like "How2Recycle" give clear directions on how to throw away things based on real recycling systems. Products that have been certified as compostable by BPI or TÜV Austria meet the technical requirements for industrial composting.
Ask the supplier for proof that the sustainable materials they sell are what they say they are: certifications for recycled content, proof that the materials can be recycled or composted, and test data for these materials. Be wary of words like "eco-friendly" that don't come with specific, verifiable qualities. Partner with suppliers who are willing to be open and honest. Companies that are genuinely committed to sustainability welcome detailed questions and give answers that go beyond marketing speak.
Conclusion
Finding the right 250g custom flat bottom pouches requires balancing a lot of things: the structural design that works for your product, materials that meet your needs for protection and your goals for sustainability, suppliers that can show you their quality systems and production capabilities, and buying processes that check performance before making big commitments. The flat bottom shape is better for shelf appearance and sturdiness, so brands that want to stand out should think about using it. Instead of guesses or copying what other companies are doing, choosing materials should be based on an honest evaluation of the barrier needs. Long-term value is higher with relationships with suppliers based on certificates, sample proof, and open conversation than with retail buying through online platforms. Sustainability is both an opportunity and a responsibility; work to make real changes for the environment instead of making empty claims. When you take the time to understand these factors and work with experienced packaging makers, you can turn packaging from something you buy as an item into a strategic tool that helps your brand grow.
FAQ
1. What is the typical minimum order quantity for custom flat bottom pouches?
Minimum order quantities vary by supplier and customization level. Fully custom printed pouches typically require 10,000-20,000 units to justify cylinder engraving costs and production setup. Some manufacturers offer lower minimums for digital printing, though at higher per-unit costs. Stock pouches with simple label application may be available in smaller quantities. When starting a new product, consider whether lower minimum suppliers serve your immediate needs or if committing to larger quantities with better pricing makes sense given your sales projections.
2. How long does custom printing take for box pouches?
Production timelines depend on printing method and supplier capacity. Digital printing generally completes within 7-10 days after artwork approval, suitable for smaller runs or urgent needs. Rotogravure printing requires 15-20 days including cylinder preparation, offering superior quality and economy for larger volumes. Allow additional time for shipping—sea freight takes 4-6 weeks, air freight 4-5 days. Building adequate lead time into your launch schedule prevents rushed decisions that compromise quality or force expensive expedited shipping.
3. Can flat bottom pouches run on standard filling equipment?
Most flat bottom pouches adapt to existing VFFS (vertical form fill seal) equipment and pre-made pouch filling lines with minimal adjustment. The stable structure often improves filling consistency compared to other flexible formats. Coordination between pouch supplier and filling equipment manufacturer helps ensure compatibility. Request technical drawings showing exact dimensions and specifications, and test samples on your actual equipment before committing to production quantities. Proper matching prevents costly delays from packaging that doesn't perform as expected on your line.
4. Are eco-friendly materials suitable for all products?
Sustainable materials vary widely in barrier performance and cost. Some products tolerate reduced barrier properties from recyclable mono-materials without meaningful shelf life compromise. Others—particularly moisture-sensitive or oxygen-sensitive products—require high-barrier structures that may not yet have fully sustainable equivalents offering equivalent protection. Honest assessment of your product's sensitivity, expected shelf life, and distribution conditions guides appropriate material selection. Testing sustainable options under real conditions before committing prevents failures after market launch.
Partner with Guoshengli Packaging for Your Custom Flat Bottom Pouch Needs
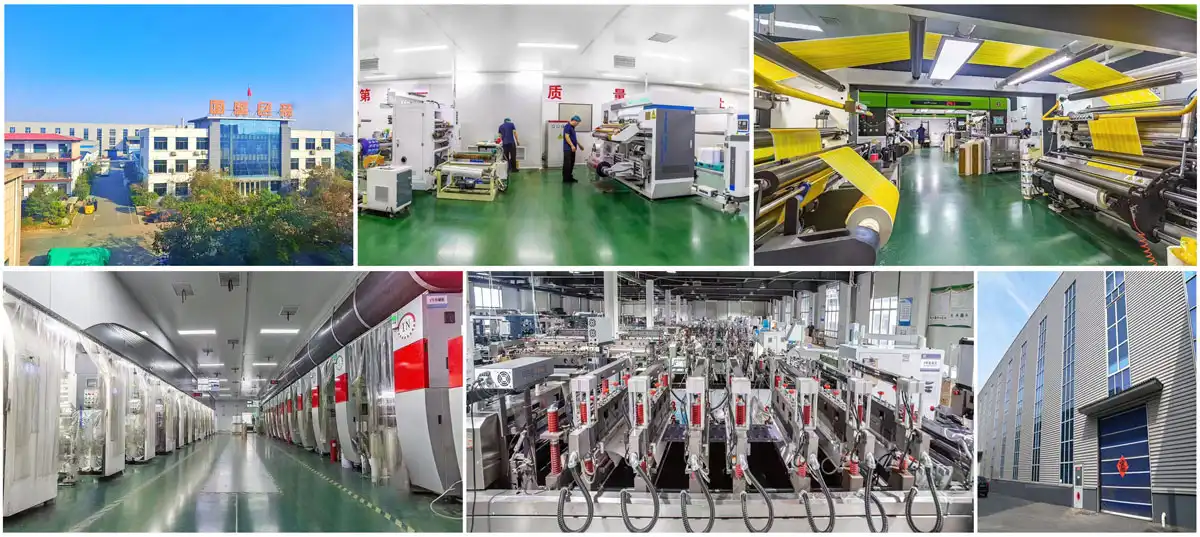
Guoshengli Packaging brings 25 years of flexible packaging manufacturing experience to brands seeking reliable custom flat bottom pouch suppliers. Our facility maintains ISO 9001, BRC, FDA, and SGS certifications, ensuring every 250g custom flat bottom pouch meets rigorous quality standards before shipment. With 7 printing machines, 6 laminating lines, and 49 converting machines, we handle orders from development samples through high-volume production runs with consistent quality and on-time delivery.
Our engineering team works closely with your specifications to optimize material structures, balancing barrier performance, sustainability goals, and cost efficiency. Whether you need traditional high-barrier laminates or recyclable mono-materials, we provide technical guidance grounded in real-world testing rather than generic recommendations. Digital printing delivers prototypes in 7-10 days; rotogravure production completes in 15-20 days with superior color consistency across repeat orders. Contact our team at sales@guoshengpacking.com to discuss your project requirements and request samples demonstrating the quality and functionality your brand deserves.
References
1. Anderson, M.J., & Chen, W. (2022). Flexible Packaging Engineering: Materials, Processes, and Applications. Packaging Technology Press.
2. European Flexible Packaging Association. (2023). Sustainability Guidelines for Flexible Packaging Procurement. EFPA Technical Report Series.
3. Institute of Packaging Professionals. (2023). Barrier Properties and Shelf Life Optimization in Food Packaging. IPP Research Publications.
4. Martinez, R.L. (2021). Global Supply Chain Management for Packaging Procurement. International Trade Publishing.
5. Sustainable Packaging Coalition. (2022). Design Guidelines for Recyclable Flexible Packaging. SPC Industry Reports.
6. Thompson, K.S., & Williams, J.R. (2023). Modern Flexible Packaging: Structures, Materials, and Manufacturing Processes. Technical Press International.
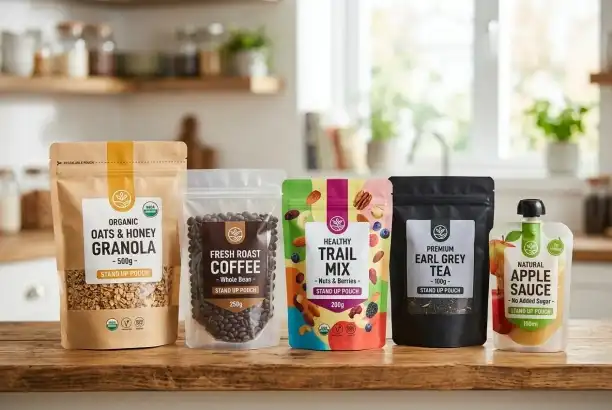
Stand up pouches have revolutionised packaging in many industries by combining functionality and aesthetics. These self-supporting flexible packages have a reinforced bottom gusset to stand upright on retail shelves, maximising visual impact and product freshness. Flexible pouch packaging is preferred by brands of snack foods, coffee, pet treats, and cosmetics for cost-effective, space-efficient product protection and convenience.
Understanding Stand Up Pouches and Their Key Benefits
Flexible pouch packaging has transformed product delivery. Multilayer barrier materials protect contents from moisture, oxygen, and light in these novel packages.
What Makes Stand Up Pouches Different


The structural design includes a bottom gusset for stability without external support. This self-standing feature improves retail display and reduces material use compared to boxes or jars. Multiple film layers—each providing a protective or functional purpose—are laminated into a durable, flexible structure during manufacturing.
Core Advantages for Procurement Teams
Procurement experts know these bundles provide supply chain value. Compact design saves storage and shipping costs and maximises shelf space. Advanced barriers reduce spoiling and refunds by extending product shelf life. Resealable zippers, tear notches, transparent windows, and high-definition printing help brands differentiate products while meeting functional needs. Our VMPET material architecture protects products from external influences that degrade quality, keeping them fresh from manufacturing to consumption.
Regulatory Compliance and Safety Standards
FDA- and BRC-certified food-grade materials assure direct food contact safety. SGS and other third-party testing verify barrier performance and material compliance. Working with qualified manufacturers that understand international standards and paperwork reduces supply chain compliance risk for brands entering regulated markets.
The Most Popular Uses of Stand Up Pouches Across Industries
Stand up pouches, a flexible pouch packaging, are popular across several industry categories owing to their performance and customer acceptability.
Food and Beverage Applications
The food business has used flexible packaging instead of jars, cans, and cartons. Oxygen barrier properties keep aromatics fresh and prevent staleness, which roasters like. Dried fruits and nuts stay crisp in moisture-resistant structures. Portion control and resealable closures help snack manufacturers. Spice manufacturers use transparent windows to display quality and exclude dampness. Light-blocking laminates preserve tea blends. These examples show how material selection affects product performance and customer satisfaction.
Pet Food and Treat Packaging
Pet brands have quickly adopted flexible pouches for dry food and treats. Pet owners may easily open and reseal the package, which protect product freshness. Barrier films prolong shelf life without preservatives by preventing fat oxidation and rancidity. High-impact graphics can convey quality and stand out in competitive retail environments. Shipping costs are lower with the lightweight construction, boosting distribution economics.
Health and Wellness Products
Supplement companies use stand up pouches for protein powders, vitamins, and superfood blends to protect them from moisture and oxygen. Resealable zippers prevent product deterioration and keep products fresh. From single-use packets to bulk containers, custom sizes are available. Modern, simple packaging for active lives matches wellness brand concept.
Non-Food Market Applications
Flexible pouches carry cosmetics, personal care, home cleansers, and industrial components. Cosmetic manufacturers provide samples and travel quantities in smaller pouches. Cleaning product makers value chemical resistance and longevity. Reclosable bags from hardware vendors protect tiny components from loss and contamination. Moisture barriers and UV protection help seeds and fertilisers. Material attributes and functional aspects must match product characteristics and user demands for each application.
How to Choose the Right Stand Up Pouch for Your Procurement Needs

Selecting effective packaging involves careful study of performance, cost, and market acceptability variables.
Material Property Assessment
Product sensitivity drastically affects barrier needs. Coffee needs strong oxygen barriers to stay fresh. Product moisture-sensitivity requires water vapour resistance. Light-sensitive contents need opaque or metallized films. Our high-performance VMPET structure provides multi-barrier protection for demanding applications. Procurement teams should set barrier performance objectives based on shelf life and storage circumstances, not general material descriptions.
Functional Features and Convenience Elements
Brand impression and repeat purchases depend on user experience. No scissors or equipment needed for easy-tear notches. Resealable zippers preserve freshness. Spouts provide regulated liquid and sauce pouring. Retail display versatility is enhanced with hanging holes. Degassing valves offgas coffee without damaging packages. Each feature increases functionality but also increases manufacturing complexity and cost, requiring brand positioning and target market expectations-based decisions.
Print Quality and Branding Capabilities
Packaging is a silent salesperson, so visual impact is crucial for purchases. Rotogravure printing maintains brand standards by reproducing colours consistently over huge manufacturing runs. Our 11-color printing allows sophisticated designs, gradients, and eye-catching photos. Spot UV coating gives a superior feel. Matte finishes look natural, while glossy surfaces look fresh and high-quality. Design elements should convey brand identity and regulatory and product information.
Supplier Evaluation Criteria
Quality control and filling line performance depend on manufacturing uniformity. Dimensional correctness guarantees automated equipment compatibility. Seal integrity avoids contamination and leaking. Colour constancy ensures brand standards throughout reorders. Lead time reliability aids inventory planning and market response. Our 25 years of manufacturing expertise and solid quality procedures ensure procurement teams' operational stability. Evaluation of suppliers based on certifications, manufacturing capacity, technical assistance, and long-term relationship potential decreases supply chain risk.
Sustainable and Eco-Friendly Stand Up Pouch Solutions

Environmental sustainability is a procurement issue as rules tighten and customers expect sustainable products.
Recyclable Material Options
Traditional multilayer constructions of stand-up pouches are complicated, making recycling difficult. Innovative mono-material developments employing polyethylene or polypropylene across all layers allow recycling using current streams. Our recyclable packaging supports circular economy concepts and barrier performance. Recycling icons and disposal instructions may show brands' environmental efforts.
Compostable and Biodegradable Alternatives
Renewable plant-based films provide end-of-life benefits for some applications. Dry items with shorter shelf lives benefit from these materials. Certified compostable packaging corresponds with environmental positioning for brands entering sustainability-focused markets, but performance restrictions demand careful application matching.
Environmental Manufacturing Practices
Production processes have a big environmental impact for stand up pouches. Our regenerative thermal oxidizer (RTO) reduces air pollution by capturing and neutralising volatile organic compounds during printing and laminating. Equipment that saves energy reduces the carbon footprint per unit. Waste reduction initiatives optimise production planning to reduce scrap. Procurement teams increasingly assess suppliers based on environmental management systems since manufacturing practices impact regulatory compliance and company sustainability.
Practical Tips for Using and Recycling Stand Up Pouches
From filling to disposal, packaging performance must be optimised.
Optimizing Filling Line Performance
Dimensional uniformity makes vertical form-fill-seal and pre-made pouch filling systems work well. Material thickness impacts machine compatibility and handling. Heat seal parameters must match film structure for dependable closures without barrier damage. Our technical team tests filling equipment compatibility and recommends parameters to avoid expensive production delays. Operators learn pouch handling, orientation verification, and quality inspection to guarantee output uniformity.
Maintaining Product Freshness and Quality
Good storage protects empty pouches and full items. Controlled temperature and humidity avoid material deterioration before use. Sealed storage prevents contamination and odour absorption. Inventory rotation keeps materials within specs. To prolong shelf life, store items according to manufacturer instructions after filling. Clear on-package instructions are essential for consumer satisfaction because resealable closures only work when opened.
Supporting Recycling Infrastructure
Labelling and consumer education can help brands dispose of waste while recycling capabilities develop. Consumers make better choices by knowing the main material composition. Working with store take-back programs helps gather goods not accepted curbside. Collaboration with recycling and material recovery organisations improves infrastructure. Brands are sustainability leaders when they buy recyclable structures to reduce waste before widespread recycling.
Conclusion
Flexible pouch packaging has been popular in the food, pet, health, and consumer goods sectors because of its protection, convenience, cost-efficiency, and sustainability. These flexible packages enhance brand visibility and consumer experience for coffee, snacks, supplements, and cosmetics. Reviewing barrier qualities, functional features, printing capabilities, and supplier dependability helps choose the correct solution to ensure package performance throughout manufacturing and market lifespan. As sustainability demands grow, recyclable and compostable alternatives help companies accomplish environmental goals without sacrificing product safety. The packaging landscape changes, yet flexible pouches' space efficiency, barrier performance, and design flexibility keep them relevant across market sectors, and stand up pouches remain a prominent example of how this format combines self-supporting structure with the same protective and aesthetic advantages demanded by modern brands.
FAQ
1. What products work best in stand up pouches?
These flexible packages excel for dry and semi-moist products including snacks, coffee, nuts, dried fruits, pet treats, protein powders, spices, and granular foods. Spouted versions accommodate liquids, sauces, and beverages. Products requiring oxygen and moisture protection particularly benefit from barrier film structures that extend shelf life compared to traditional packaging.
2. How do I determine the right pouch size for my product?
Calculate required volume based on product weight or volume plus appropriate headspace for sealing and gas release if applicable. Consider retail presentation and handling convenience—oversized pouches waste material while undersized versions appear insufficient. Our design team provides sizing recommendations based on your specific product characteristics and target market positioning.
3. Can stand up pouches run on automated filling equipment?
Yes, these packages work with both vertical form-fill-seal machines using rollstock film and pre-made pouch filling systems. Material specifications and dimensional tolerances must match equipment requirements. We provide technical support ensuring compatibility with your existing filling lines or assist with equipment selection for new operations.
Partner With a Trusted Stand Up Pouches Manufacturer

Guoshengli Packaging brings over 25 years of flexible packaging manufacturing expertise to brands seeking reliable, high-performance pouch solutions. Our comprehensive capabilities include advanced VMPET material construction with superior barrier protection, up to 11-color rotogravure printing with spot UV enhancement, and complete customization from material selection through final production. We maintain ISO 9001, BRC, and FDA certifications, ensuring consistent quality and regulatory compliance for international markets. Our production capacity—featuring 7 printing lines, 6 laminating machines, and 49 converting machines—supports both urgent orders with 7-10 day digital printing and standard production with 15-20 day lead times. Whether you need packaging for snacks, coffee, pet treats, supplements, or specialty products, our technical team provides comprehensive consultation on material properties, barrier optimization, and filling line compatibility. Contact our experts at sales@guoshengpacking.com to discuss your specific requirements and discover how our proven manufacturing systems deliver packaging that performs consistently, order after order. Experience the difference of working with a stand up pouches supplier committed to reducing your operational risk while supporting long-term growth.
References
1. Robertson, Gordon L. "Food Packaging: Principles and Practice, Third Edition." CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, Volume 72, 2007.
3. Selke, Susan E.M., John D. Culter, and Ruben J. Hernandez. "Plastics Packaging: Properties, Processing, Applications, and Regulations, Third Edition." Hanser Publications, 2015.
4. Yam, Kit L. "The Wiley Encyclopedia of Packaging Technology, Third Edition." Wiley, 2009.
5. Coles, Richard and Mark Kirwan. "Food and Beverage Packaging Technology, Second Edition." Wiley-Blackwell, 2011.
6. Brody, Aaron L. and Kenneth S. Marsh. "The Wiley Encyclopedia of Packaging Technology, Second Edition." John Wiley & Sons, 1997.
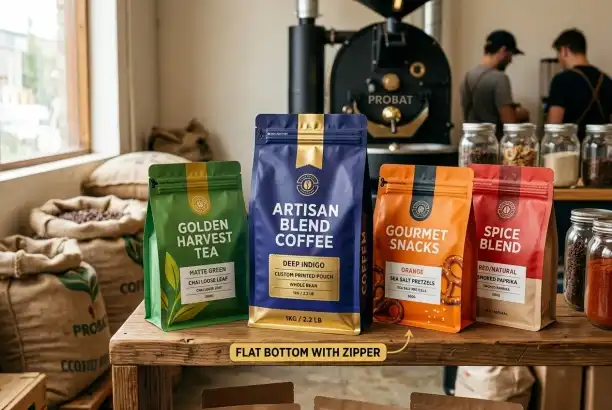
Custom flat bottom pouches with zippers are just what you need for today's competitive markets when you need packaging that will stay put on store shelves and keep contents fresh through multiple uses. Our 250g custom flat bottom pouch is stable like a box and easy to reseal, making it a smart way to protect products from the time they are made until they are eaten. Multiple layers of barriers protect these bags from wetness, air, and light. They are also easy to open and close with notches and zippers that stay closed, even after being opened many times.
Understanding 250g Custom Flat Bottom Pouches with Zipper
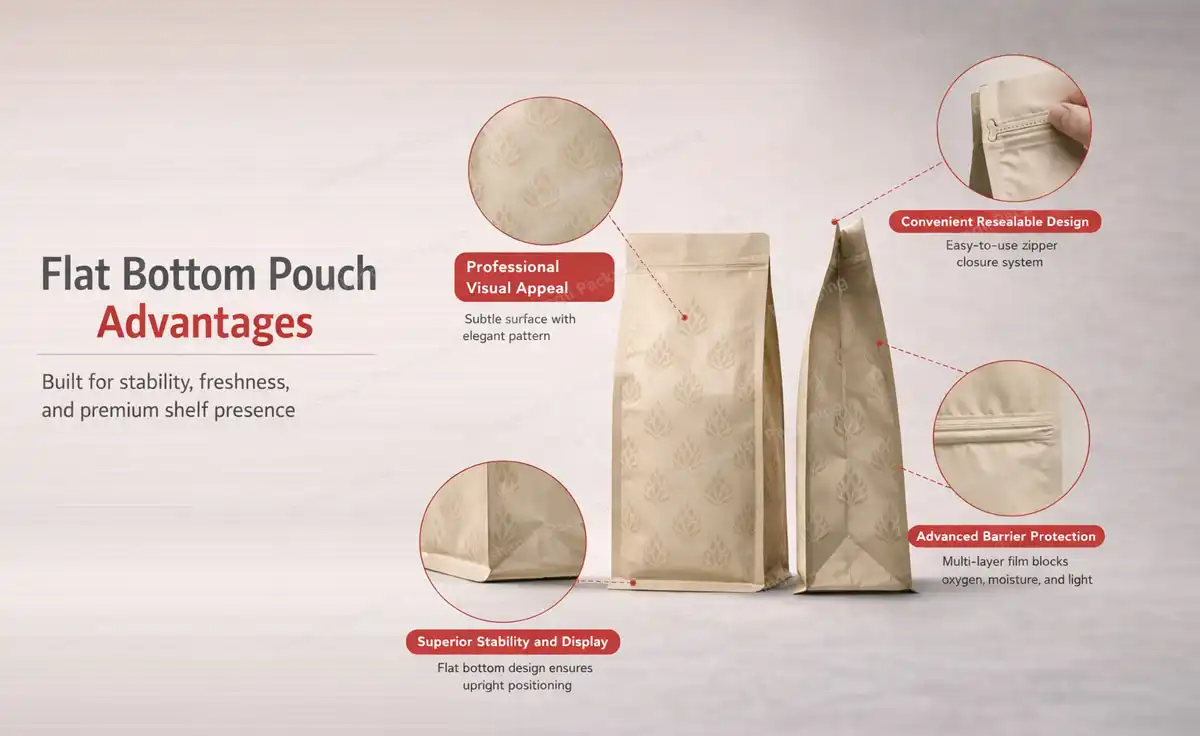
What Makes Flat Bottom Pouches Different
Box-style bags are a big step forward in the design of bendable packaging. Traditional stand-up pouches are stable because their gussets are folded, but flat bottom designs have five separate panels: the front, the back, two side gussets, and a fully flat base. This makes a structure that stands straight even before it is filled. This special design makes it stand out more on the shelf than regular pouches, which can lean or fall over when they're half full.
These bags' engineering strikes a mix between making good use of materials and keeping the structure strong. The flat base spreads the weight evenly across the bottom panel, and the side gussets expand to fit the size of the object. This design stops people from tipping and gives the store a professional look that makes customers feel more confident at the point of sale.
Material Composition and Barrier Technologies
Modern flat bottom pouches with zippers utilize sophisticated laminate structures tailored to specific product protection requirements. Common material combinations include:
- PET/PE Laminates provide excellent moisture resistance and puncture strength, making them suitable for dry snacks, coffee, and pet treats. The polyester outer layer accepts high-quality printing, while the polyethylene inner layer creates reliable heat seals.
- PET/Foil/PE Structures offer maximum barrier protection against oxygen, light, and moisture. This configuration extends shelf life significantly for sensitive products like ground coffee, protein powders, and specialty food ingredients that degrade when exposed to environmental factors.
- Kraft Paper Composites meet growing sustainability demands while maintaining functional performance. These structures typically combine kraft paper exterior layers with thin barrier films, creating packaging that feels natural yet protects contents effectively.
Our factory can make laminate structures that are unique to your product and meet the requirements for its shelf life using all of these combinations of materials. We improve the protective qualities without adding extra thickness to the material, which would raise costs and have a negative effect on the environment.
The Functional Advantage of Zipper Closures
With resealable zippers, single-use boxes can be turned into cases that can be used more than once and keep food fresh for weeks. It's especially important for products that are eaten slowly, like coffee, pet food, snacks, and supplements, to have reliable reclosure mechanisms.
Precise manufacturing control is needed for good zipper fitting in a 250g custom flat bottom pouch. The zip needs to be able to close all the way along its length while still being easy to open and close many times. Customers will complain about the product and the brand will be damaged if the zipper is placed wrong or the adhesive is not strong enough. As part of our production process, we check the quality of the zipper line, seal strength, and opening force to make sure that the product always works the same way.
Eco-Friendly Material Options
Sustainability affects purchase decisions in every market. Our environmentally friendly choices fulfil product safety standards:
- Normal recycling techniques may recycle mono-material assemblies with suitable polymer layers. Mixed-material laminates block more light than these designs, but they're appropriate for moderately protected objects.
- Addition of post-consumer recycling reduces new material use while meeting food contact safety standards.
- RTO exhaust gas treatment removes volatile organic compounds from printing and laminating in our factory. This makes production considerably greener than before.
How to Choose the Right 250g Flat Bottom Pouch with Zipper for Your Product
Evaluating Barrier Requirements
Safety relies on product sensitivity. Coffee requires oxygen barriers to preserve volatile taste compounds. Pet food must be moisture-resistant to maintain texture and prevent microbial growth. Protein powders should be kept away from air and water to maintain their nutritional value and prevent sticking.
Knowing your product's shortcomings helps us create laminate constructions. In our barrier tests, we measure oxygen, water vapour, and light passage using standard methods. These steps ensure that your packaging keeps your products safe for the expected storage term.
Accuracy in measurements matters too. For automated packaging equipment to operate, pouches must retain the same size to avoid becoming caught, misaligned, or not sealing. Our converting equipment ensures high-speed packaging lines work smoothly by keeping crucial dimensions.
Zippered Versus Non-Zippered: Cost-Benefit Analysis
When compared to standard heat-seal closures, adding zipper functionality raises the cost of packaging by about 15 to 25 percent per unit. This investment makes sense when resealability clearly adds value for end users—products that are used more than once benefit a lot from being able to reclose them.
Products that are offered in single-serving amounts or are eaten right away may not need the extra cost of a zip. We help procurement teams make this choice by looking at how the product is used, how it compares to other products on the market, and what the target customer wants.
For example, zippers work well on retail packaging for consumers, but easier closures work better on food service or institutional sizes where the contents are moved to other containers after being opened.
Customization Techniques That Enhance Brand Impact
How the surface is finished has a big impact on how appealing the shelf is and how people feel about the brand. Matte finishes give things a high-end, classy look that health and speciality food brands like. Gloss finishes are great for snack foods and pet products because they make colours stand out and shine brightly.
We can do both rotogravure printing and digital printing for a 250g custom flat bottom pouch. Rotogravure printing has wait times of about 15 to 20 days and always makes high-quality prints, even when doing a lot of them. Digital printing lets you print fewer products and get them to you faster (usually 7–10 days), which makes it perfect for testing the market, launching a new product, or making seasonal products.
Transparent windows let people see the products inside, which boosts their trust by letting them see the product before buying it. Placing windows correctly requires careful planning to keep the structure's strength and blocking qualities while also showing off the product's look well.
Applications and Use Cases of 250g Flat Bottom Pouches with Zipper
Coffee and Tea Packaging Solutions
When it comes to packing, speciality coffee roasters have their own problems. Freshly roasted beans keep giving off carbon dioxide for days after they've been roasted, so they need one-way degassing valves that let the gas leave but not the oxygen. Our flat-bottom coffee pouches have these valves built in without any problems, and the zippers still work for your convenience.
The stable base design makes coffee branding look great, and the four vertical panels give you plenty of room for information about the coffee's origin, grinding, and drinking suggestions. A lot of roasters have clear windows on the front that let customers see the quality of the beans and the level of roasting before they buy them.
Moisture barriers and reusable seals that keep delicate flavour profiles safe are also good for tea packing. Loose-leaf tea needs extra care because humidity can make it clump together and lose its flavour over time.
Snack Food and Dried Fruit Applications
Chips, nuts, dried fruits, and other similar foods need to be packaged in a certain way to keep their texture. The main quality issue for these groups is that they lose their brightness when moisture gets in. Our multi-layer laminates keep the right amount of moisture in them while they are being shipped and used by customers.
When compared to bag-style packaging, which needs to be hung or laid flat, the flat bottom pouch format makes for efficient shelf displays that make the most of facings per linear foot. Retailers like packaging that makes the best use of expensive store space and presents products in a way that looks good.
Portion control is becoming more important as people look for easy, pre-measured amounts. The 250g size is good for normal family use because it's big enough to provide value but small enough to keep fresh during normal use cycles.
Pet Food and Treat Storage
When pet owners buy treats and extra food for their animals, they look for things that are fresh and easy to use. Resealable pouches are a good solution for both problems because they keep the quality of the product and make it easier to store and use.
Keeping smells in check is another important thing to think about. Good barrier films stop smells from moving and affecting other kept foods or making your home smell bad. This also keeps the food's taste, since many pet foods and treats lose their appeal when volatile flavour compounds break down.
Our food-grade materials and production approvals make sure that products meant for animals are safe to use. We keep our BRC approval for packaging pet food, which means we meet the quality standards set by retailers and brands.
Health Supplements and Protein Powders
For powder to flow and not clump, the moisture level needs to be carefully managed. Hygroscopic ingredients are often found in protein powders, vitamin supplements, and other speciality nutrition products. These ingredients easily absorb water, which can make the texture of the product and the amount of water that it takes in inconsistent.
High-barrier pouches keep the low-moisture environment that powder needs to stay stable. When compared to non-resealable packaging that lets moisture in with each use, zip seals keep products from getting damaged when they are opened more than once.
On flat-bottom designs with clear labelling space, you can put full supplement facts panels, usage directions, and the regulatory statements that are needed for health goods. This information is presented in a clear and professional way by the organised style.
Practical Packaging Ideas for Brand Recognition
Visual distinction helps you stand out in crowded markets. We assist businesses in finding new packaging perspectives by:
- Custom colour matching ensures the brand appears the same across goods and packages. Our rotogravure printing makes accurate colour copies with 11 ink stations.
- Touchable textures make people want to connect with the product. Soft-touch coatings provide luxury, while etched components highlight brand names or characteristics.
- Different flat bottom shapes give brands personalities. Bags with die-cut hang holes, zipper pulls, or handles are more functional.
Procurement and Ordering Guide for 250g Custom Flat Bottom Pouches with Zipper
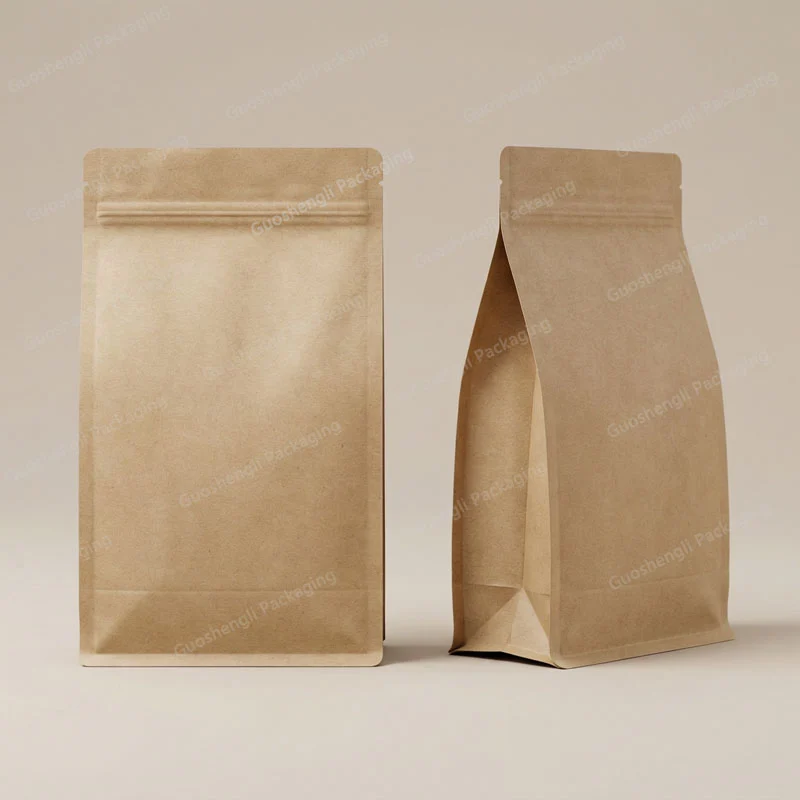
Step-by-Step Ordering Process
Creating clear specifications is the first step to a successful custom packing job. During the initial meetings, we help clients choose the right material, finalise the dimensions, and integrate features—whether for a 250g custom flat bottom pouch or other formats. This way of working together avoids misunderstandings and makes sure that the finished pouches meet the requirements for their purpose.
Sample production lets you test things physically before committing to large quantities of production. We offer pre-production samples that show the real materials, printing quality, and how well the structure works. This step looks for possible problems while fixes are still easy and cheap.
Production wait times change based on the type of printing the order is and how big it is. Digital printing jobs are usually done 7–10 days after the artwork is approved. For rotogravure printing, the barrel has to be made and set up, which adds 15 to 20 days to the process. We suggest that you plan your inventory needs ahead of time, especially for seasonal products or campaigns that use them.
Understanding Minimum Order Quantities and Pricing
MOQ requirements streamline manufacturing and give customers many options. Digital printing enables you to produce 5,000–10,000 pieces at once, which is useful for innovative goods or niche markets. Rotogravure printing requires 20,000 or more units to justify the cylinder investment, but it has lower ongoing production costs.
Bulk orders are quite cost-effective. Big savings can result from buying more materials, fewer setups, and better production schedule planning. Our pricing clearly demonstrates how prices vary by number. This helps buying managers decide when and how much to order.
Factors impact unit pricing beyond number. Material type greatly affects cost; high-barrier foil laminates cost more than plastic films. Adding buttons, vents, or windows gradually raises the price. The pricing depends on the quantity of colours, print area size, and special finishing.
Selecting Reputable Suppliers and Building Partnerships
Technical support and quality control are available directly from the factory, eliminating middlemen markups. Communicating with makers enables you to discuss modifications, plan production, and handle issues swiftly.
Supplier trust grows with quality assurance transparency. We list all materials, test results for barrier properties and seal strength, and inspection reports showing quality control checks during production. This documentation supports your quality plans and tracks products across supplier chains.
Long-term collaborations benefit both parties beyond transaction expenses. After building contacts, you may obtain assistance arranging your supply, create new goods, and book first during peak demand. It costs money to learn about our customers' operations, estimate what they'll require, and recommend improvements before they materialise.
Clear communication is crucial for international sourcing. Our team uses straightforward business language when discussing technical topics to avoid misconceptions that might lead to production errors or mismatched specs. For all orders, modifications, and agreements, we provide full written confirmation.
Innovations and Future Trends in Flat Bottom Pouch Packaging
Emerging Sustainable Material Solutions
Consumer preferences and regulatory pressures drive packaging sustainability innovation. Extended producer responsibility regulations in Europe and similar initiatives in North America require brands to plan packaging end-of-life.
Development of mono-material structures is promising. These designs, such as a 250g custom flat bottom pouch, allow recycling using existing infrastructure by employing suitable polymers in laminate layers. Performance gains continue to close the mono-material-multi-material barrier property gap.
Biodegradable and compostable films are another option; however, performance and infrastructural issues restrict commercial feasibility. Certain dry products benefit from PLA-based structures, but moisture-sensitive or oxygen-sensitive contents lose protection. Industrial composting capacity is limited in many regions, reducing environmental benefits.
We study and test new materials and introduce proven technology as they achieve performance and commercial viability standards. Our development strategy prioritises real-world solutions above ecologically good but unworkable ones.
Advanced Sealing and Closure Technologies
Tamper-evidence features address safety and quality assurance concerns across food, supplement, and pet food categories. Integrated tear bands provide visible evidence of package integrity, building consumer confidence while protecting brand reputation. These features add minimal cost while delivering substantial risk mitigation value.
Smart packaging technologies incorporating QR codes, NFC tags, or printed electronics enable consumer engagement and supply chain tracking. Brands use these features for authentication, usage instructions, recipe ideas, and loyalty program integration. Implementation costs continue declining, making smart packaging accessible for mid-volume production.
Improved zipper designs enhance usability and durability. Recent innovations include easy-glide profiles requiring less force to open and close, extended zipper life supporting hundreds of open-close cycles, and child-resistant options for products requiring access restrictions.
Enhanced Printing and Customization Capabilities
Digital printing technology advancement enables shorter runs and faster iterations compared to traditional rotogravure methods. This flexibility supports market testing, limited editions, and personalized packaging campaigns that strengthen consumer connections with brands.
High-definition printing delivers photographic image quality and intricate detail reproduction. Extended color gamut printing expands achievable color ranges beyond standard CMYK limitations, enabling more accurate brand color matching and vibrant shelf appeal.
Variable data printing allows individualized package content within production runs. Serialization for traceability, regional language variations, or personalized messaging all become feasible without inventory complications from maintaining multiple SKUs.
Evolving B2B Supply Chain Dynamics
Recent global disruptions elevated supply chain resilience. In procurement networks, brands prioritise supplier diversification, inventory buffer maintenance, and transparency. These changes impact supplier selection and relationship management.
Brands want distinction, raising customisation demands. Standard catalogue goods work effectively for limited applications; most successful packaging projects today customise specifications to product needs and brand positioning.
Leading time compression is difficult. Manufacturing realities clash with buyers' demands for extensive customisation and fast turnaround. Capacity investment, process optimisation, and clear communication about achievable timelines under different specification scenarios address this.
As companies increase manufacturing and distribution, repeat order quality matters more. Packaging that works effectively in first shipments but not in later orders disrupts operations and destroys customer relationships. Our production processes prioritise specification integrity and performance stability throughout the order lifecycle.
Conclusion
Custom flat bottom bags with zip closures fulfil market demands. The 250g custom flat bottom pouch works well for speciality coffee, premium snacks, pet treats, and health supplements. Material innovation, production accuracy, and customisation flexibility provide package solutions that safeguard product integrity, improve brand appearance, and maximise customer convenience. Understanding barrier requirements, weighing feature benefits against costs, and working with reliable suppliers are key to successful procurement. Long-term packaging success depends on choosing experienced manufacturing partners with technical depth and production capability as sustainability standards rise and customisation requests rise.
FAQ
1. What products work best in 250g flat bottom pouches?
Products consumed over multiple occasions benefit most from this format and capacity. Coffee, tea, snacks, dried fruits, pet treats, protein powders, and supplements all perform well. The size provides enough volume for household value while maintaining freshness through normal consumption patterns. The flat bottom design creates excellent shelf presence for retail environments where visual impact drives purchasing decisions.
2. How long does custom pouch production take?
Production timelines depend primarily on printing method selection. Digital printing projects complete within 7-10 days after artwork approval, making them suitable for quick launches or seasonal products. Rotogravure printing requires 15-20 days due to cylinder preparation and setup requirements but delivers superior quality for large production runs. We recommend planning inventory timing accordingly and ordering samples before committing to full production quantities.
3. Can flat bottom pouches with zippers run on automated filling equipment?
Properly manufactured pouches integrate smoothly with most vertical form-fill-seal and pre-made pouch filling systems. Dimensional consistency and material stiffness specifications must match equipment requirements to prevent jamming or misalignment. We provide technical specifications and can coordinate with equipment manufacturers to confirm compatibility before production. Our quality control processes maintain tight dimensional tolerances essential for automated handling reliability across production shifts.
Partner With Guoshengli Packaging for Your Custom Pouch Needs
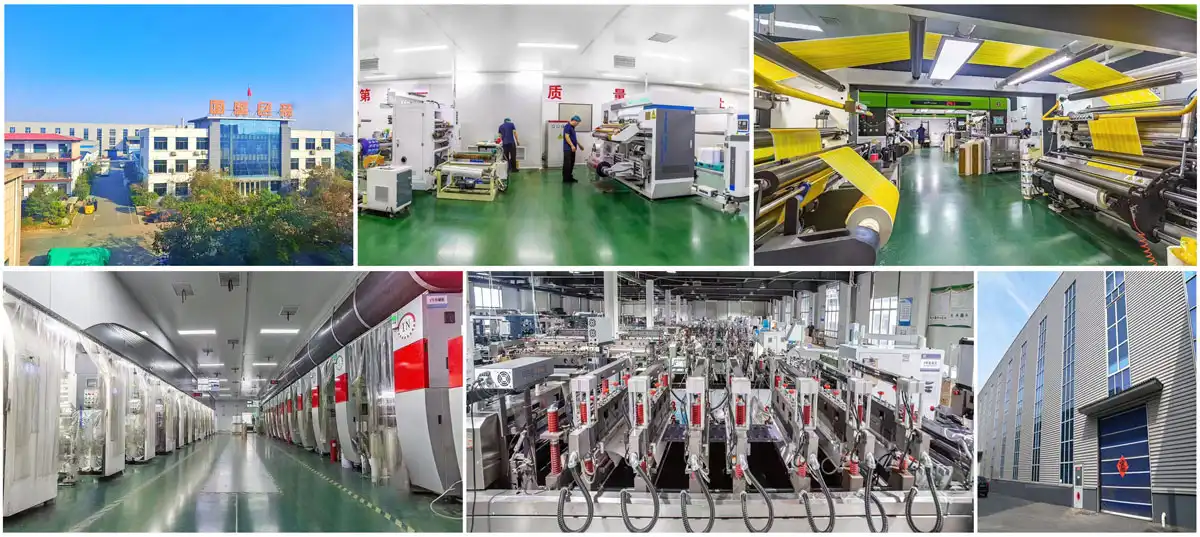
Quality packaging shouldn't create production headaches or compromise product protection. Guoshengli Packaging brings 25 years of flexible packaging manufacturing experience to every custom flat bottom pouch with zipper project we undertake. Our facility operates advanced rotogravure printing, precision laminating, and converting equipment that delivers consistent results across repeat orders—not just initial shipments. We maintain ISO 9001, BRC, FDA, and SGS certifications that meet international quality standards and support your compliance requirements. Whether you need 250g custom flat bottom pouch solutions for coffee, pet food, supplements, or specialty products, our engineering team designs packaging matched to your specific barrier requirements, filling equipment, and brand positioning. Contact our team at sales@guoshengpacking.com to discuss your project specifications with experienced flat bottom pouch manufacturers who understand B2B procurement priorities and deliver reliable packaging that performs consistently in real production environments.
References
1. Robertson, Gordon L. Food Packaging: Principles and Practice. 3rd ed. CRC Press, 2012.
2. Marsh, Kenneth and Betty Bugusu. "Food Packaging—Roles, Materials, and Environmental Issues." Journal of Food Science, vol. 72, no. 3, 2007, pp. 39-55.
3. Selke, Susan E.M., et al. Plastics Packaging: Properties, Processing, Applications, and Regulations. 3rd ed. Hanser Publications, 2015.
4. Coles, Richard and Derek McDowell, editors. Encyclopedia of Packaging Technology. 3rd ed. Wiley, 2011.
5. Yam, Kit L., editor. The Wiley Encyclopedia of Packaging Technology. 3rd ed. John Wiley & Sons, 2009.
6. Emblem, Anne and Henry Emblem. Packaging Technology: Fundamentals, Materials and Processes. Woodhead Publishing, 2012.
You can choose between a 1kilo side gusset pouch with valve and a flat-bottom coffee bag based on your brand's needs. If keeping the coffee fresh for longer and saving room are the most important things to you, side gusset pouches with degassing valves are the best option because they let CO2 out while blocking oxygen in. However, flat bottom bags stand out more on the shelf because they are shaped like boxes and have a larger surface area for marking. Both types of barriers are strong, but side gusset designs usually cost less to ship and work better with automatic filling lines. Your choice should be based on the features of the product, how it will be distributed, and whether your market positioning is based on freshness or visual impact.
Introduction
The way businesses buy and sell things has changed a lot when it comes to coffee packaging. Brands now want solutions that protect the purity of their products, make them look better on shelves, and make operations easier. Finding the right structure for one-kilogram coffee pouches means finding a balance between keeping the coffee fresh, making sure the bags work with other machines, and making the brand stand out. Side gusset pouches with valves and flat bottom coffee bags have become the most popular options. Each has its own technical and business benefits.
Side flap designs with built-in degassing holes solve the unique problem of freshly roasted beans giving off CO₂, which stops the pouch from expanding and going bad. Flat bottom structures, on the other hand, have a stable, rectangular footprint that makes them stand out visually. Procurement professionals can make smart choices that are in line with supply chain goals and market standards when they know how these forms differ in terms of barrier performance, filling efficiency, and branding potential.
This analysis makes things clear for packaging engineers, distributors, and brand managers who are investing in coffee packaging. To help you make your choice, we look at changes in structure, performance measures, buying factors, and actual usage issues.
Understanding Side Gusset Pouches with Valve and Flat Bottom Coffee Bags
Structural Design and Core Functionality
Side gusset pouches with valve have vertical expansion pleats on both sides, which lets the package hold more while still being small and saving space. The built-in one-way degassing valve is designed to let out the CO₂ that freshly roasted coffee beans give off while blocking oxygen from the outside.
Multi-layer laminate structures like PET/AL/PE or MOPP/VMPET/PE are often used in a 1 kg side gusset pouch with valve. These structures provide excellent protection against moisture, oxygen, and light. The thickness is between 120 and 160 microns so that it can hold a one-kilogram load without warping while it's being moved or stored. The side gussets spread the weight evenly across the base, which stops stress from building up that could damage the seal.
Flat bottom coffee bags, on the other hand, make the most of shelf space by having a strong rectangular base that lets the pouch stand up straight without any help. This design makes the front display area bigger, which is great for big branding and high visibility in stores. Flat bottom formats can also have valves, but their main benefit is the quality look and box-like stability that shoppers like when they're browsing store shelves, compared with a 1kilo side gusset pouch with valve.
Material Selection and Barrier Properties
High-barrier laminates can be used in both formats, but the choice of material is usually based on the needs of the application. Most side gusset bags with valves focus on keeping out as much air and wetness as possible to keep food fresh longer in storage and delivery settings. Some flat-bottom bags may have clear window films or special finishes added to them to make them look better, even if it means sacrificing some of their barrier performance.
The valve itself is an important point of quality control. Using vacuum methods to test the functionality of valves makes sure that air can only flow in one direction and not backwards. Tests that measure burst pressure show that side gusset seals can handle the stress of a full kilogram load. Oxygen Transmission Rate and Water Vapour Transmission Rate tests show that the barrier is strong enough to meet FDA and EU food contact compliance standards.
Performance and Functional Comparison
Freshness Preservation and Shelf Life Extension
Side gusset pouches with valves keep coffees that are sensitive to smells fresh longer. The degassing valve solves the biggest problem in the business, which is keeping the inside of the pouch oxygen-free while stopping the pouch from bloating. Over the next 7 to 14 days after being roasted, freshly roasted beans give off large amounts of CO2. Without a valve, internal pressure can build up and break the seal or make packaging take longer than planned. This problem is solved by the one-way valve, which lets you pack right away while keeping the best flavour and taste.
When used in side gusset designs, multi-layer barrier films offer strong protection against air, moisture, and light. This security can be seen through increased shelf life tests. When kept in controlled settings, properly made bags can keep coffee fresh for an extra 12 to 18 months. The small size cuts down on headspace, which lowers the amount of air left over that speeds up the staling process.
It is also possible to integrate valves into flat bottom bags, which can provide similar barrier performance. Their advantage comes from being able to handle bigger batches and making it easier to see the products inside through clear panels. Brands that want to be seen as high-end often choose flat bottom forms because they look more expensive, even if it means paying a little more for materials and needing more space to store them.
Space Efficiency and Logistics Optimization
A 1-kilogram side gusset bag with a zipper makes sending and storing things more efficient. When it's full, the side gusset design expands to its full size, but it stays narrower than flat-bottom versions of the same thing. This means fewer pallets, lower freight costs, and better use of warehouse space, all of which are important for B2B buyers who handle large orders.
Even though flat-bottom bags look nice, they take up more room per unit. Because their bases are rigid, they can't be nested or stacked as well as side gusset formats. Because of these logistical benefits, distribution centers that ship a lot of coffee often choose side gusset pouches with valves. This is especially true when shipping internationally.
Printing Capabilities and Brand Differentiation
Both types can handle high-quality rotogravure printing, which can produce images with up to 11 colours that catch people's eyes. Side gusset bags, including 1kilo side gusset pouch with valve, have four printable areas: the front, the back, and the two side panels. This gives you a lot of room to put your logo on them. The vertical layout works well with big graphics and a clear hierarchy of product information.
The stable, box-like shape of flat bottom bags makes them great for making a statement on the shelf. The front panel can be used as a natural sign, and the flat base can have more branding elements added to it. Premium coffee brands that want to sell in stores often choose this format to stand out from competitors who use standard pillow pouches.
Procurement Considerations for B2B Buyers
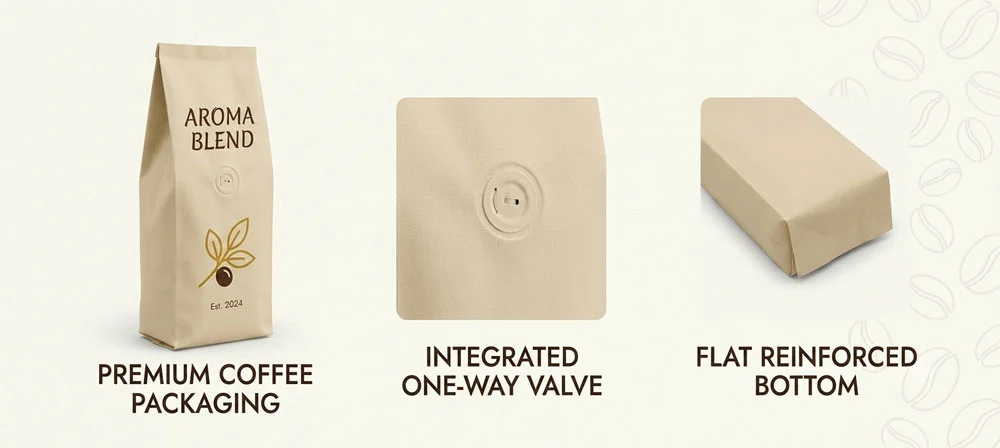
Cost Analysis and Pricing Structures
Because they use less material and are easier to make, side gusset sacks with valve usually cost 15 to 25 percent less per unit than similar flat bottom bags. For custom-printed rotogravure production, the minimum order quantity varies by supplier but is usually between 10,000 and 30,000 units. With digital printing, MOQs can be as low as 5,000 to 10,000 units, which makes them more suitable for smaller names or test market launches.
Lead times are different for each format and printing method. Rotogravure printing takes 15 to 20 days from the time the artwork is approved until the side gusset pouches with valve are delivered. For rush orders or seasonal products, digital printing cuts this time down to 7–10 days. Due to more complicated changes, flat bottom bags may add 2–5 days to wait times.
Due to their small size, side gusset designs are cheaper to ship. It usually takes four to five days to ship by air, and twenty to thirty-five days to ship by sea, depending on where it's going. When you add up all the costs, like packing, printing, and shipping, side gusset bags with valves are often the best deal for high-volume businesses.
Supplier Evaluation and Quality Assurance
Reliable makers show uniform quality across multiple orders, which is an important factor that is often missed when choosing the first provider. Baseline guarantee comes from ISO 9001 quality management approval, BRC food packing accreditation, and FDA compliance paperwork. Third-party testing results from SGS back up claims about the performance of barriers and the safety of the materials.
When processes are scaled up, production ability is important. Multiple rotogravure printing lines, advanced binding equipment, and precise pouch-making tools in a facility lower the risk of bottlenecks during times of high demand. Suppliers who offer in-house testing and inspection at every important stage reduce the number of defects that stop the filling line from working.
Professional packing partners are different from product providers because they can communicate clearly and offer expert help. You can expect thorough information about the materials, drawings of the sizes, and data on how well the valves work. Beyond just supplying products, manufacturers who offer design advice, artwork optimisation services, and filling trial help add a lot of value.
Sustainability and Eco-Friendly Options
Environmental duty is becoming more and more important when it comes to buying things, especially for brands that want to sell in Europe and North America. Using single-material PE or PP laminates in recyclable packaging supports the idea of a circular economy while still having good barrier properties for coffee uses. Compostable PLA/PBAT-based solutions are useful for people who care about the environment, but they need to be carefully tested for shelf life performance.
Concerns about sustainability come up with degassing valves themselves. Traditional valve materials have a lot of plastic parts that make recycling harder. New solutions for biodegradable valves are addressing this issue, but they are still not widely available in the market. When suppliers spend money on eco-friendly valve solutions, they show that they are ahead of regulation trends and buyer tastes.
The ways things are made are also important. RTO exhaust gas treatment systems keep printing and laminating operations as environmentally friendly as possible. Certifications that show sustainable practices improve the story of a brand and meet retailer needs in markets that care about the environment.
Matching Packaging Solutions to Your Brand Needs
Segment-Specific Recommendations
Side gusset pouches with valves are best for coffee roasters who want to keep their coffee fresh and save money. The improved degassing technology, better barrier protection, and better transportation optimisation work well with wholesale distribution models where keeping the integrity of the product during long storage periods is very important. This format is perfect for medium- to large-volume operations that handle 1-kilogram bulk packages because it keeps the smell and taste of the food fresh throughout the supply chain.
Speciality coffee brands that want to stand out on store shelves and be seen as high-end should think about using flat-bottom bags. The high-end design gets people's attention in busy stores, which makes up for the slightly higher packing costs by improving how people see the brand. This format is good for artisan roasters who want to sell to gourmet markets where visual differences are important for making decisions about what to buy.
Side gusset pouches with valves are also used by companies that make pet food and health supplements to package powdered products. The 1kilo side gusset pouch with valve shape is flexible enough to fit a wide range of dry goods that need to be kept dry and under controlled pressure while they are stored. The side panels that can be expanded make it easier to pour, which is good for customers in both store and food service settings.
Automated Packaging Line Compatibility
Compatibility with the filling line is an important but often overlooked factor in choosing packaging. Side gusset pouches with valves usually work well on vertical form-fill-seal machines and pre-made pouch fillers because they have consistent sizes and behave in predictable ways, which cuts down on downtime. Precision in valve placement affects the trustworthiness of the seal, which is why quality control standards set by the maker are so important.
To make the hard base that is typical of flat-bottom bags, you need special making tools. Not all filling lines can be used with this style without being changed. Checking for compatibility before placing big orders avoids the need for expensive updates or retrofitting. By asking for filling trials with sample bags, problems can be found before full production starts.
Practical Usage and Storage Tips for Side Gusset Pouches with Valve
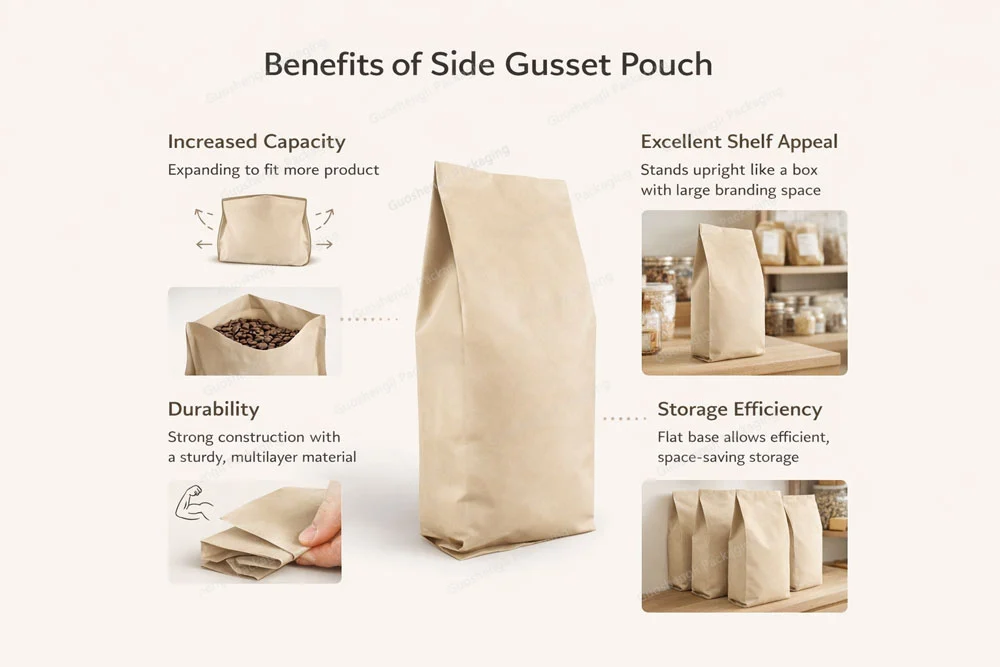
Understanding Valve Mechanics
The one-way degassing valve works with a thin silicone membrane that opens when pressure inside the valve rises, letting CO2 escape while keeping air from the outside out. The best valve performance depends on how well it is calibrated to the coffee. For example, valves that need slightly lower opening limits are needed for darker roasts because they give off more gas. Valve placement is usually in the upper third of the back panel of the pouch to make it easier for gas to escape when the package is kept upright.
Filling and Sealing Best Practices
Using the right filling methods will increase the shelf life and lower the number of defects. To avoid problems with under- or over-filling, filling machines should always give accurate weights within ±2 grams. Keeping the right amount of headspace—usually between 15 and 20 mm—allows for changes in internal pressure without putting too much stress on seals. Temperatures between 160°C and 180°C, stay times between 1.5 and 2 seconds, and sealing pressures between 0.4 and 0.6 MPa are all important factors for heat sealing that need to be carefully calibrated.
The conditions of storage have a big effect on how well packing works. To keep things from breaking down because of moisture, warehouses should keep the temperature between 15°C and 25°C and the relative humidity below 60%. Palletised bags are better protected by wrapping that keeps them from getting damaged by light or handling. Following the first-in, first-out rule of regular rotation makes sure that customers get older stock within the best freshness windows.
Common Issues and Troubleshooting
Fine coffee droplets can sometimes block the membrane and cause the valve to get stuck. This risk is kept to a minimum by keeping production areas clean and adding inner screens to equipment used for filling. Limiting the height of the pallet and putting protective dividers between layers can stop the pouch from deforming under the weight of storage. Most seal failures are caused by incorrect heat-sealing settings or dirt along the seal areas. These problems can be fixed by properly teaching operators and maintaining equipment on a regular basis.
Conclusion
Which side gusset pouches with valve to use versus flat bottom coffee bags depends on how your brand wants to protect freshness, run its business efficiently, and place itself in the market. Side gusset forms are great for extending the shelf life of goods, cutting down on transportation costs, and working with automatic systems that handle large amounts of work. Flat-bottom bags stand out more on the shelf and are easier to see in stores. When designed correctly, both formats offer strong barrier properties, but the 1kilo side gusset pouch with valve consistently performs better for B2B buyers who value product integrity and cost-effectiveness across long supply chains.
FAQ
1. Can side gusset pouches with valves include resealable features?
Resealable zipper closures can be integrated into side gusset pouches with valves, combining degassing functionality with consumer convenience. This combination suits retail packaging where customers purchase one-kilogram quantities for home use. The zipper placement occurs below the valve, preserving freshness after initial opening. Manufacturing complexity increases slightly, affecting minimum order quantities and unit costs. Brands targeting premium retail segments find resealable formats enhance perceived value and repeat purchase rates.
2. What are typical minimum order quantities for custom-printed pouches?
Rotogravure printing requires 30,000-50,000 units to justify cylinder engraving costs, though some manufacturers accept 10,000-unit minimums with surcharges. Digital printing reduces MOQs to 5,000-10,000 units, ideal for new product launches or limited editions. Ordering larger quantities reduces per-unit costs through economies of scale. Balancing inventory investment against price optimization requires careful demand forecasting and supplier negotiation.
3. Are biodegradable valves commercially available?
Biodegradable valve technology has advanced significantly, with several manufacturers now offering compostable alternatives made from PLA and other plant-based materials. Performance validation remains critical, as valve reliability directly impacts product freshness. Not all biodegradable valves match conventional petroleum-based versions in pressure tolerance and longevity. Brands committed to sustainability should request testing data and conduct shelf life trials before full-scale adoption.
Partner with a Trusted 1Kilo Side Gusset Pouch with Valve Manufacturer
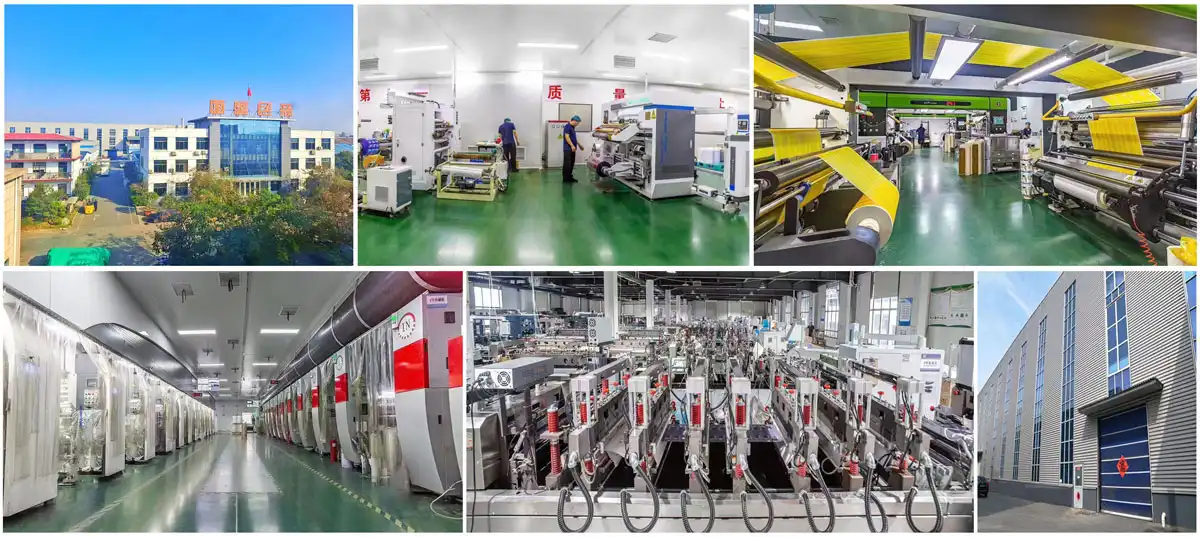
Guoshengli Packaging delivers reliable, export-ready packaging solutions engineered for consistent performance across repeat orders. Our 1kilo side gusset pouch with valve combines 25+ years of manufacturing expertise with advanced production capabilities, including 11-color rotogravure printing, ISO 9001 and BRC certifications, and 100% recyclable material options. We understand that packaging problems rarely appear in samples—they emerge during production scaling and market expansion. Our quality systems prevent costly failures through rigorous barrier testing, valve functionality validation, and dimensional consistency verification.
Whether you're a coffee roaster, pet food manufacturer, or health supplement brand, we provide customized solutions matching your filling equipment, regulatory requirements, and growth objectives. Contact our team at sales@guoshengpacking.com to request samples, discuss your specific needs, or receive detailed technical specifications. We offer flexible MOQs, rapid production timelines—7-10 days for digital printing—and fast global delivery. Connect with a 1kilo side gusset pouch with valve supplier committed to reducing your procurement uncertainty and supporting long-term success.
References
1. Smith, J. & Anderson, K. (2022). Flexible Packaging Engineering for Coffee Preservation: Barrier Properties and Valve Technology. Journal of Food Packaging Science, 15(3), 245-267.
2. Chen, L. (2021). Comparative Analysis of Coffee Packaging Formats in B2B Procurement. International Packaging Research Association, Technical Report Series No. 89.
3. Williams, R. (2023). Sustainability in Flexible Packaging: Materials, Manufacturing, and Market Trends. Packaging Technology Review, 28(1), 112-134.
4. Thompson, M. & Rodriguez, A. (2022). Optimizing VFFS Operations for Side Gusset Pouches with Degassing Valves. Automation in Packaging Conference Proceedings, pp. 567-582.
5. European Coffee Packaging Alliance (2023). Best Practices Guide for One-Kilogram Coffee Pouch Selection and Quality Control. Brussels: ECPA Publications.
6. National Coffee Association (2021). Packaging Impact on Coffee Freshness and Shelf Life Extension: A Technical White Paper. New York: NCA Research Division.